Insights & Updates
What's happening on the floor.
Buyer’s guides, spec references, project milestones, and company updates from FabTek Industries — straight from Hazlehurst, Mississippi.
Buyer’s guides, spec references, project milestones, and company updates from FabTek Industries — straight from Hazlehurst, Mississippi.
“For most fabricators, the grid boom is a national headline. For us, it's a local one.”
A $25 billion wave of hyperscale datacenter investment — anchored by Amazon — has landed in central Mississippi, paired with Entergy's largest grid upgrade to date. The build-out reshaping the national power grid is happening in the same counties FabTek has operated in for years.
When the demand is in the region and the fabrication is in the region, the math gets simple: shorter freight, tighter coordination, and a partner already investing in capacity ahead of the curve in the same state the build is happening.
Read the full storyArticles, announcements, and milestones — written to share. Each post has its own link, so it travels well on LinkedIn and brings readers back here.
Part 17 of 17. How modular data center, power and cooling OEMs and developers specify ISO-dimension frames, insulated shells and equipment fit-out, and how to buy them in series.
Read post →
Part 16 of 17. For data center GCs and developers: how to scope, specify and qualify a fabricator for multi-trade prefabricated modules, and why the frame, spools, duct and enclosures should come from one plant.
Read post →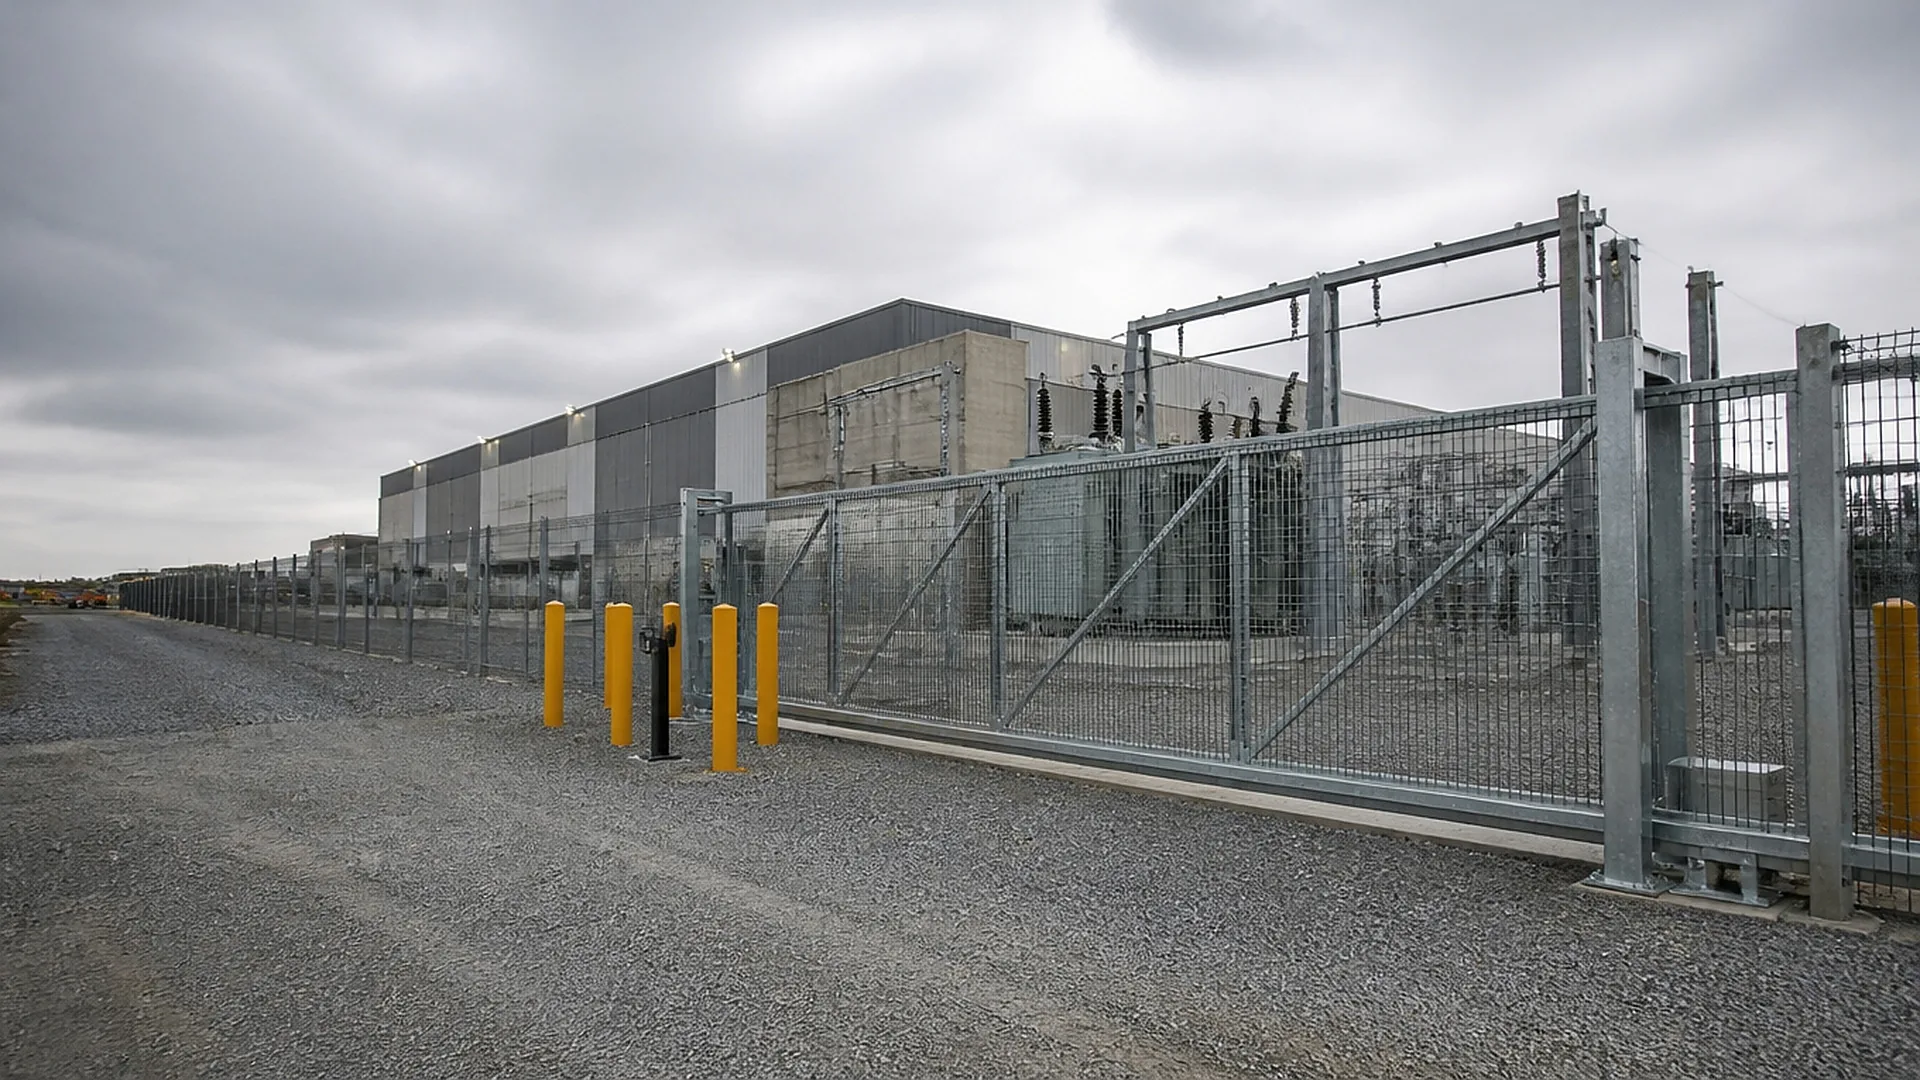
Part 15 of 17. How data center buyers package welded fence panels, cantilever and swing gates, bollards and vehicle barriers into one fabrication RFQ, and what the security spec needs to say.
Read post →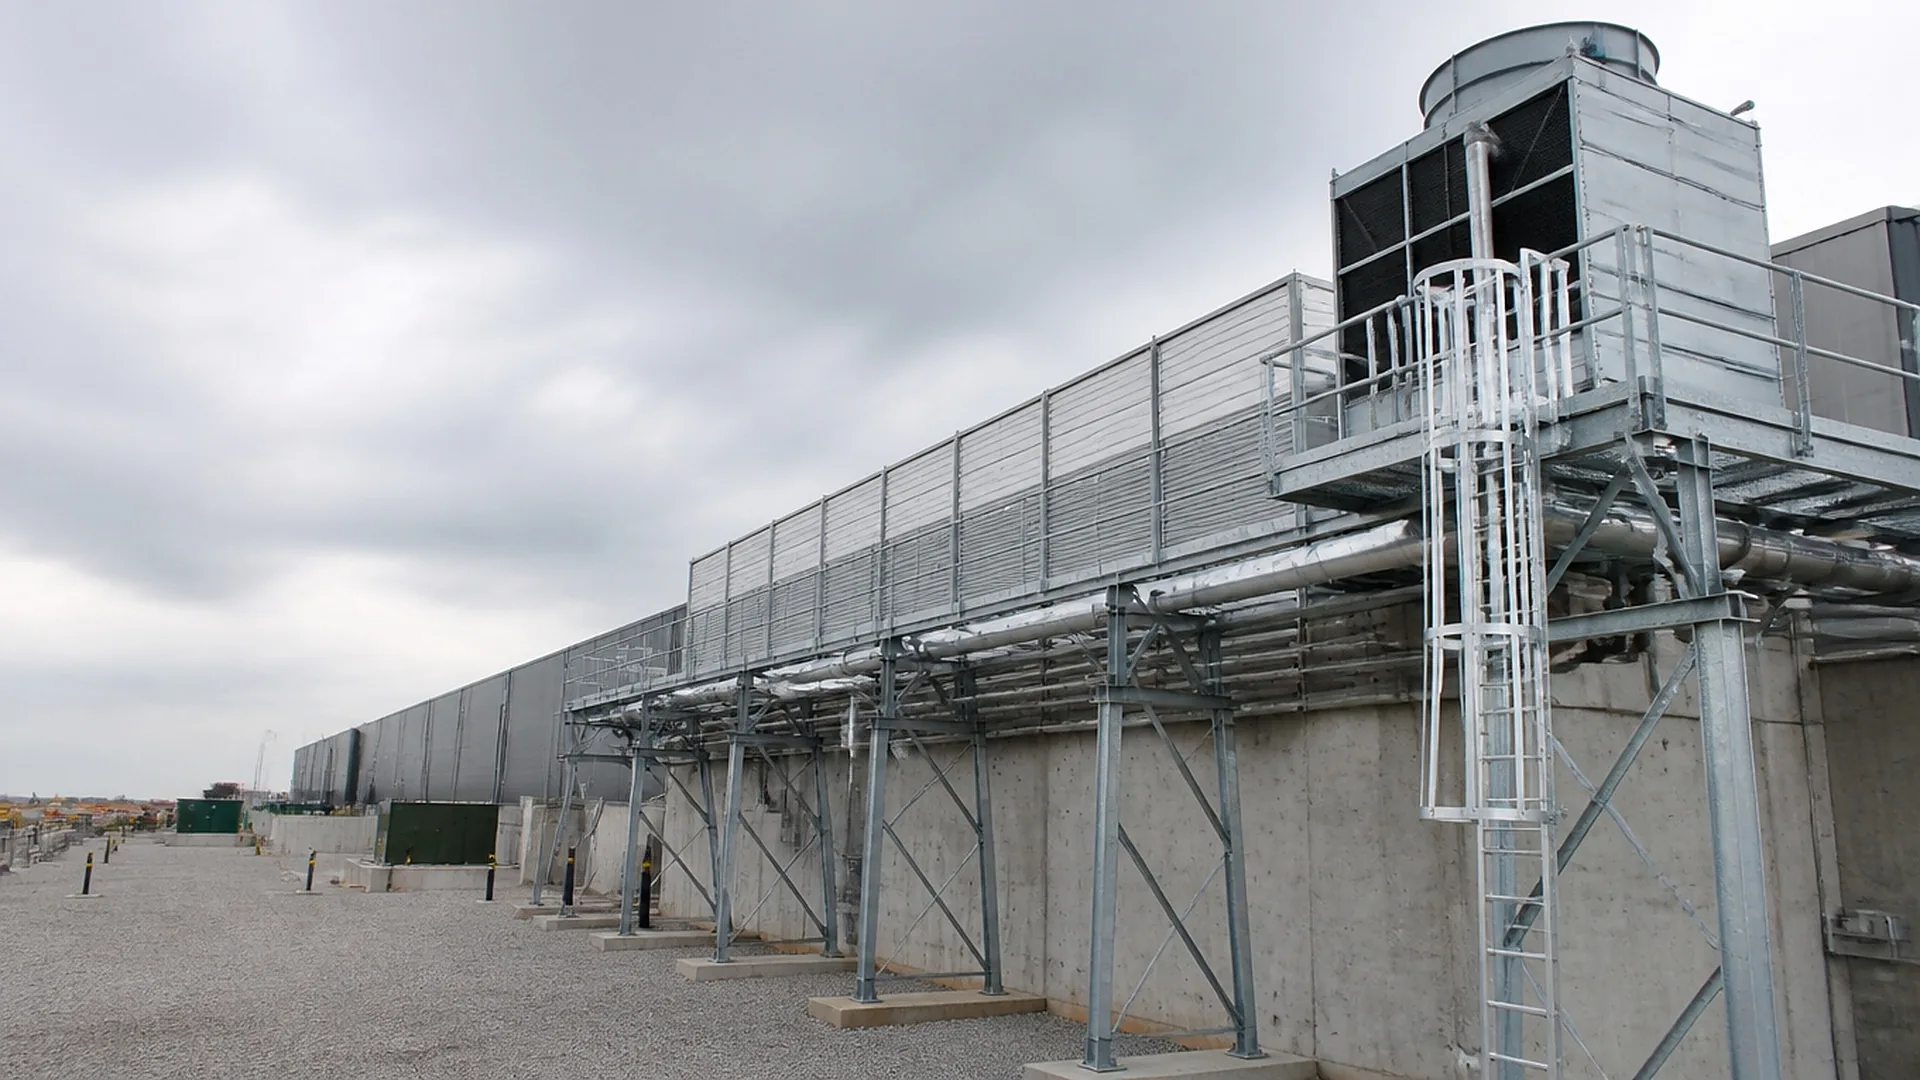
Part 14 of 17. A sourcing guide to the miscellaneous-metals package on a data center campus: access steel to OSHA, rooftop equipment screens to the architect, and how to keep it off the final inspection.
Read post →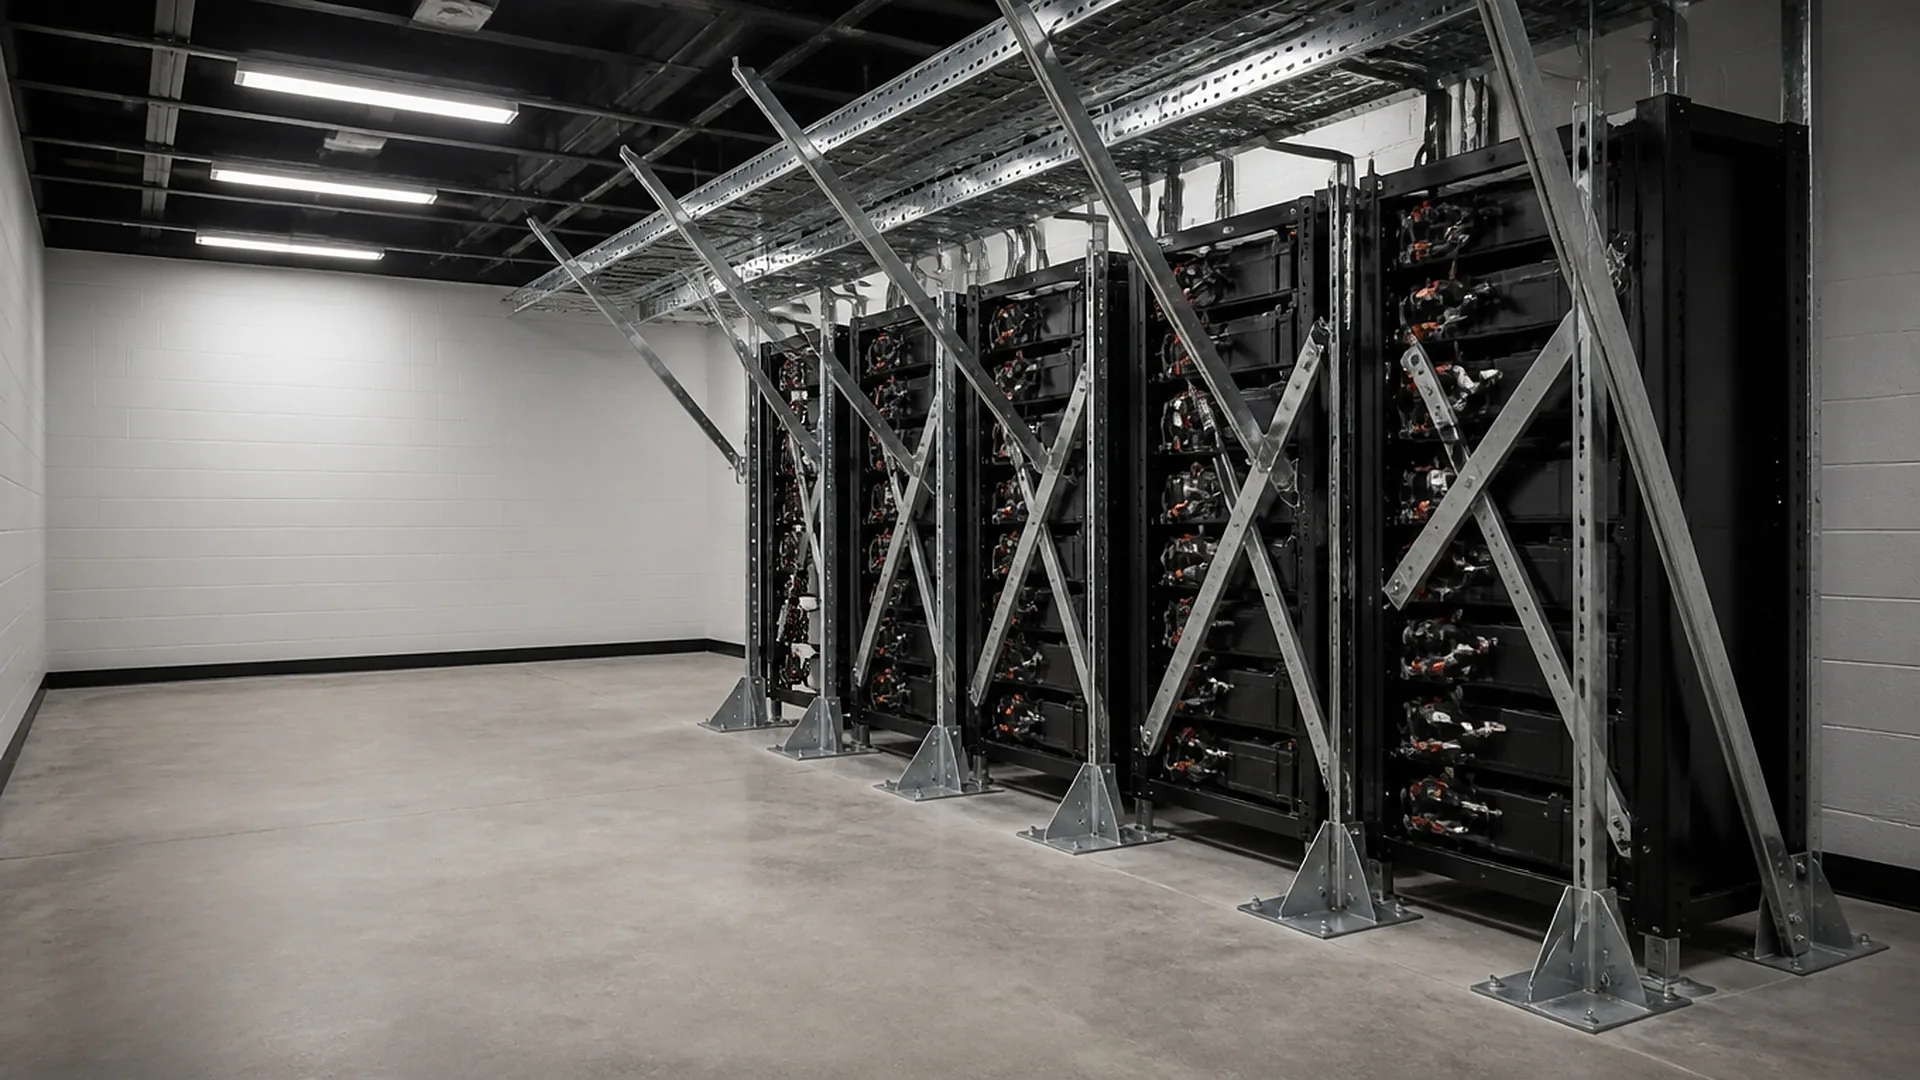
Part 13 of 17. How data center buyers package seismic restraint frames, anchorage bases and brace assemblies from stamped details, what the special inspector will ask for, and who to qualify.
Read post →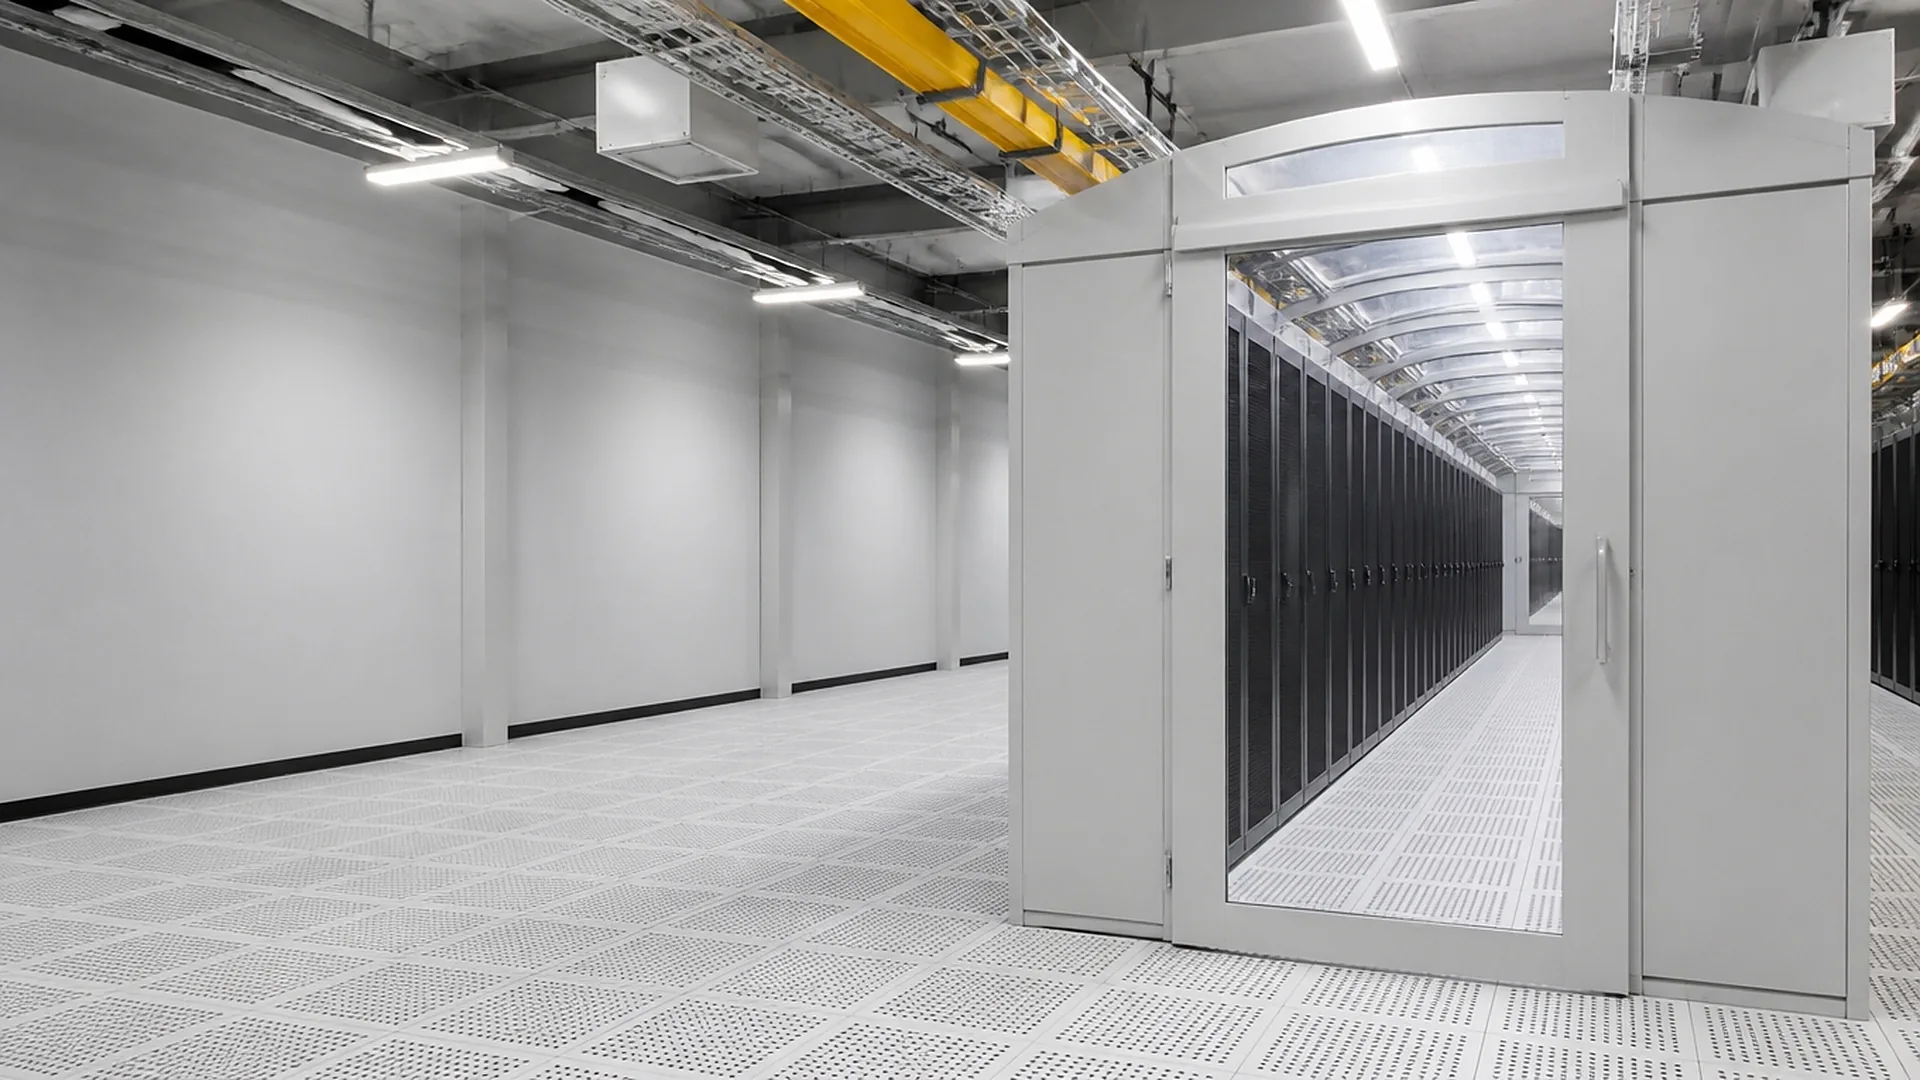
Part 12 of 17. How data center buyers specify containment frames, end-of-row doors, roof frames and chimney structures, when to use a vendor system and when to fabricate, and how to kit by row.
Read post →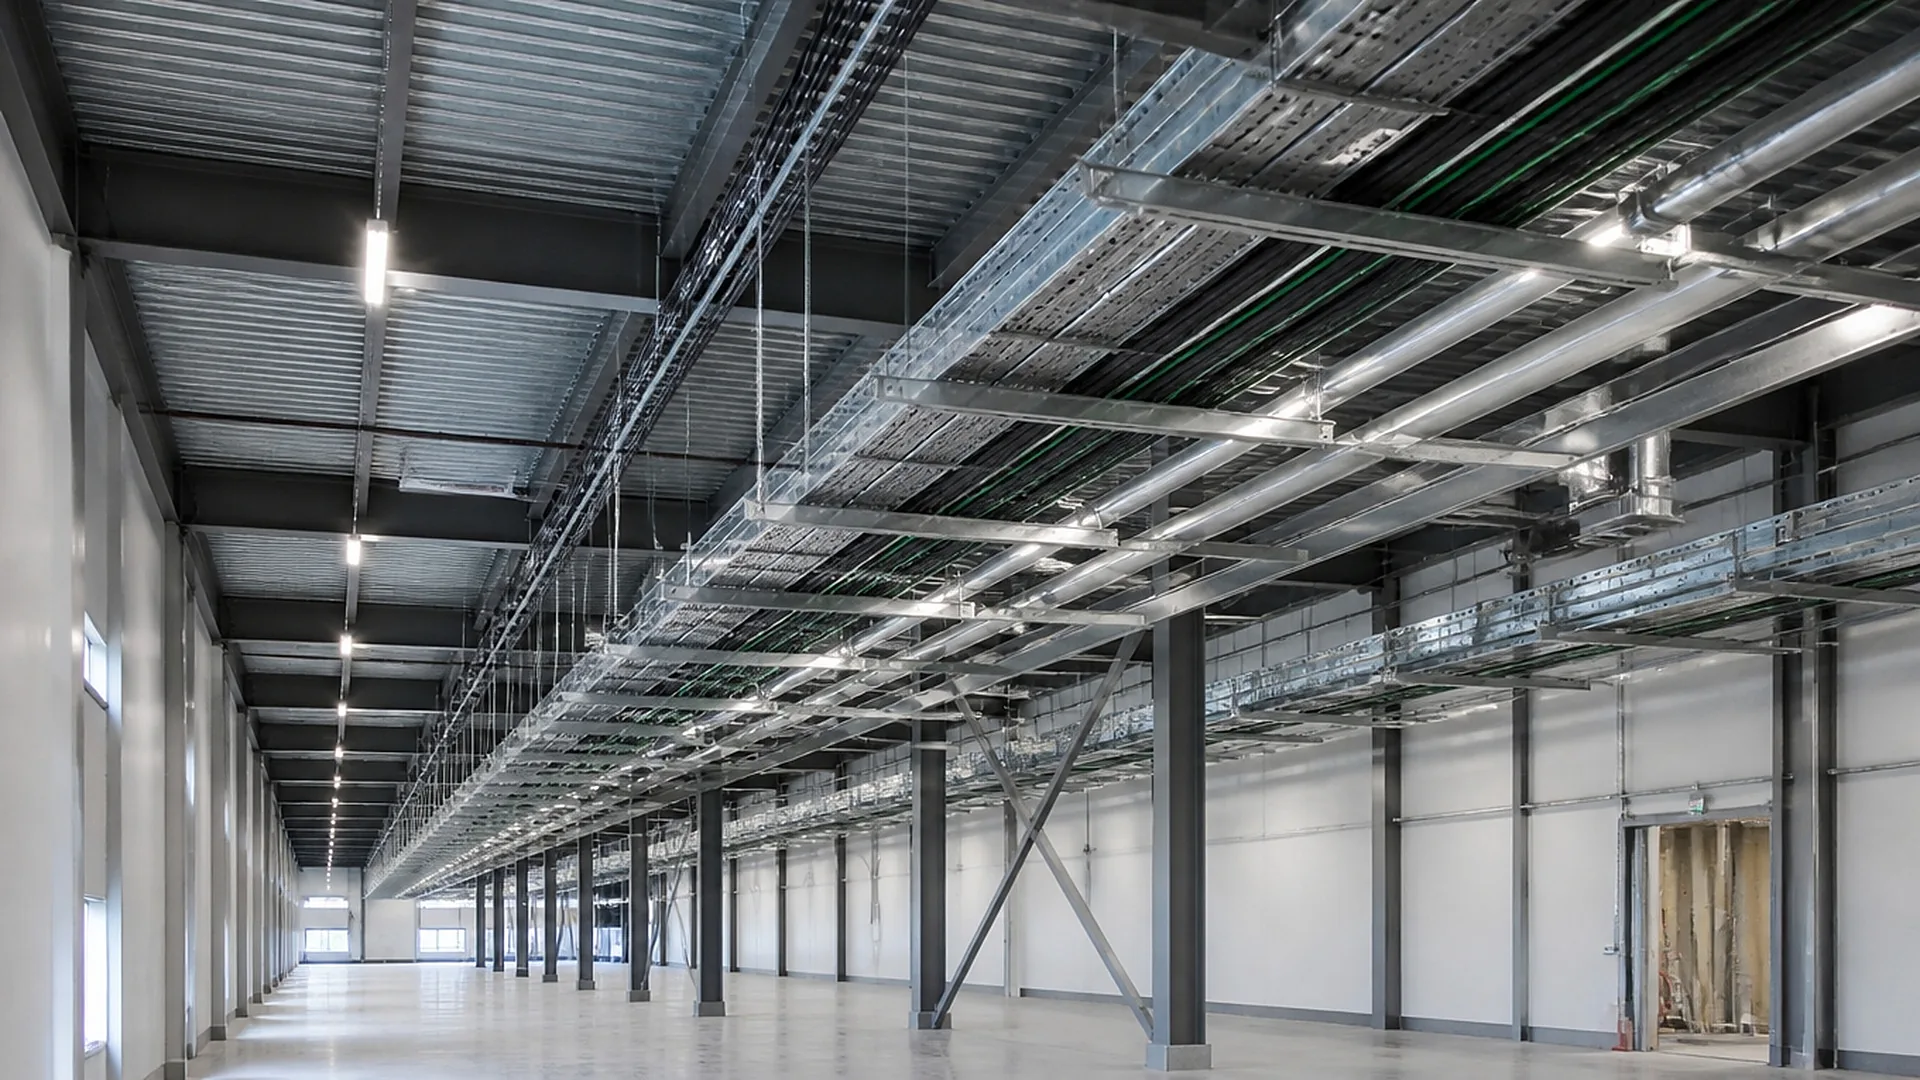
Part 11 of 17. For data center GCs and buyers: how to package the unified ceiling grid and prefabricated multi-trade racks that carry busway, tray, pipe and lighting, and what the fabricator needs.
Read post →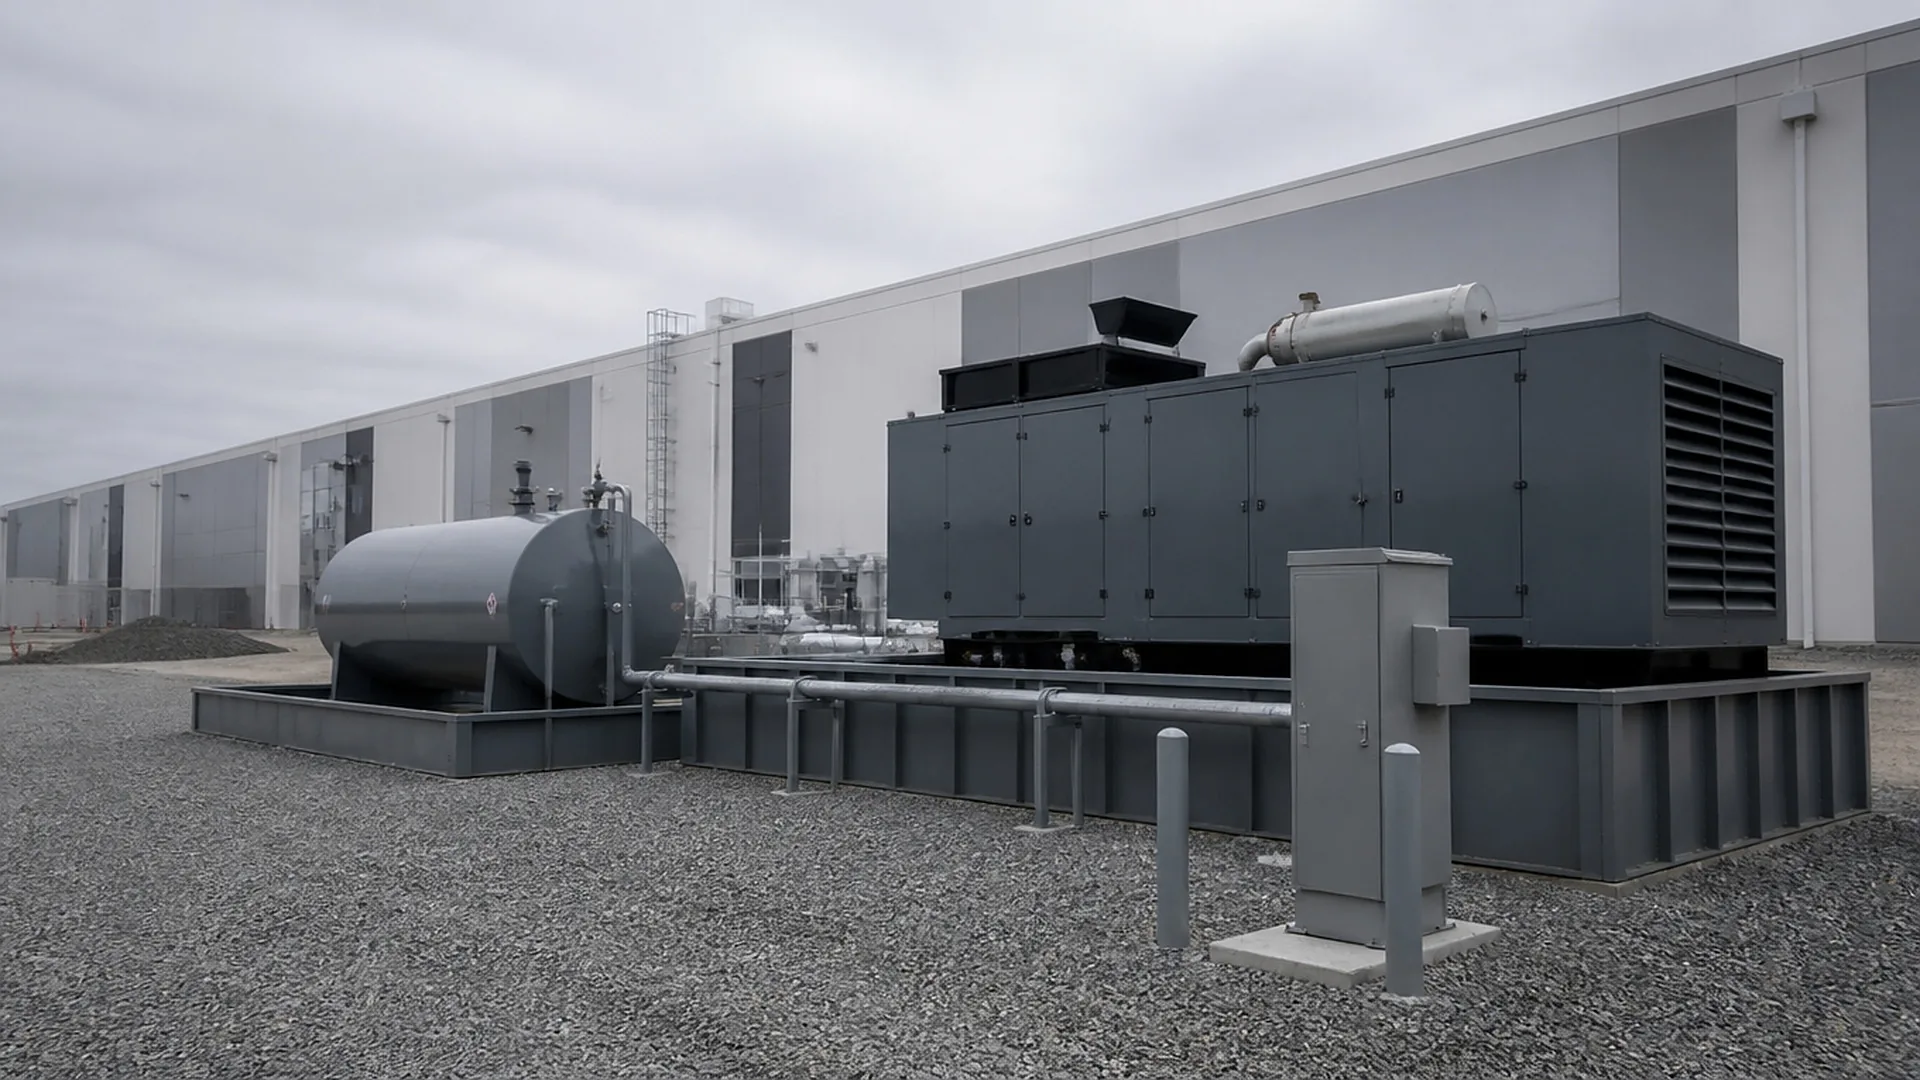
Part 10 of 17. How to specify day-tank skids, containment, tank saddles, fill stations and welded fuel piping for data center generator yards, and what to require on testing.
Read post →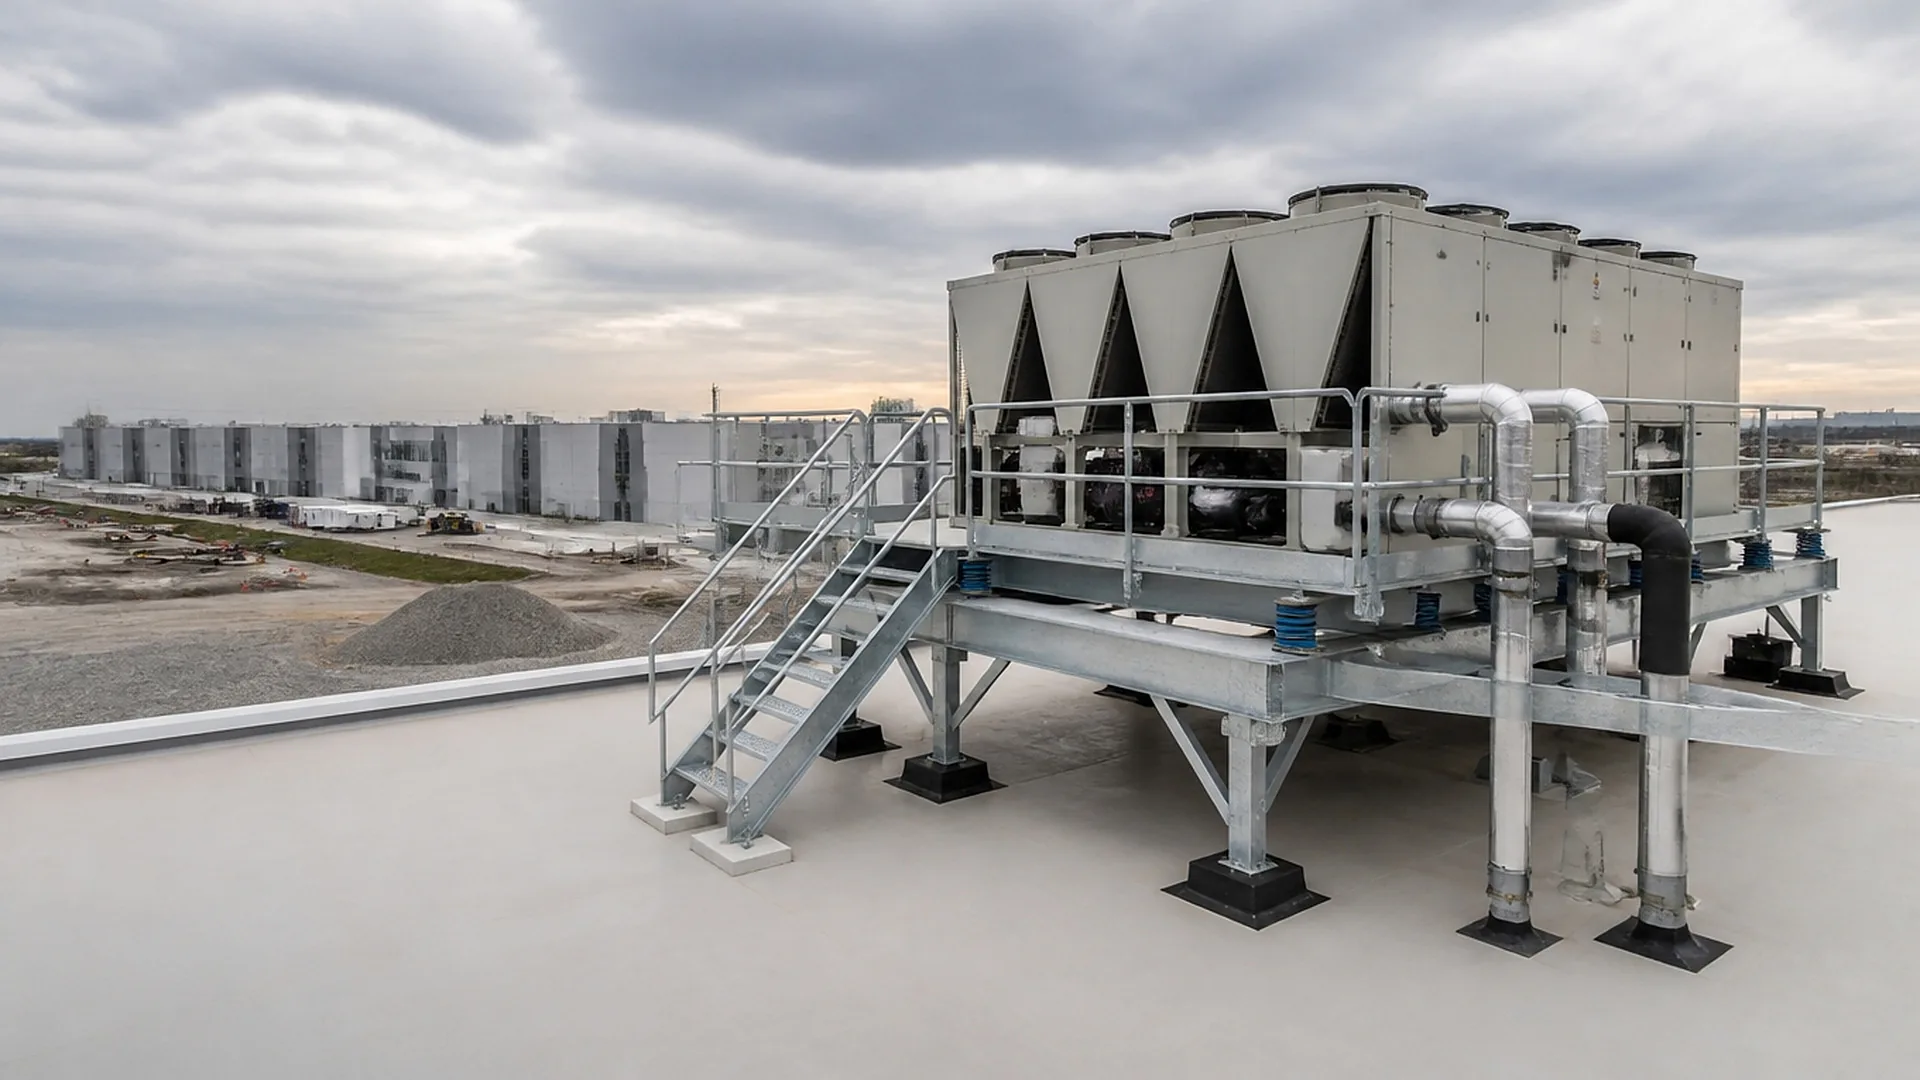
Part 9 of 17. A sourcing guide to rooftop dunnage, equipment platforms, chiller and cooling tower support frames and isolation bases: what to specify, who to qualify and when to release.
Read post →
Part 8 of 17. For data center mechanical buyers: when heavy duct, plenums and fan-wall frames belong with a metal fabricator rather than a sheet-metal shop, and how to write the RFQ.
Read post →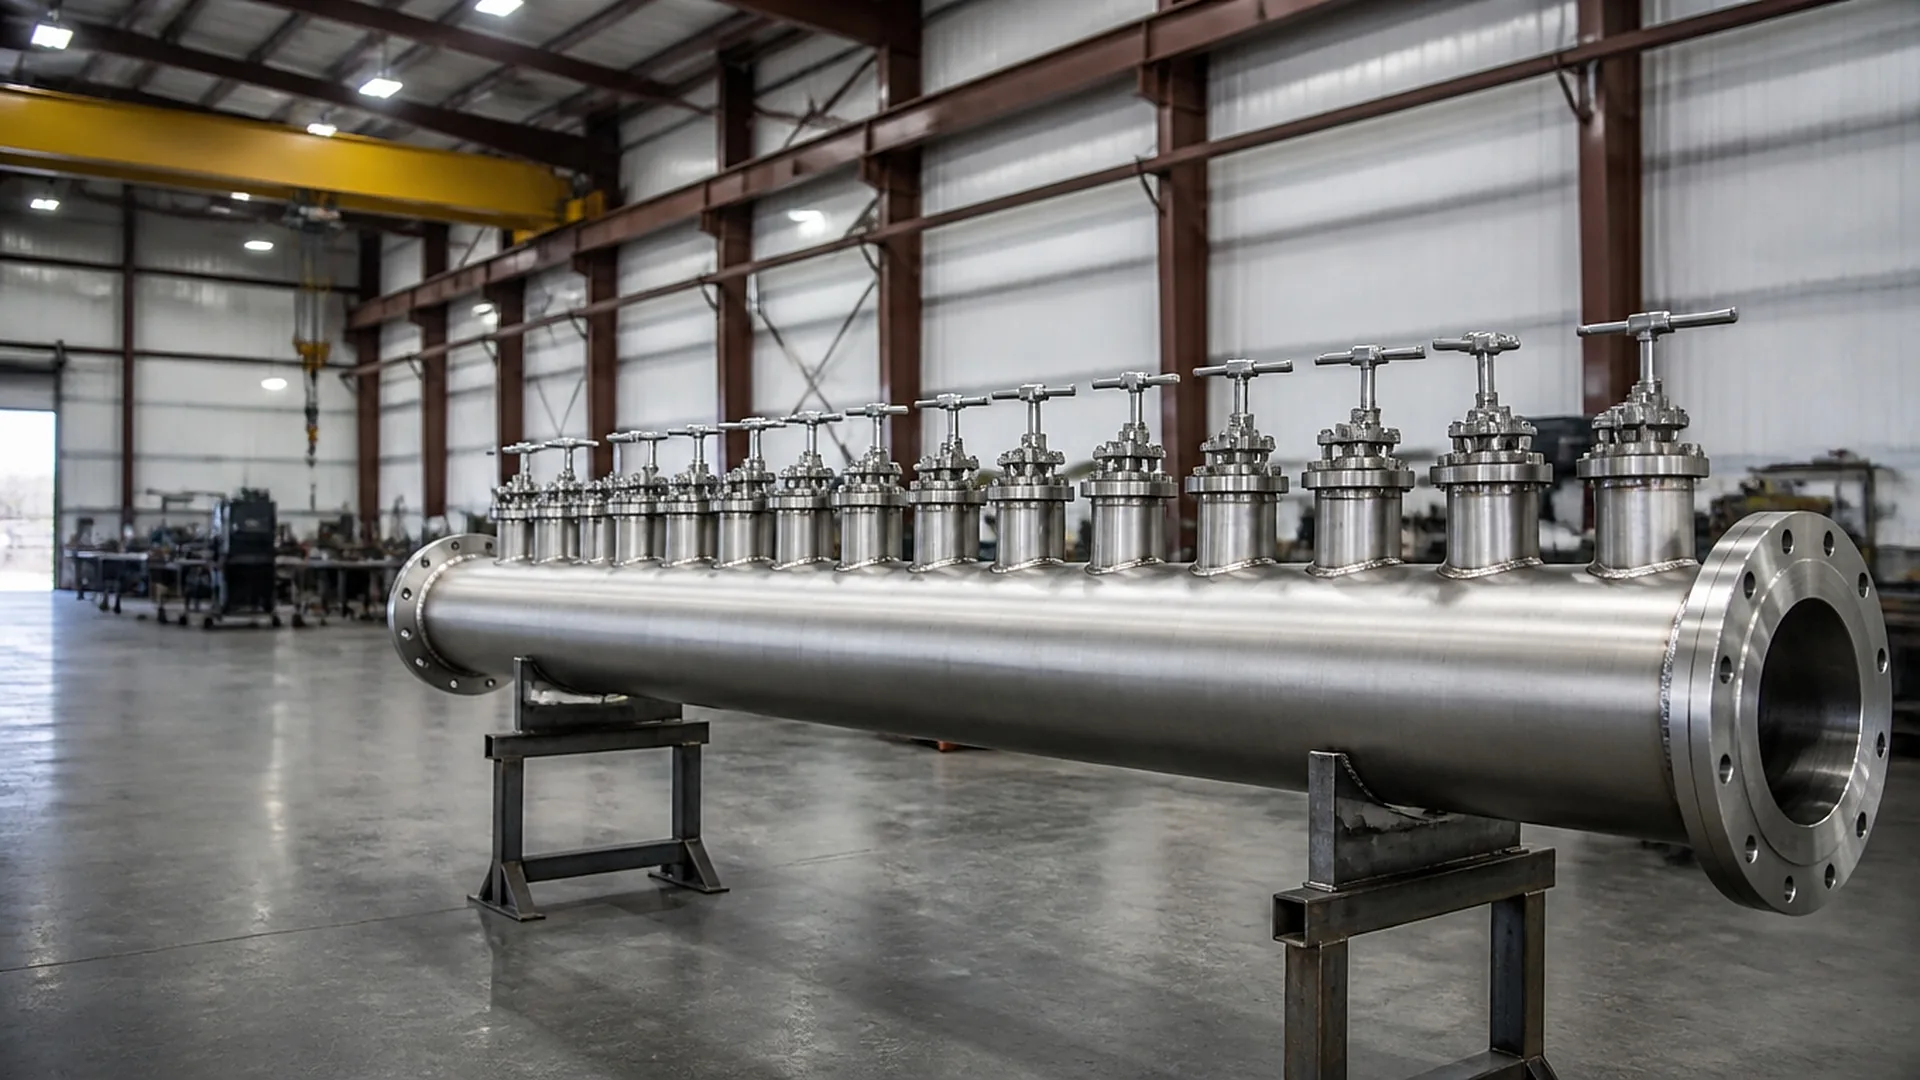
Part 7 of 17. How data center buyers specify distribution manifolds, plant headers and CDU connection headers for liquid cooling, what the fabricator needs, and what to require on test and tagging.
Read post →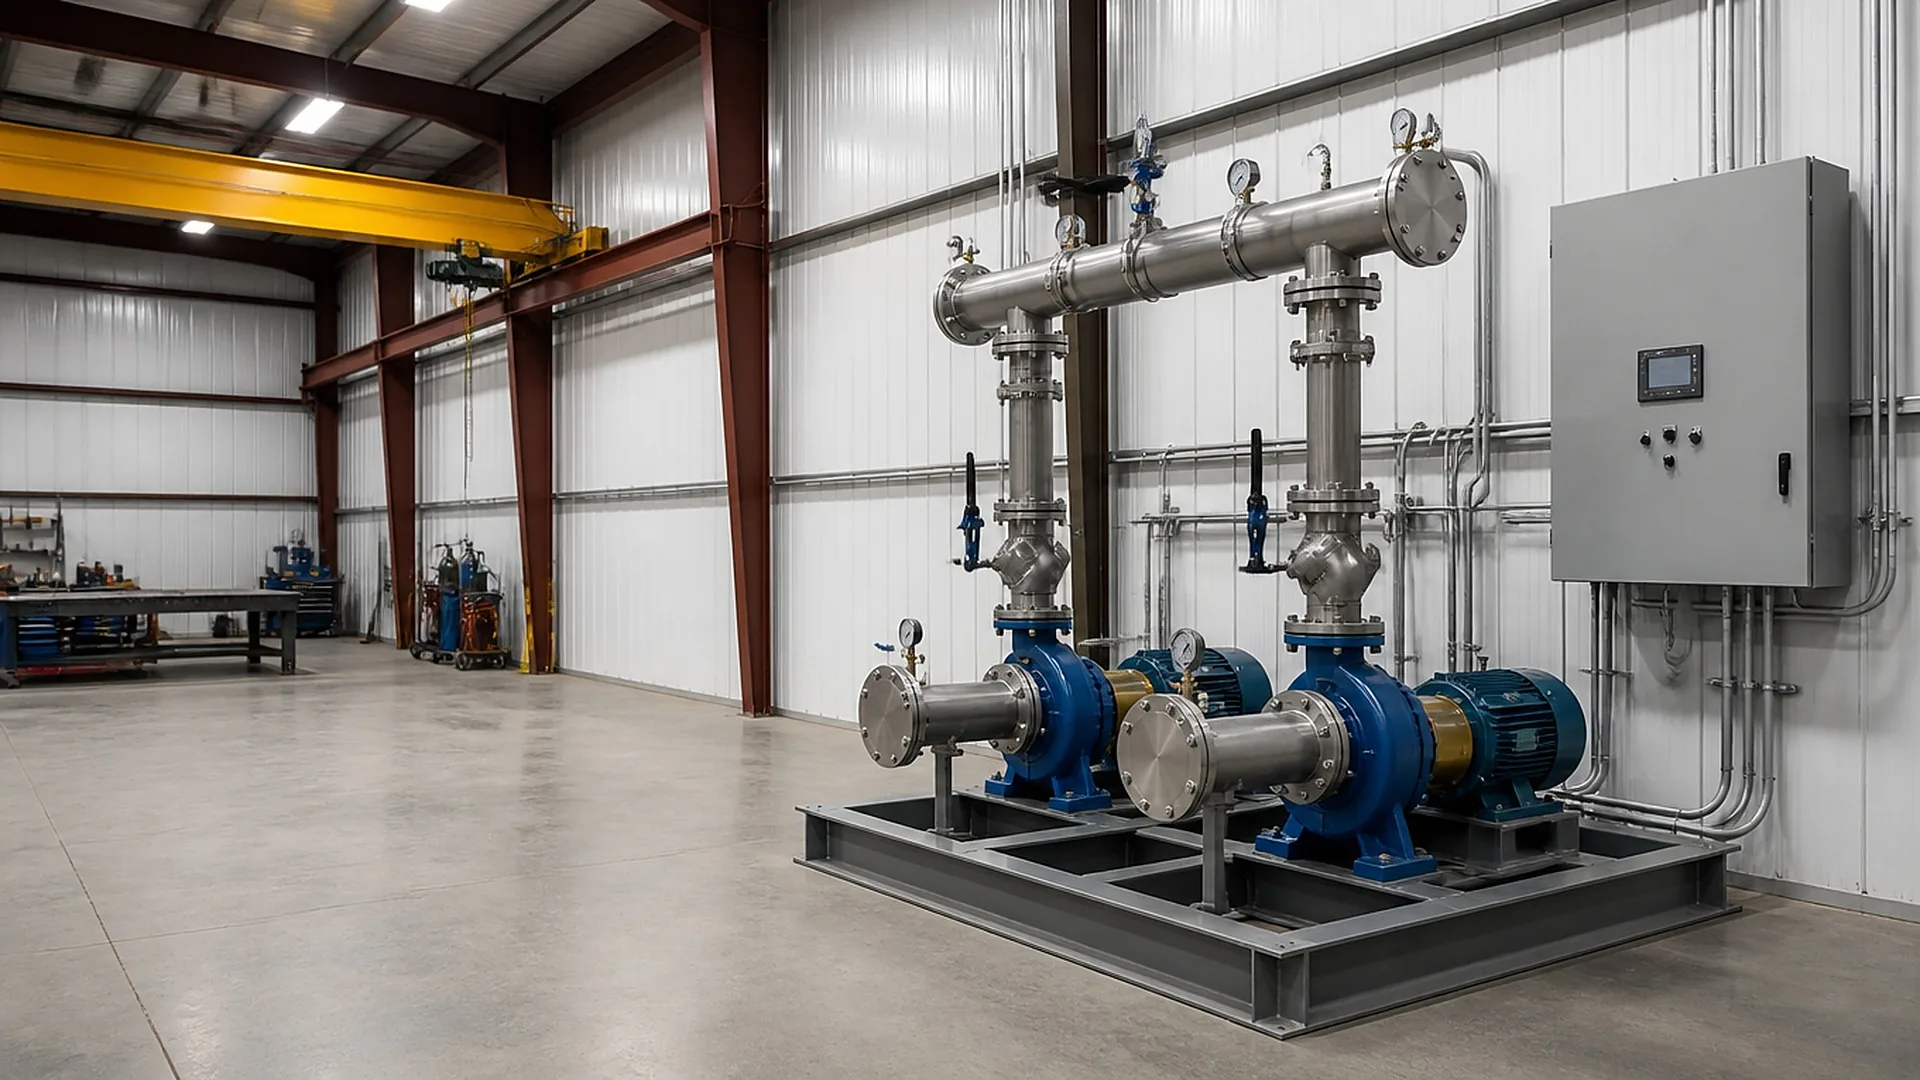
Part 6 of 17. A procurement guide to pre-piped skid packages for liquid cooling: how to split equipment from fabrication, what the P&ID package must include, and how to compare skid bids.
Read post →
Part 5 of 17. How data center buyers package pipe racks, trapezes, stanchions, anchors and guides into a fabrication RFQ, what to require, and how to avoid the supports arriving after the pipe.
Read post →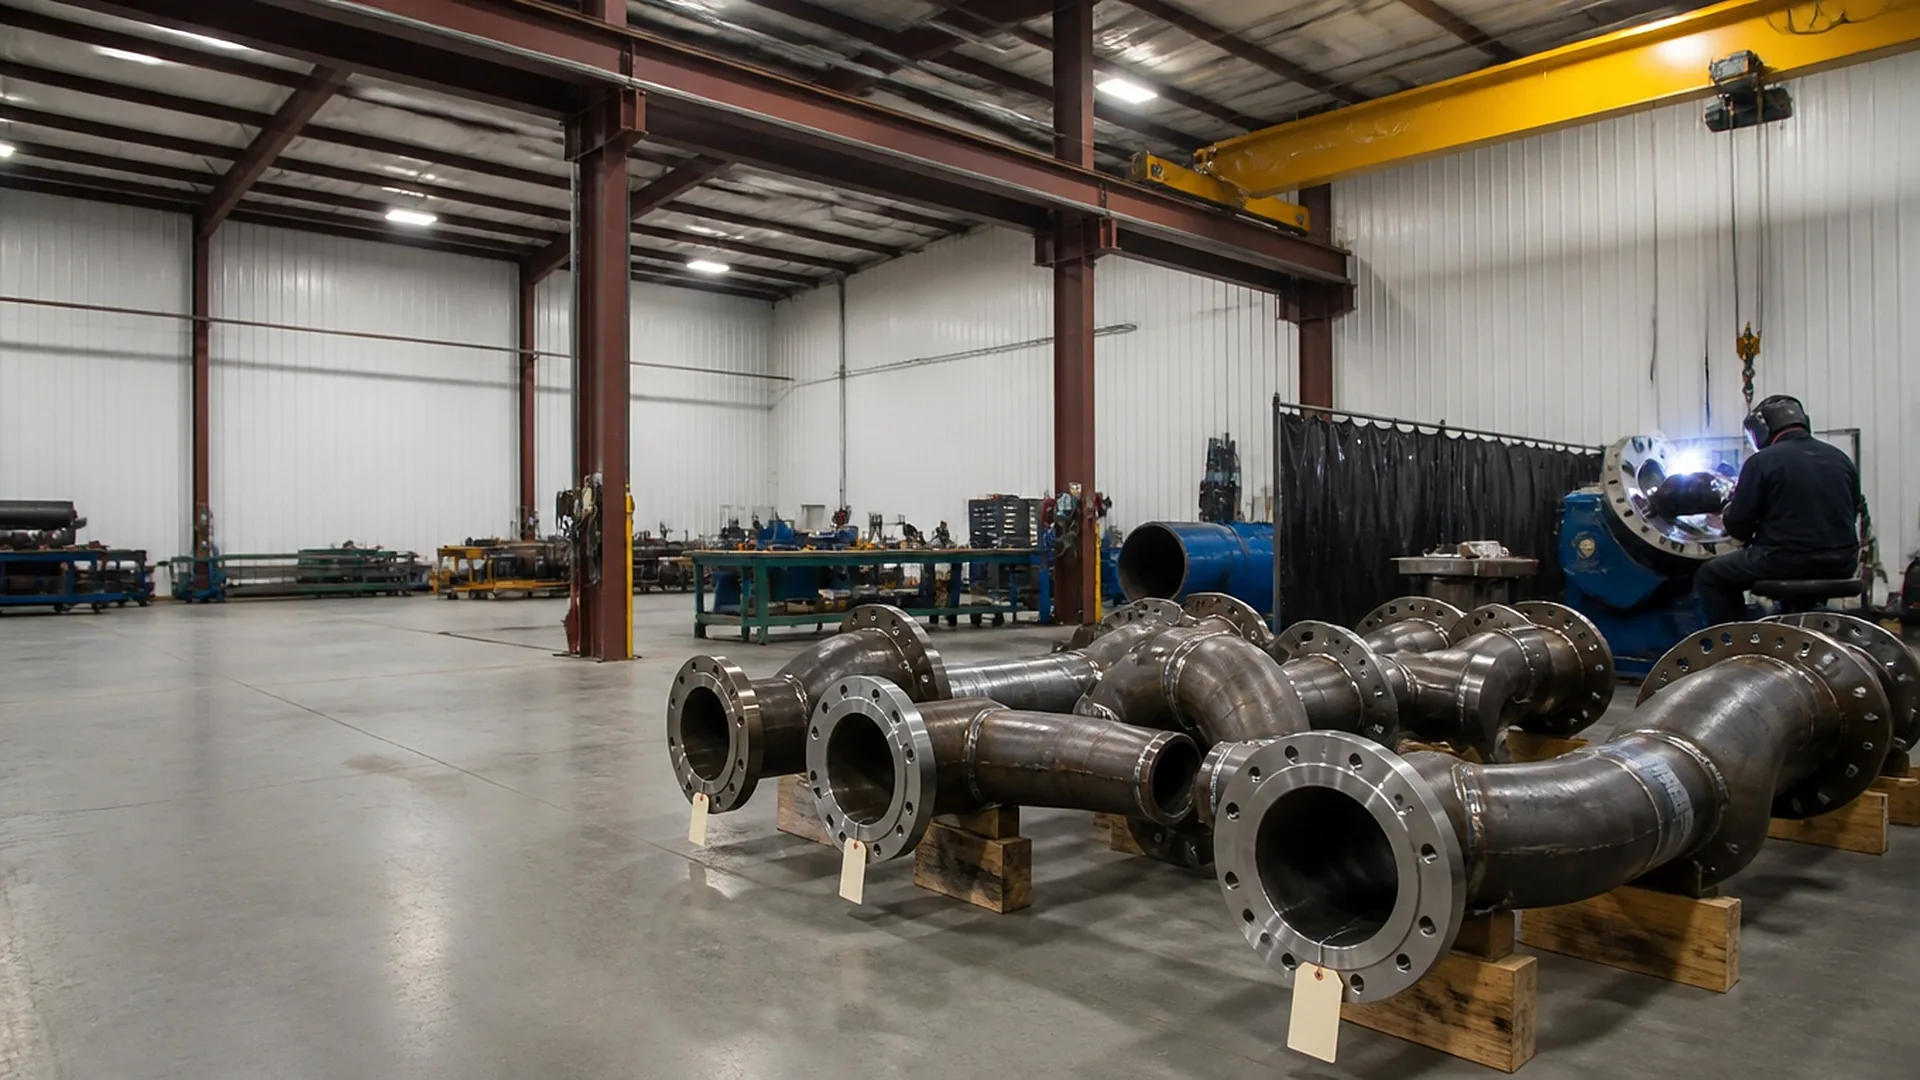
Part 4 of 17. For data center procurement and mechanical buyers: how to package a pipe spool RFQ, split shop from field work, compare fabricators and require the right test records.
Read post →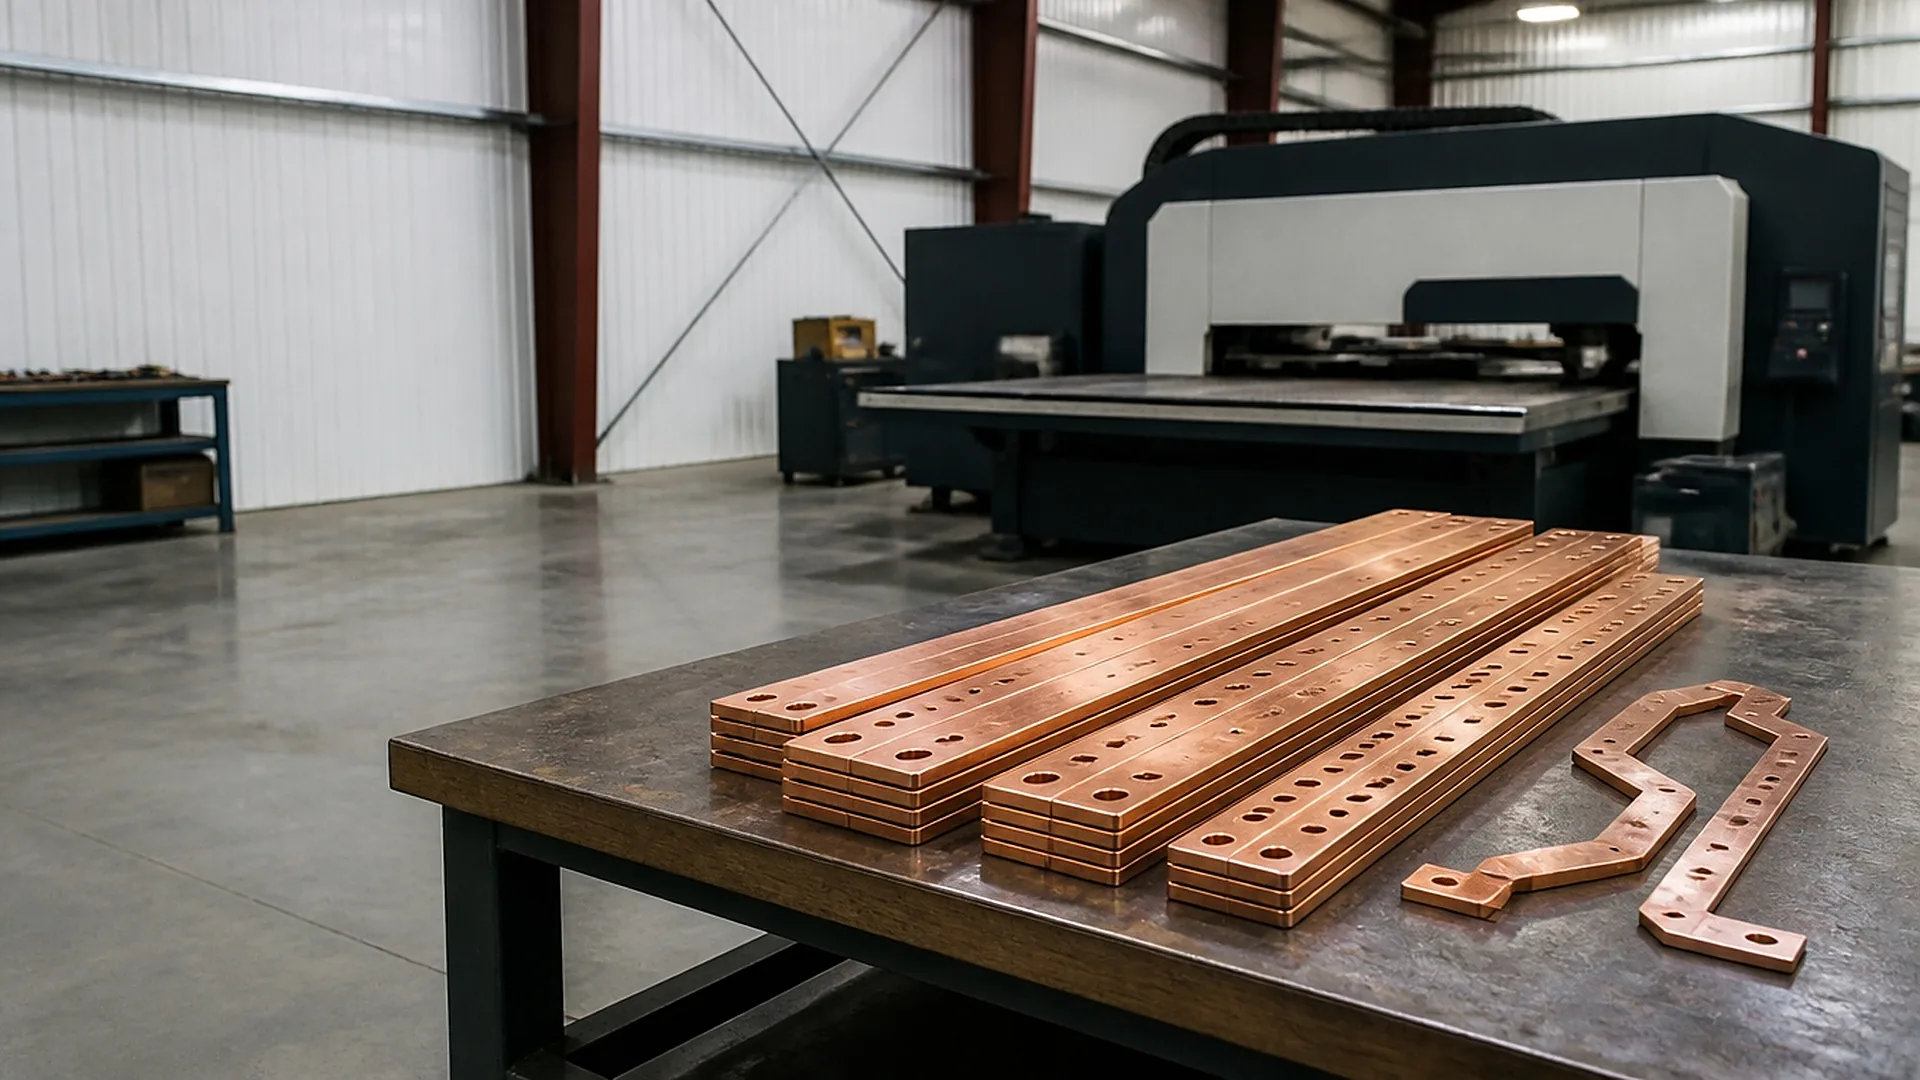
Part 3 of 17. How to specify and source fabricated bus bar, ground bars and bonding bars for data center switchgear, busway and grounding systems, and how to manage copper price risk.
Read post →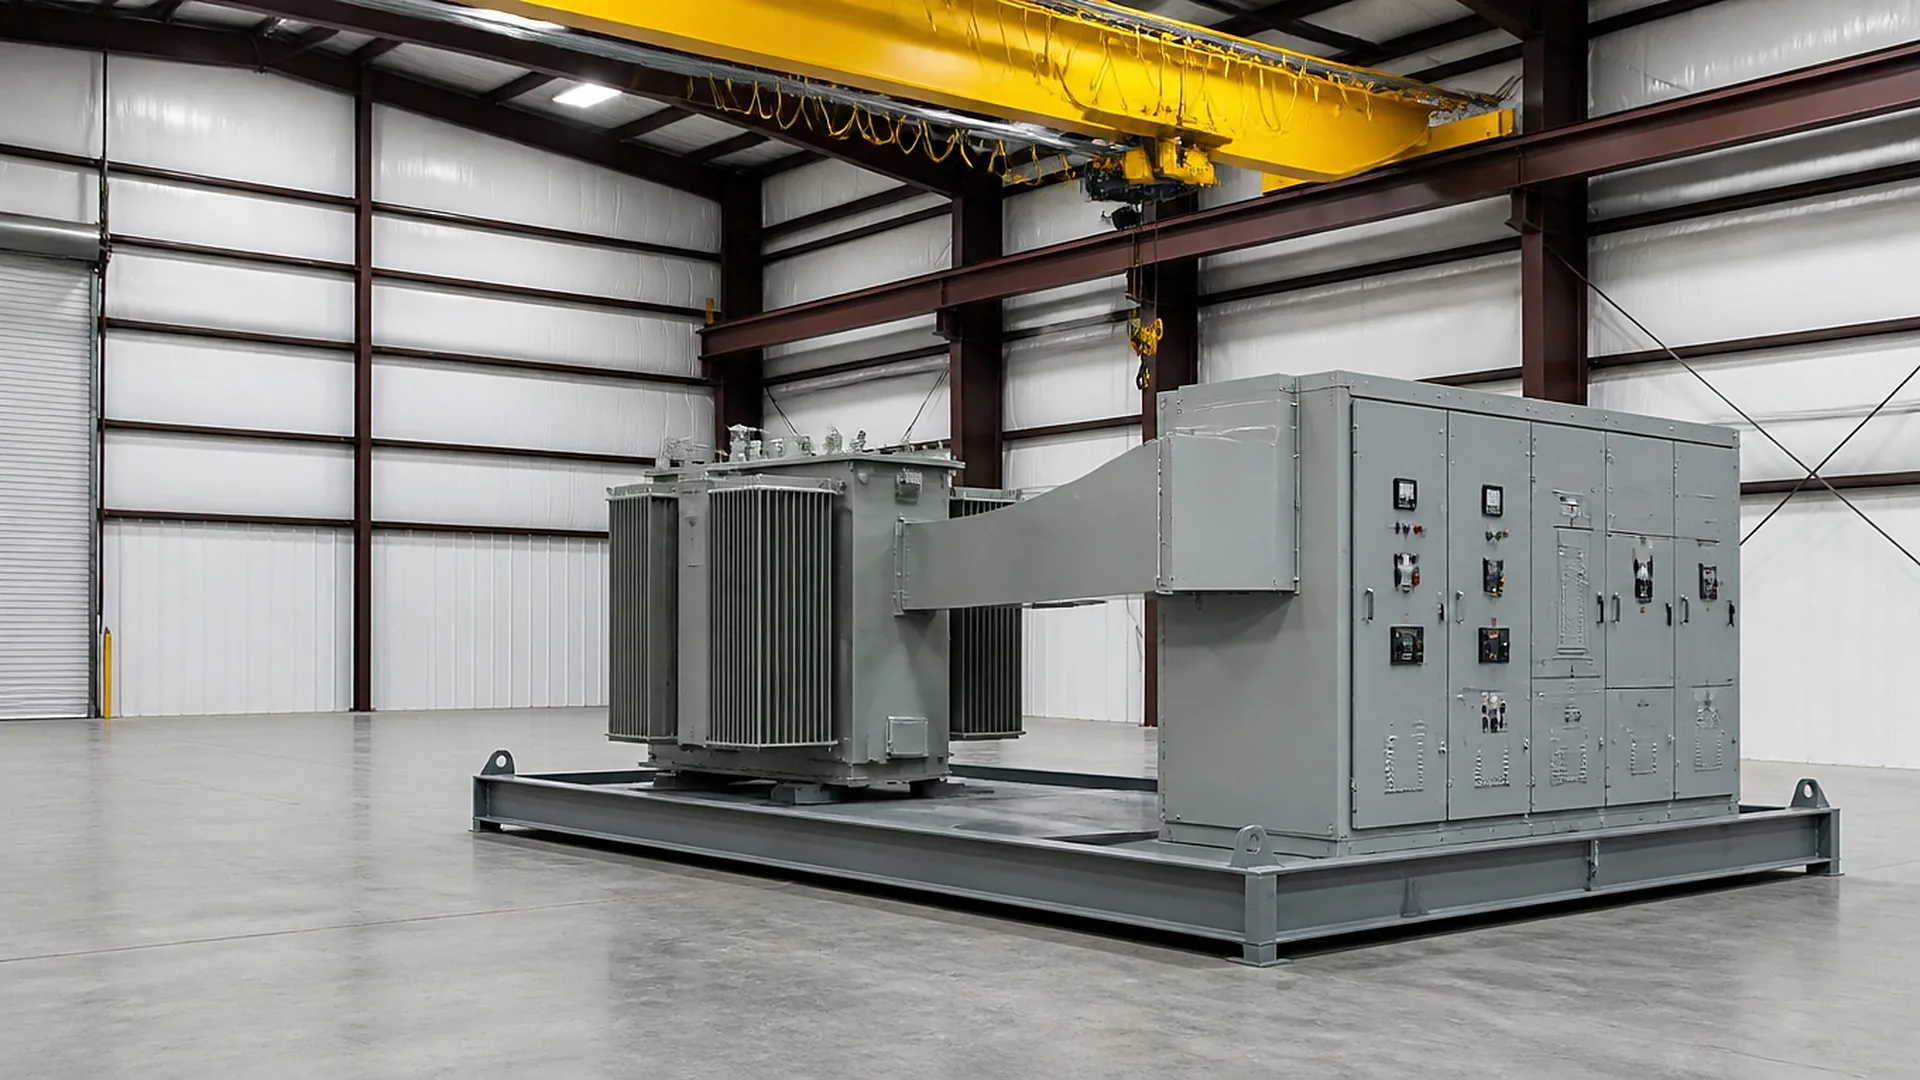
Part 2 of 17. How data center procurement teams specify skid-mounted transformer and switchgear assemblies, what the fabricator needs, and how to compare bids on scope, not just price.
Read post →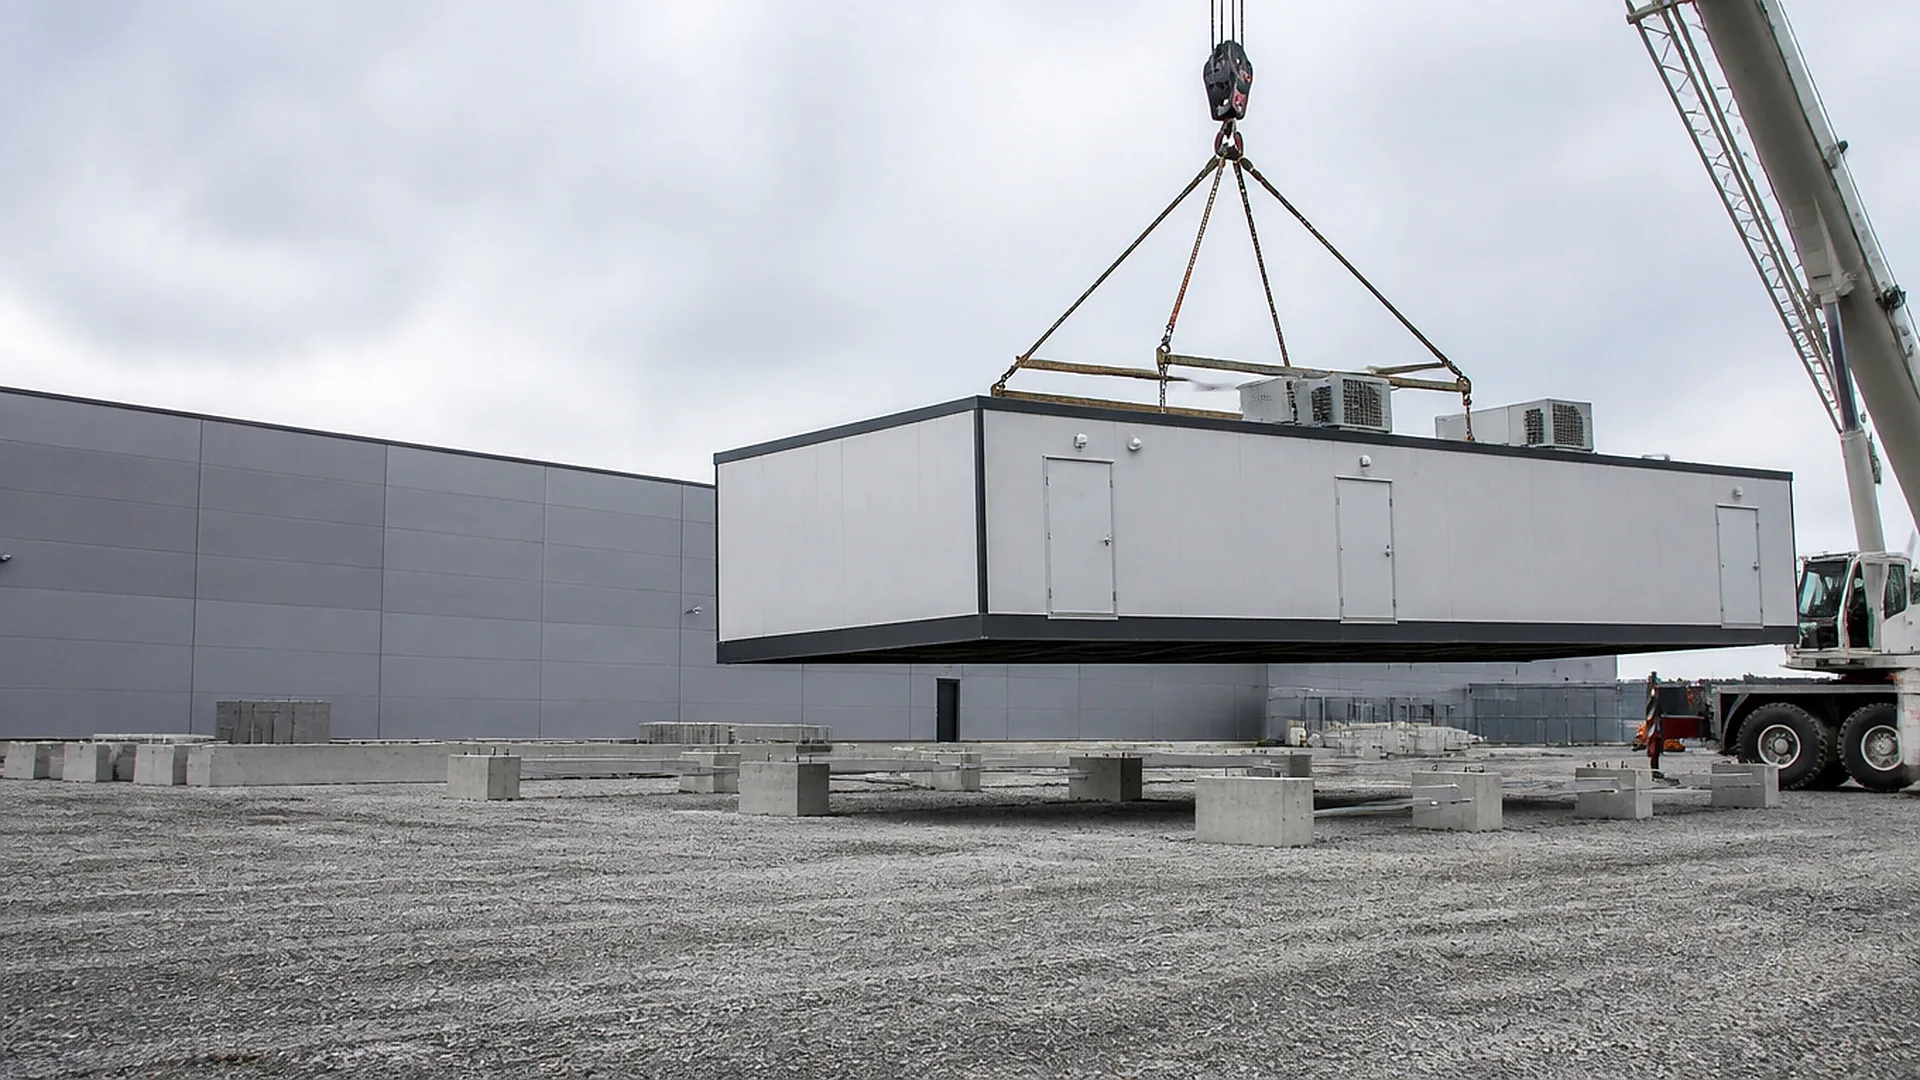
Part 1 of 17. A sourcing guide for data center buyers: how to scope, specify and qualify a fabricator for prefabricated E-Rooms and E-Houses, and what to require back.
Read post →
Part 3 of 3. The complete fabricated-metal scope on a hyperscale campus — electrical, mechanical, structural and modular — and how general contractors package it.
Read post →Part 2 of 3. When a prefabricated E-Room beats a site-built electrical room on schedule, risk and cost — and what to send a fabricator to get one quoted.
Read post →Part 1 of 3. What to send a pipe fabricator, how to split the spool scope from field work, and what documentation to require for data center cooling piping.
Read post →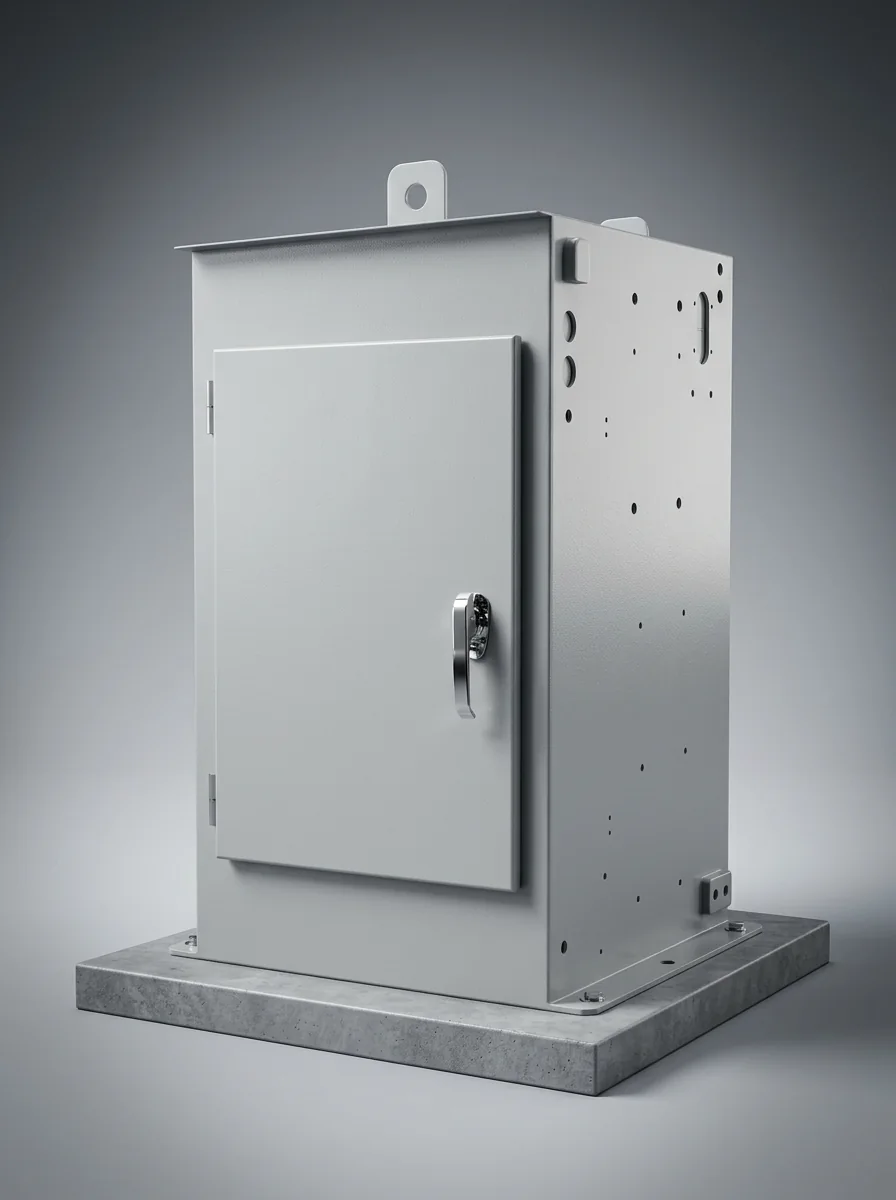
Spec Sheet. 12- or 11-gauge for panels and doors, heavier for base and roof — the gauge table, what NEMA 3R requires, and what pushes gauge up.
Read post →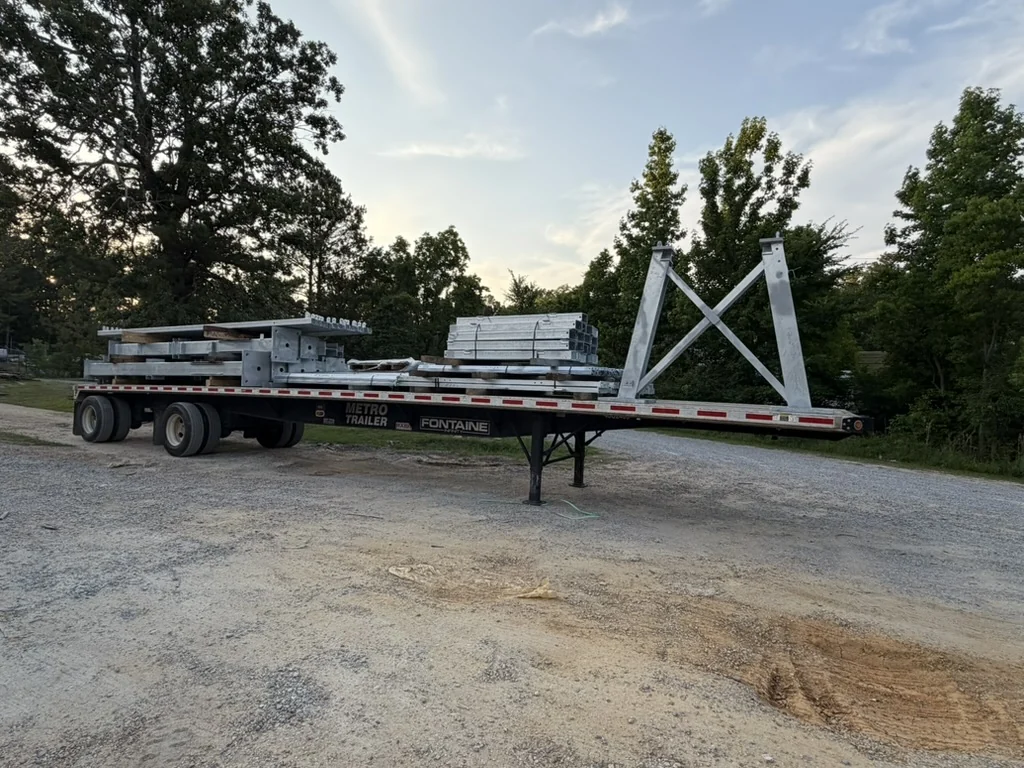
Spec Sheet. A123 for structures and fabricated steel, A153/F2329 for hardware — coating grades, thickness in mils, and the companion specs to cite.
Read post →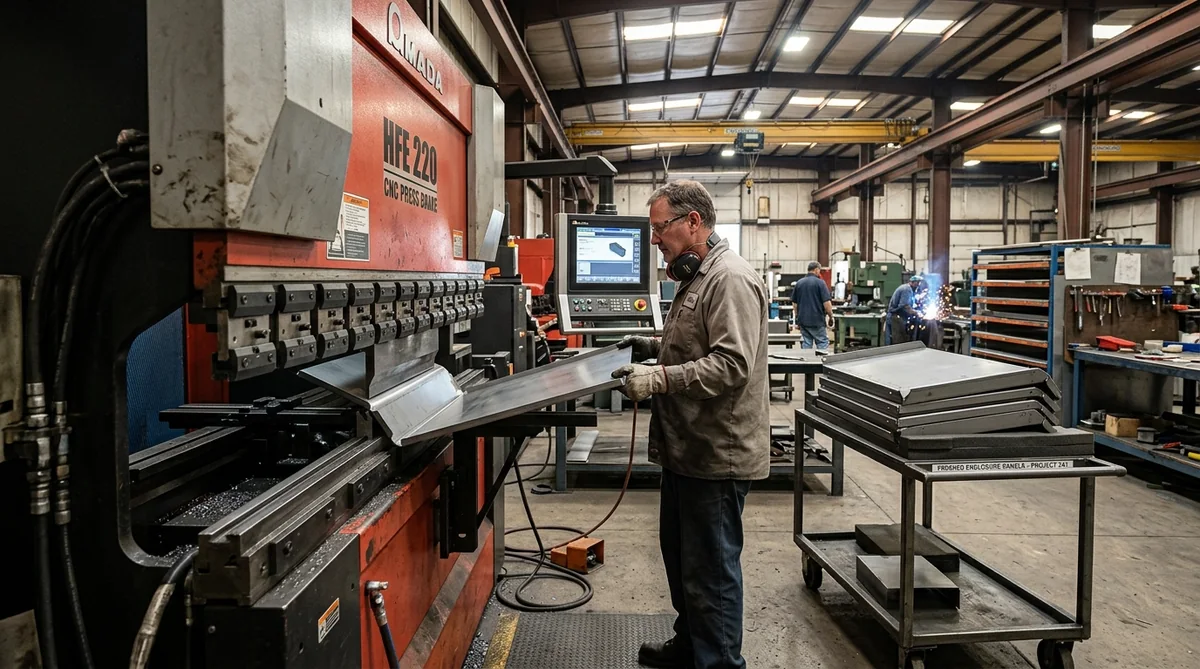
Spec Sheet. ~1t inside radius up to 1/8″ for 5052-H32, 1.5–2t on heavier gauges — the table by thickness and temper, 6061 comparison, grain and tooling notes.
Read post →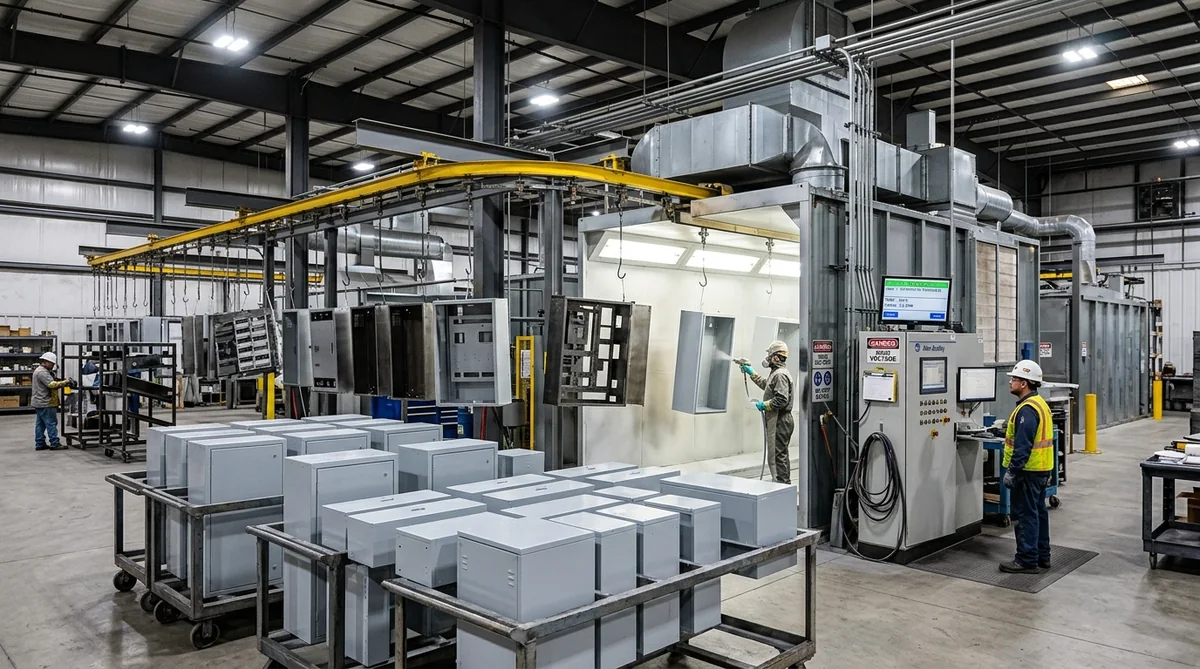
Spec Sheet. 3–5 mils polyester or super-durable powder over pretreatment outdoors, 2–3 mils indoors — chemistry by environment, duplex systems, and how to measure.
Read post →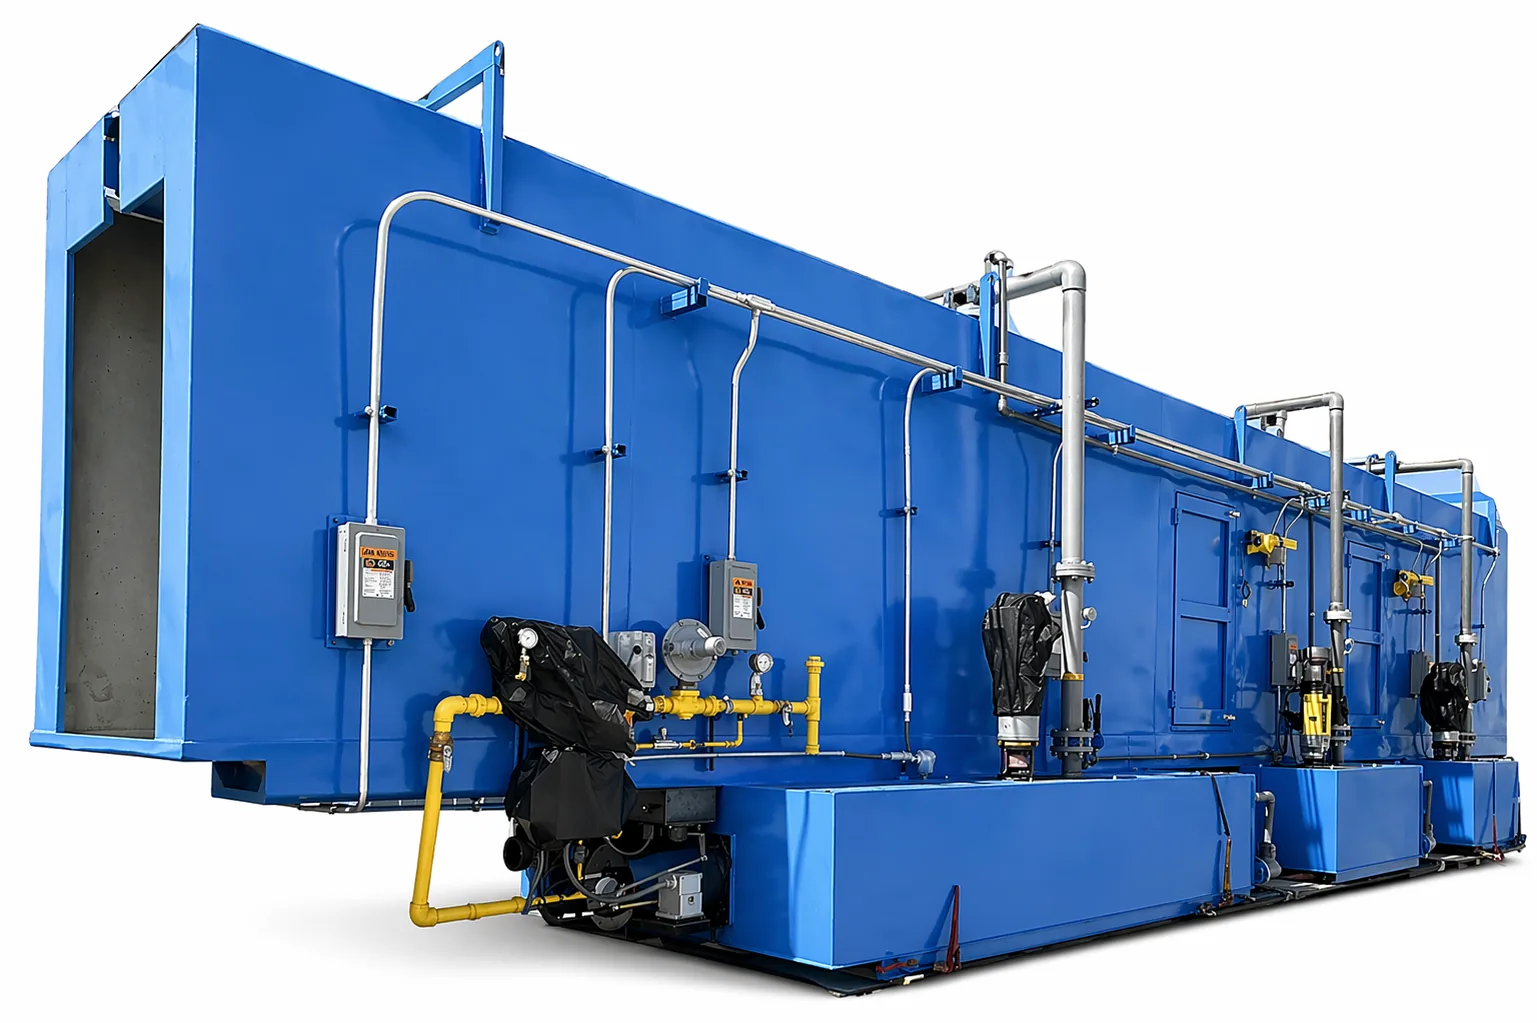
Spec Sheet. ASTM B117 salt fog, what’s measured at the scribe, what IEEE C57.12.28 requires, and how 2000 hours relates to years in the field.
Read post →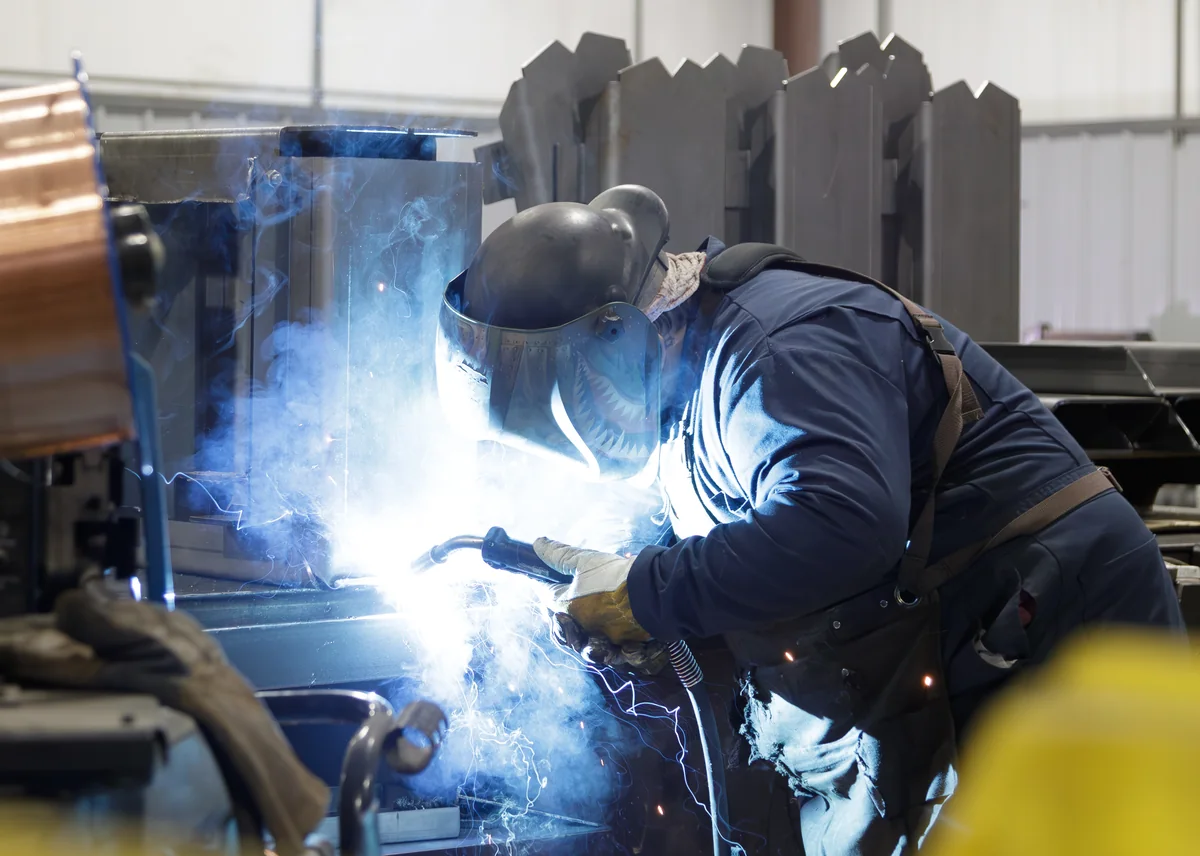
Spec Sheet. D1.1 for structural steel 1/8″ and up, D1.3 for sheet to 3/16″, D1.6 stainless, D1.2 aluminum — the overlap, WPS/PQR and welder quals, and how to specify.
Read post →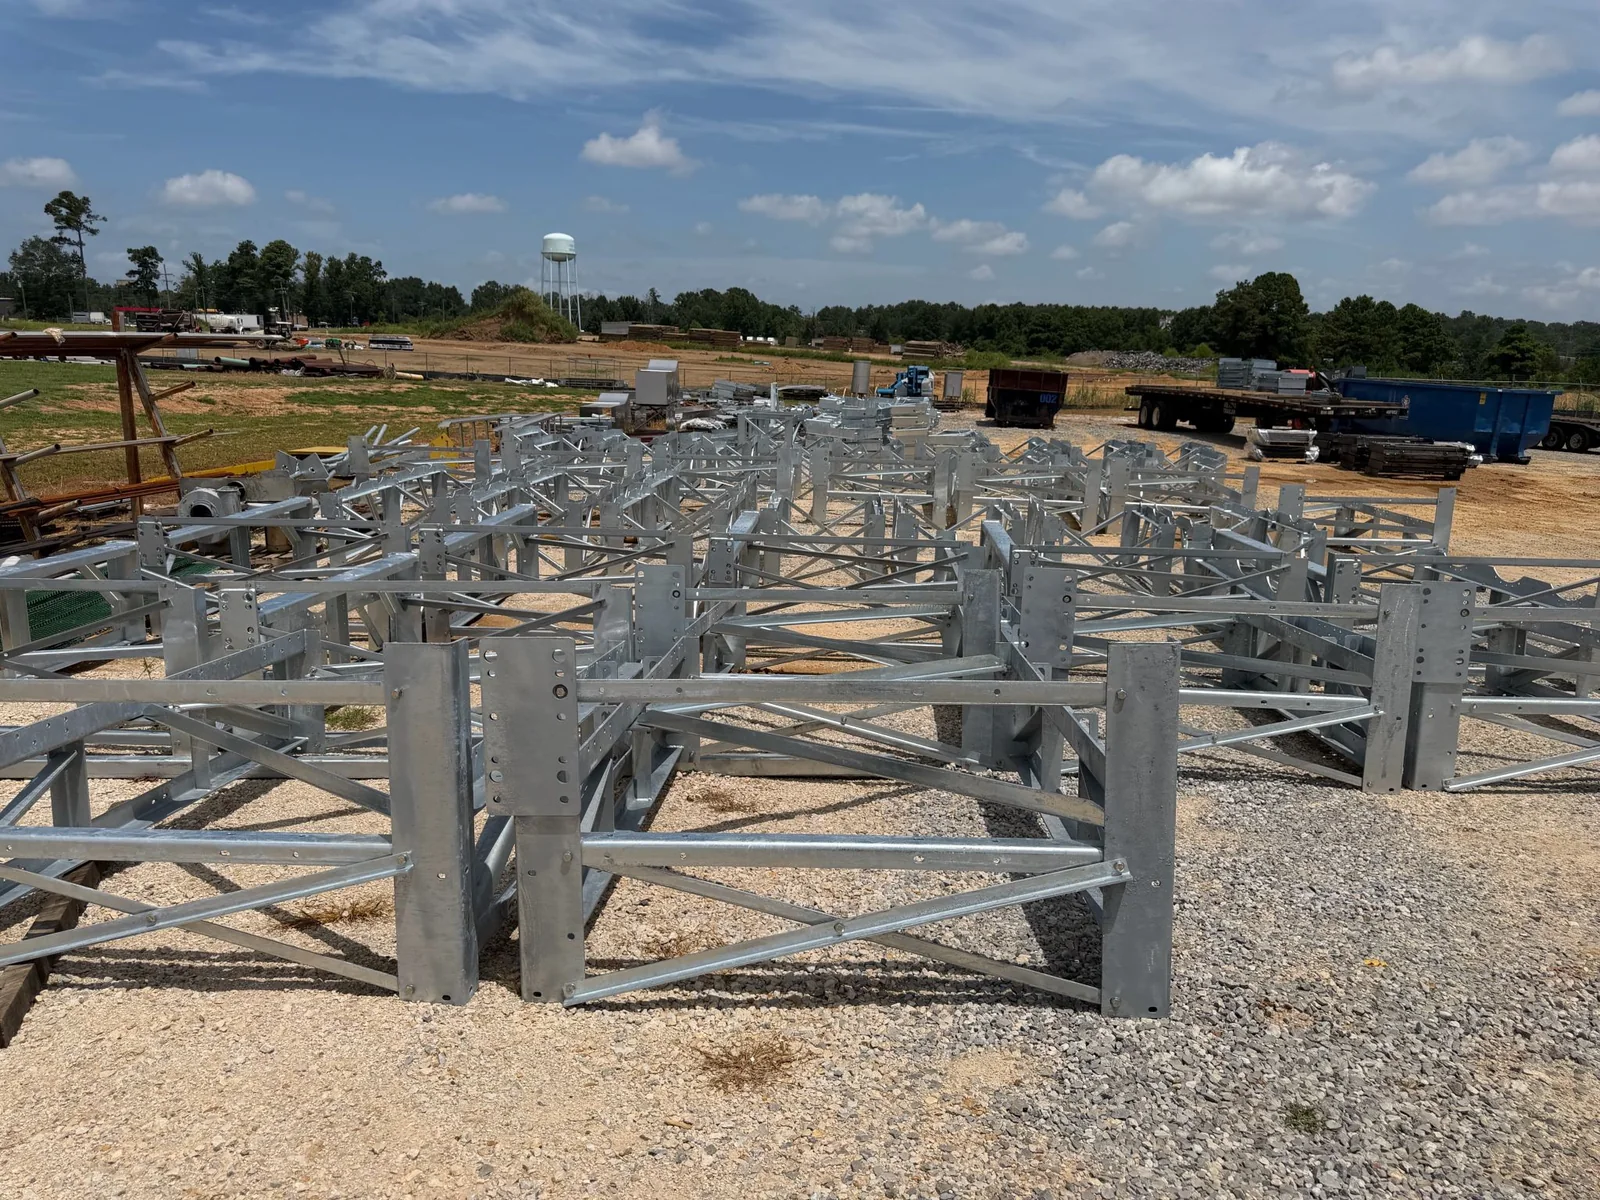
Spec Sheet. Standard hole = bolt + 1/16″ (+1/8″ at 1″ and up), oversized base-plate holes per AISC DG1, slot rules, and the location tolerances a beam line holds.
Read post →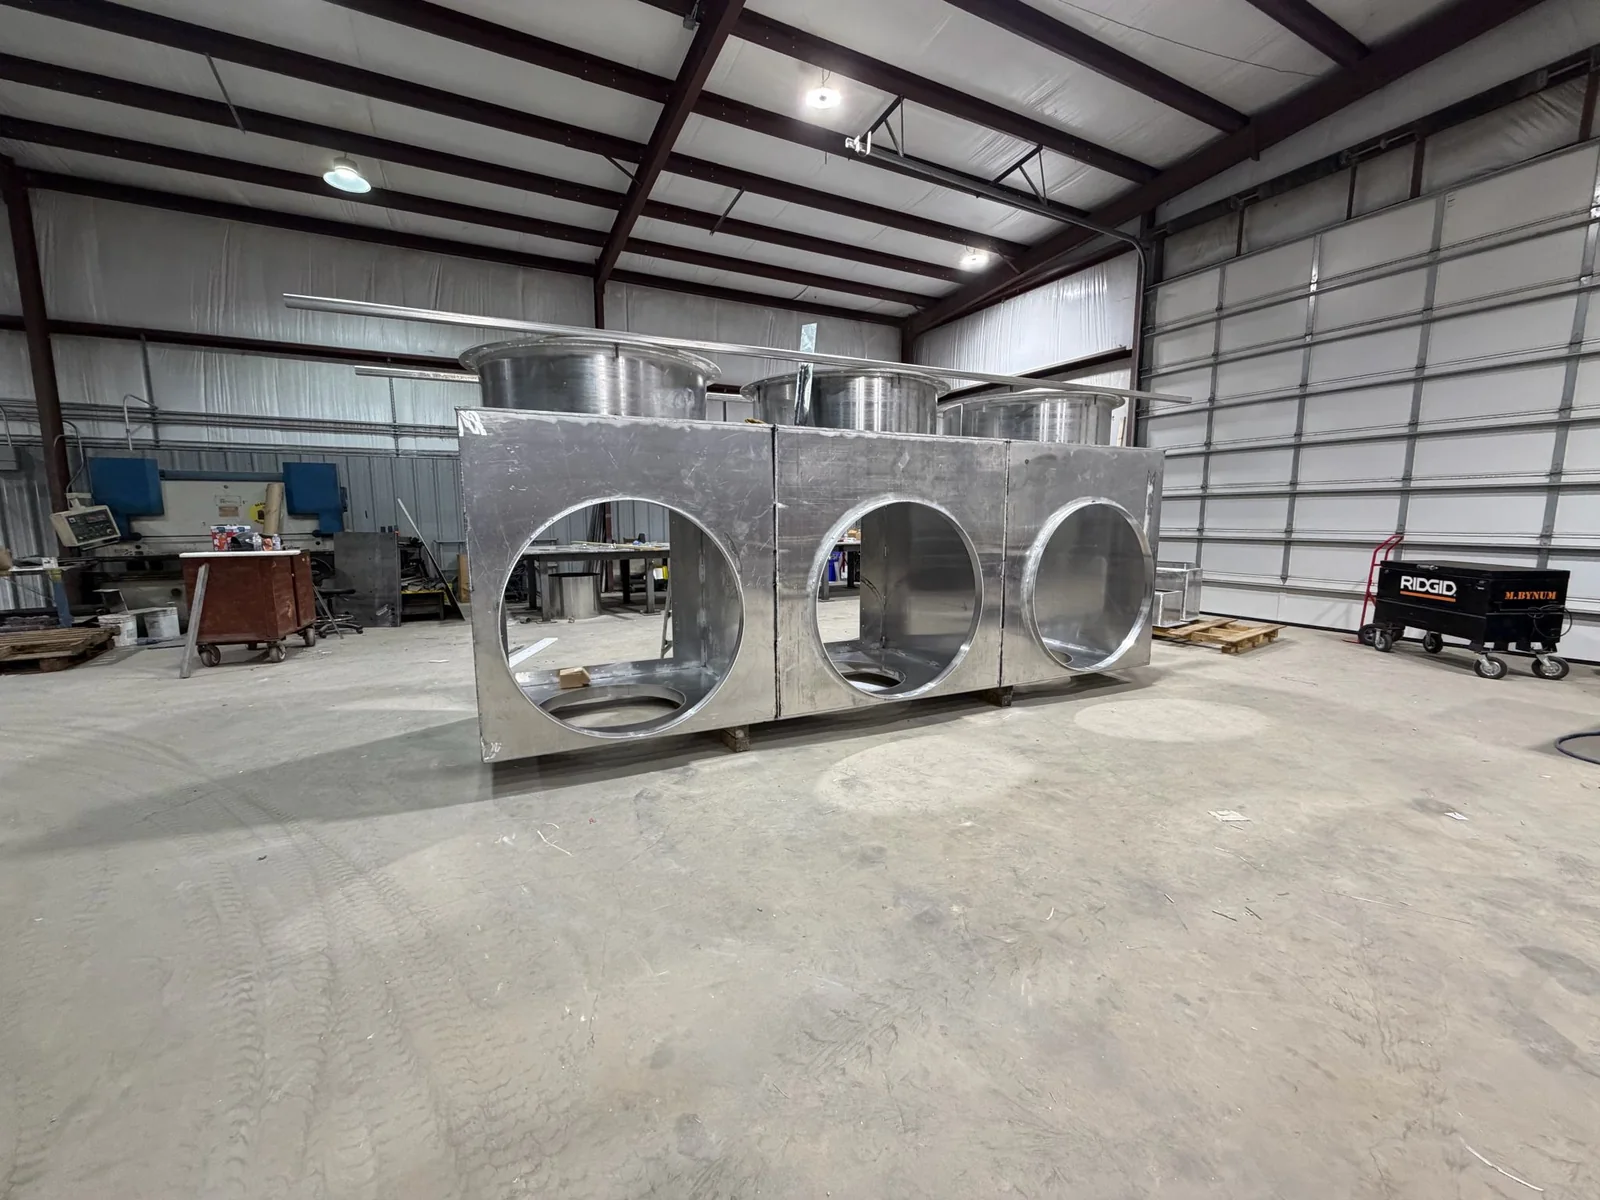
Spec Sheet. Rating is set by bar cross-section, material, temperature rise and housing ventilation; typical 1,200–6,000 A. Indicative bar ampacities, IEEE C37.23, and what the housing fabricator needs.
Read post →
Spec Sheet. What an MTR certifies, how a heat number follows steel from mill to piece mark, why it matters for Buy America and audits, and how to specify it.
Read post →
Spec Sheet. F1554 grade, diameter and pattern, projection and embedment, ACI 117 tolerances, the fabricator’s template, oversized base-plate holes, leveling nuts vs. grout — and the survey.
Read post →
Part 1 of 8. A large load, a reliability need, a new line: how a substation project begins, who’s involved, and the point where the steel package should enter.
Read post →
Part 2 of 8. Transformers at 2–4 years, breakers and switchgear at a year-plus: how the equipment order sets the schedule, and what to build while you wait.
Read post →
Part 3 of 8. ASCE 113 loads, structure types, connections, bolt patterns from OEM drawings, detailing for the galvanizing kettle, and the shop-drawing cycle.
Read post →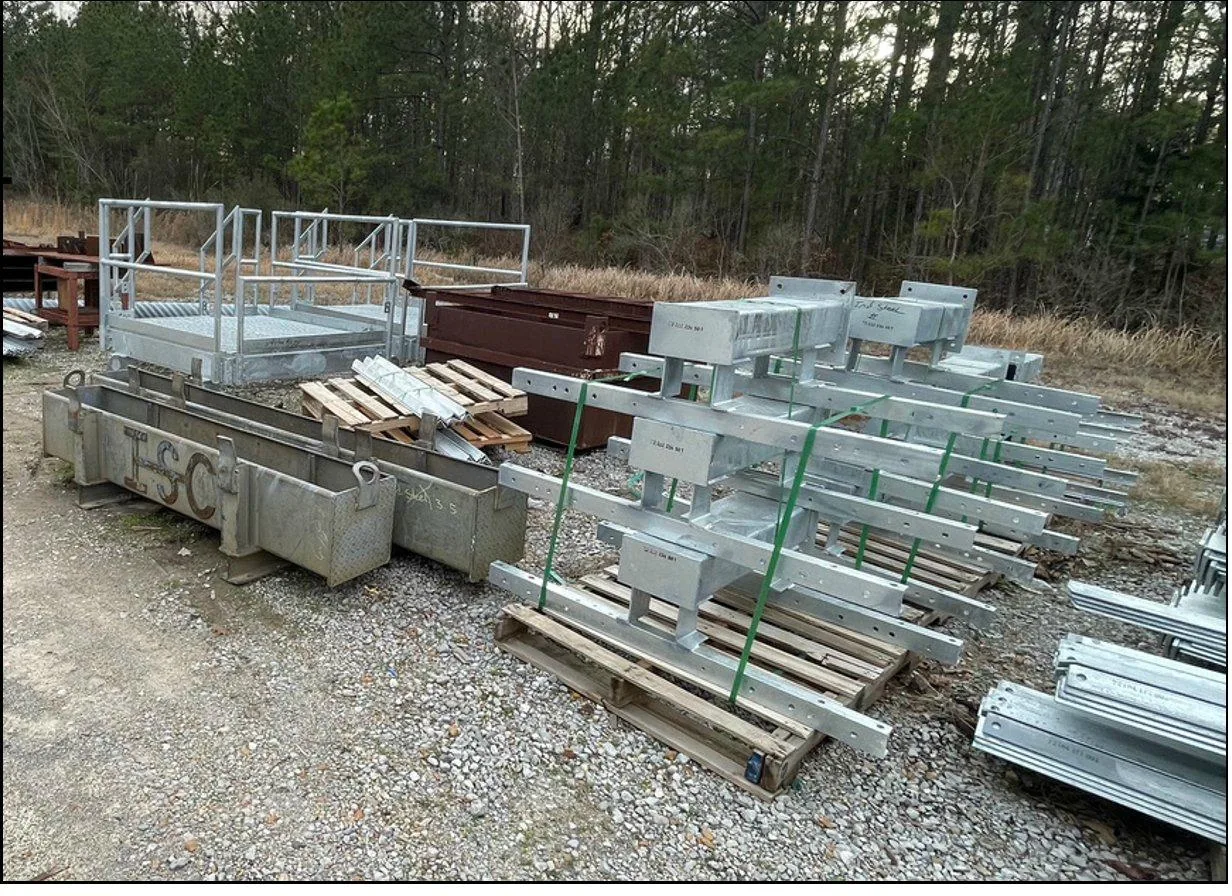
Part 4 of 8. Beam line to kettle: material traceability, robotic processing, AWS D1.1 welding and inspection, the galvanizing bath, ASTM A123 inspection and repair.
Read post →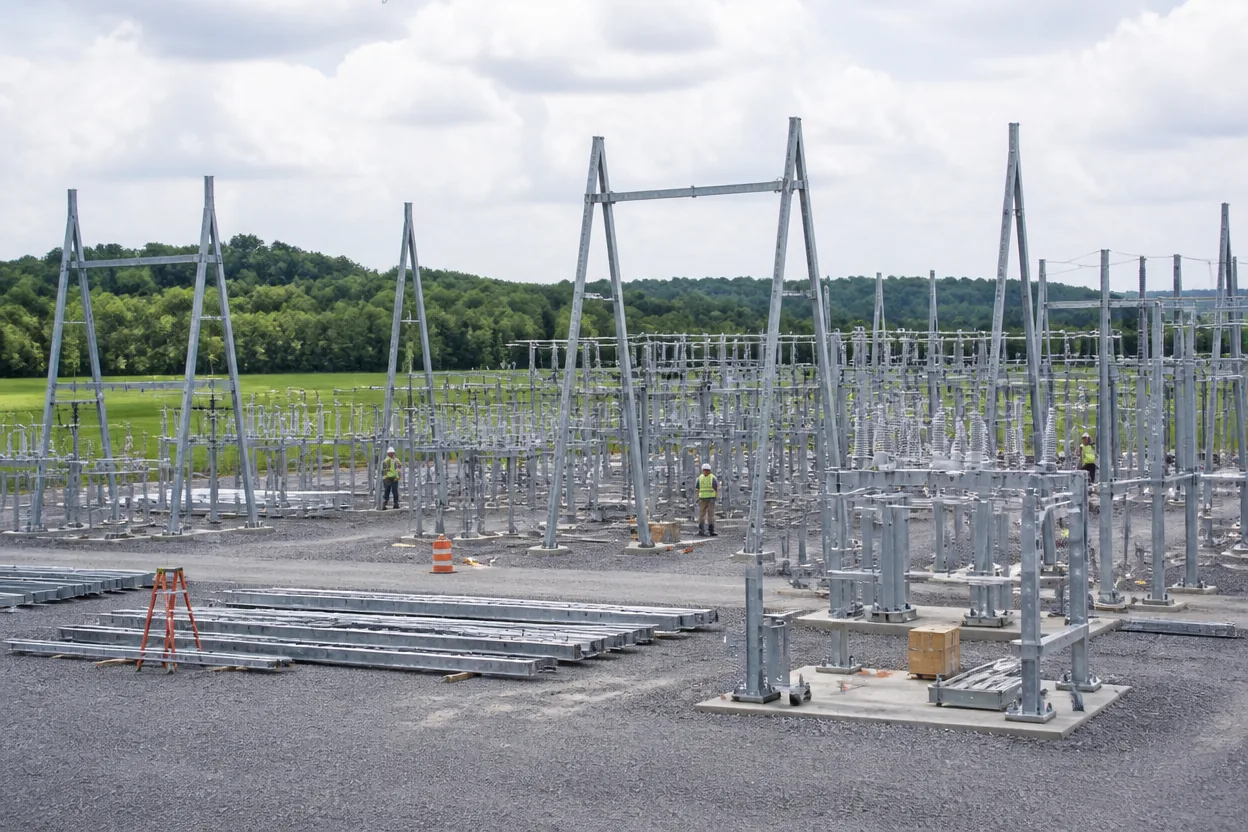
Part 5 of 8. Bundled by structure, loaded in erection order, match-marked, kitted with hardware, staged on dunnage — the logistics that keep the crane working.
Read post →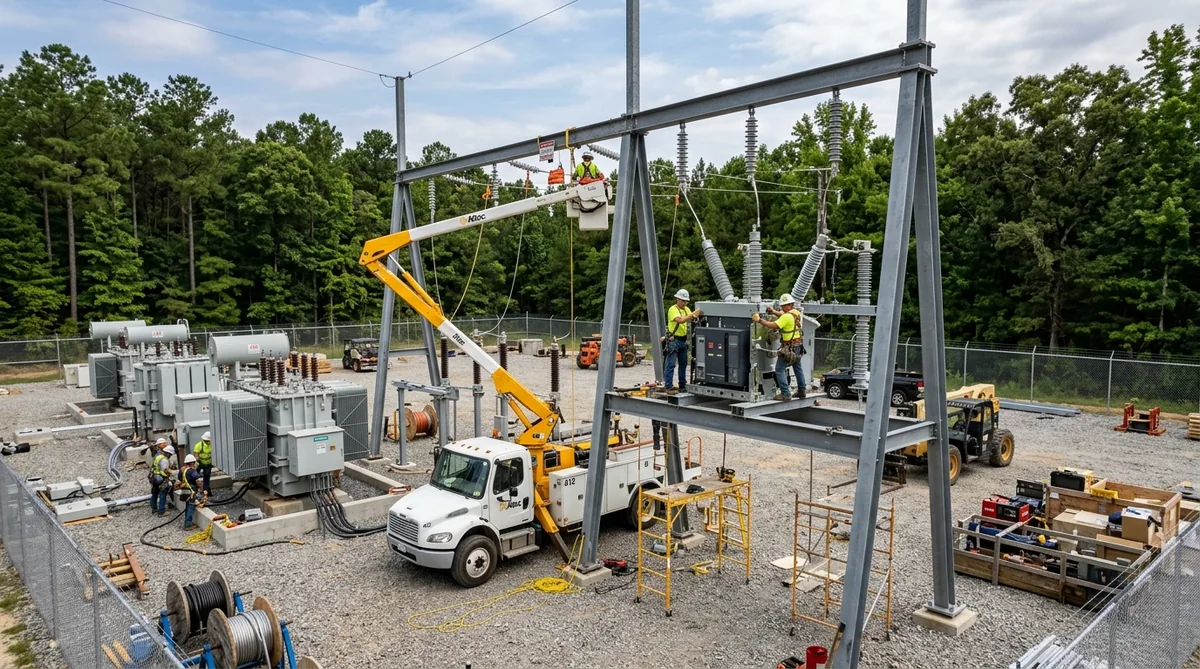
Part 6 of 8. Anchor-bolt survey, sequence, setting and plumbing, bolting, grounding, equipment setting — and why fabricator-erected steel removes the biggest handoff.
Read post →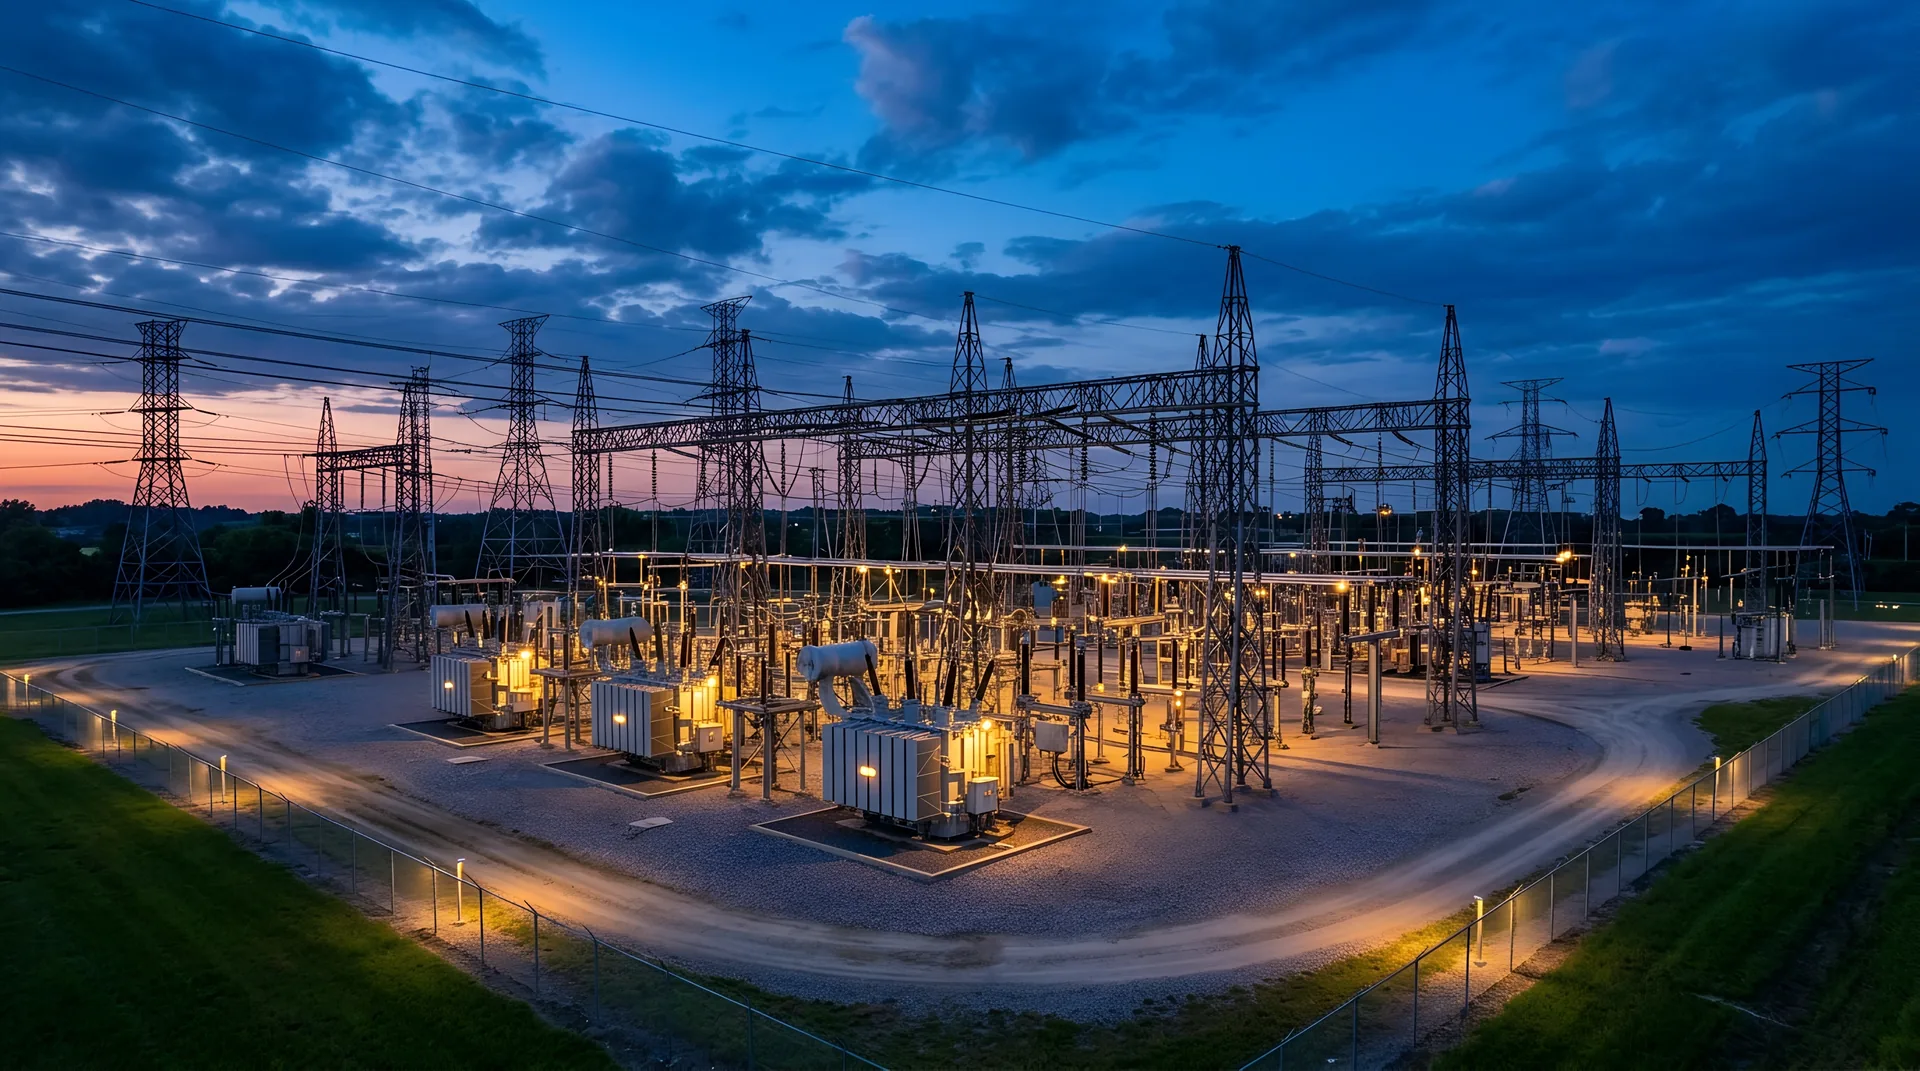
Part 7 of 8. Acceptance tests, relay checks, ground-grid tests, the walkdown and the staged energization sequence — and where clearances, grounding and bus alignment trace back to the steel.
Read post →
Part 8 of 8. Substituted equipment, revised bus heights, added bays, misplaced anchor bolts — how late changes hit the steel and how to manage them without losing the date.
Read post →
Part 1 of 7. What tank and cabinet fabrication costs an OEM in floor, crane and welders — and how outsourcing the metal adds output without adding a plant.
Read post →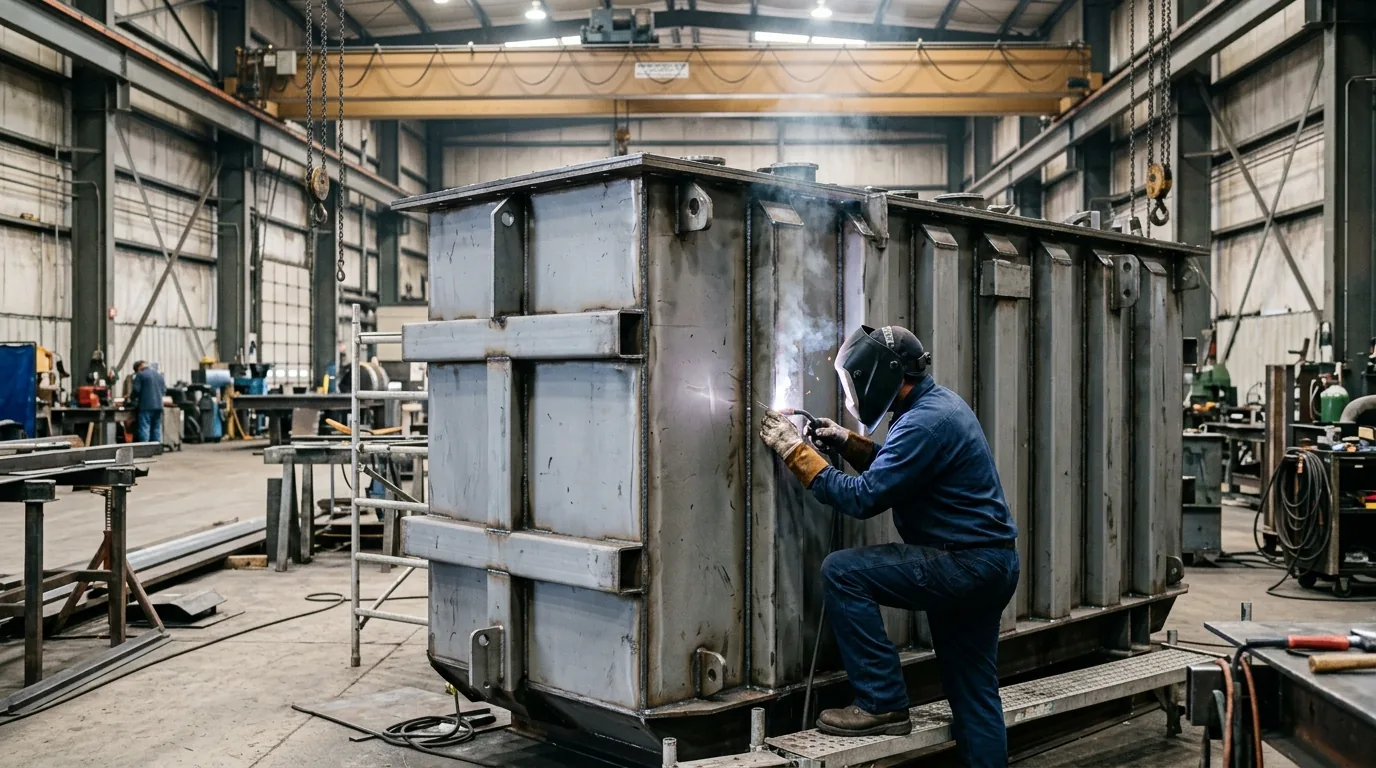
Part 2 of 7. Weld procedures, pressure and vacuum test, plate traceability, coatings, first-article, capacity — the checklist before the first tank PO.
Read post →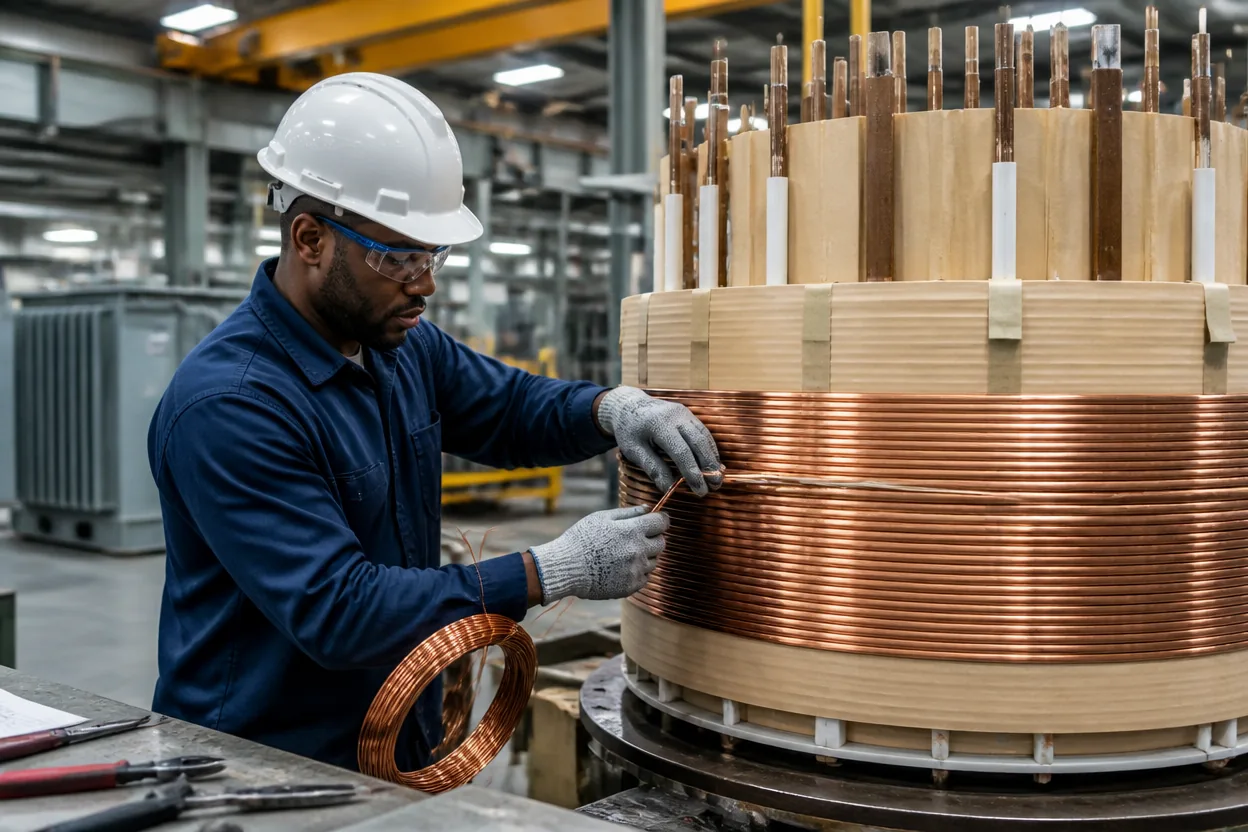
Part 3 of 7. Winding labor is the industry’s hardest constraint. When outsourcing windings and core-and-coil sub-assemblies makes sense, what to specify, and how a program runs.
Read post →
Part 4 of 7. Covers with turrets and gasket faces, conservators, cable boxes, radiator supports, bases and lifting hardware — the next tier of transformer metal, and why to buy it with the tank.
Read post →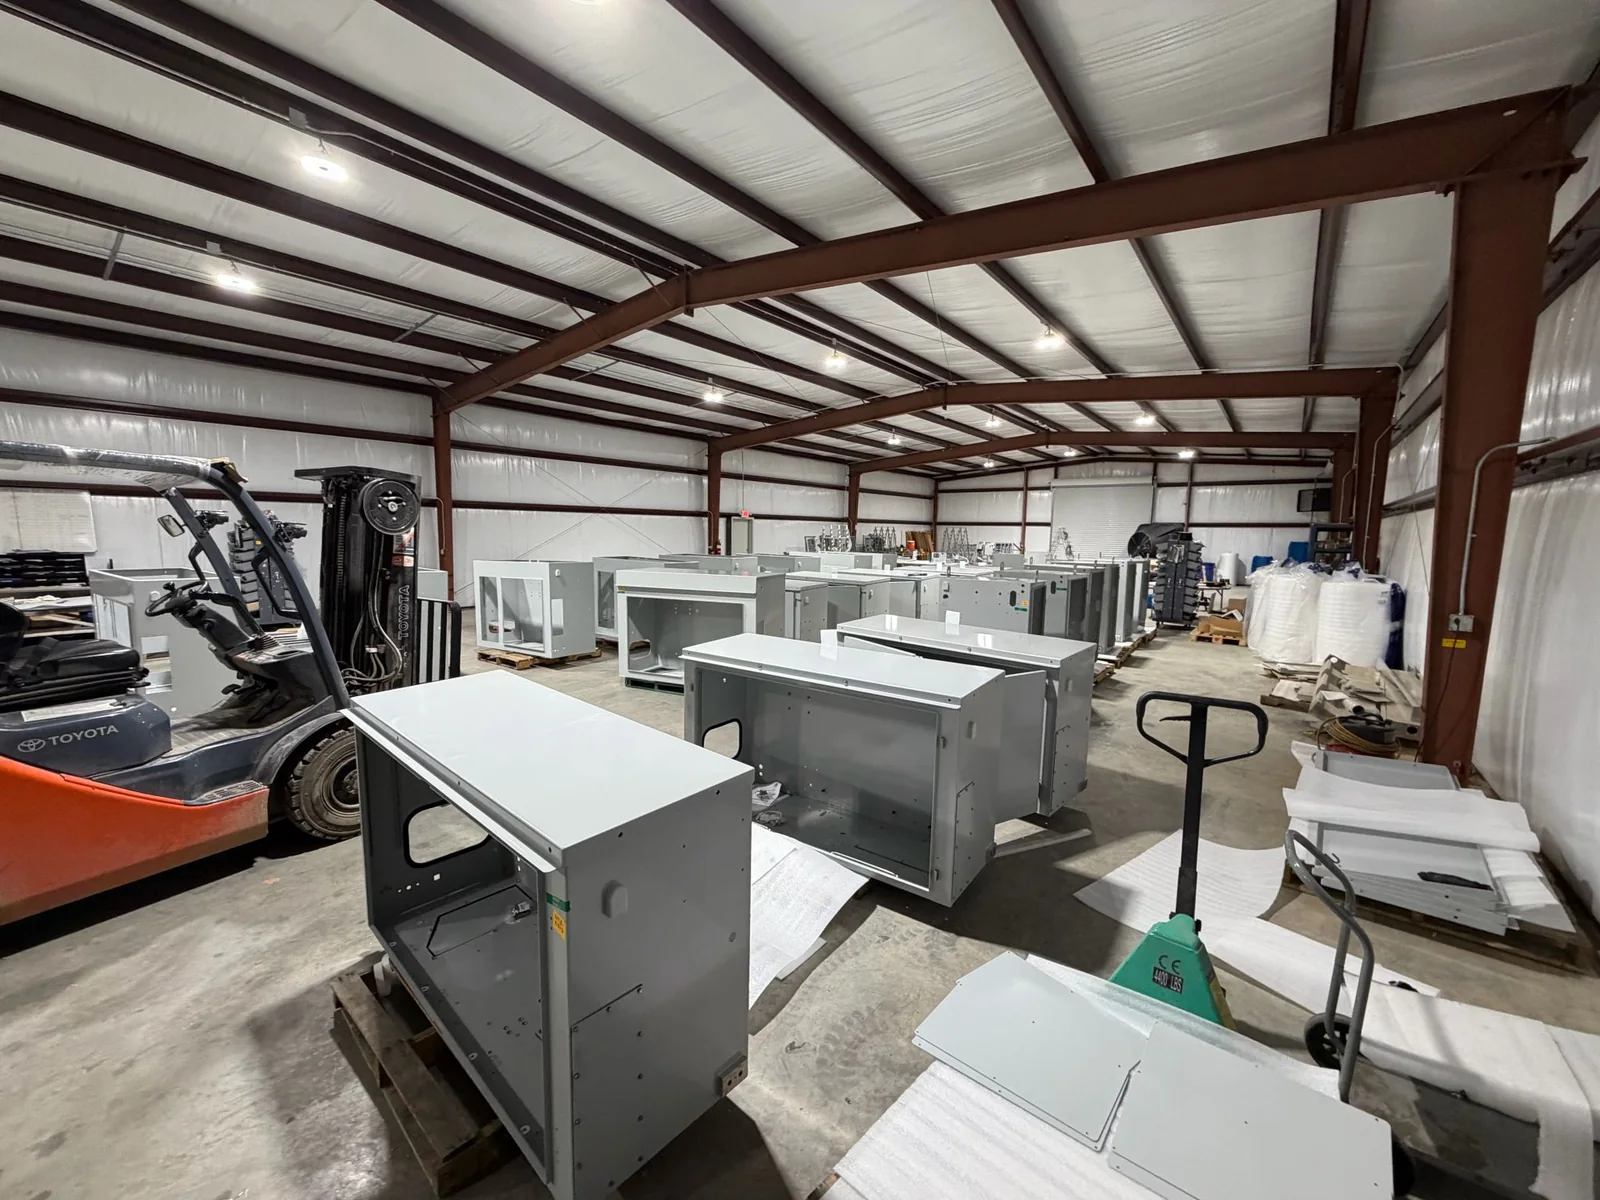
Part 5 of 7. Blanket agreement, reserved line, releases against the build plan, revision control, consigned material, kanban and the weekly call — how a multi-year program actually runs.
Read post →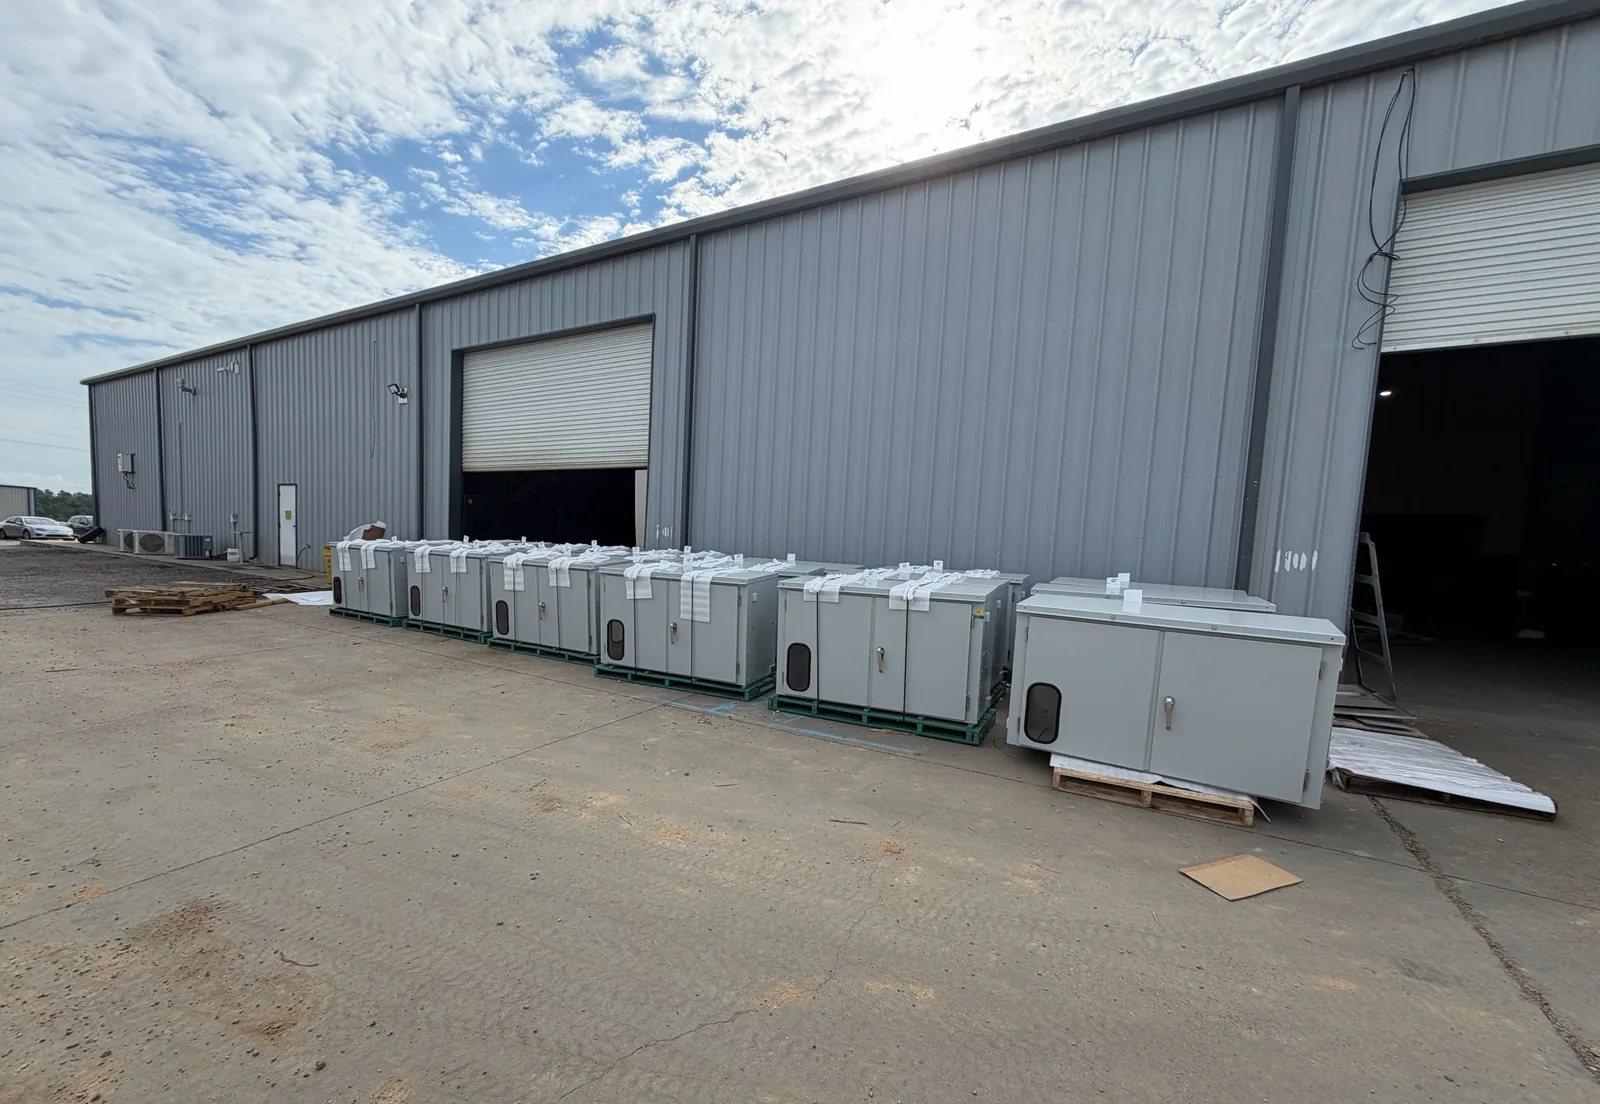
Part 6 of 7. What a day of stalled output really costs, what reserved capacity costs, and why the lowest unit price is often the most expensive supplier you can pick.
Read post →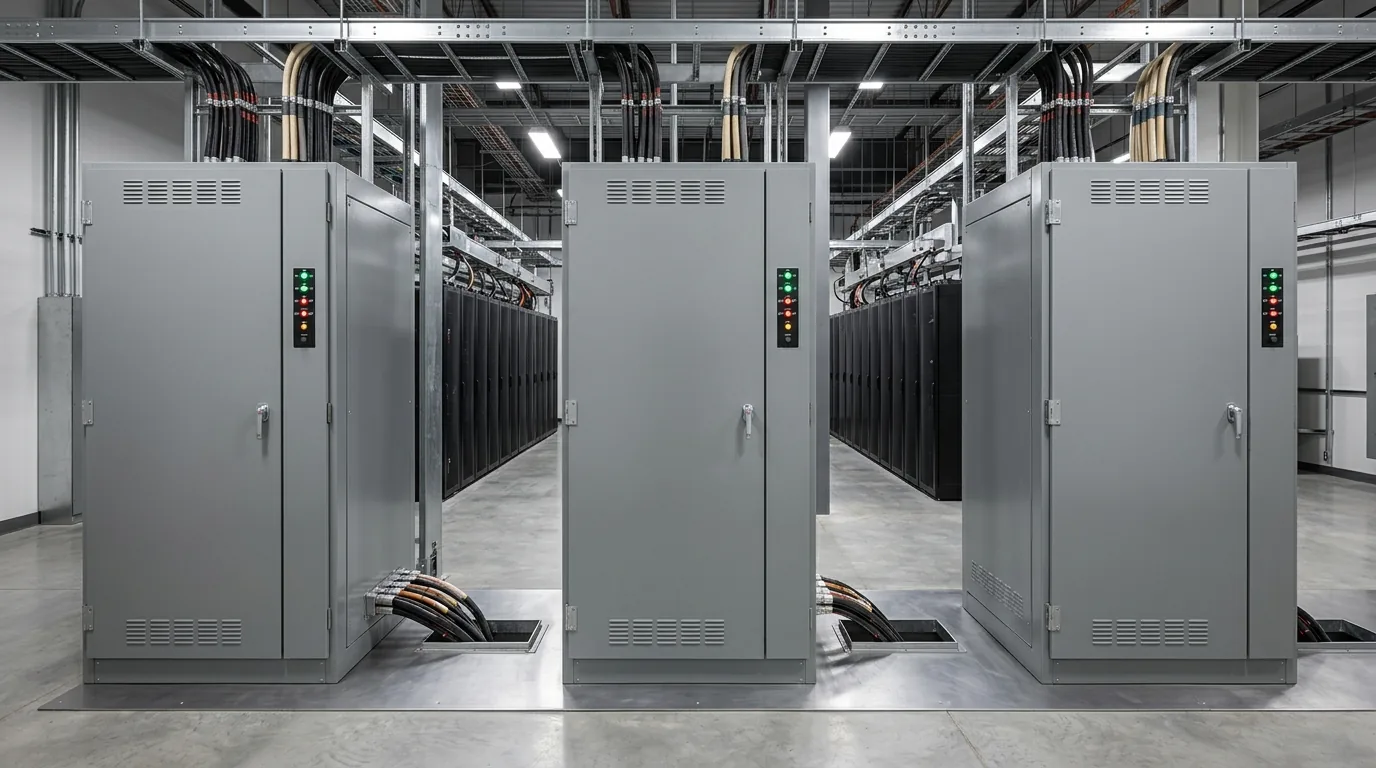
Part 1 of 10. Walk-in NEMA 3R houses, indoor sections and paralleling-gear enclosures — what to specify, how they’re fabricated, and how to source them on schedule.
Read post →Part 2 of 10. Feeder duct vs. row busway, 1,600–6,000+ A ratings, non-seg vs. iso-phase, and what it takes to fabricate housings that align across a 300-foot run.
Read post →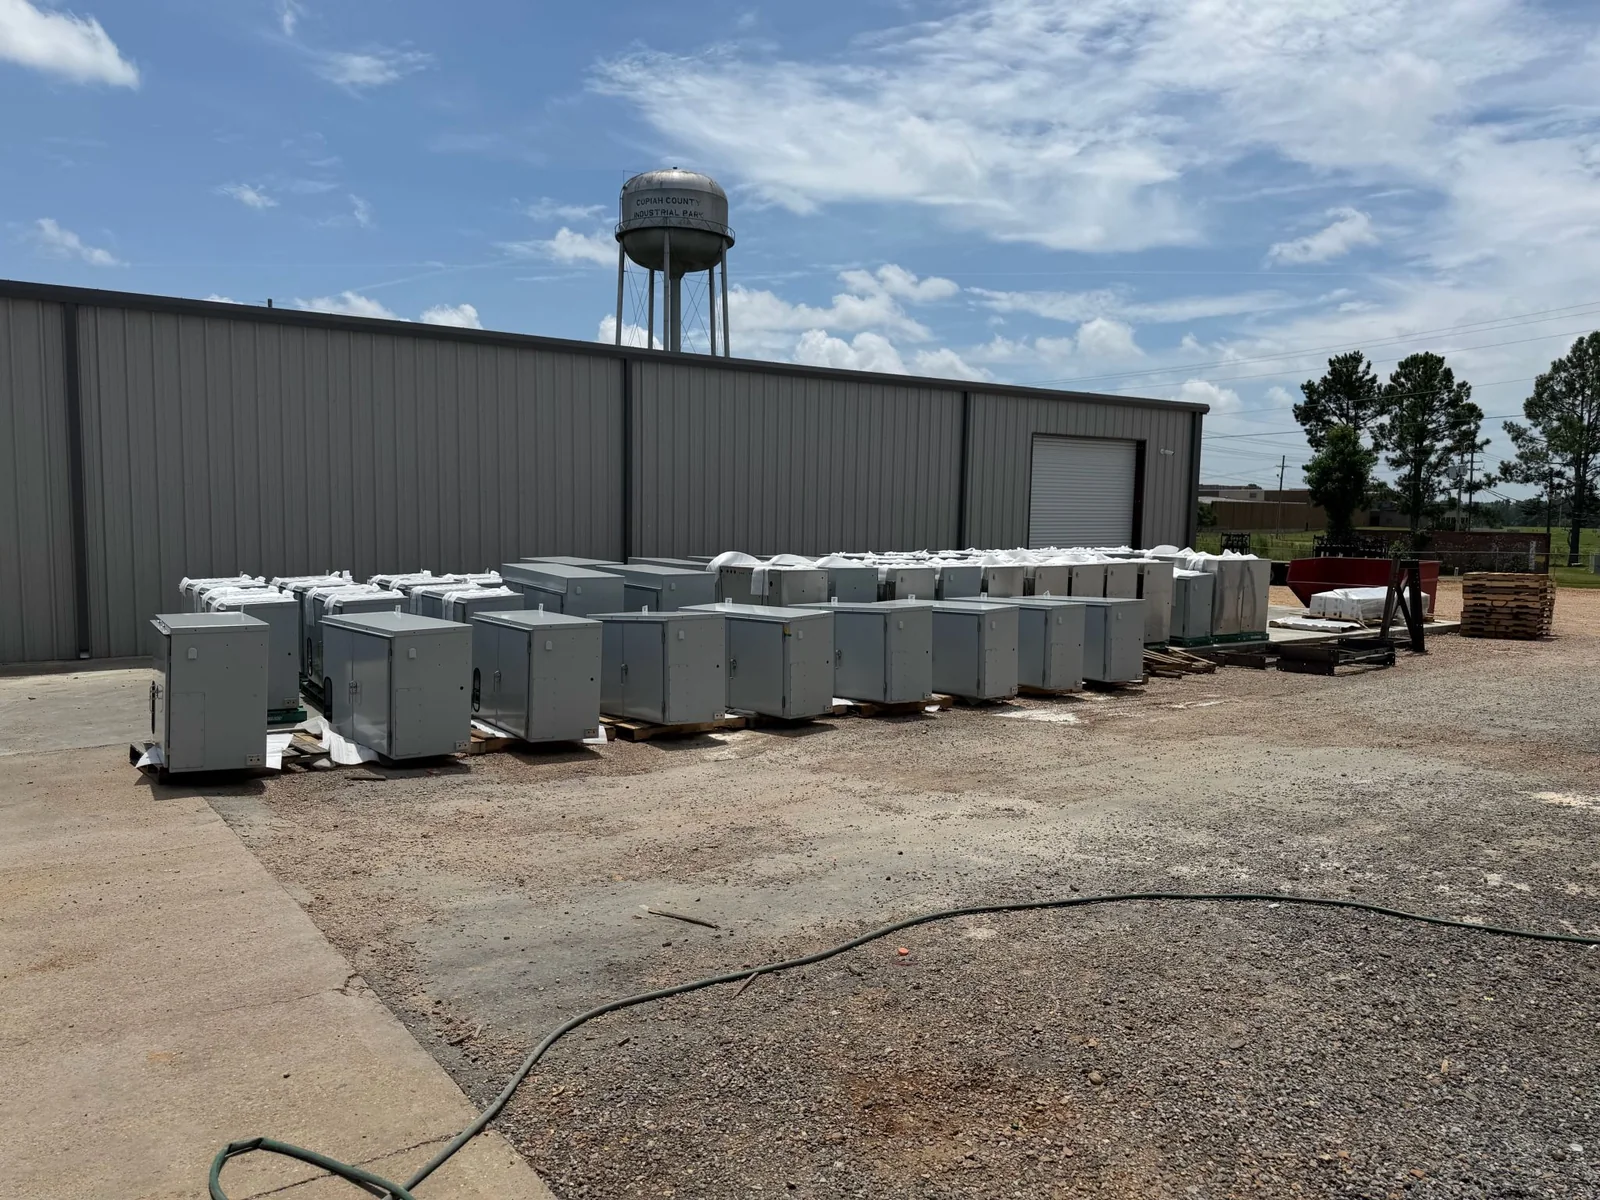
Part 3 of 10. Pad-mount cabinets, dry-type enclosures and unit-substation housings — the NEMA 3R spec, the finish that lasts 30 years outdoors, and building them by the hundred.
Read post →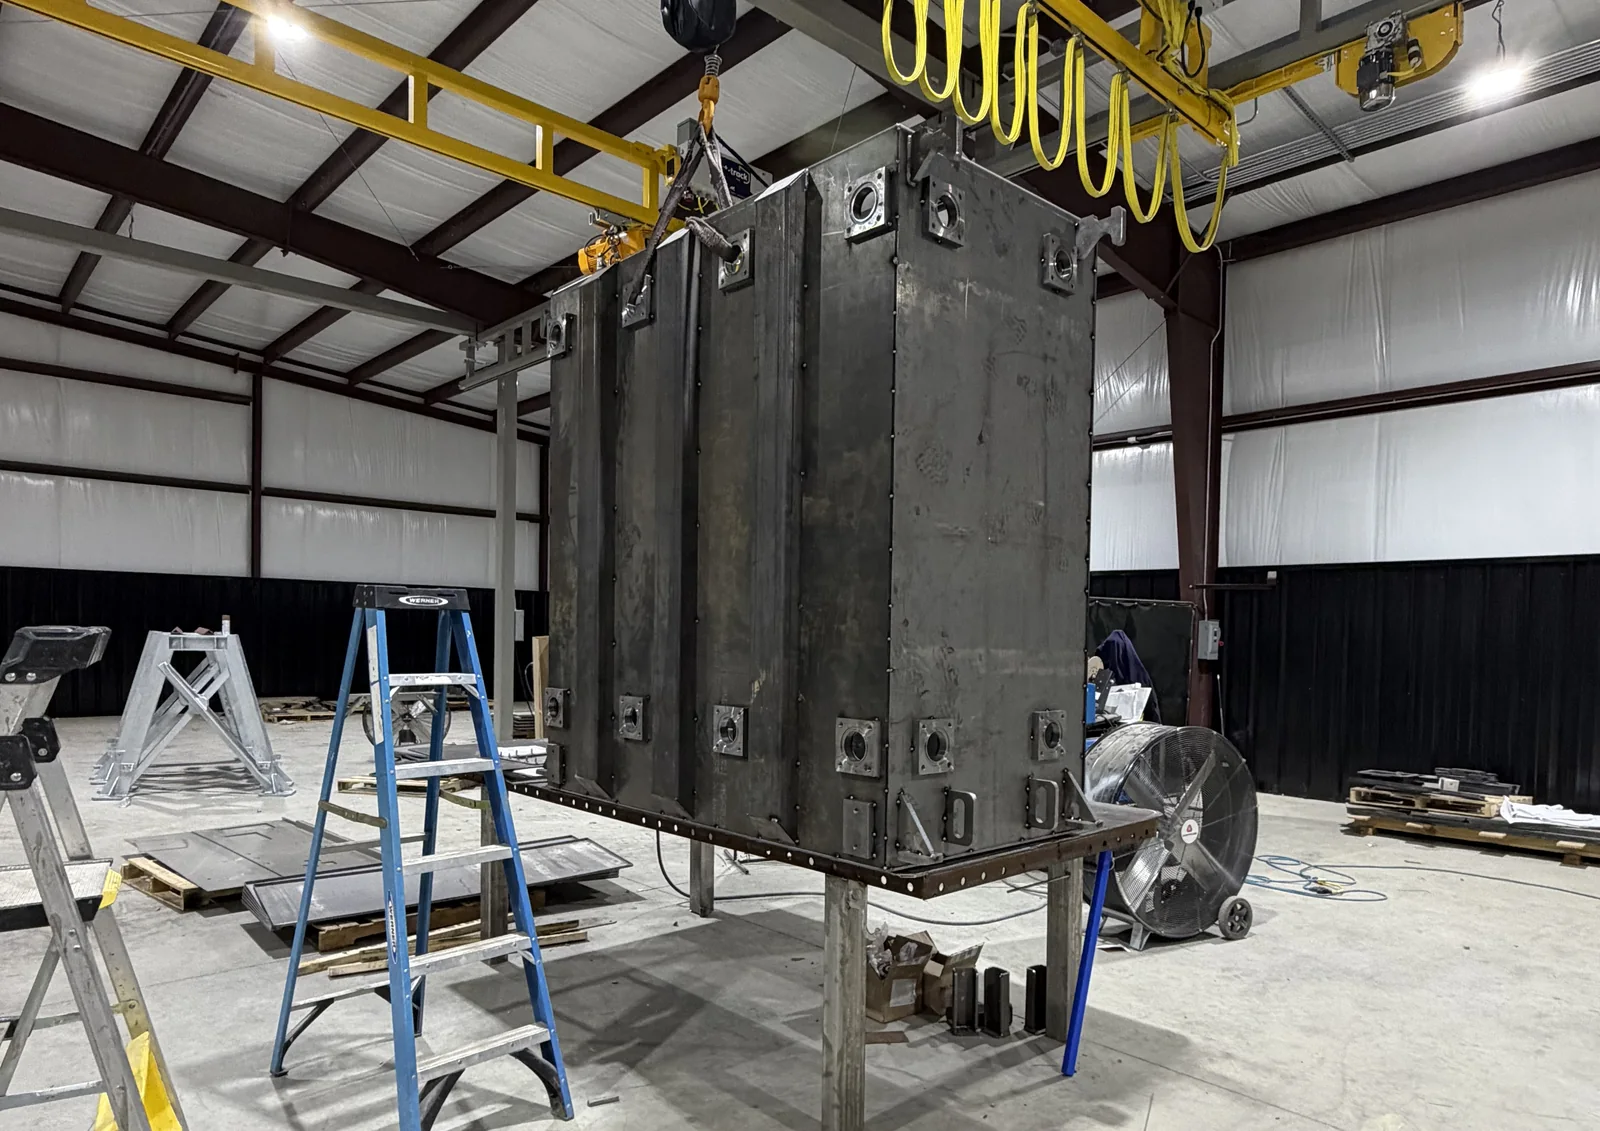
Part 4 of 10. Power, pad-mount, corrugated-wall and conservator tanks — plate, welding, testing, and why tank fabrication capacity is part of the transformer lead-time problem.
Read post →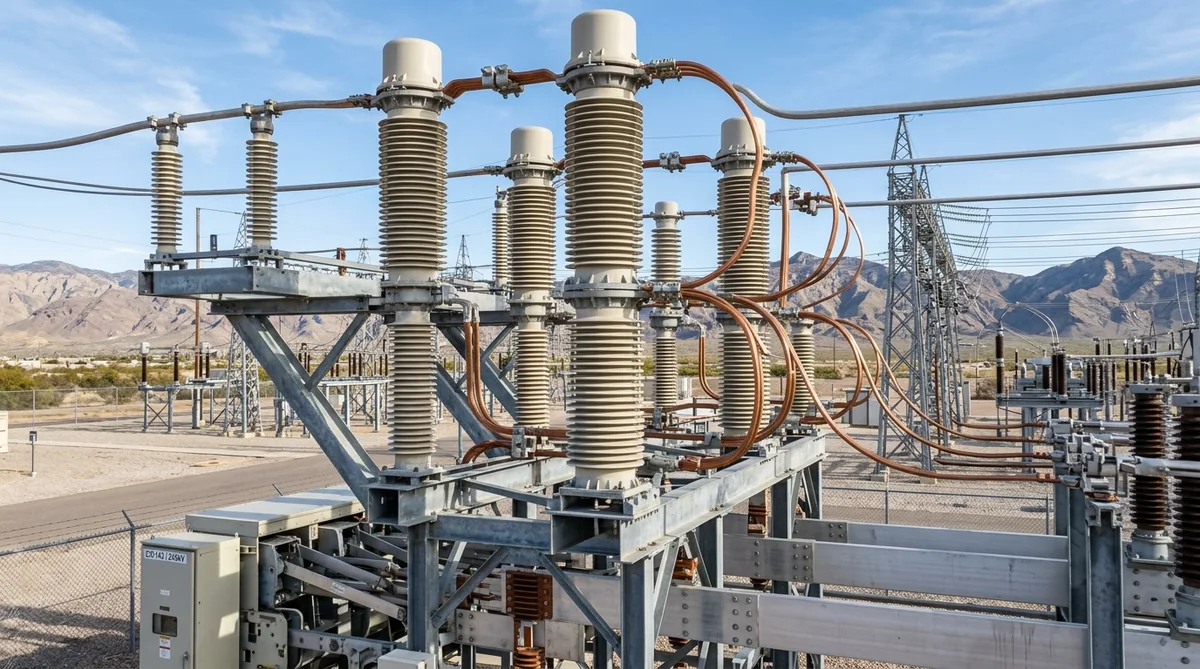
Part 5 of 10. Dead-ends, A-frames, bus supports, equipment stands and control enclosures — the galvanized steel a campus substation stands on, and why to order it before the transformer.
Read post →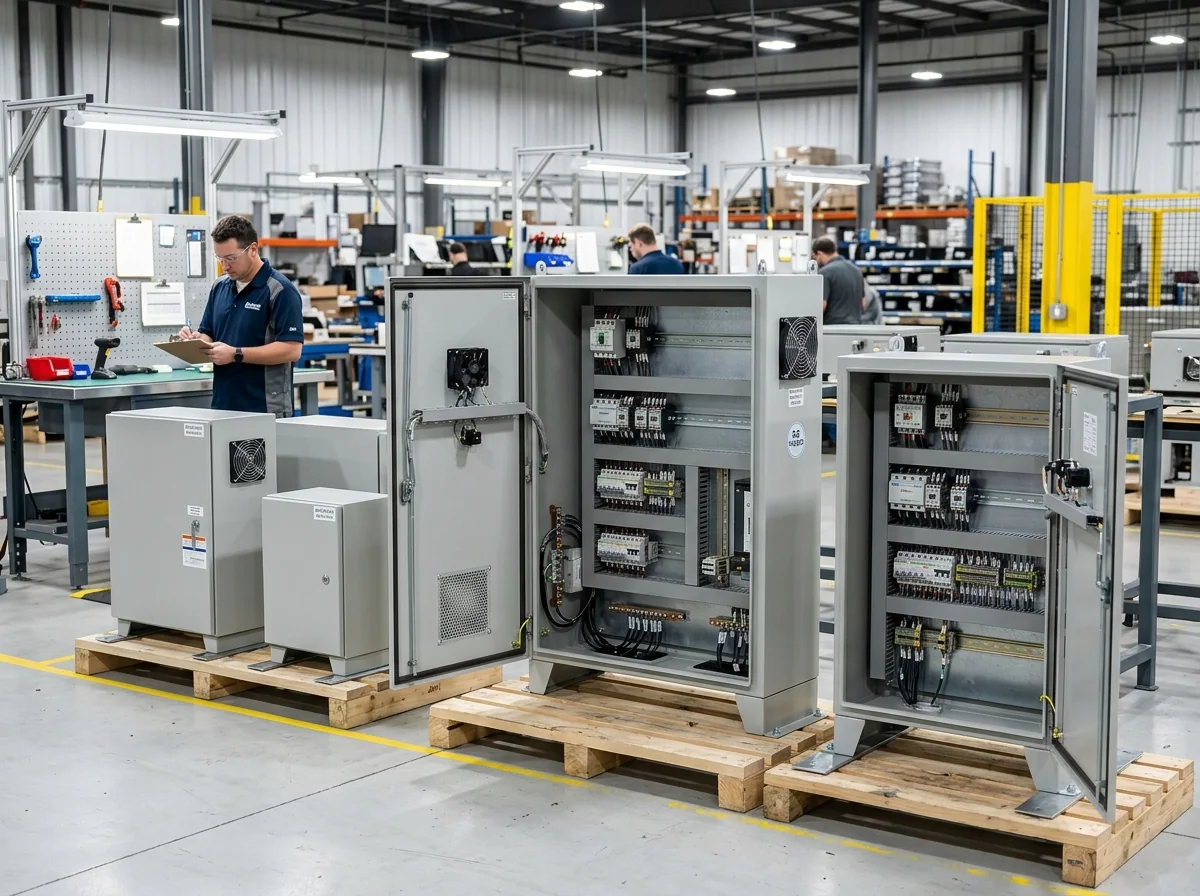
Part 6 of 10. The cabinets between the switchgear and the rack — PDUs, RPPs, UPS and battery housings, control panels — and why buying them wired changes the schedule.
Read post →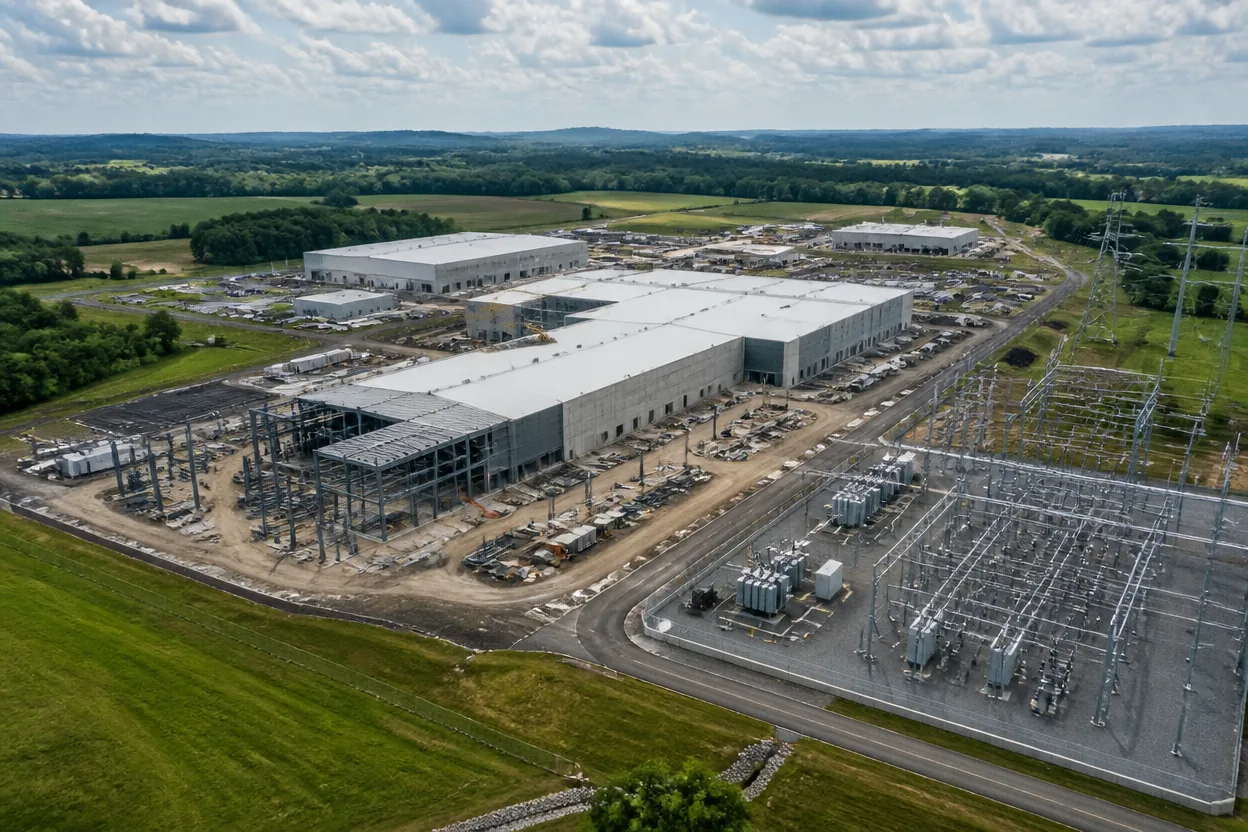
Part 7 of 10. Sound-attenuated generator enclosures, fuel bases and containment, and weatherproof BESS enclosures — the steel around backup power, built before the engines arrive.
Read post →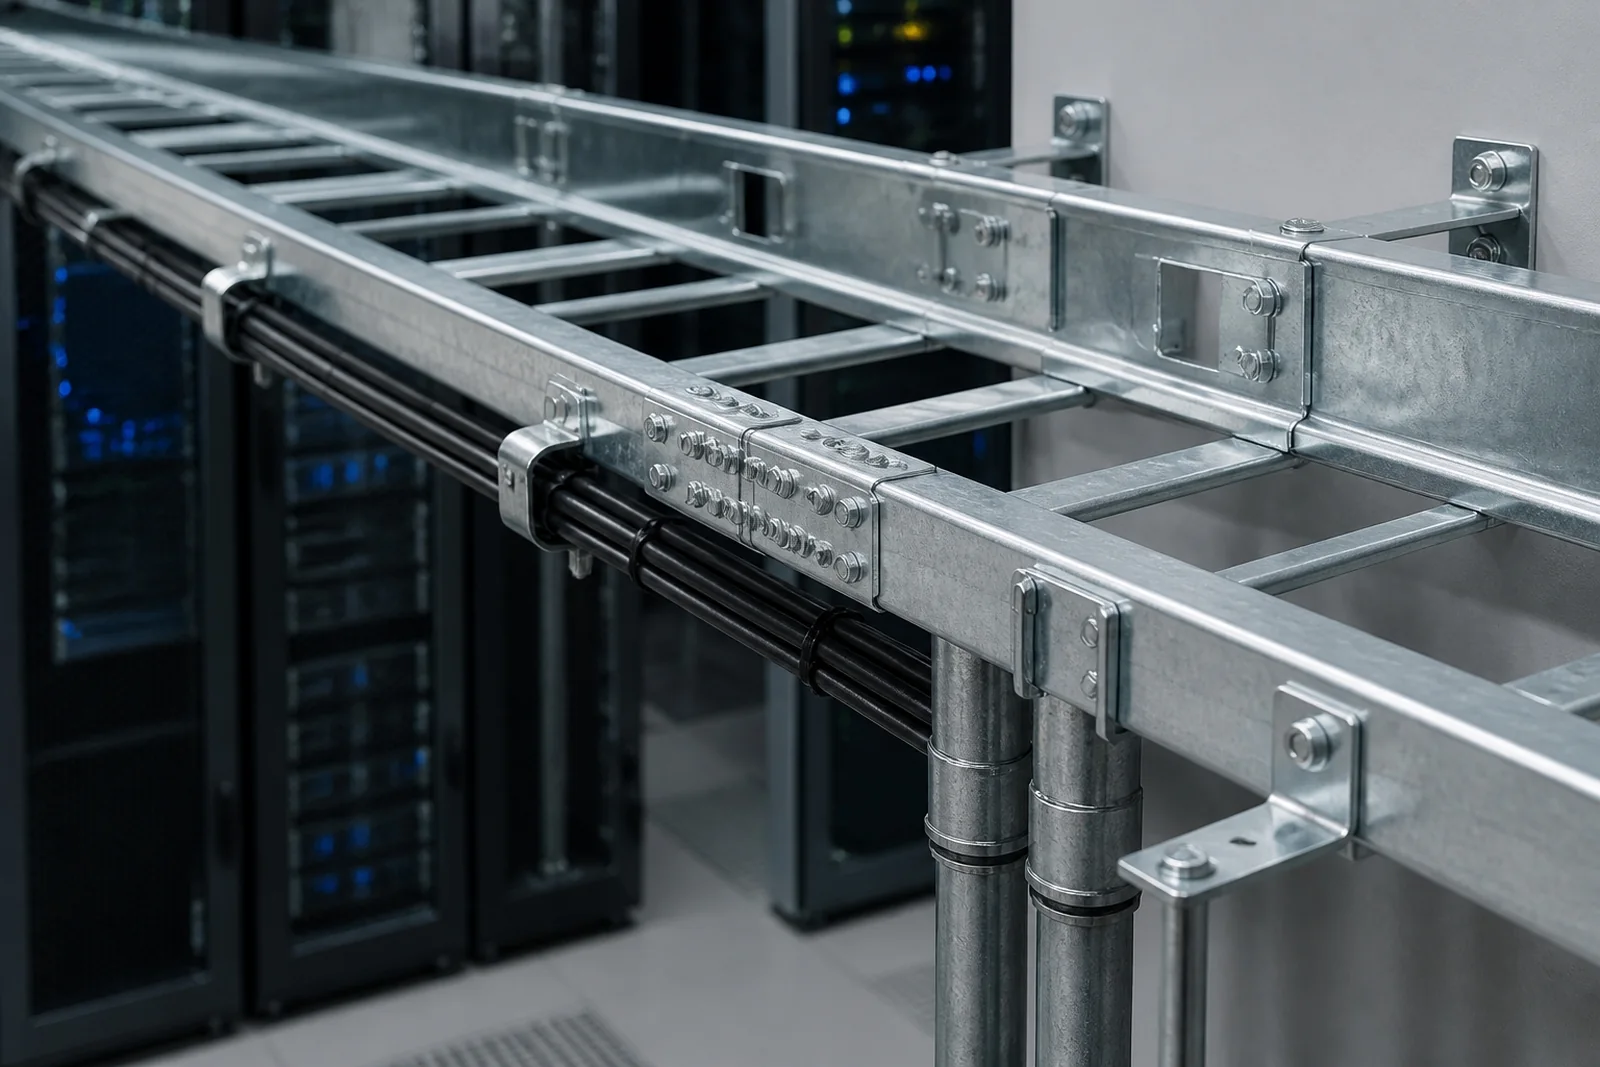
Part 8 of 10. Trapeze hangers, wall brackets, conduit racks, busway hangers and overhead support frames — thousands of parts, delivered in the order the trades install them.
Read post →Part 9 of 10. CDU frames, pump and electrical skids, mezzanine steel, platforms and dunnage — the structural steel that liquid cooling and prefabrication brought into the data hall.
Read post →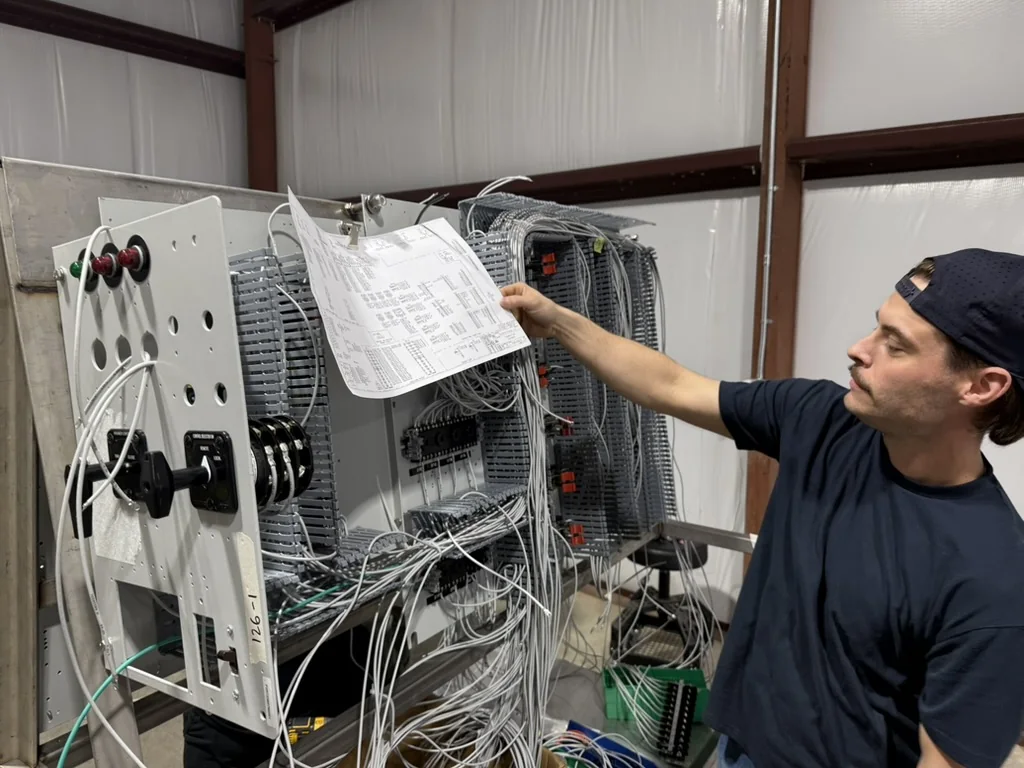
Part 10 of 10. Component mounting, point-to-point wiring, harnesses, labeling and bench testing — the step that turns an enclosure into a finished product before it reaches the site.
Read post →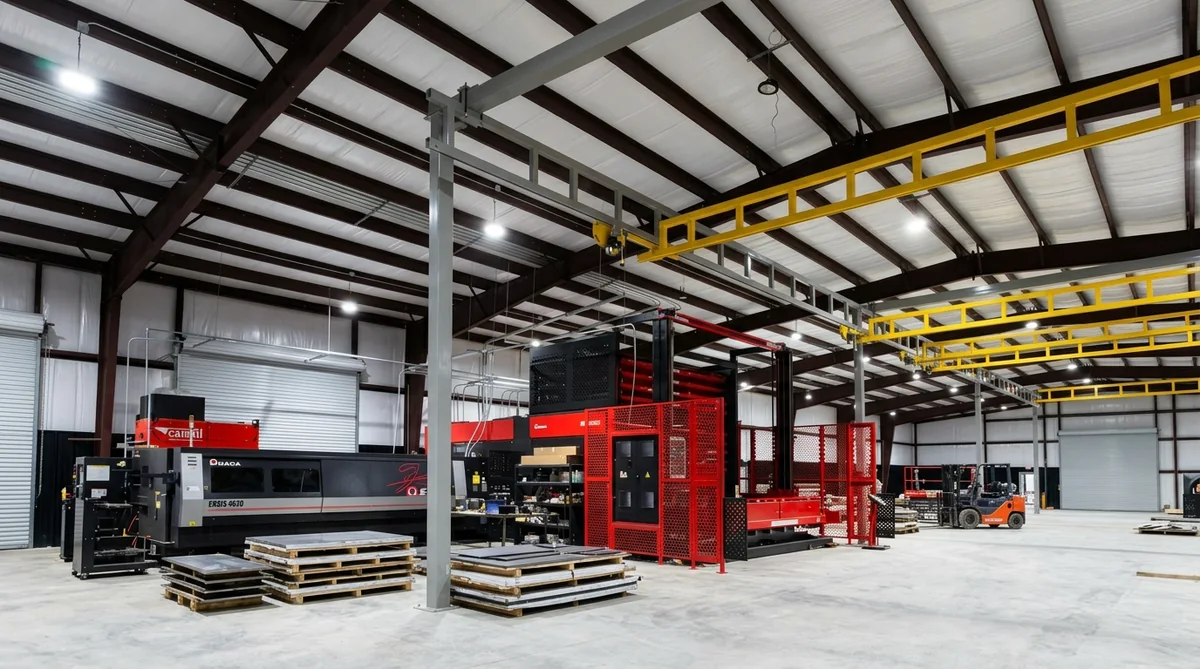
Part 1 of 7. The six core processes — cutting, forming, welding, machining, finishing, assembly — and how a part moves from drawing to truck.
Read post →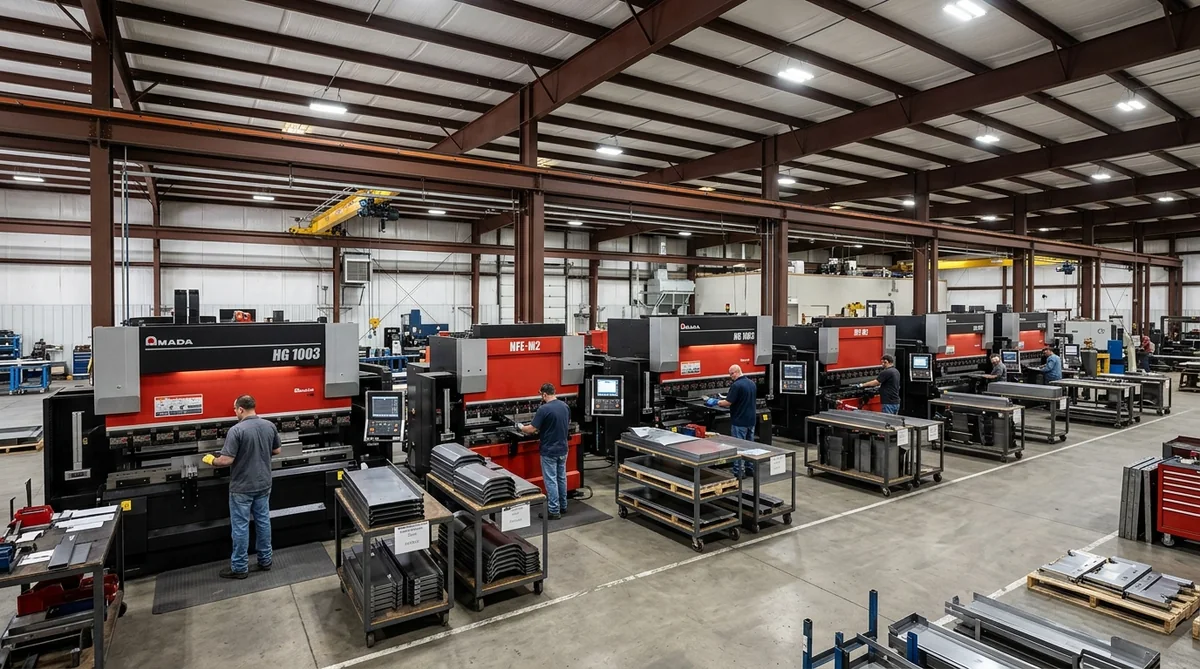
Part 2 of 7. What each machine does and why it matters — fiber lasers, CNC press brakes, robotic plasma, waterjet, CNC machining, welding cells and the finish line.
Read post →Part 3 of 7. Carbon steel, stainless, aluminum, galvanized sheet, copper — grades, gauges, forms, how each behaves in the shop, and how to choose for the environment.
Read post →
Part 4 of 7. Blacksmiths and the American System, the steel boom, welding’s wartime rise, NC and CNC, the offshoring decades — and the shops that held on.
Read post →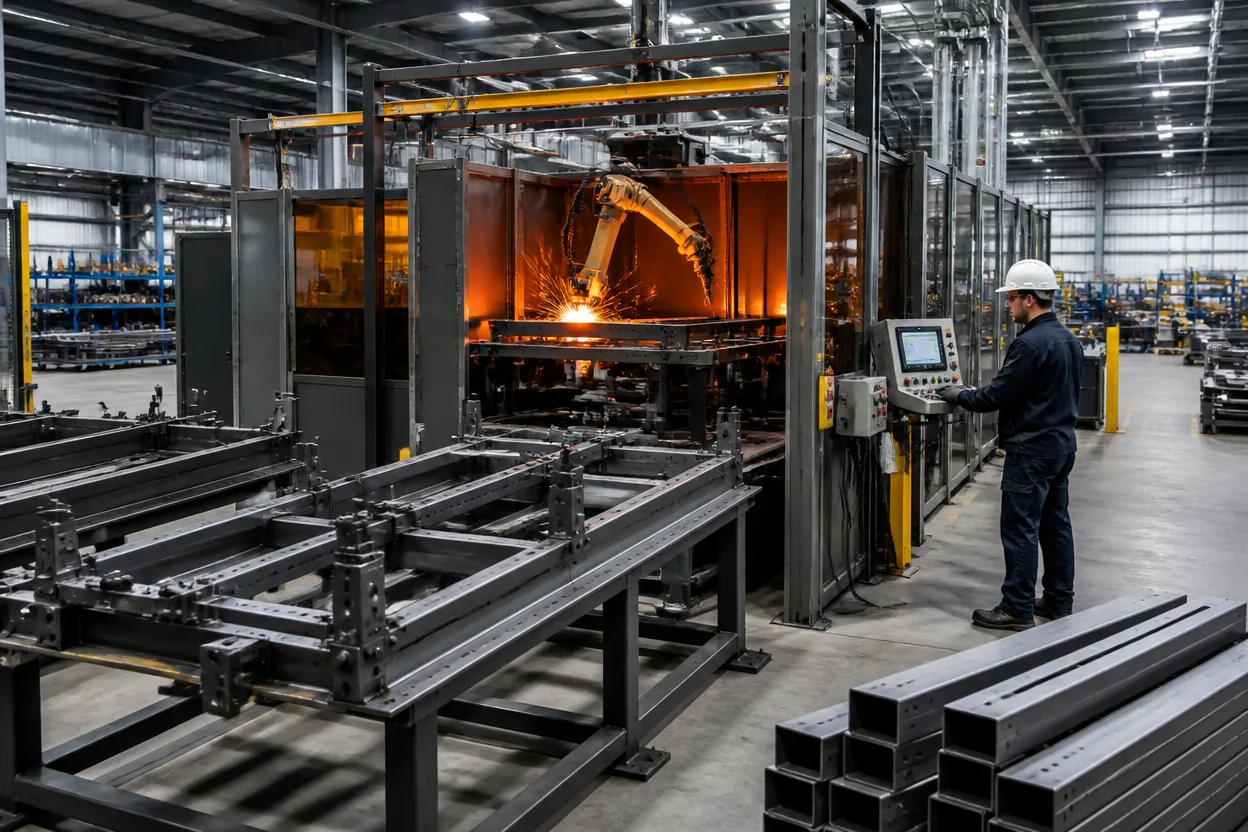
Part 5 of 7. Layout tables to lasers, hand welding to robotic cells, whiteboards to AI-native ERP — the breakthroughs, what they replaced, and what comes next.
Read post →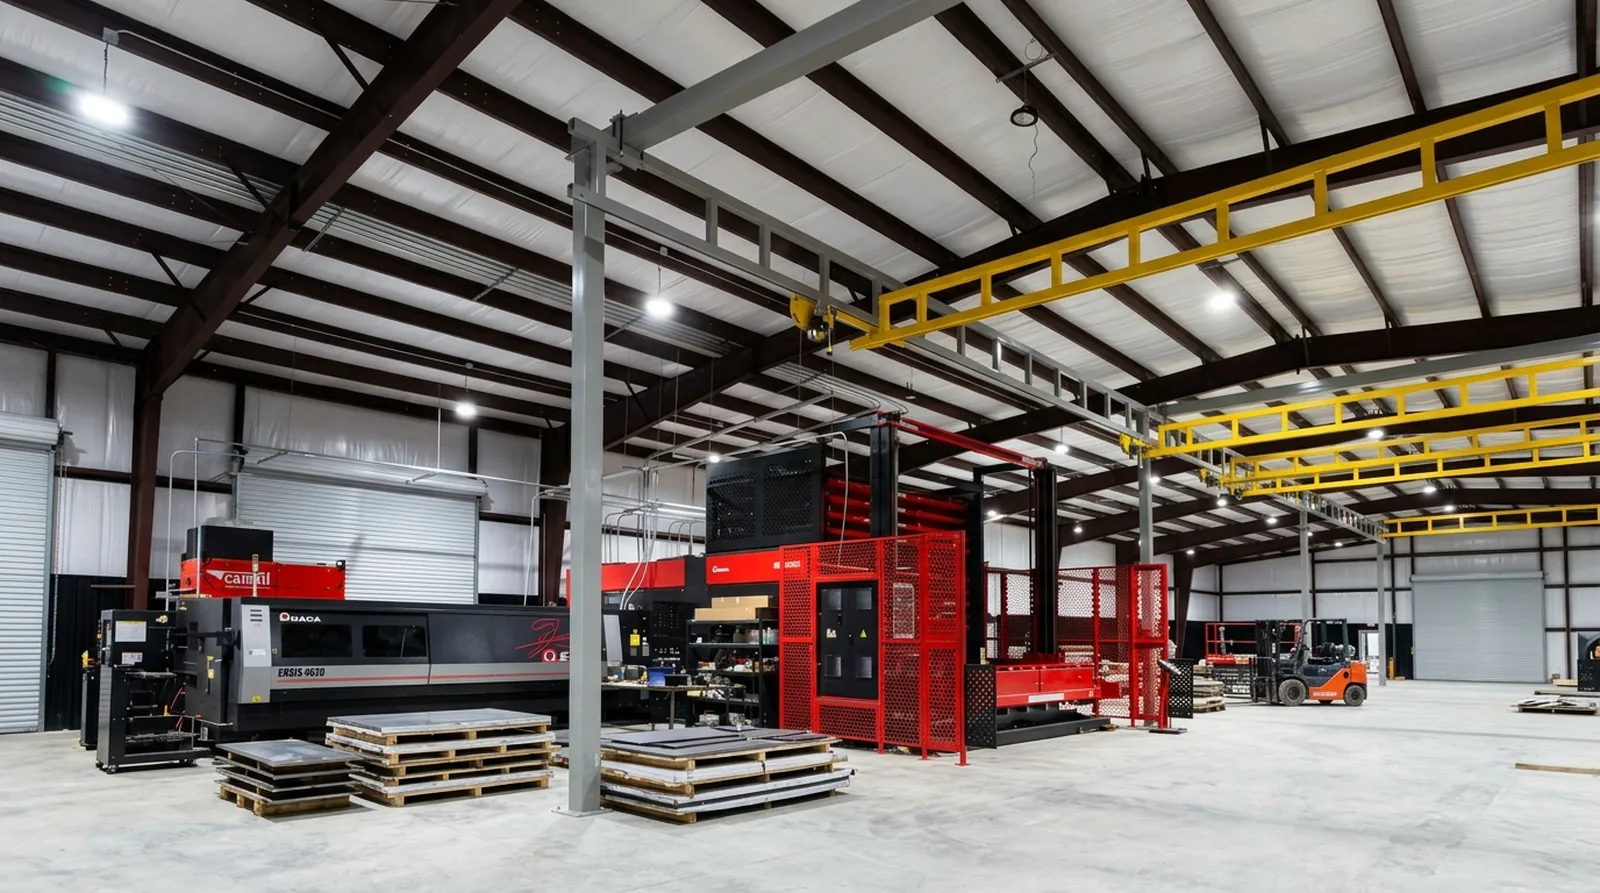
Part 6 of 7. Grid transformers and substations, the data center build-out, reshored plants and OEM outsourcing — four demand waves hitting U.S. shops at once, and how they’re responding.
Read post →
Part 1 of 10. Hard, heavy, angular powders grind through conveyors specified for something else — the material data, wear package, containment and structure that make a system last.
Read post →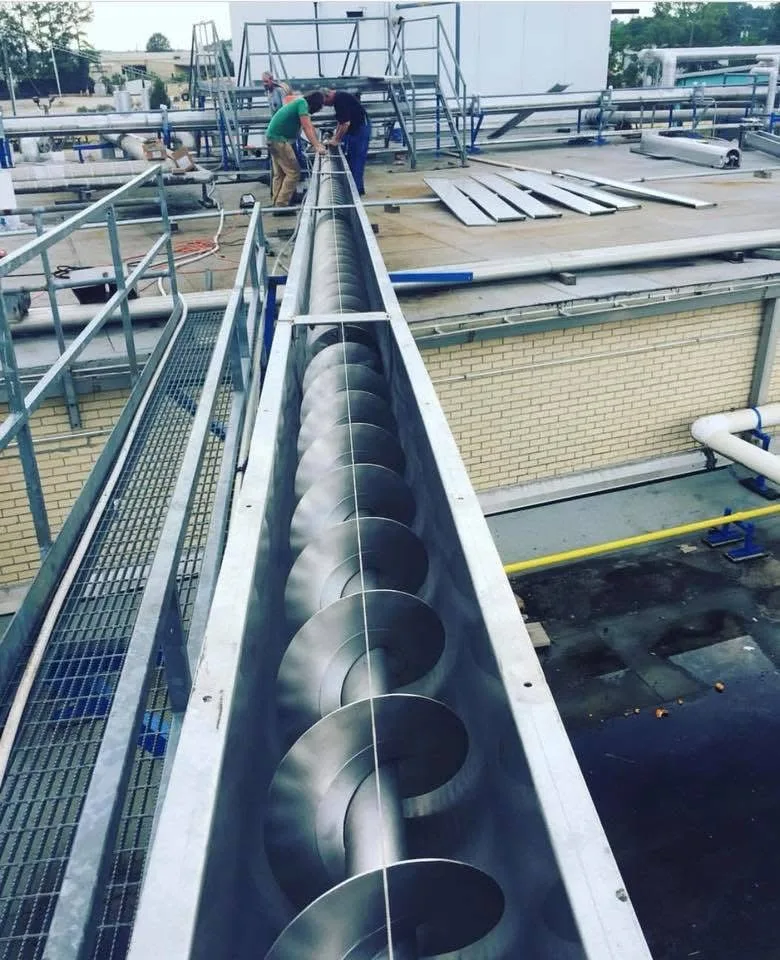
Part 2 of 10. Moving a bulk solid across a plant and up to height without spilling, dusting or stalling — how screw, drag, belt, bucket elevator and pneumatic options compare leg by leg.
Read post →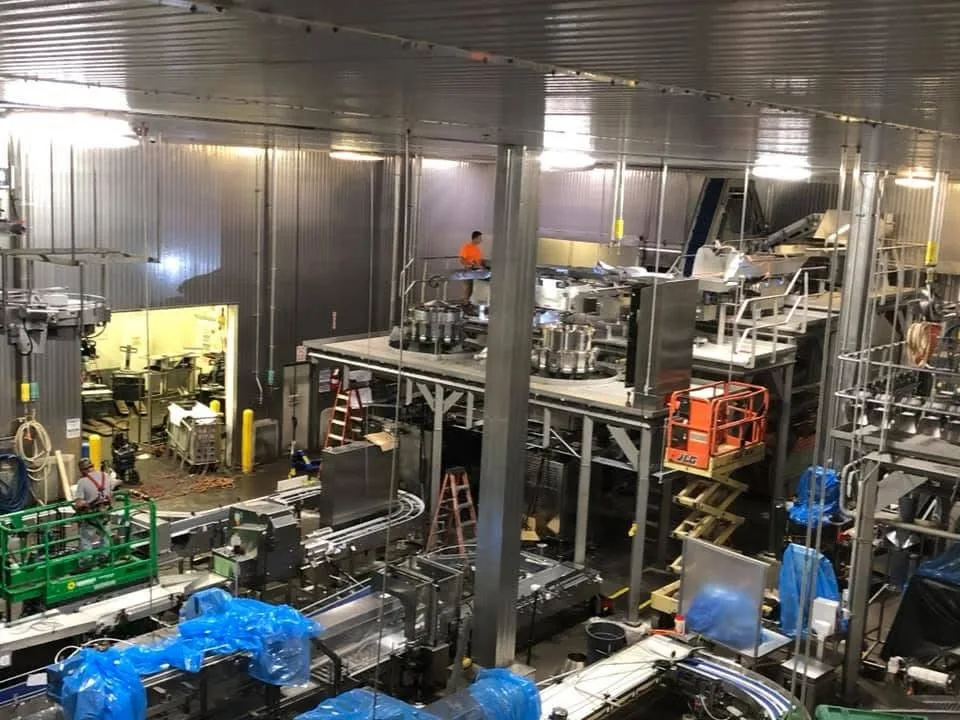
Part 3 of 10. Depots, shipyards, labs and bases buy conveyor, flow-rack track and structures under rules that favor domestic builders who can meet the spec exactly. How that buying works.
Read post →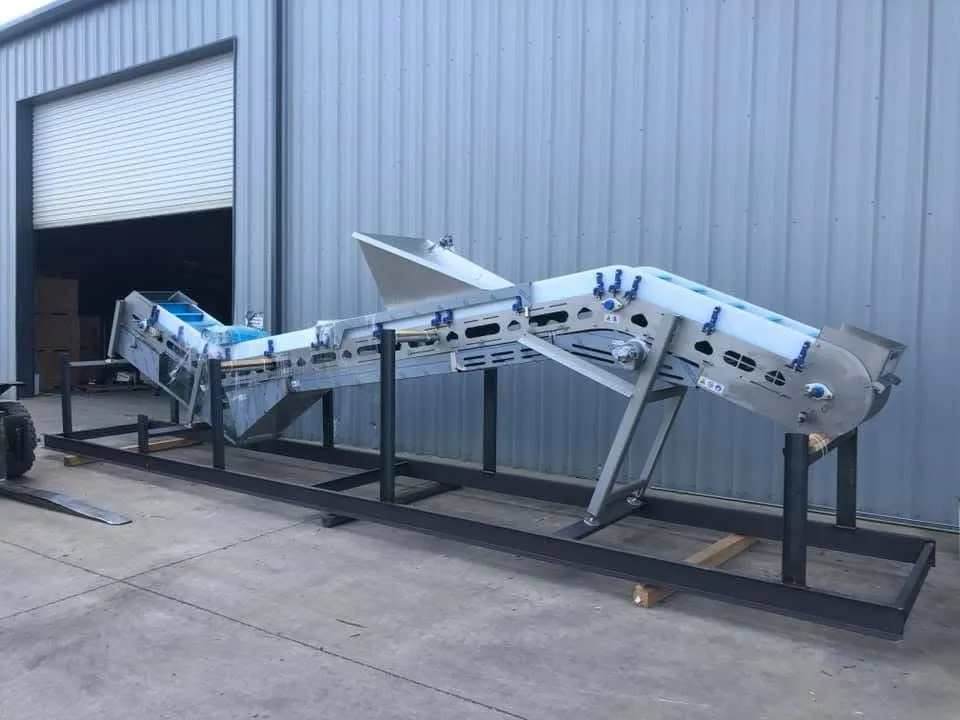
Part 4 of 10. A catalog conveyor is the right answer until the material is abrasive, the route climbs, or the structure has to carry a platform — five signs you need custom, and where the money goes.
Read post →
Part 5 of 10. Manufacturing construction is ~30% off its 2024 peak while reshoring announcements hold at ~244,000 jobs a year. The plants are moving from concrete to fit-out — and fit-out is conveyors.
Read post →Part 6 of 10. 50% on steel articles, 25% on derivatives, applied to full value. For a conveyor, that is most of the weight and most of the money — what Built in the U.S.A. changes on price and lead time.
Read post →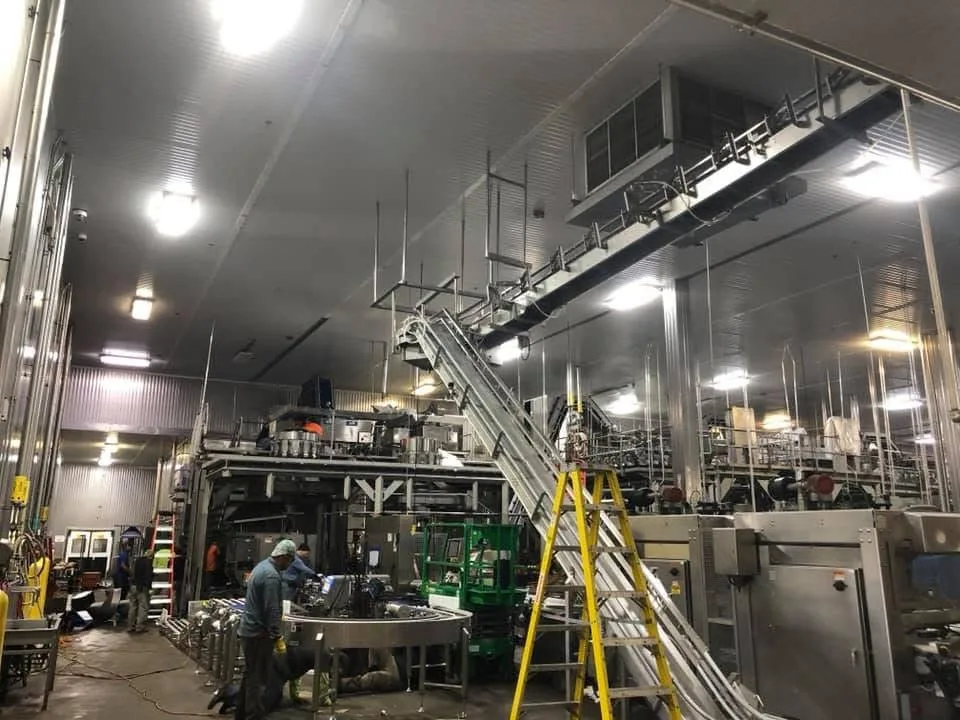
Part 7 of 10. Misalignment, weak supports and rushed commissioning cause more early failures than the equipment itself. The six steps our own crews follow from survey to first shift.
Read post →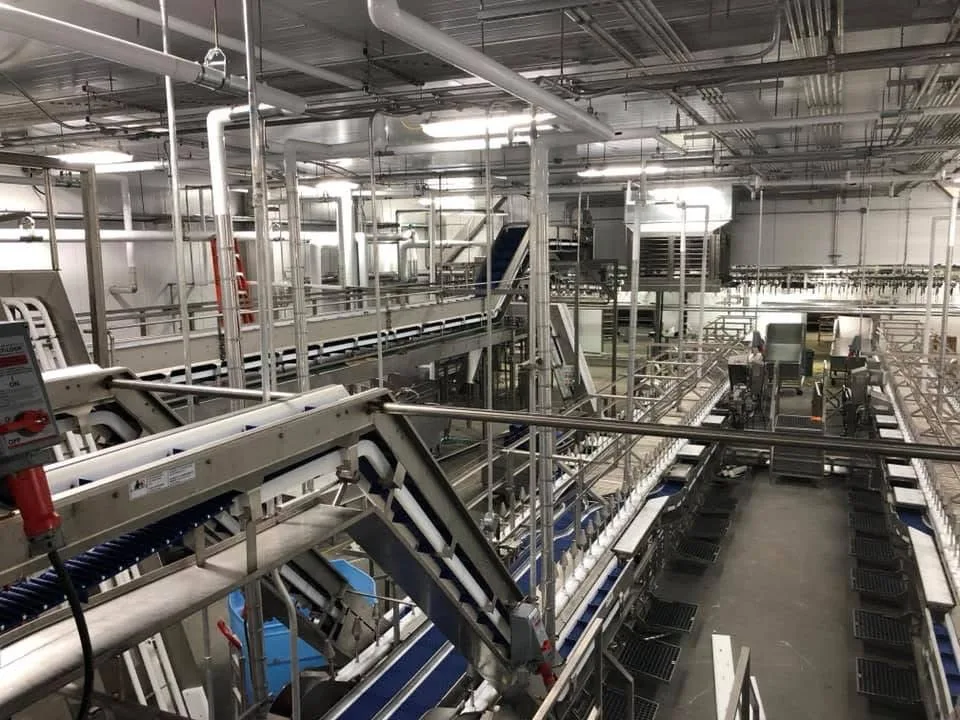
Part 8 of 10. A conveyor lasts 15–20 years; a lot of the Southeast's was installed in the 2000s. Retrofit, rebuild or replace — how to tell which one your line needs before it tells you.
Read post →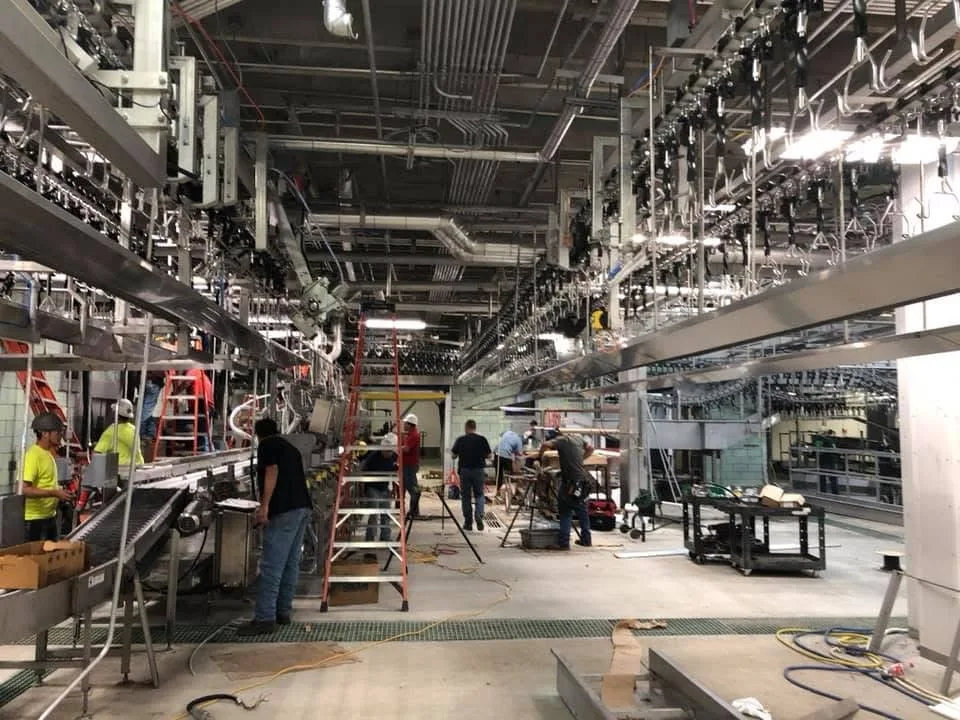
Part 9 of 10. A sanitary conveyor isn't a standard conveyor in stainless. Frame, belt, drives and layout all change when the line is washed down every night — what to look for.
Read post →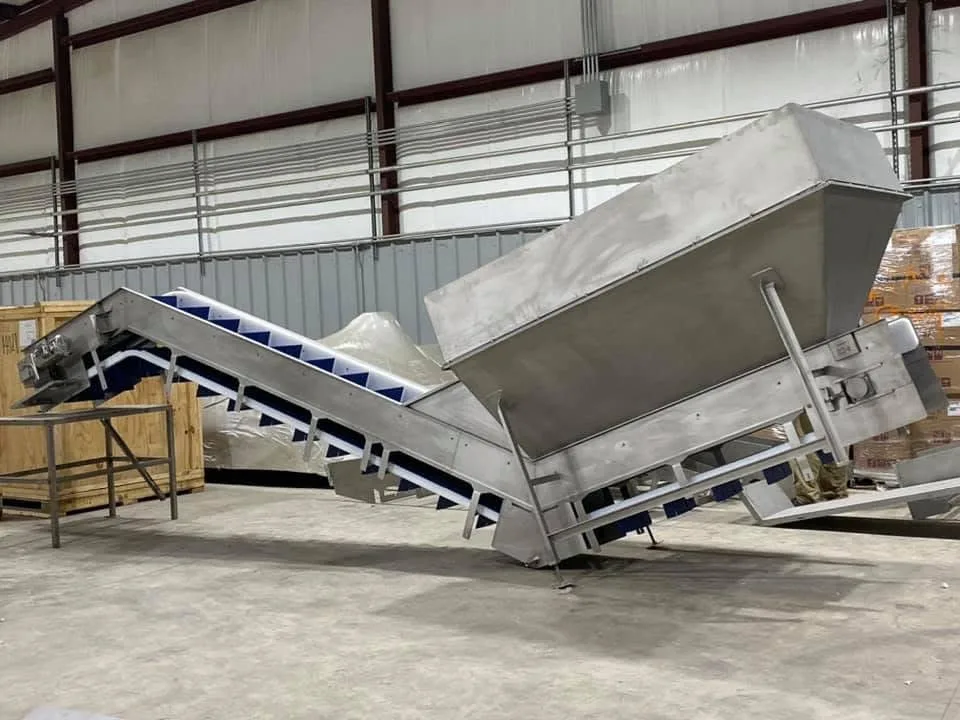
Part 10 of 10. You don't need drawings to start a conveyor project with us. What to send, how NDAs work, what a FabTek quote states, and who picks up the phone.
Read post →Part 7 of 7. Every plant, substation and data center is built from fabricated metal; the work can’t be offshored; and it anchors jobs where they were lost. Why the whole project runs through the shop floor.
Read post →
Part 1 of 5. White space, gray space, the generator yard and the on-site substation — a room-by-room tour of a hyperscale campus and the fabricated metal inside it.
Read post →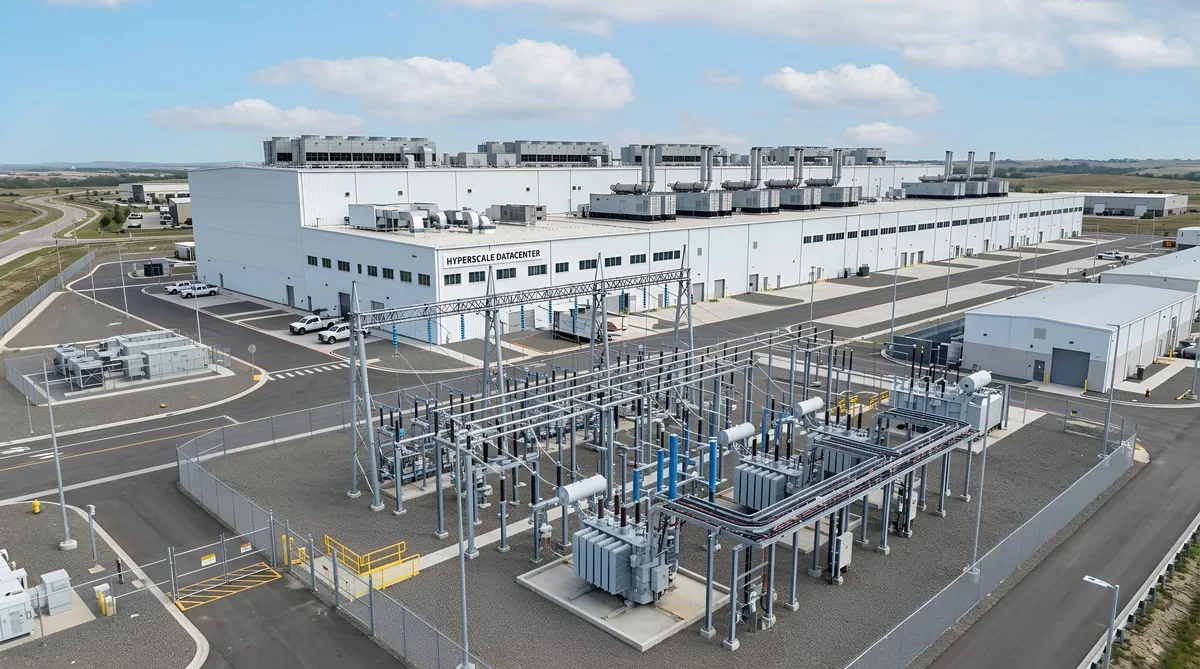
Part 2 of 5. Site selection, the interconnection queue, the transmission tap and the on-site substation — how hundreds of megawatts get from the grid to the property line.
Read post →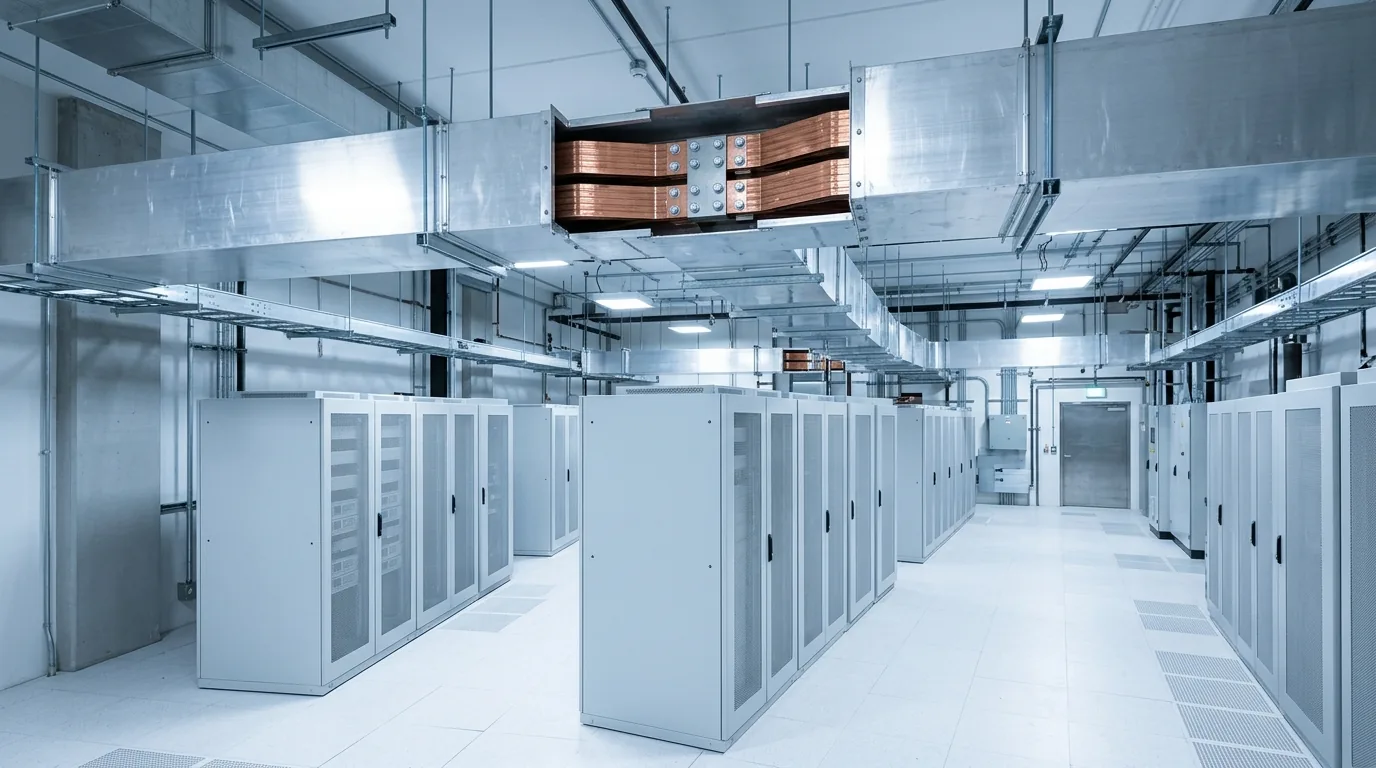
Part 3 of 5. The one-line diagram, explained: MV switchgear, unit substations, UPS, generators and bus duct — and why 2N redundancy doubles the enclosures.
Read post →Part 4 of 5. Interconnection queues, 2–4 year transformer lead times, switchgear and generator backlogs, skilled labor — and why fabricated steel is the piece you can actually control.
Read post →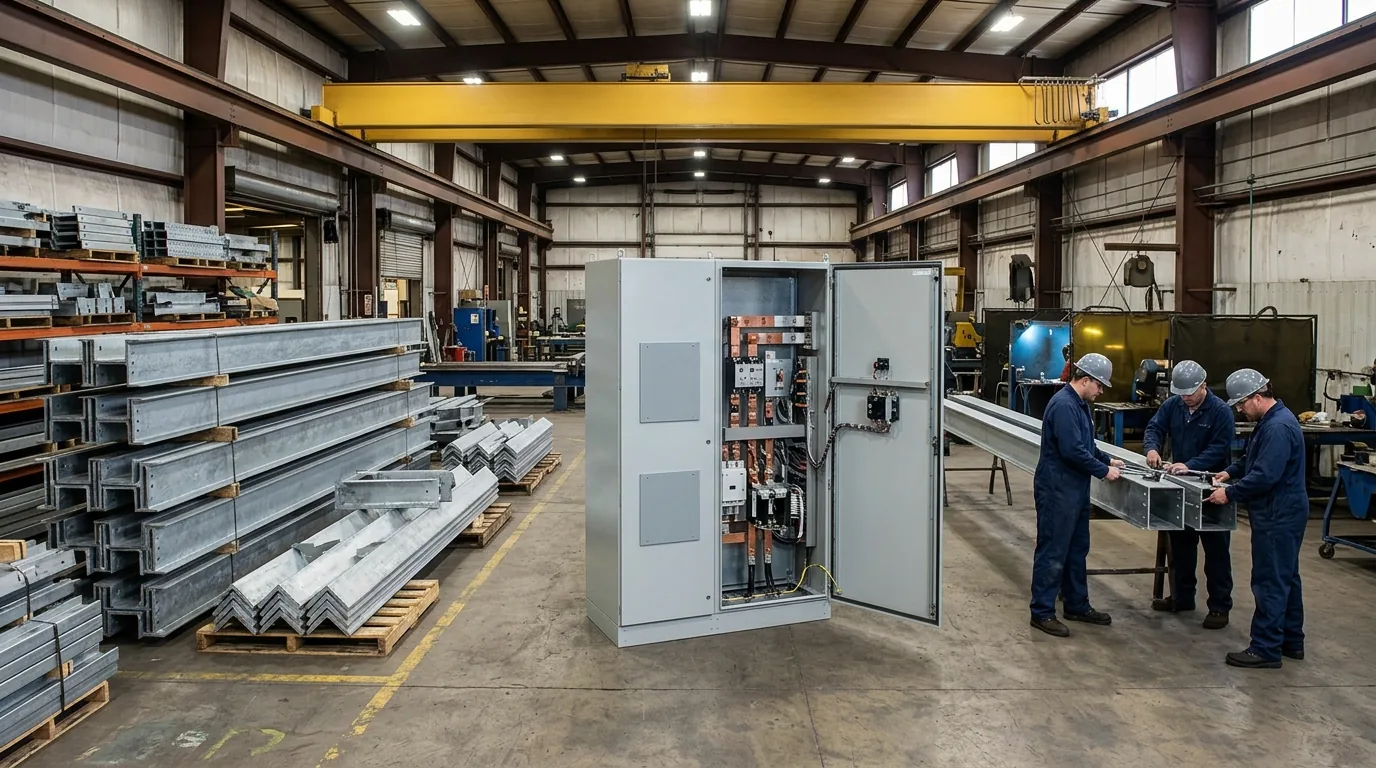
Part 5 of 5. What to spec, how to vet a fabricator, and how to lock capacity around your long-lead dates — with a 12-point RFQ checklist for enclosures, bus duct and steel.
Read post →Roughly $2B in new transformer plants won’t clear the backlog on their own — the binding constraint is a winding workforce that takes years to train.
Read post →More than $21B in capital investment landed in Mississippi in 2025, with multi-billion-dollar follow-ons in 2026 — the causes behind the pattern, from a fabricator that scaled inside it.
Read post →When mills stop negotiating and lead times hit multi-year highs, every one-off PO restarts the queue. What a committed agreement lets your fabricator do — on volume, schedule, staffing, capex, and quality.
Read post →Year-to-date data center starts hit $84.1B through July — nearly triple last year — while electrical supply chains delay half of all projects. How builders and fabricators keep schedules together.
Read post →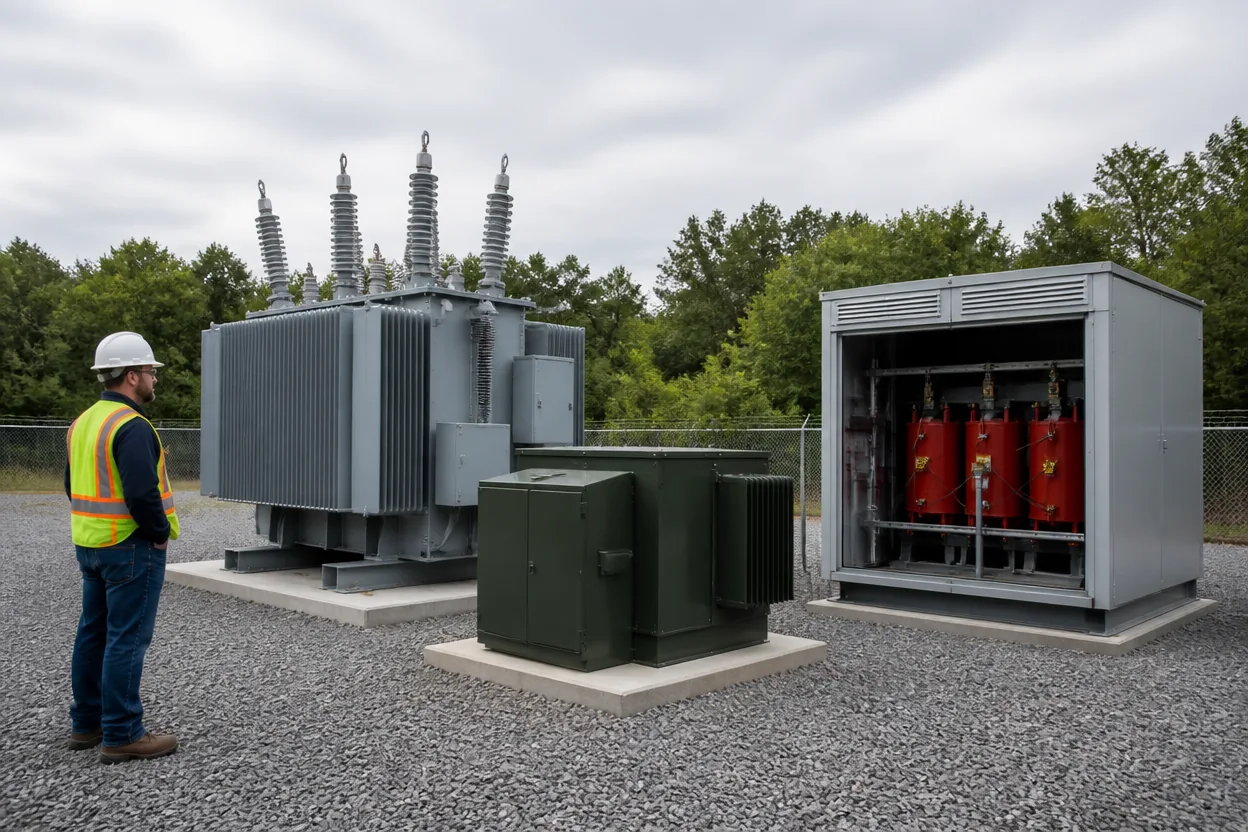
“The transformer shortage” isn’t one shortage — GSUs, substation units, distribution transformers, and regulators each stress a different part of the manufacturing chain.
Read post →Nearly everything in a substation yard stands on fabricated steel — and operators estimate 4,200–5,100 new or upgraded stations by 2035. The anatomy, piece by piece.
Read post →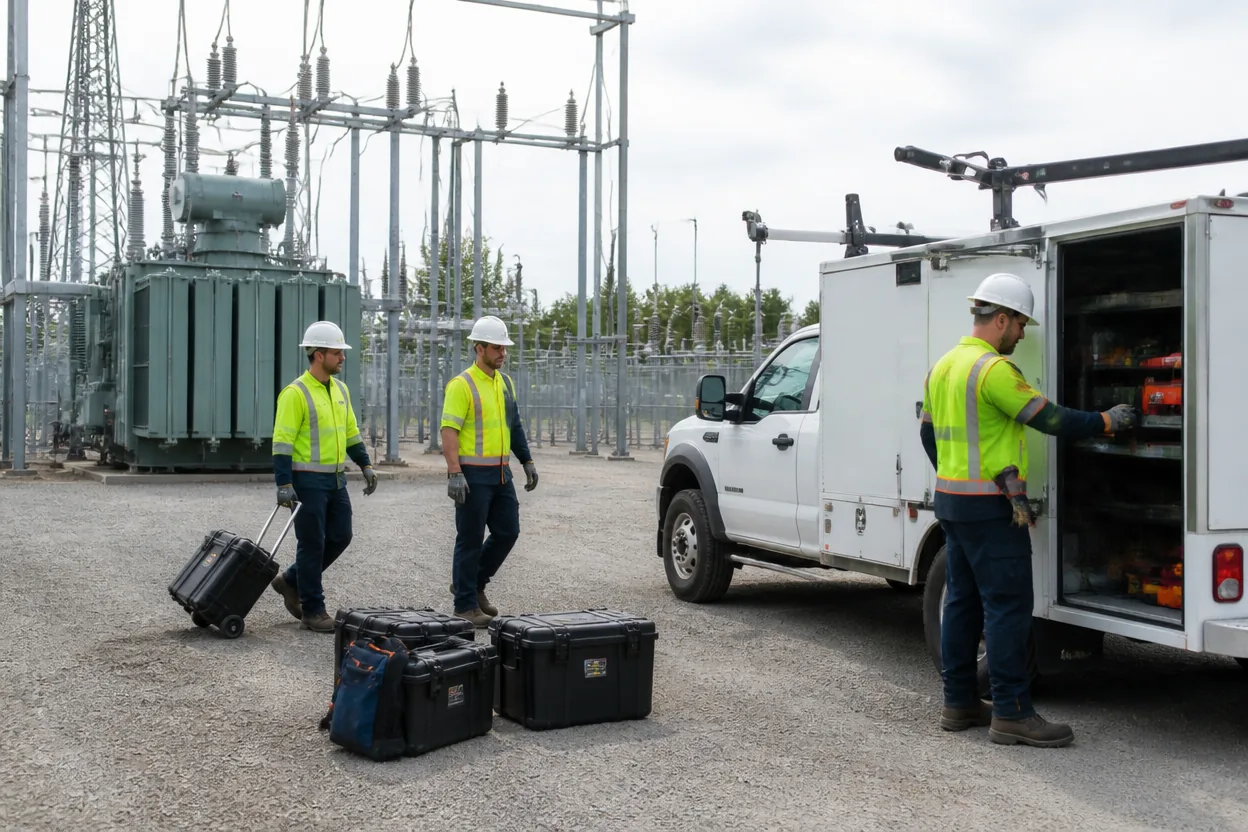
The industry spent three years managing equipment queues. The next constraint is the crews who install the equipment — and the projects adapting are moving field hours into the shop.
Read post →Factory construction reset to roughly triple its 2021 baseline, grid capex is headed past $1.4T, and the load is already contracted. Why this build-out runs a decade — supply-constrained the whole way.
Read post →The largest machine ever built, explained — how power travels from a distant plant to the outlet on your wall.
Read post →How a device with no moving parts changes voltage — and why the grid can't run without it.
Read post →
Follow a single electron from the power plant, across the grid, and into your wall — the whole journey.
Read post →
The fenced maze of steel and wires, explained — what a substation actually does and why it's so equipment-dense.
Read post →What actually causes a blackout, how the grid protects itself in milliseconds, and why the lights sometimes just flicker.
Read post →
Why a transformer that once took months now takes years — the materials, the demand, and the import problem.
Read post →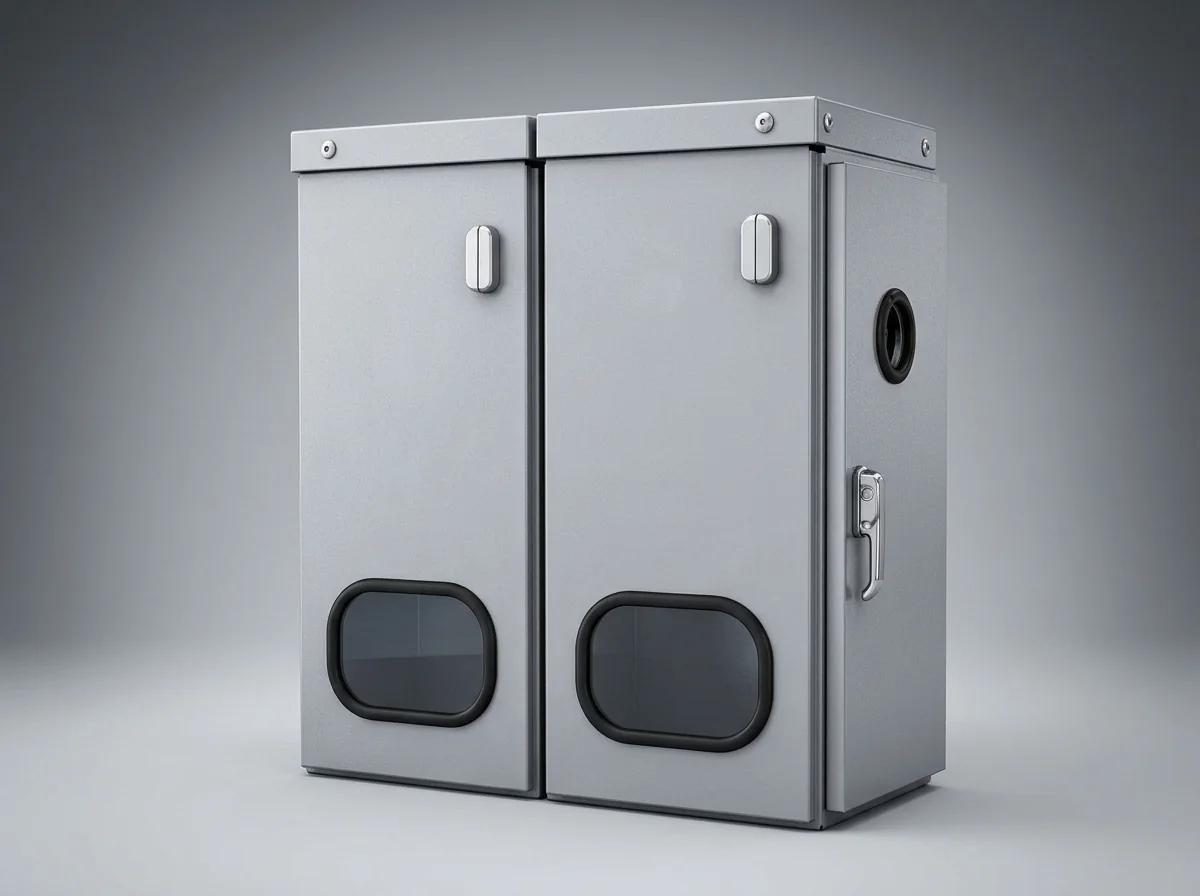
How to choose the right enclosure rating — 3R vs. 4 vs. 4X — plus gauge, finish, and gasketing to confirm before you order.
Read post →
A single campus can draw as much power as a small city — here's how it gets from the grid to the server rack.
Read post →How domestic fabrication reduces supply-chain risk — lead time, tariff exposure, and continuity — and what Built in the U.S.A. buys you.
Read post →The grid build-out has reached Mississippi — a $25 billion wave of hyperscale datacenter investment and a major grid upgrade are reshaping our own backyard.
Read post →When a utility partner asked if we could absorb their datacenter bus duct demand, we said yes — and had a dedicated line running in weeks, not months.
Read post →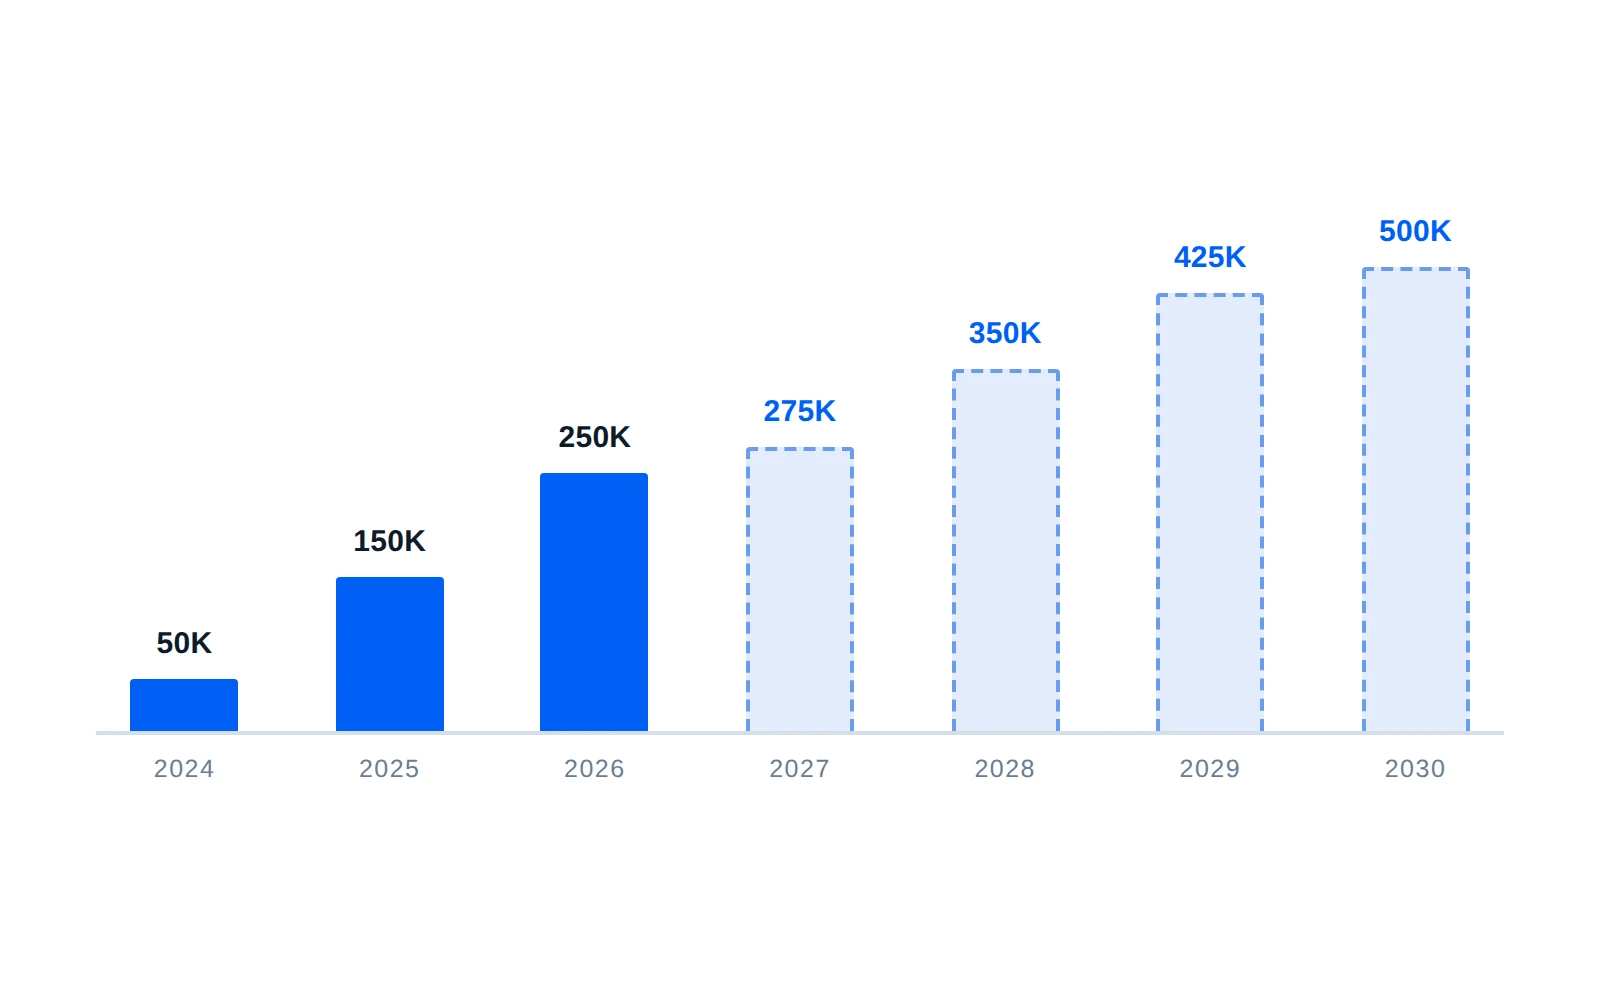
Our production footprint has more than tripled since 2024 — over 400K sq ft across four Mississippi sites today, with 500K targeted by 2030. Capacity, added ahead of the grid's curve.
Read post →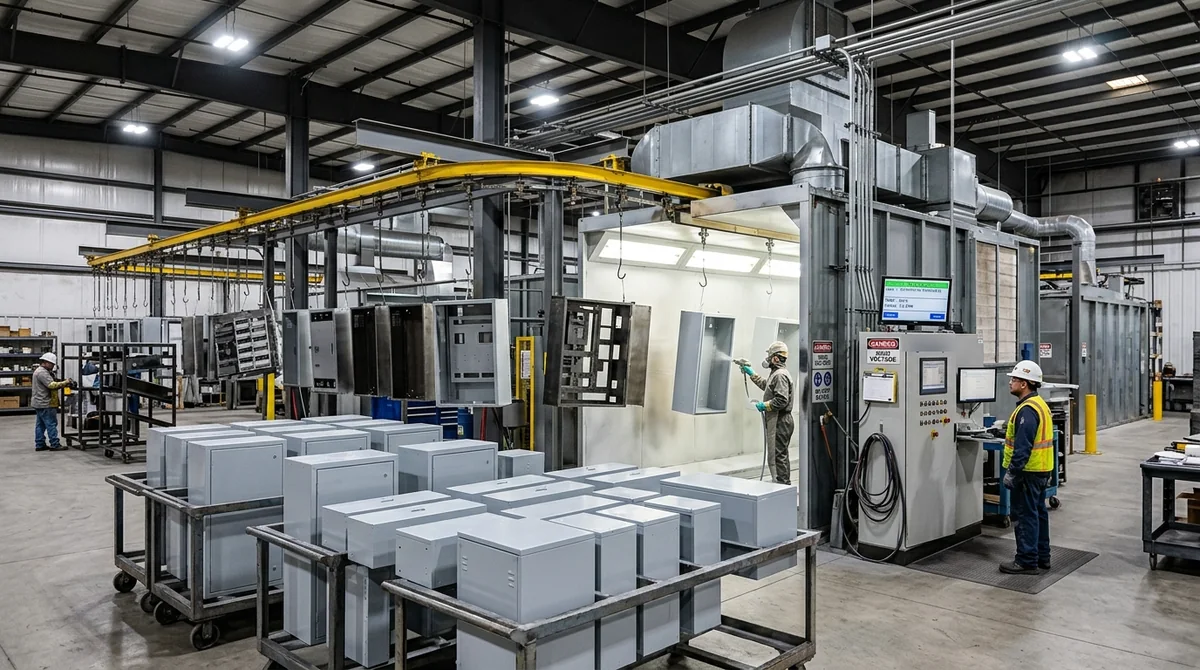
A 10-point due-diligence checklist for vetting a fabricator — capabilities, certifications, capacity, traceability, and lead-time reliability.
Read post →Specifying switchgear enclosures for hyperscale datacenter builds — rating, gauge and finish, thermal and access, and lead time.
Read post →How to write a build-to-print spec package that avoids rework — drawings, tolerances, materials, finish, and acceptance criteria.
Read post →What datacenter EPCs should confirm when sourcing bus ducts — ampacity and spec, lead time, surge capacity, and single-source coordination.
Read post →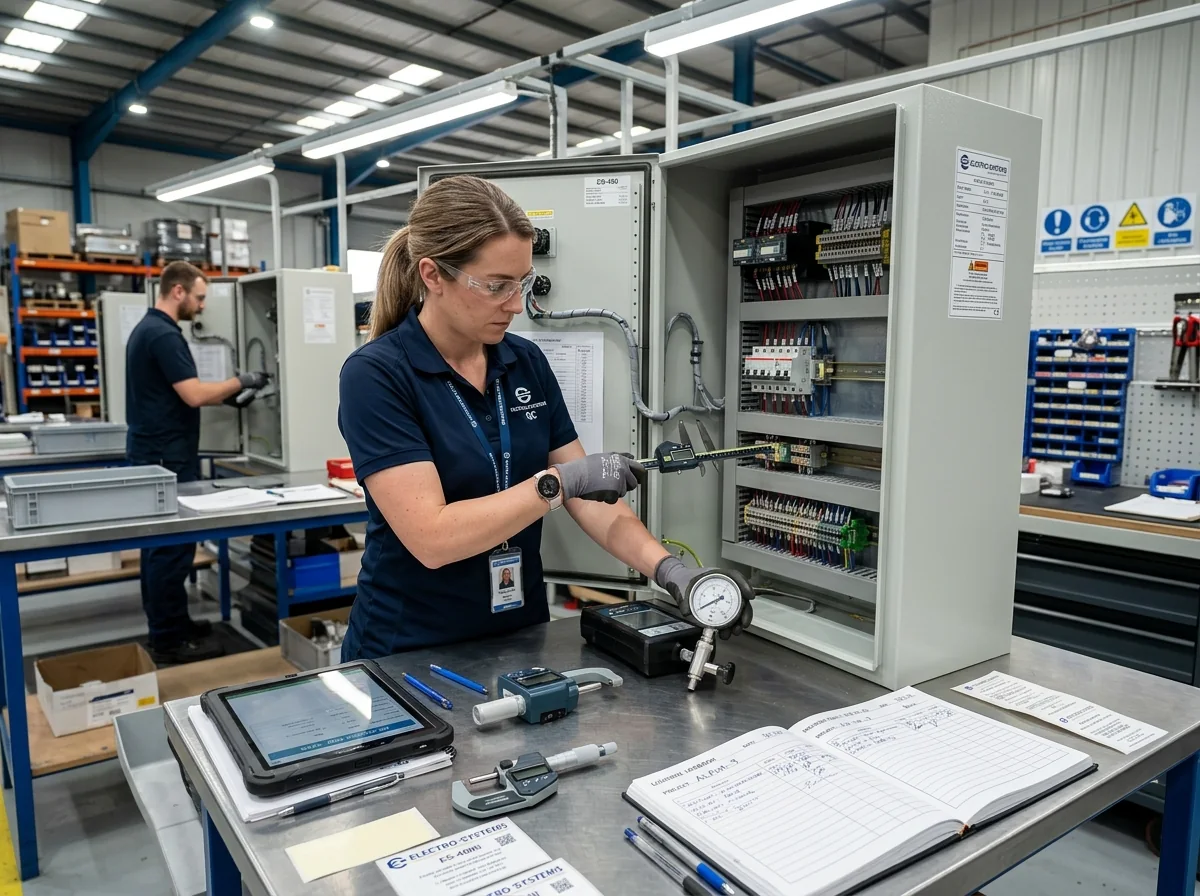
Why hyperscale EPCs benefit from single-source fabrication — bus ducts, enclosures, and structures with the electrical build under one roof.
Read post →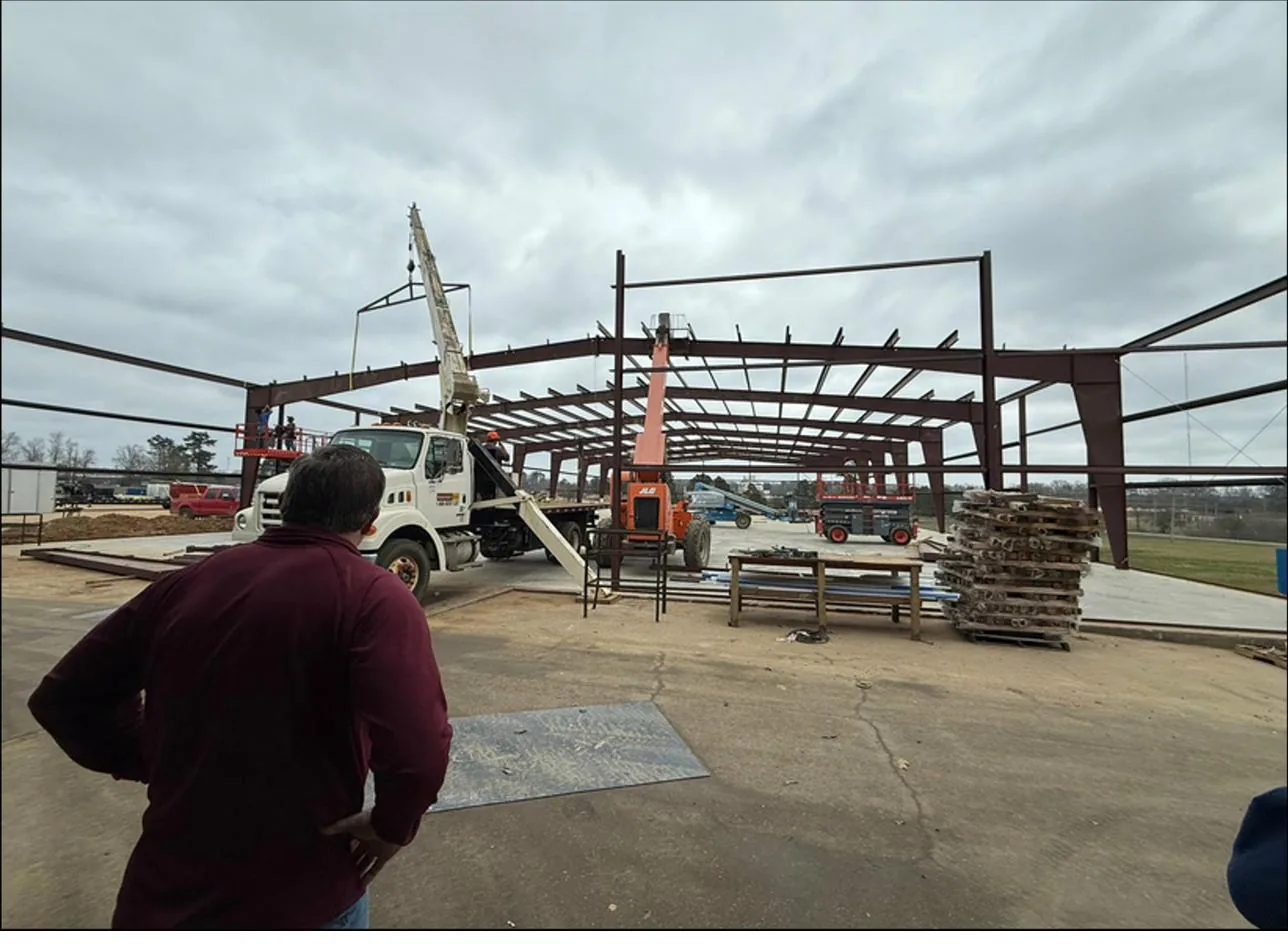
Capacity added ahead of demand — a 50K sq ft expansion on the path to 400K sq ft across four Mississippi production sites in 2026, with 500K sq ft targeted by 2030.
Read post →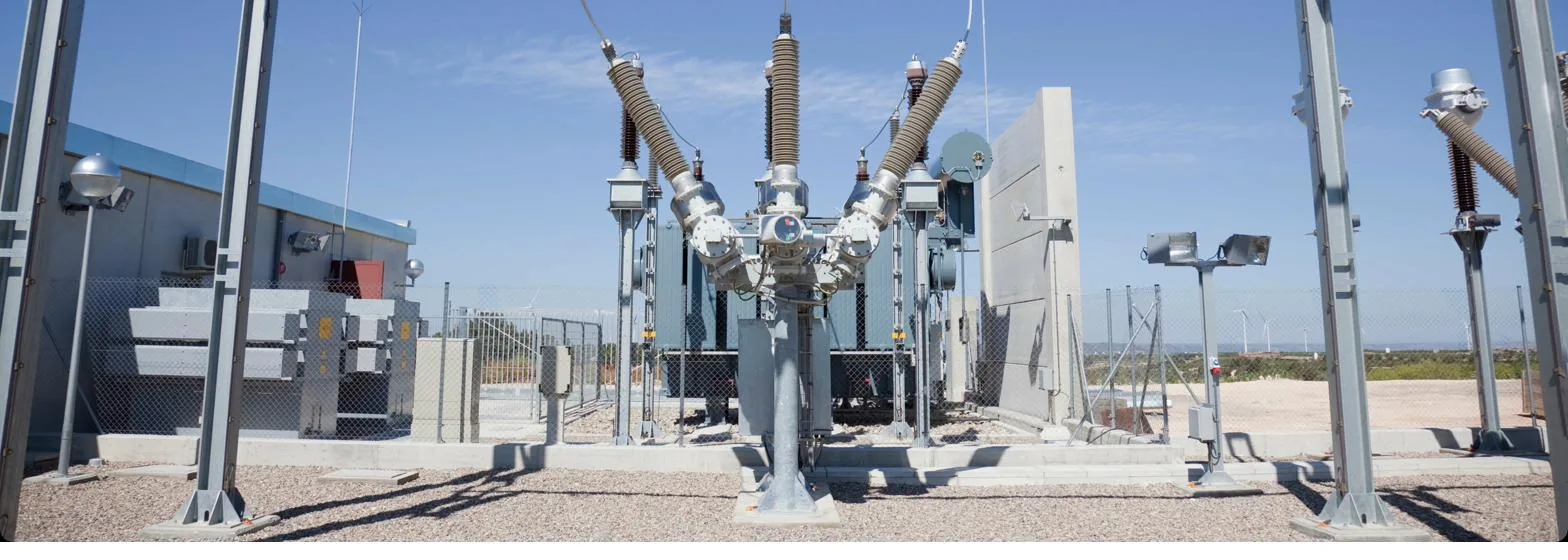
What to confirm before you award a substation steel package — drawings, galvanizing, certifications, lead time, and shipping.
Read post →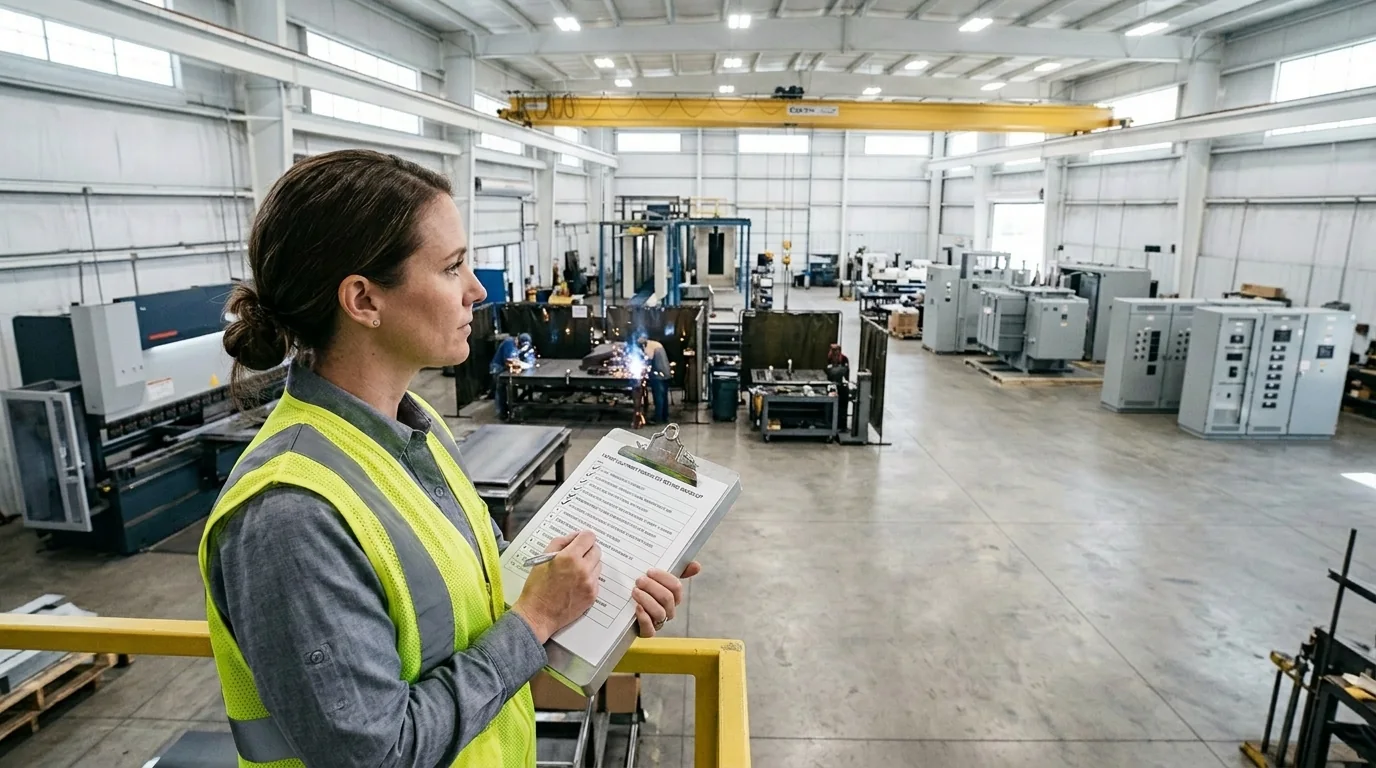
How to vet a fabricator's surge capacity — shifts, backup equipment, overflow, and continuity — without sacrificing quality.
Read post →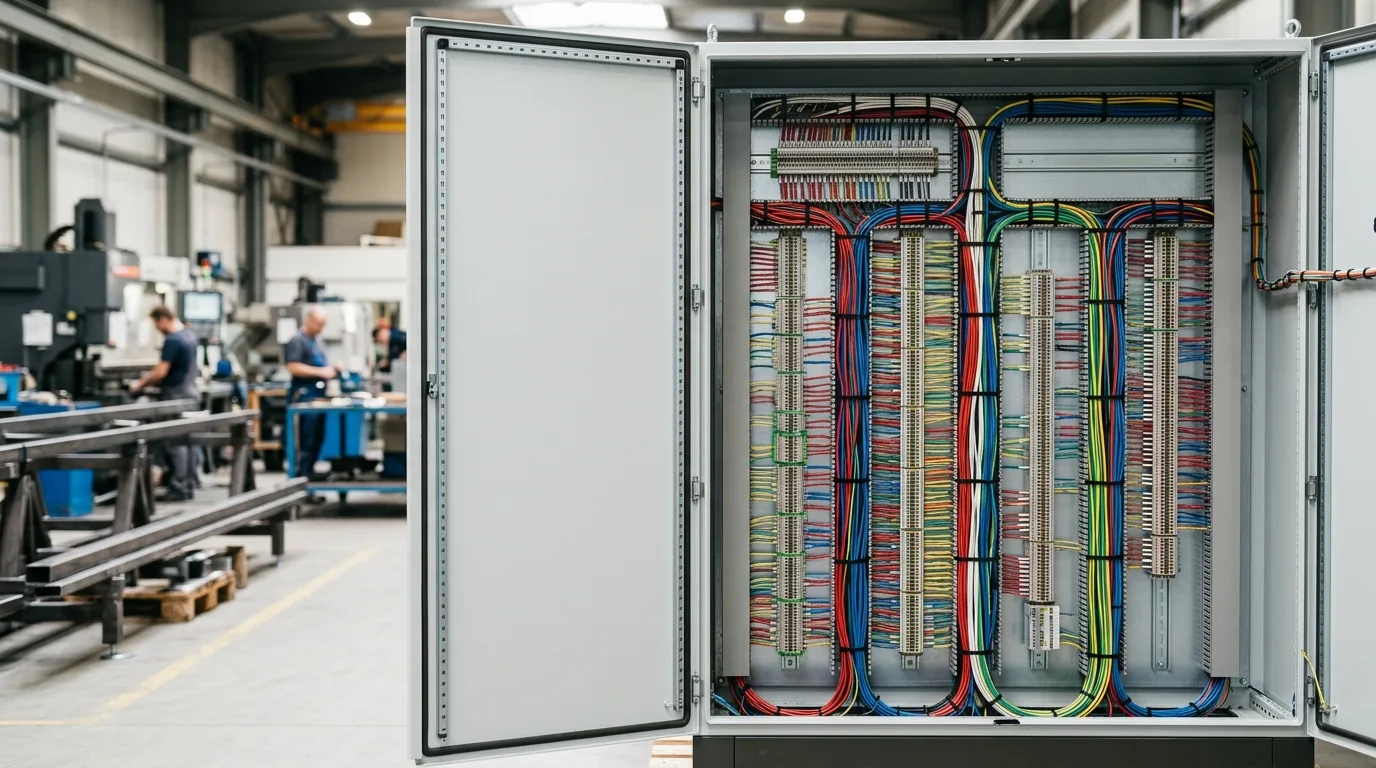
FabTek now wires out what it builds — components mounted, harnesses run, and cabinets fully assembled to your drawings under our ISO 9001:2015 system. A tested, pre-wired deliverable instead of split-vendor coordination.
Read post →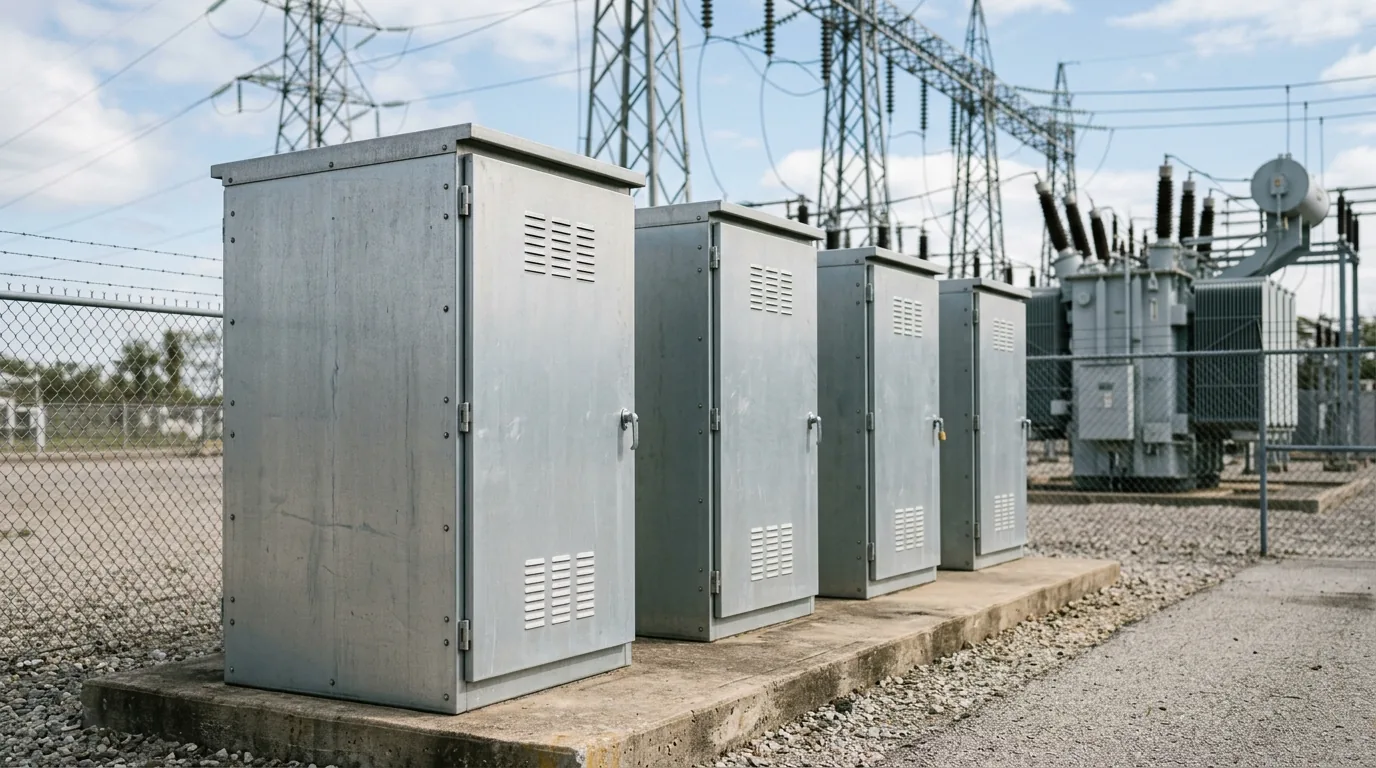
A utility buyer's guide to awarding steel fabrication — capabilities, certifications, finish coordination, capacity, and documentation.
Read post →A buyer's guide to specifying substation support structures — dead-end vs. A-frame, galvanizing, lead time, and what to confirm before you award the package.
Read post →A deep dive on NEMA 3R, 4, and 4X — what each protects against, where each fits, and how to avoid over- or under-speccing.
Read post →Electricity is made and used in the same instant — how operators keep supply and demand matched, second by second.
Read post →
We're proud to partner with Industrial Steel Company (ISC) — pairing their heavy-structural expertise in substation frames, dead-end and A-frame structures, and transmission steel with FabTek's transformer and electrical build for a single source across the metal and the make.
Read post →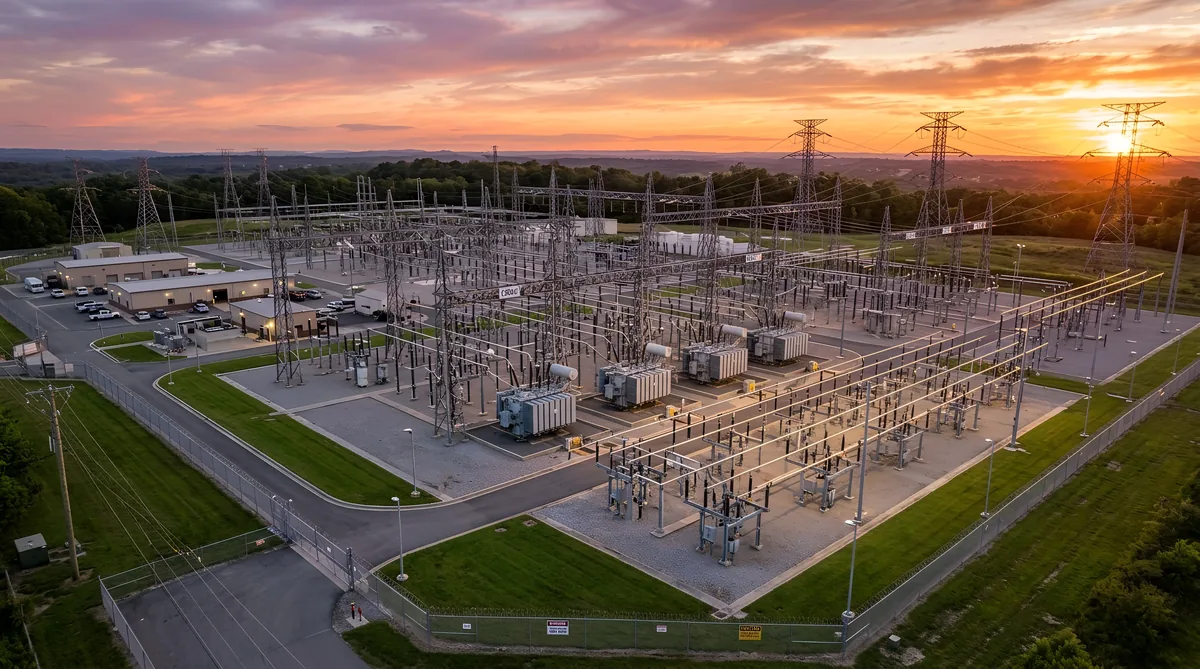
Tubular vs. lattice transmission structures — right-of-way, load, cost, and lead time, and what actually drives the choice.
Read post →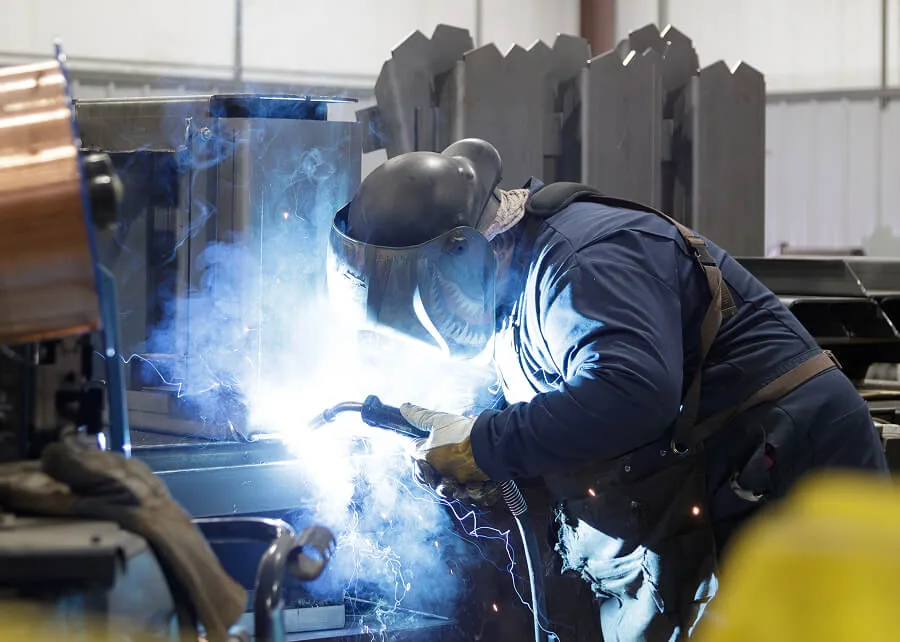
What ISO 9001:2015 and AWS-certified welding really mean — what they guarantee, what they don't, and what records to ask for.
Read post →Hot-dip galvanizing vs. paint and powder coat for substation steel — corrosion protection, life-cycle cost, and when to specify each.
Read post →Single-source — metal and electrical under one roof — removes the vendor handoffs where power-equipment schedules slip.
Read post →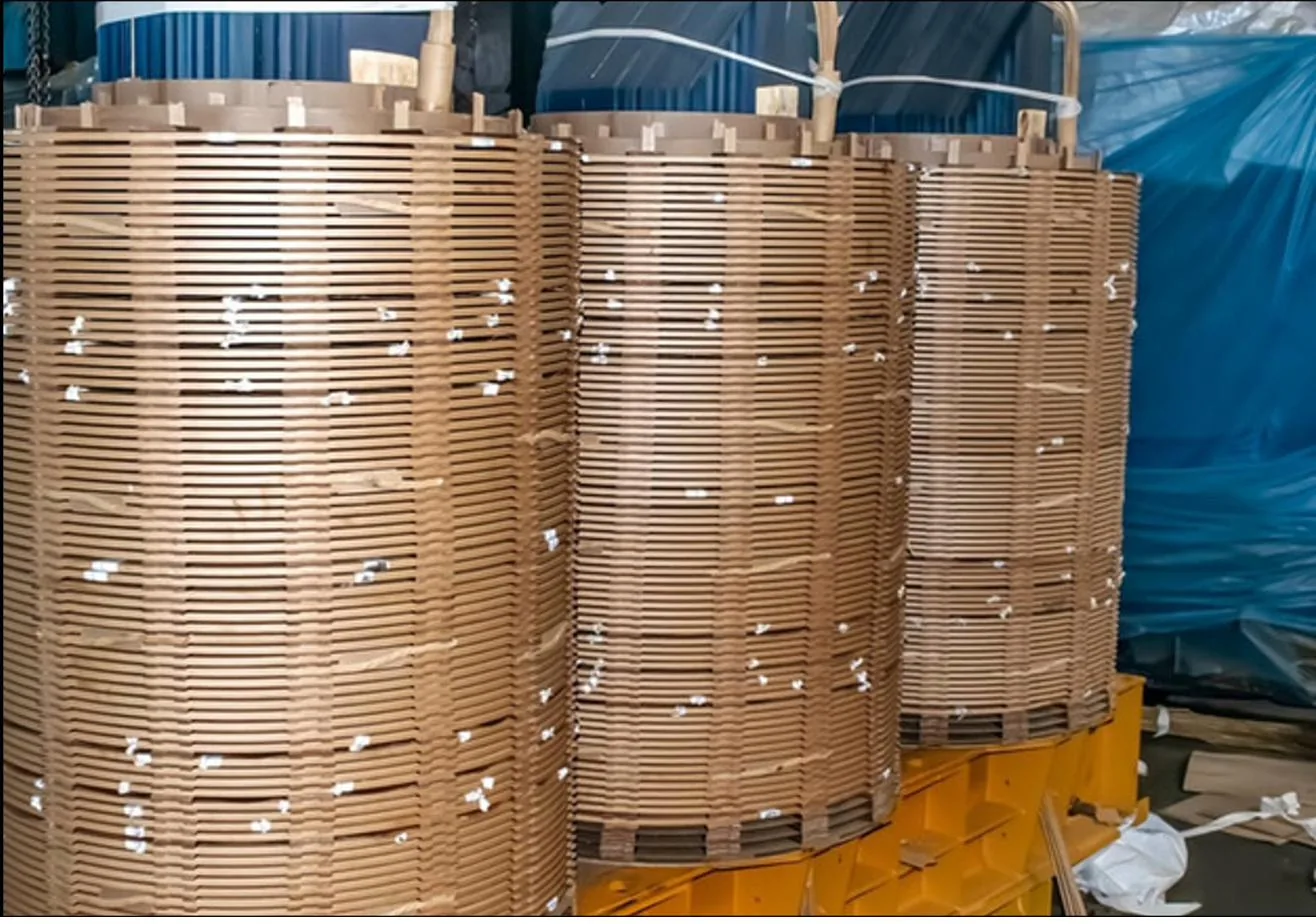
When to outsource transformer coil winding — capacity, quality systems, and the single-source advantage of pairing windings with metal.
Read post →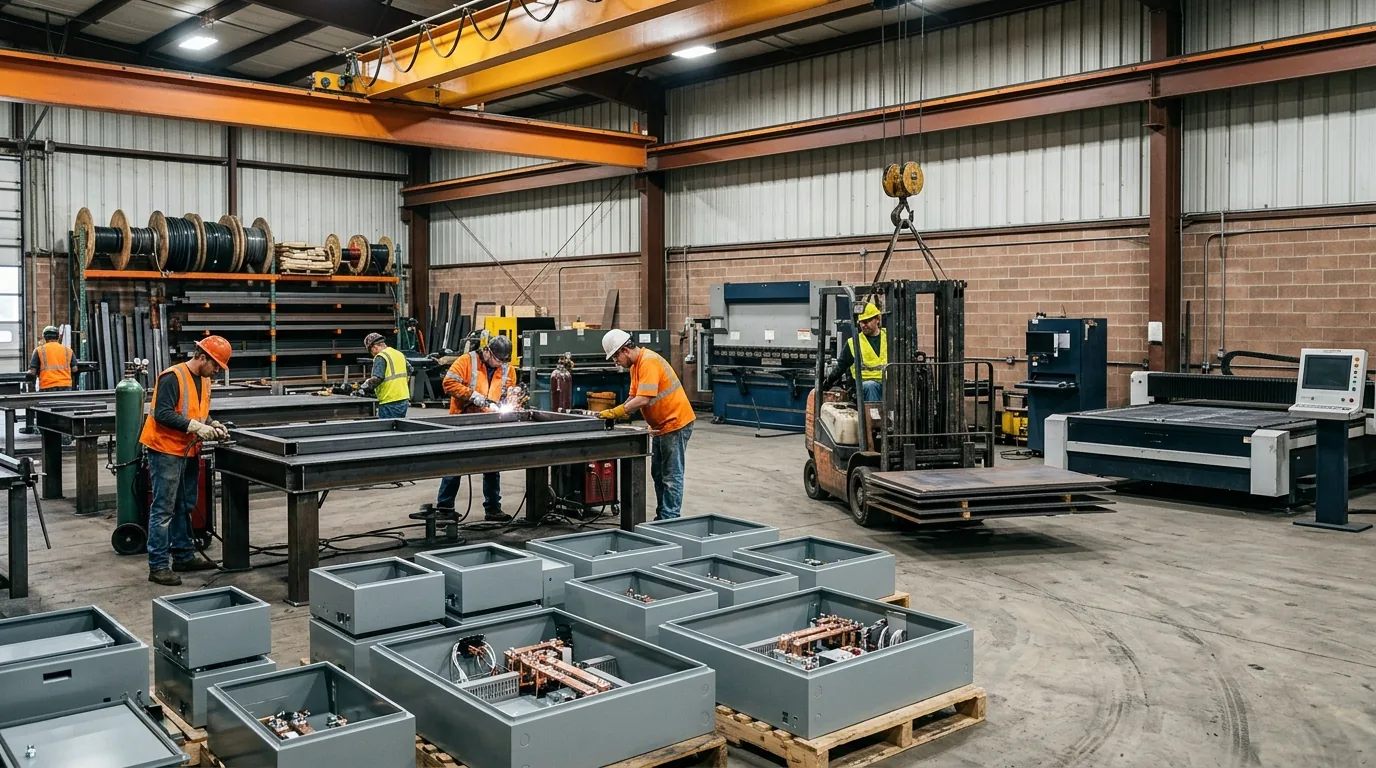
AI and hyperscale growth are stretching power-equipment lead times — how datacenter demand reshapes schedules, and how to protect your dates.
Read post →Welded vs. bolted transformer tanks — sealing, lead time, repairability, and cost, and how to choose for your application.
Read post →Follow us on LinkedIn or reach out directly — we post project milestones, facility expansions, and industry events.
Send us a spec or give us a call. We'll respond fast.