Capabilities
Plate Plasma & Torch Cutting
A 10-foot by 20-foot Hornet water-table CNC plasma with oxy-fuel torch for heavy plate — base plates, gussets, transformer tank walls and covers, cut to print and moved straight to fit-up.
A 10-foot by 20-foot Hornet water-table CNC plasma with oxy-fuel torch for heavy plate — base plates, gussets, transformer tank walls and covers, cut to print and moved straight to fit-up.
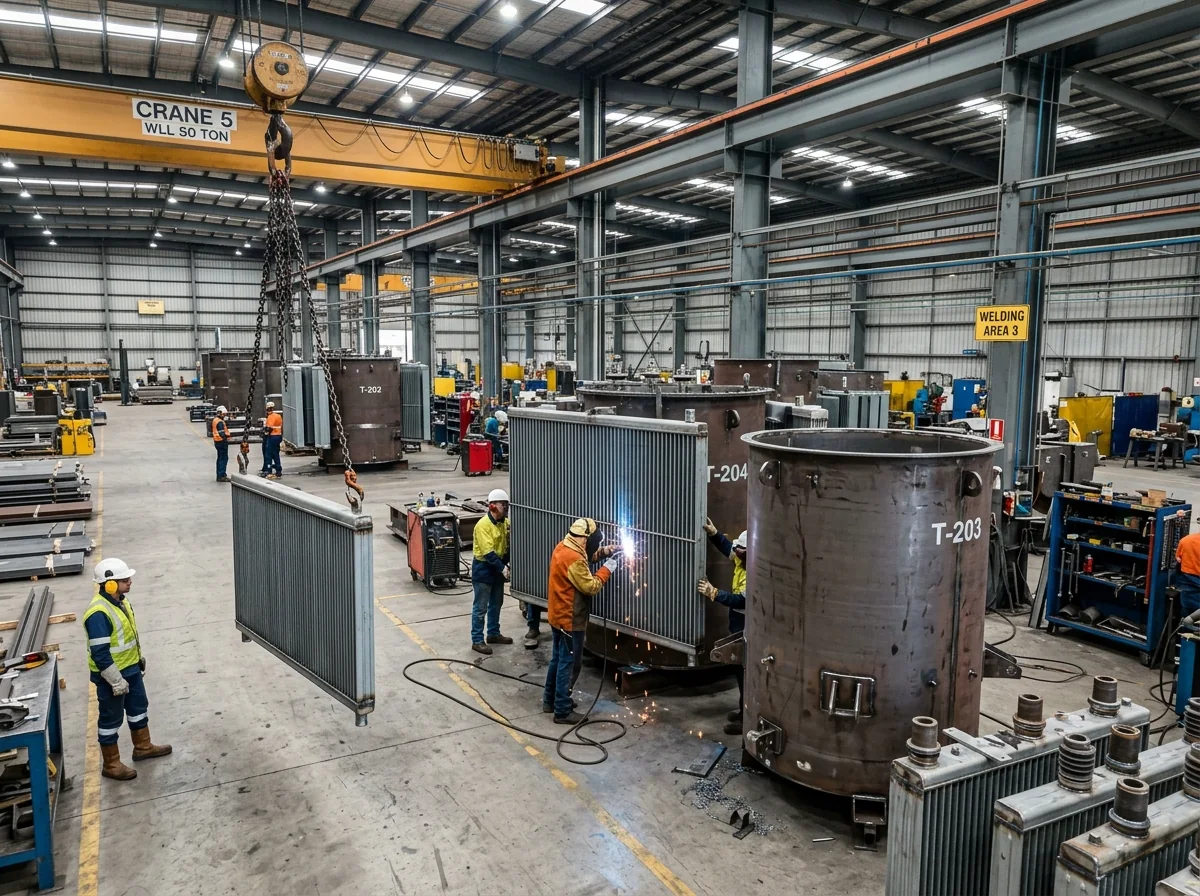
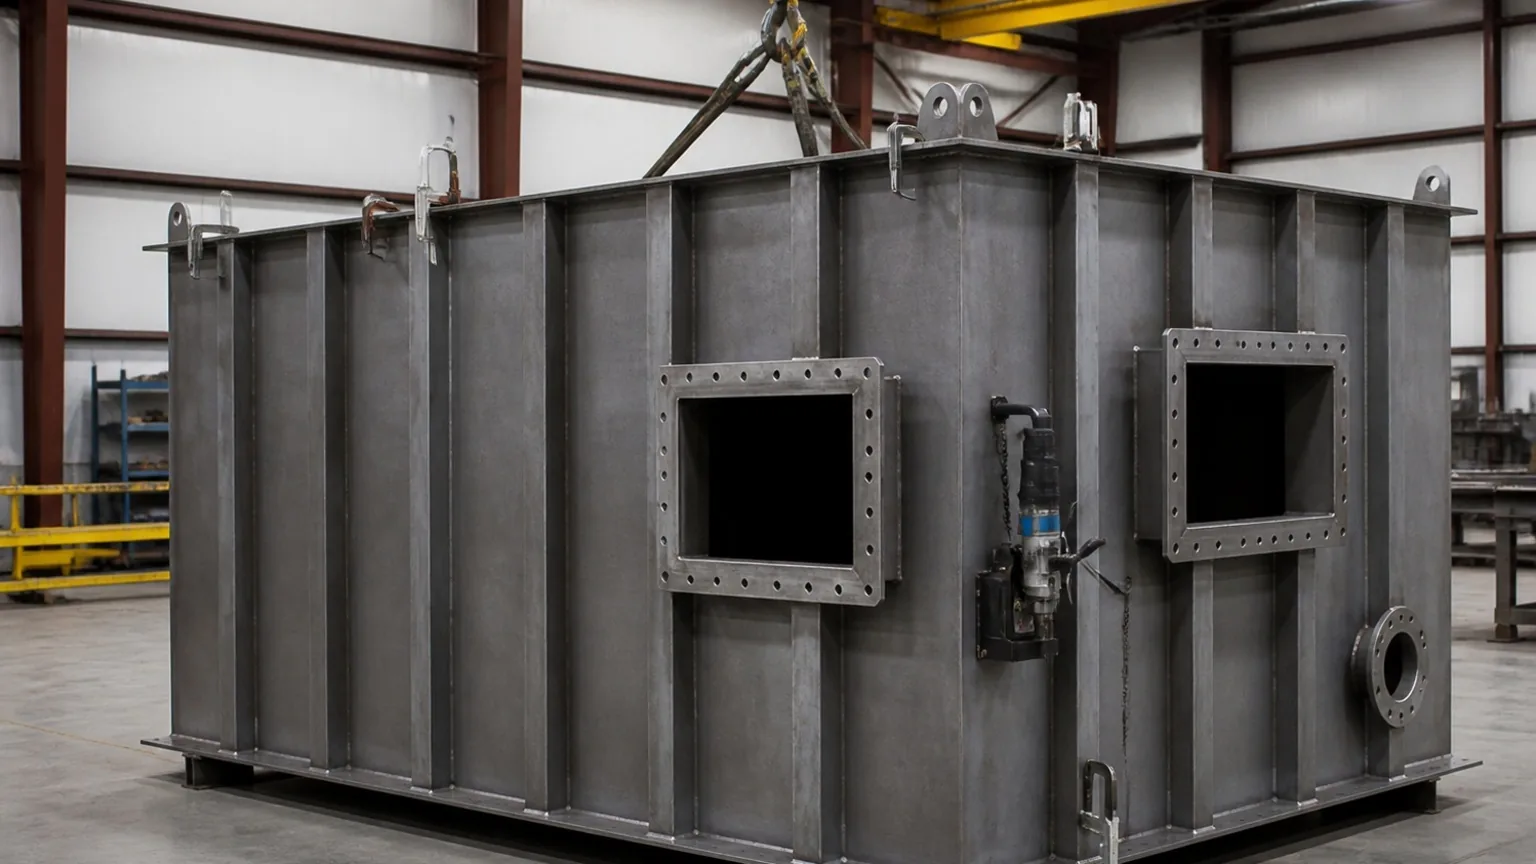
Plate work in power-system fabrication is big: transformer tank walls and covers, base plates for dead-end structures and poles, gussets and stiffeners, skid bases and lifting lugs. It needs a table large enough to take a full plate and a process fast enough to keep a structural or tank line fed. FabTek's Hornet CNC plasma has a 120" × 240" water table, so a standard plate goes on whole and is nested edge to edge, and an oxy-fuel torch on the same gantry takes the thicknesses beyond plasma range.
The water table holds fumes and warpage down on heavy cuts, and the CNC programs come from the same engineering group that details the tank or the structure, so plate parts arrive at fit-up with holes, bevels and marks already in place. Plasma-cut plate feeds the welding cells and the plate rolls; parts that can't tolerate a heat-affected zone move to the waterjet instead.
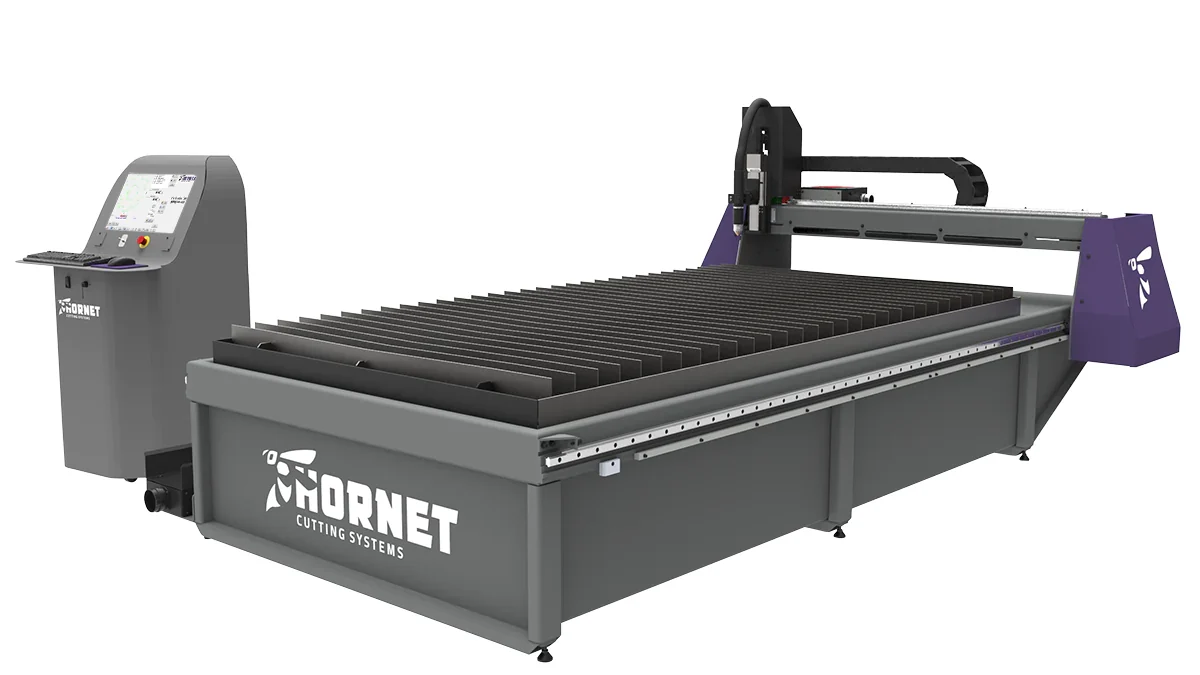
Plate for power, pad-mount and round tank bodies, covers and conservator ends.
For dead-end structures, equipment stands, tubular poles and platform columns, with bolt patterns cut in the program.
Connection gussets, tank stiffeners, lifting lugs and jacking pads.
Skid base plates, drip pans, checker plate decking and kick plates.
Weld-prep bevels cut on the table for full-penetration tank and structural welds.
Plate blanks and profiles shipped to customers who weld and finish in their own plants.
Tank walls, covers, base plates and gussets nested to use the full plate.
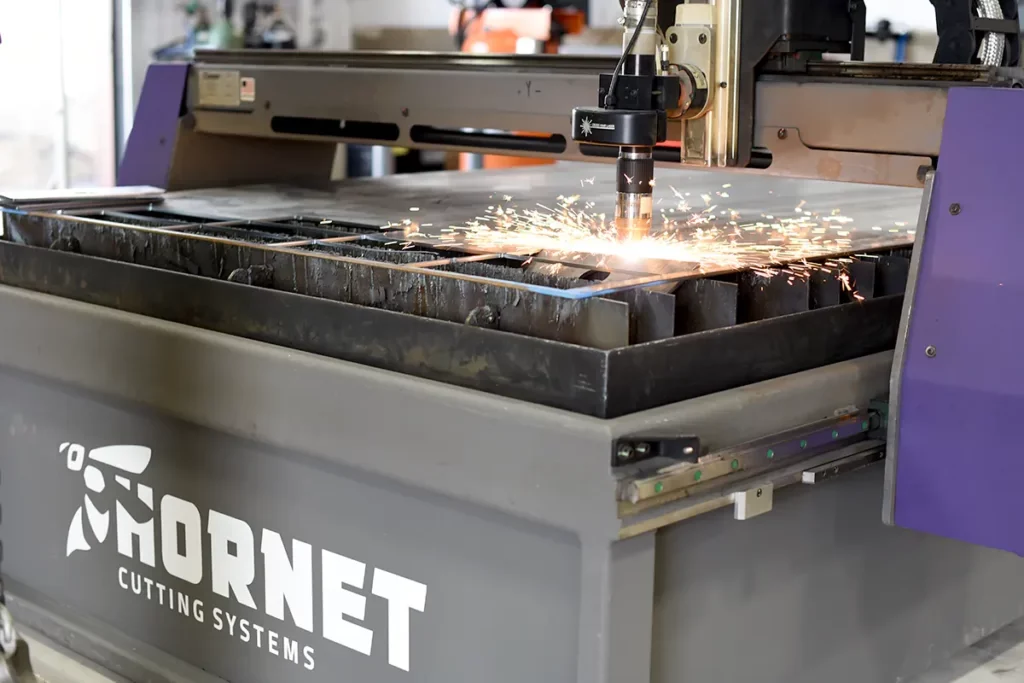
Plasma for the run of plate work; oxy-fuel torch for the heaviest sections.
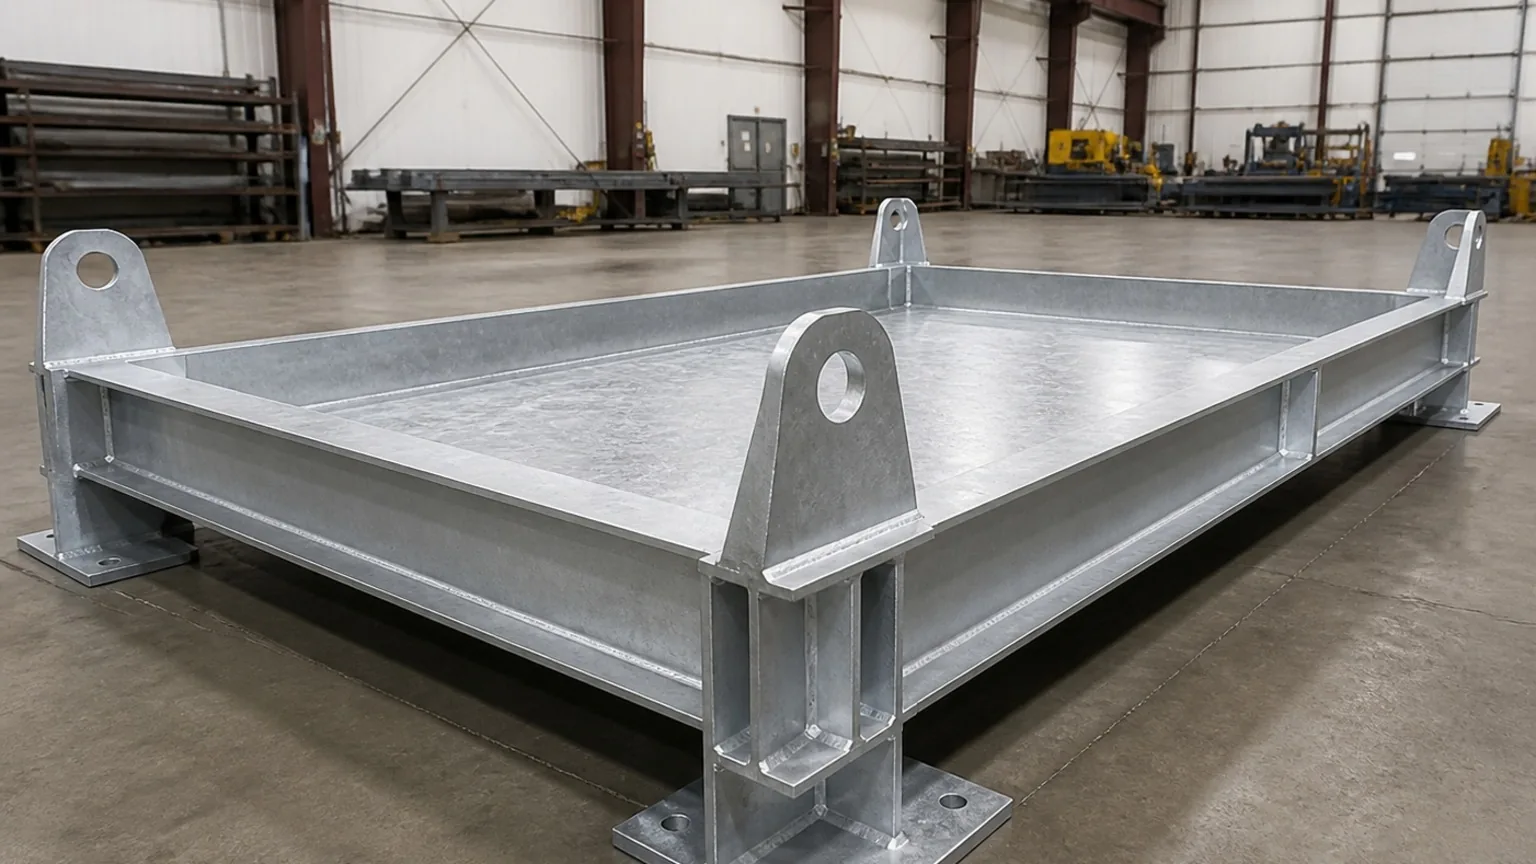
Weld preps and layout marks cut in the same program.
Plate parts move to fit-up by tank or structure number.
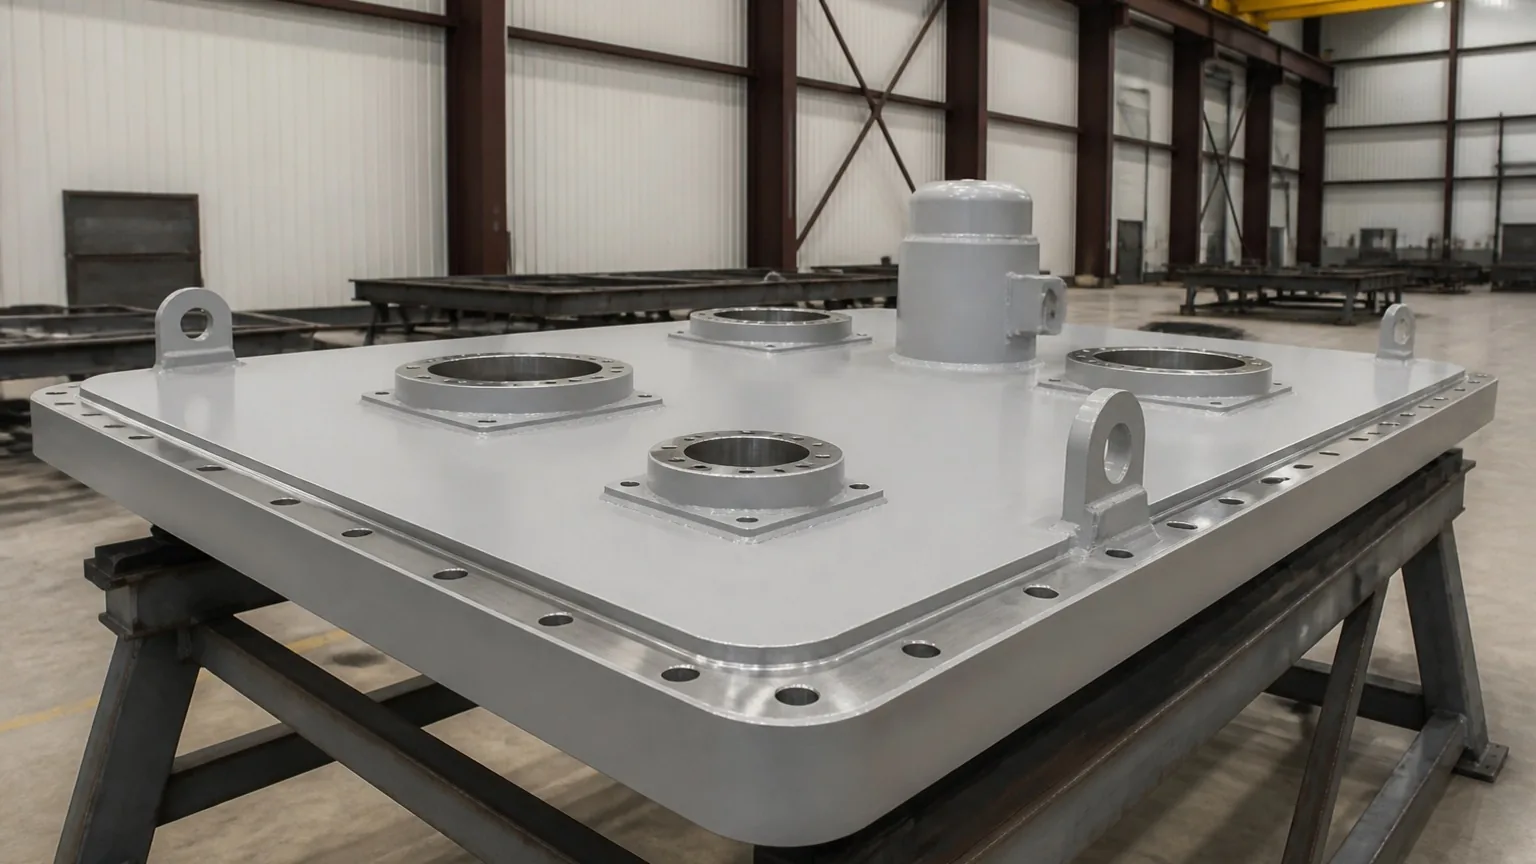
Transformer tanks and their covers, conservators and radiator headers; substation and transmission base plates; equipment skid bases and platform steel; bus duct flanges and heavy brackets. The same table cuts one-off repair plate for rebuild shops and repeat plate parts for OEM tank programs.
| Machine | Hornet CNC plasma with oxy-fuel torch, 120" × 240" water table |
|---|---|
| Materials | Carbon steel plate; stainless and aluminum by plasma; heavy carbon plate by oxy-fuel |
| Operations | Profiles, holes and slots, bevels, part marking; nested from full plate |
| Programming | From FabTek engineering's shop details; DXF, DWG and STEP accepted |
| Downstream | Plate rolling, fit-up and welding, blast and powder coat on site |
| Traceability | Plate heat numbers carried to each part; ISO 9001:2015 |
| Also specified as | Plasma cutting services, CNC plasma cutting, plate cutting services, oxy-fuel cutting, heavy plate cutting, steel plate profiles |
Representative capabilities — exact ranges, ratings, and finishes are confirmed per project. Send drawings for a firm quote.
A tank wall cut a sixteenth long shows up as a flange that won't seal. Plasma plate parts at FabTek are cut from the same shop details the fitters work to, checked at the table, and moved to fit-up on carts marked by tank number, so the plate that reaches the welder is the plate the drawing shows. For plate parts with tight flange patterns — covers, headers, base plates that meet a machined surface — the pattern is cut on the table and finished on the drill line or in machining where the tolerance calls for it.
Built at four production sites in Hazlehurst, Mississippi.
ISO 9001:2015 quality management, AWS-certified welding, OSHA-compliant facilities.
In-house powder coat backed by an IEEE 2000-hour salt-spray certification.
Reserved-line capacity and the automation to grow with your volume.
The Hornet table is 120" × 240", so a full 10' × 20' plate goes on whole and parts are nested across it.
FabTek Industries cuts plate on a 10' × 20' water-table CNC plasma with oxy-fuel at its Hazlehurst, Mississippi plants, and fabricates the tanks, structures and skids the plate goes into.
Plasma for carbon plate where a small heat-affected zone is acceptable and speed matters; waterjet for stainless, aluminum, thick sections and parts where heat distortion or edge hardening can't be tolerated. We'll recommend the process from the drawing.
Yes. Weld-prep bevels are cut on the table in the same program as the profile.
Explore related lines: Transformer tanks · Power transformer tanks · Dead-end & A-frame structures · Equipment skids & platforms
Further reading: Welded vs. bolted transformer tanks · AWS D1.1 vs D1.3 vs D1.6 · Material certs and heat-number traceability







Have plate to cut? Send the drawings and quantities — we'll come back with a process, a price and a date, typically within one business day.