Built in the U.S.A.
Hazlehurst, MS·Call 601.892.5017·ISO 9001:2015
Overview

Code welding is a different discipline, and we run it as one.

Structural welding and pipe welding share an arc and nothing else. Pipe welding runs on qualified procedures (WPS), qualified welders (WPQ), joint-by-joint traceability and a test at the end that either passes or does not. FabTek runs a dedicated pipe welding program at our Hazlehurst, Mississippi plants under ASME Section IX, fabricating carbon and stainless pipe to ASME B31.1 and B31.3, hydrotesting to the specification, and shipping a record with every spool, manifold and skid.

Pipe Welding & Pressure Testing at FabTek Industries
How It Runs

From isometric to test record.

  1. 01

    Review

    Isometrics, piping spec and inspection plan reviewed; WPS matched to material, size and service; field-joint plan confirmed with the contractor.

  2. 02

    Cut & bevel

    Pipe cut and beveled on saw and plasma; fittings and flanges verified against the spec and certs.

  3. 03

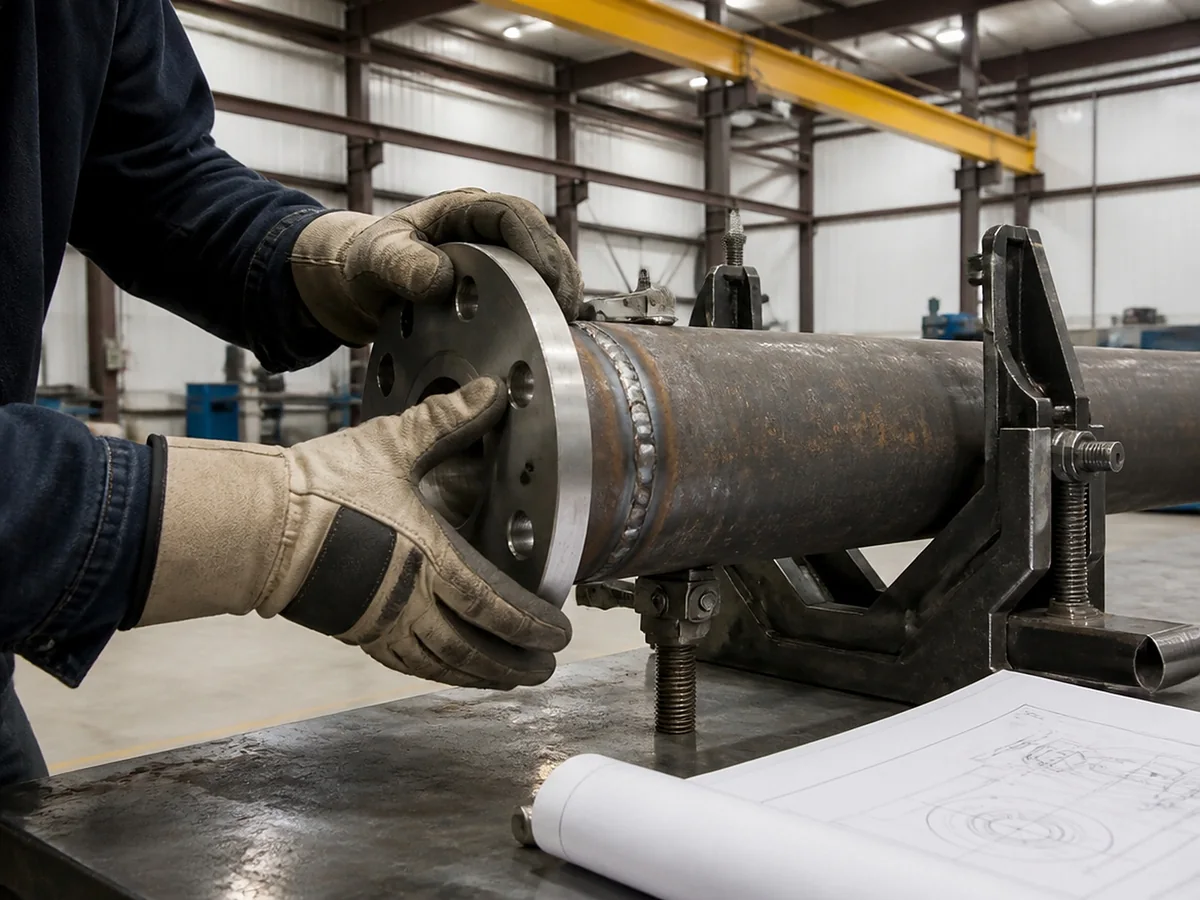
    Fit-up

    Spools fitted on tables and positioners, alignment and root gap checked, tacked and marked by the fitter.

  4. 04

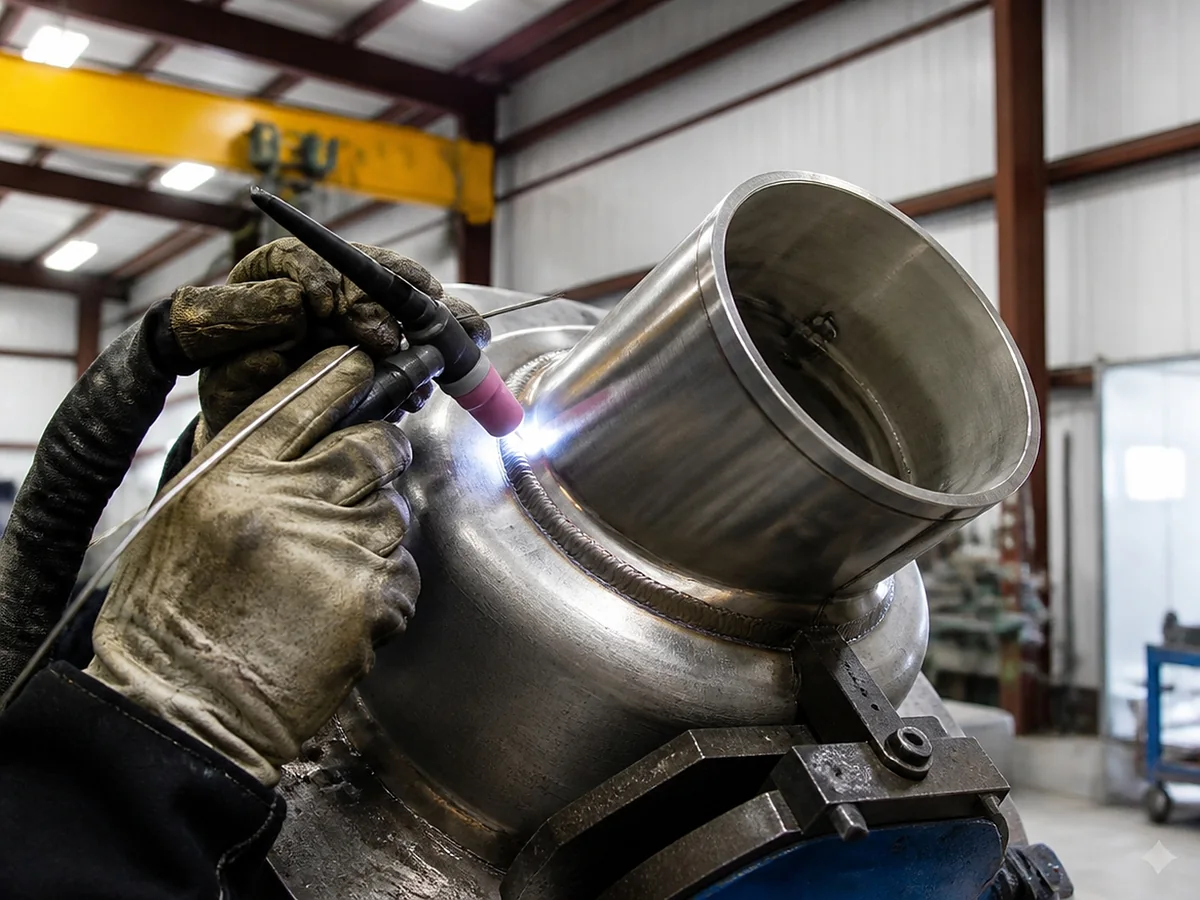
    Weld

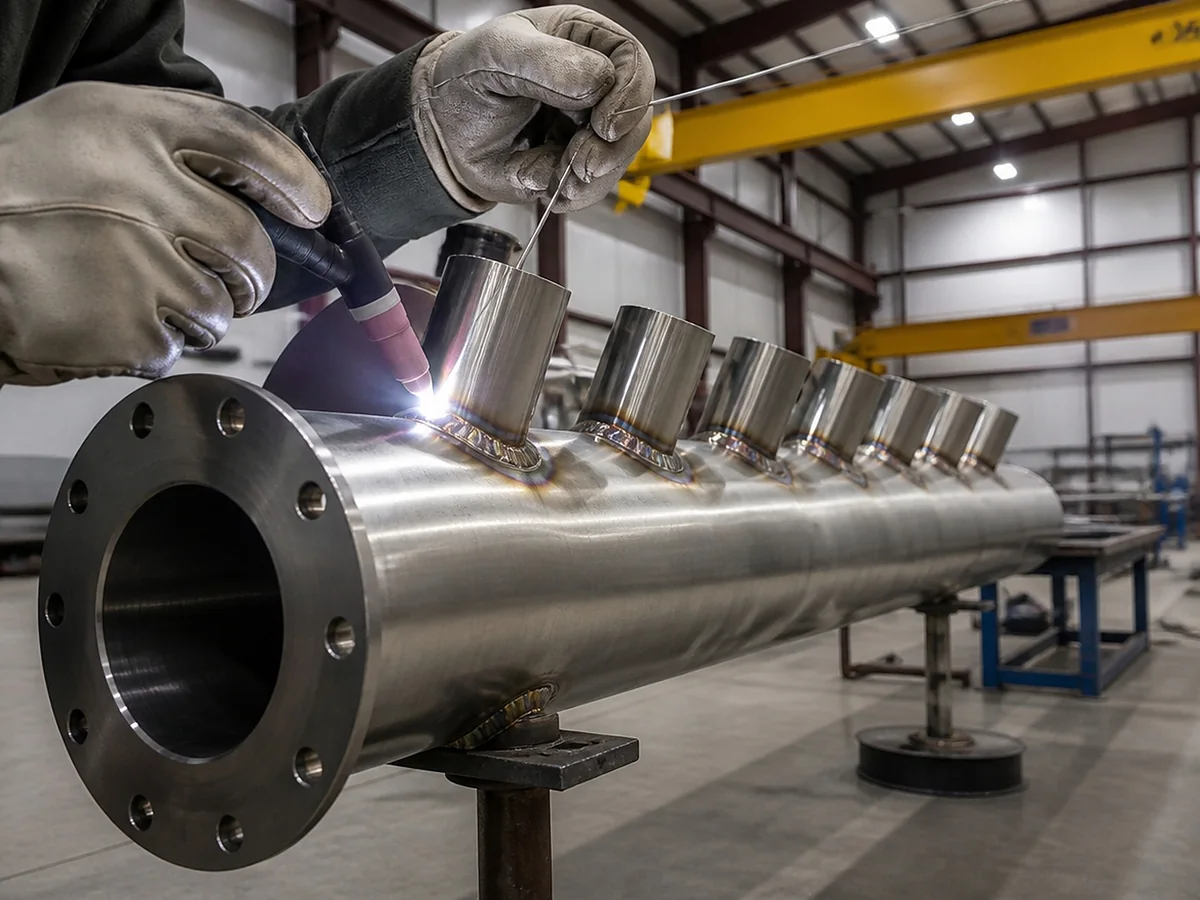
    GTAW root with GMAW, FCAW or SMAW fill and cap, or full GTAW on stainless and small-bore; each joint logged to the welder's ID.

  5. 05

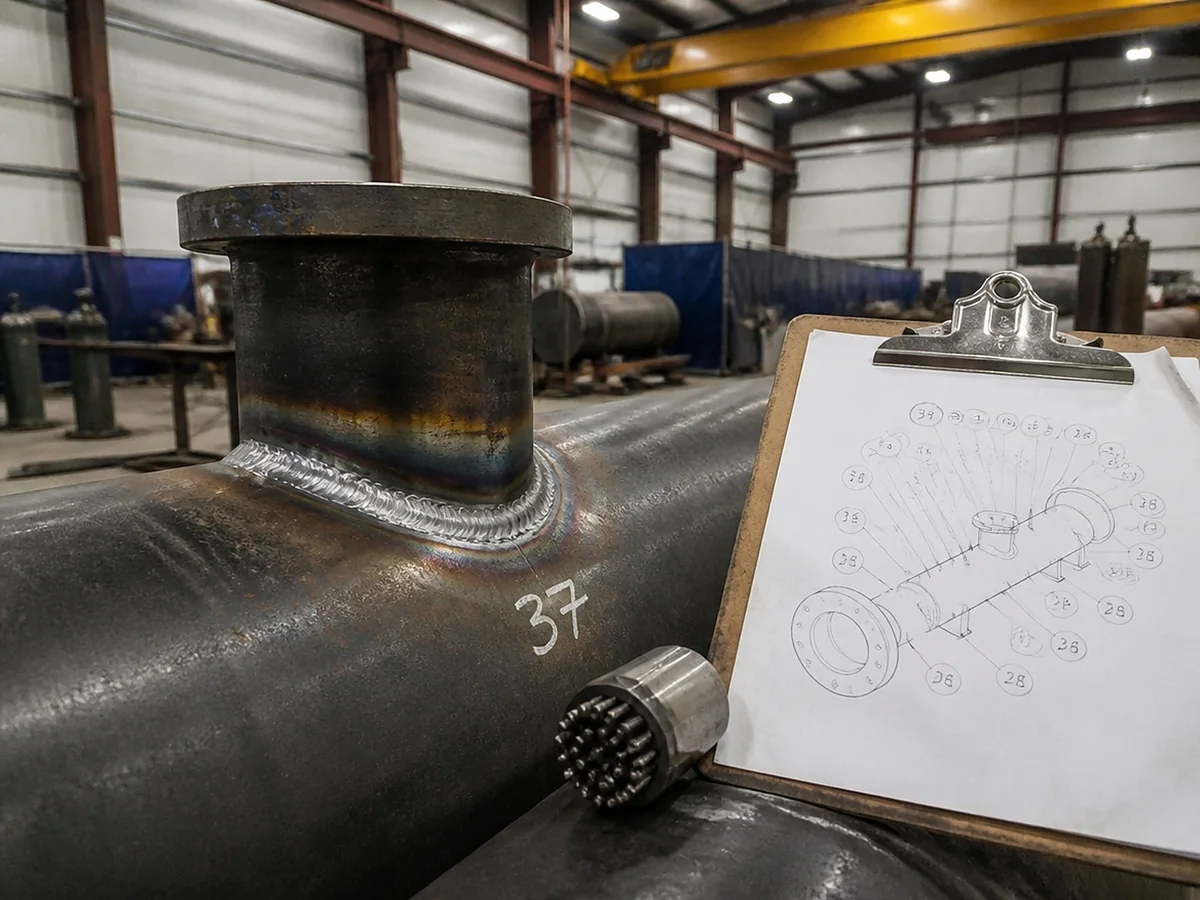
    Inspect

    Visual inspection on every joint; PT, RT or UT per the inspection plan through our NDE partners.

  6. 06

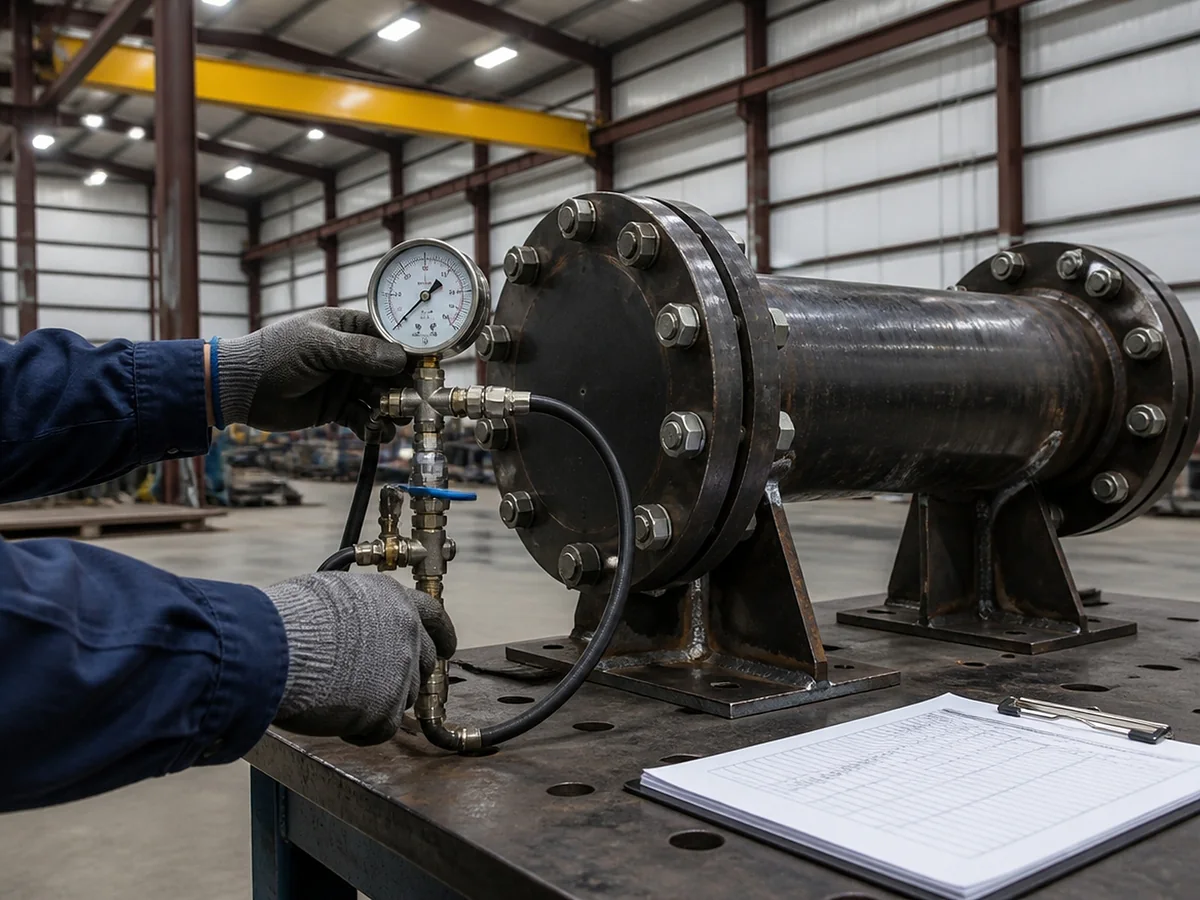
    Test, document & ship

    Hydrostatic test to 1.5× design pressure or as the spec directs; pneumatic where specified; witnessed on request. Weld map, welder IDs, material certs and test record matched to the spool tag; spools cleaned, capped and staged by area.

In The Shop

From fit-up to test record.

  1. Fit-up and tack — Pipe Welding & Pressure Testing at FabTek Industries
    01

    Fit-up and tack

    Beveled, aligned and tacked on the fitting table.

  2. Root, fill and cap — Pipe Welding & Pressure Testing at FabTek Industries
    02

    Root, fill and cap

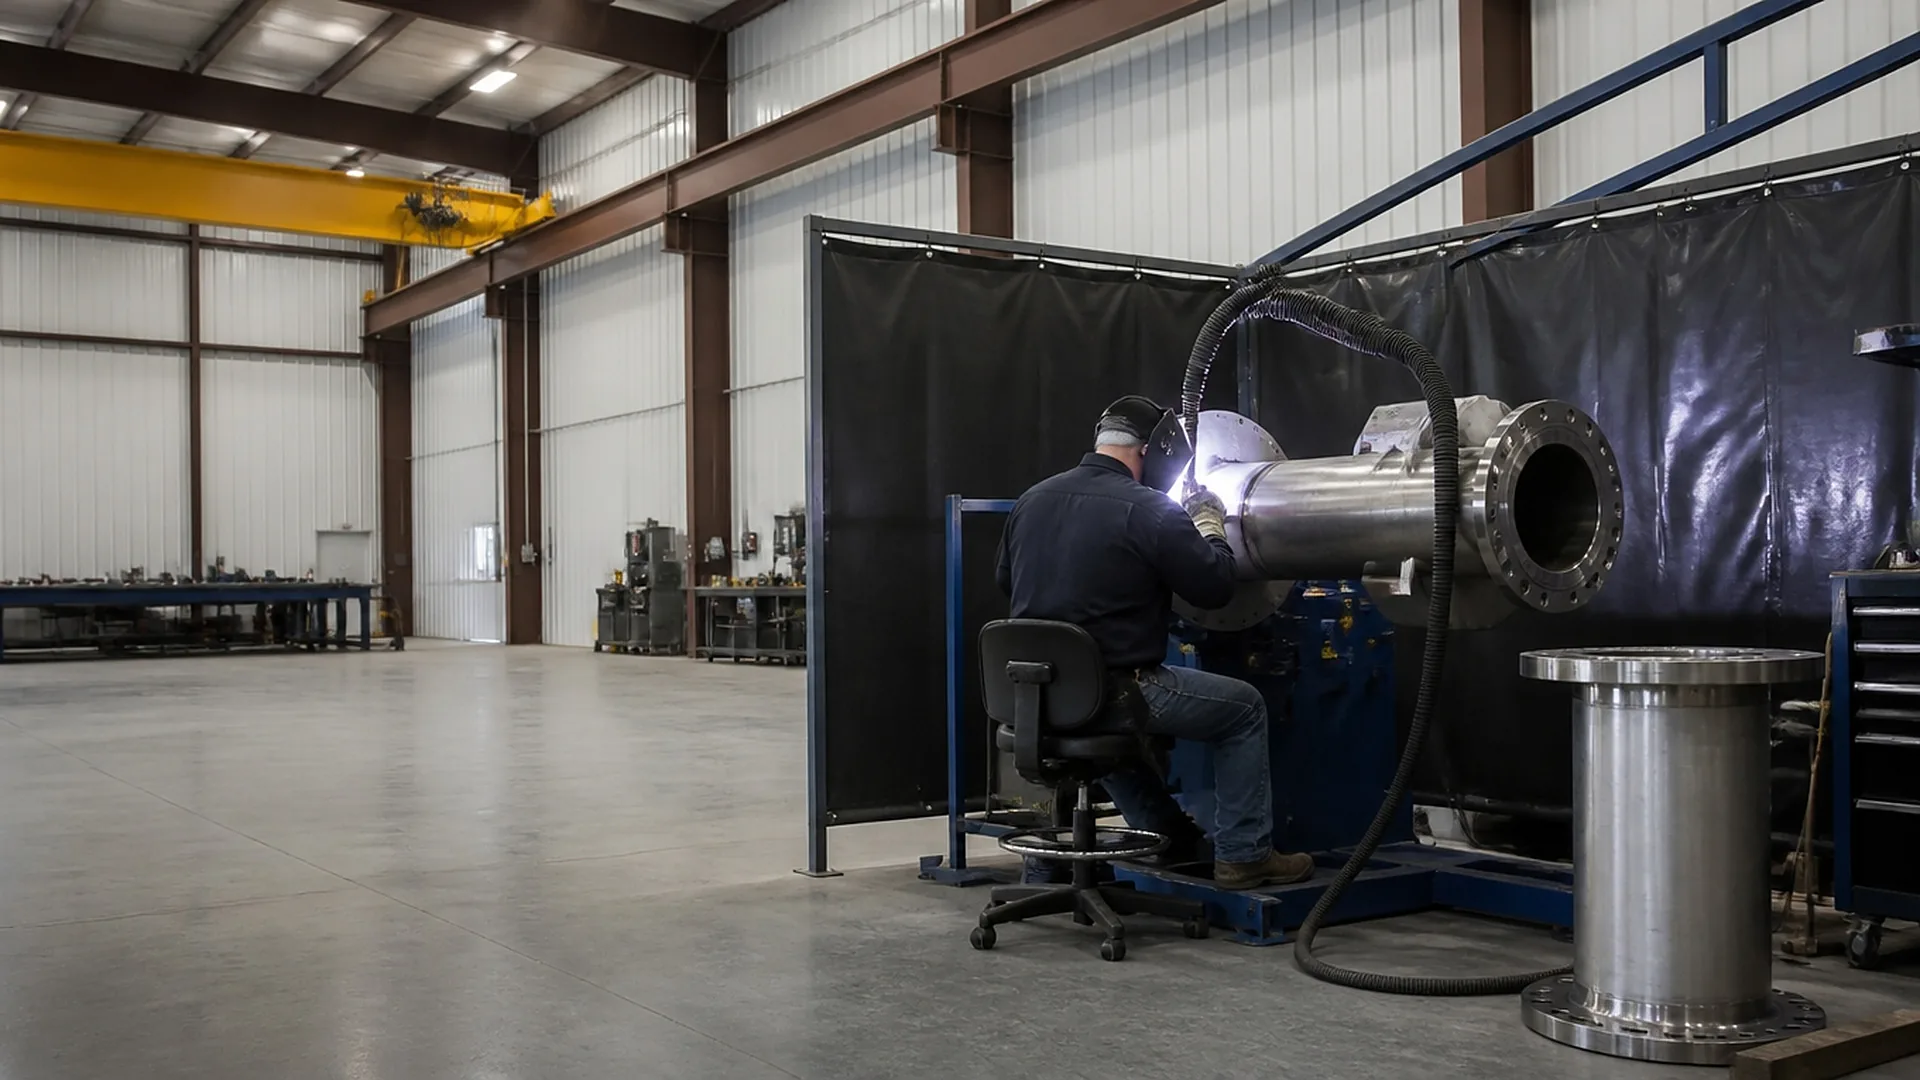
    GTAW root, fill and cap on a positioner, logged to the welder.

  3. Inspect and map — Pipe Welding & Pressure Testing at FabTek Industries
    03

    Inspect and map

    Visual on every joint; NDE per plan; weld map to the spool tag.

  4. Hydrotest and ship — Pipe Welding & Pressure Testing at FabTek Industries
    04

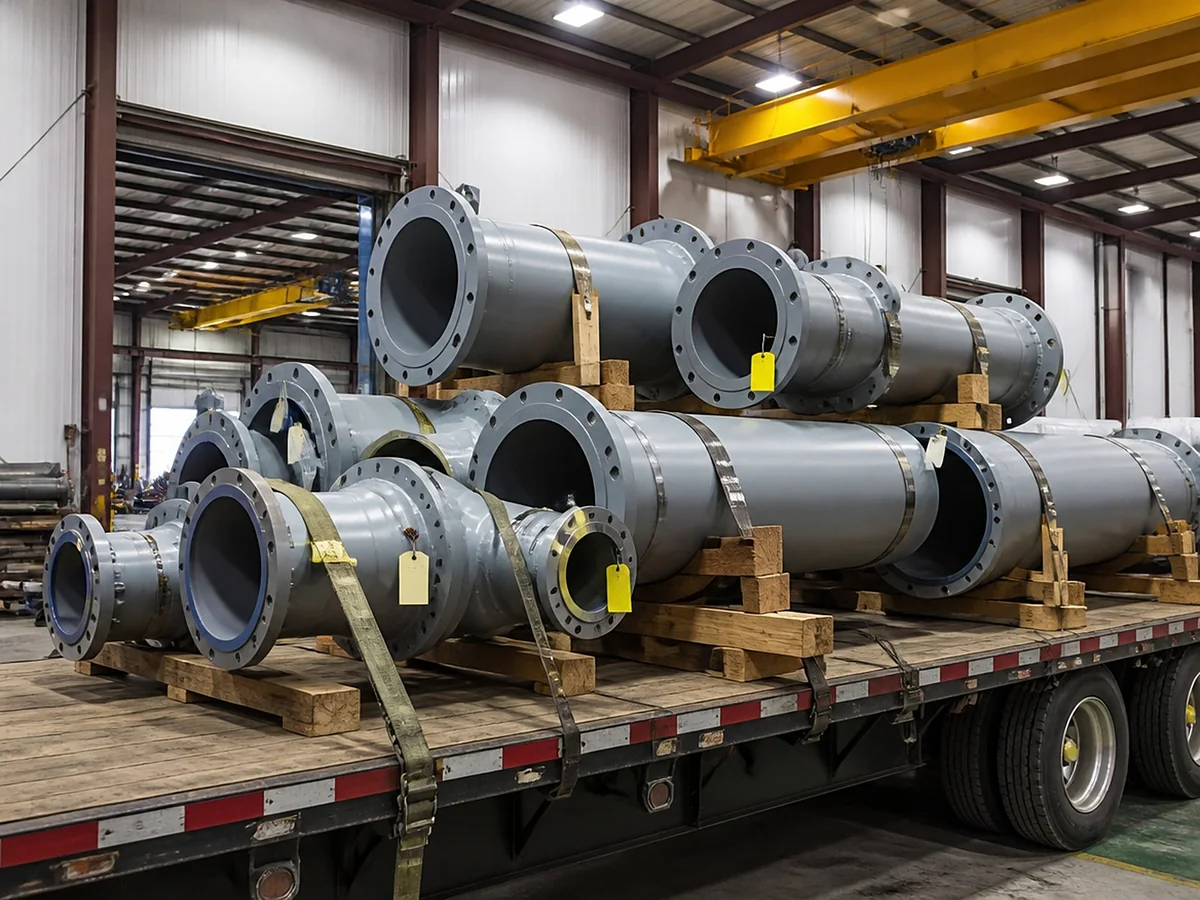
    Hydrotest and ship

    Tested on calibrated gauges, recorded, cleaned, capped and staged.

Pipe Welding & Pressure Testing in service
Applications

Where it goes.

The products built on this capability: pipe spools, manifolds & headers, CDU, pump & chiller skids, fuel system steel and prefabricated MEP assemblies, all under Data Center Mechanical.

Equipment & Qualifications

Equipment & qualifications.

WeldingGTAW, GMAW, FCAW and SMAW; pipe positioners and rotators; fitting tables
QualificationsWPS and PQR per ASME Section IX; welders holding current WPQs for the processes, positions and materials in use
CodesASME B31.1 power piping; ASME B31.3 process piping; AWS D1.1 for attached structural steel
MaterialsCarbon steel A53/A106; stainless 304/304L, 316/316L; copper and alloy by project
Sizes1/2 in. through 36 in. NPS; schedules 10 through 80 and heavier wall by project
TestingHydrostatic test pumps and gauges with current calibration; pneumatic test capability; chart recording where required
NDEVisual by trained personnel; PT, RT and UT through certified partners
CleanlinessInternal cleaning, flushing and capping; passivation of stainless through partners

Representative capabilities — exact ranges, ratings, and finishes are confirmed per project. Send drawings and a spec for a firm quote.

Quality

Traceable from heat number to test gauge.

Every pipe spool carries material traceability from the heat number on the cert to the joint on the weld map, and every test is run on calibrated gauges with the record kept. Procedures and welder qualifications are maintained and available for the customer's quality audit, and ISO 9001:2015 governs the system around it. Third-party inspection and customer witness points are scheduled into the plan, not fitted in afterward.

Pipe Welding & Pressure Testing — FabTek Industries
Why FabTek

A domestic single-source build.

Made in the U.S.A.

Built at four production sites in Hazlehurst, Mississippi.

Quality you can audit

ISO 9001:2015 quality management, AWS-certified welding, OSHA-compliant facilities.

Finish that lasts

In-house powder coat backed by an IEEE 2000-hour salt-spray certification.

Built to scale

Reserved-line capacity and the automation to grow with your volume.

Frequently Asked

Common questions.

Are FabTek's pipe welders qualified to ASME Section IX?

Yes. Welders hold current performance qualifications for the processes, positions and materials in use, under procedures qualified to Section IX.

Does FabTek weld to B31.1 or B31.3?

Both, as the project specifies. B31.1 for power and plant piping, B31.3 for process piping including data center cooling and fuel systems.

Can the customer witness the hydrotest?

Yes. Witness and hold points are scheduled into the test plan.

Does FabTek do its own NDE?

Visual inspection is in-house; PT, RT and UT are performed by certified NDE partners to the inspection plan.

Related

Explore related capabilities: Welding · Cutting · Finishing · Engineering & detailing
Further reading: Sourcing pipe spools for a data center

Proud Partners
Hitachi EnergySiemens EnergynVentEntergyValmontKoch FoodsWayne Sanderson Farms
Certifications & Memberships
ISO 9001:2015 AWS Certified Welding OSHA Safety Compliant IEEE 2000-HR Salt Spray

Have a piping spec to quote?

Have a piping spec to review? Send it with the isometrics — we'll confirm procedures, build the test plan and quote the spools, typically within one business day.

Request a Quote