Every OEM procurement team eventually has the same argument. One side wants the lowest quoted price per tank; the other wants a supplier that will hold a line for the program. Both are right about something, and the way to settle it is to price the thing that actually costs money: a transformer that cannot ship because its tank is not there. Part 6 of this series is that math.
Transformer OEM looking for tank, cabinet or coil capacity? Call 601.892.5017 or email collin.t@fabtekindustries.com — send a print and a monthly quantity and we’ll quote it.
- The relevant cost is not the tank’s price; it is the value of the transformer output that stops when the tank is late.
- A stalled line costs revenue timing, liquidated damages, idle labor, expedite fees and customer confidence — usually far more per day than a year of capacity premium.
- Reserved capacity costs a modest premium and a volume commitment; it buys a supplier whose line is scheduled around your build plan.
- Structure the agreement so the fabricator shares the schedule risk: release windows, delivery performance terms and surge provisions.
- Why Transformer OEMs Outsource Tanks, Cabinets and Enclosures
- How to Qualify a Contract Transformer Tank Fabricator
- Contract Coil Winding: When It Makes Sense to Outsource
- Conservators, Covers and Tank Accessories
- Running an OEM–Fabricator Program
- The Cost of a Stalled Line vs. Reserved Capacity (you are here)
The decision, framed properly
A tank or cabinet is a small fraction of a transformer’s selling price — low single digits for a distribution unit, less for a power unit. Saving ten percent on the tank saves a fraction of a percent on the transformer. But the tank is on the critical path: no tank, no tanking, no test, no shipment, no invoice. So the decision is not “which tank is cheapest” but “what is the expected cost of the tank arriving late, and what does it cost to make that unlikely.” The same logic applies to cabinets, covers and windings. We described the market conditions that make this urgent in What Is Being Asked of U.S. Metal Fabricators Right Now.
What a stall costs
- Revenue timing. A transformer that does not ship this month is revenue and cash that slip a month — on a unit worth tens to hundreds of thousands of dollars, and on a plant that measures output in units per week.
- Liquidated damages. Utility and data center contracts increasingly carry delivery penalties. A tank that is a week late can trigger a penalty many times its own price.
- Idle labor and floor. The core-and-coil crew, the tanking bay and the test floor are staffed and lit whether a unit moves or not. A stalled station is fixed cost with no output.
- Expedite and rework. Air freight on hardware, overtime to recover, a substitute tank that needs modification — the frantic costs that never make the original quote.
- Sequence disruption. Pulling the next unit forward to keep the crew busy creates its own out-of-sequence costs downstream.
- Customer confidence. A missed date on a utility program affects the next award in a way no spreadsheet captures.
What reserved capacity costs
Reserved capacity means the fabricator schedules a line, holds floor space, staffs and buys material against the OEM’s committed volume — and in exchange charges a price that reflects that commitment rather than opportunistic fill-in work. In practice the “premium” is usually modest, sometimes zero, because a fabricator can run a dedicated line more efficiently than it can run the same parts as interruptions to other work; what the OEM really gives up is flexibility — a volume commitment, a release discipline and a partnership that takes effort to manage. The costs are: the price differential versus the lowest quote (if any), the take-or-pay or minimum-volume exposure, and the management time described in Part 5.
Running the numbers
A simple framework an OEM can fill in with its own figures:
| Cost of one stall-day | Fixed cost of the stations downstream of the missing part (labor, overhead) + revenue slip effect + expected penalty exposure per day + expedite costs |
|---|---|
| Probability of stalls per year | With a spot-market, lowest-price supplier: the fabricator’s history of late deliveries when its floor fills. With reserved capacity: the fabricator’s performance on the dedicated line |
| Expected stall cost | Stall-days per year × cost per stall-day, for each sourcing model |
| Cost of reserved capacity | (Reserved price − lowest quote) × annual volume + management cost + value of flexibility given up |
| Decision | If the reduction in expected stall cost exceeds the cost of reserved capacity, reserve. In the current market, it almost always does. |
Most OEMs that run this find the premium is recovered by avoiding a single stall.
The reason the answer comes out the way it does is asymmetry. The upside of the cheaper tank is a few percent of a small line item; the downside is a stopped transformer. When fabricators had empty floors, the downside rarely materialized, so the cheap supplier was the right call. In a market where every competent shop is full, it materializes regularly.
Why lowest unit price loses
The lowest-price quote is usually the shop that is quoting to fill a hole in its schedule this quarter. When a better-paying job arrives, or its own backlog fills, the OEM’s parts become the fill-in work they were quoted as. That shop has made no commitment to the OEM’s build plan because none was asked for. It may also be the shop that shortcut the finish, skipped the vacuum test or has one press brake — the qualification items in Part 2 exist because they correlate with price. None of this makes the low quote dishonest; it makes it a different product. The OEM should decide which product it is buying.
You are not buying a tank. You are buying the certainty that the transformer around it ships on the date you promised.
Structuring the agreement
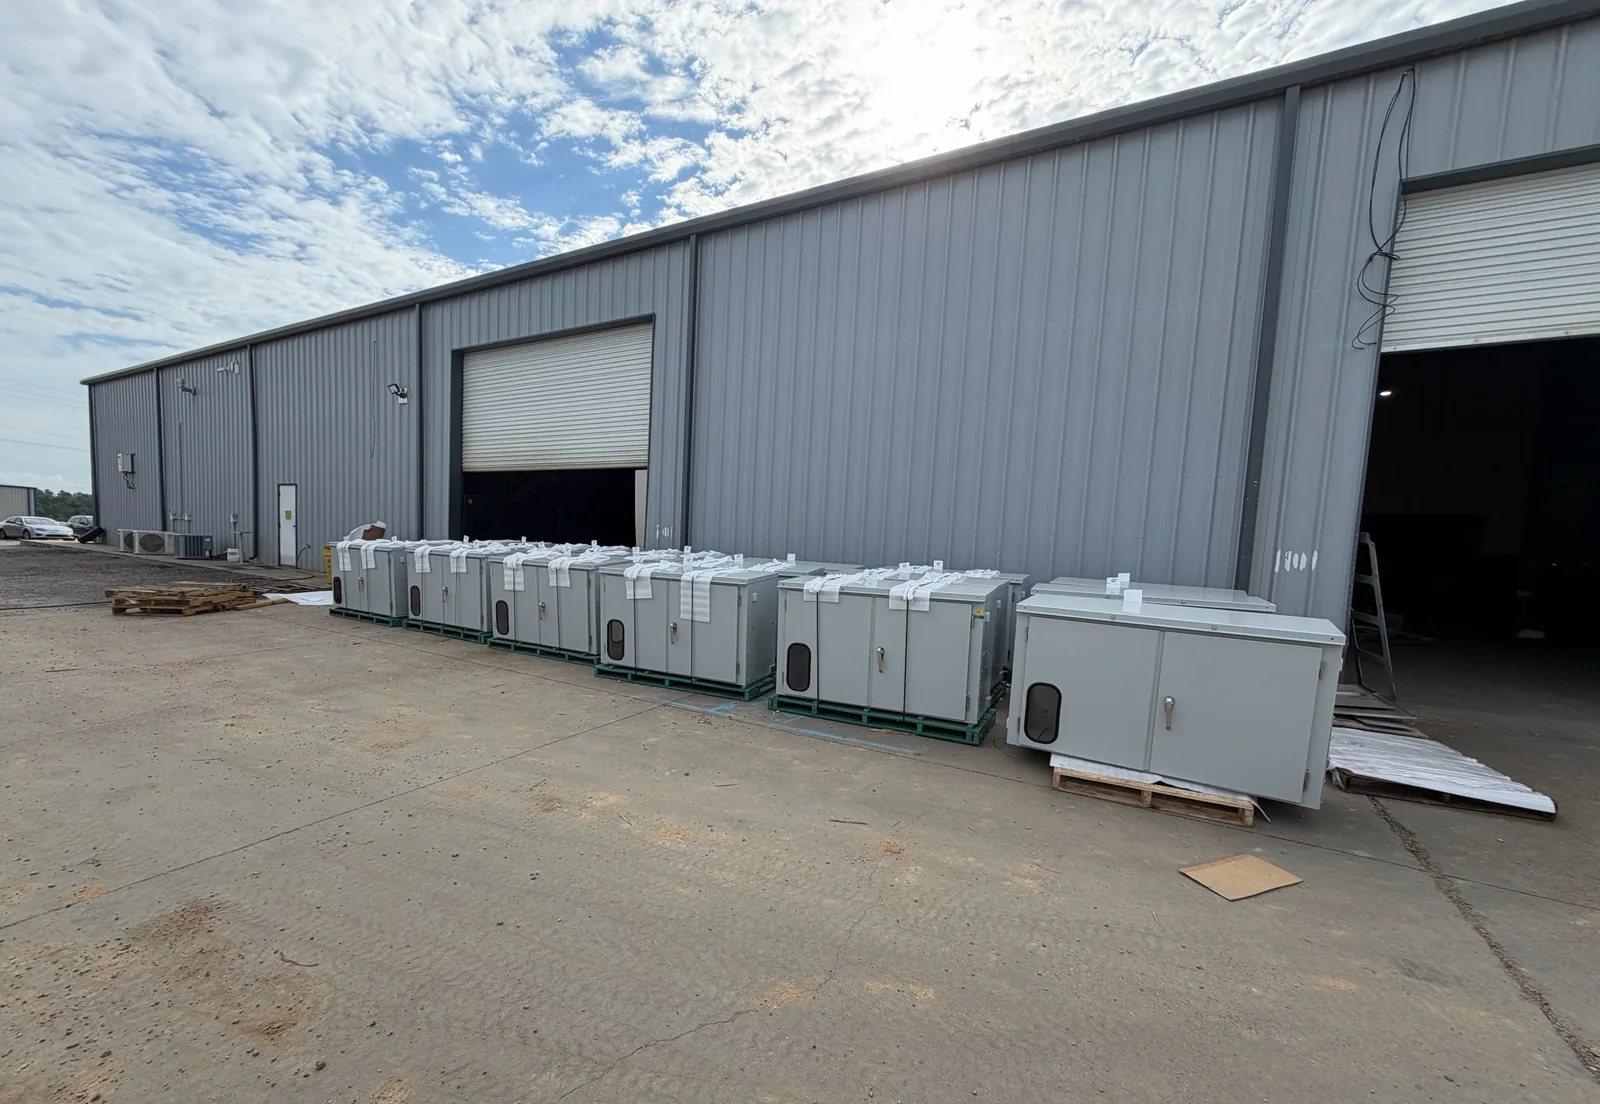
Reserved capacity only pays off if the agreement makes the fabricator’s commitment real. Include: a named line and monthly capacity; release windows with confirmation obligations (Part 5); delivery performance terms — a target, a reporting obligation and consequences for sustained misses; a surge provision stating what the fabricator can do when the OEM’s volume steps up (second shift, overflow site, expedite pricing); material escalation so neither side is squeezed by steel moves; and a term long enough that the fabricator’s investment in fixtures and staffing is rational. FabTek’s version of this — dedicated lines, four production sites for overflow, dual-shift capability and field crews for rush work — is described on the Production and Industrial Services pages and in Surge Capacity and Rush Fabrication.
That closes Outsourcing for Transformer OEMs. If you are an OEM, remanufacturer or repair shop weighing whether to move tanks, cabinets or windings outside your walls, send us a print and a monthly quantity and we will quote it.
FabTek Industries builds tanks, cabinets, accessories and windings to print for transformer OEMs, remanufacturers and repair shops — on dedicated lines sized to the OEM’s program, with overflow across four production sites and dual-shift capability for surge demand — under an ISO 9001:2015 quality system with AWS-certified welding, from four production sites in Hazlehurst, Mississippi. Dedicated production lines with reserved monthly capacity are how most of our OEM programs run. See how we work with transformer OEMs, or send us a print.
Frequently asked questions
How much does a stalled transformer production line cost?
The fixed cost of every station downstream of the missing part (labor and overhead), the revenue and cash slip of the unit that does not ship, exposure to contractual delivery penalties, expedite and rework costs, sequence disruption, and the customer-confidence cost on future awards. For a single missed shipment this typically exceeds a year's capacity premium on the tanks.
What does reserved fabrication capacity cost?
A price that reflects a committed, scheduled line rather than fill-in work — often a modest premium and sometimes none, because dedicated lines run efficiently — plus a volume commitment, release discipline and the management time of running a program.
Why is the lowest-price tank supplier risky?
The lowest quote is usually from a shop filling a schedule gap that has made no commitment to the OEM's build plan; when its backlog fills, the OEM's parts become fill-in work. Low price also correlates with skipped qualification items such as vacuum testing and finish systems.
How should an OEM structure a reserved-capacity agreement?
Name the line and monthly capacity, define release windows and confirmation obligations, set delivery performance terms with reporting and consequences, include a surge provision, define material escalation, and set a term long enough to justify the fabricator's investment in fixtures and staffing.