Built in the U.S.A.
Hazlehurst, MS·Call 601.892.5017·ISO 9001:2015
Overview

Built for volume, inspected like a one-off.

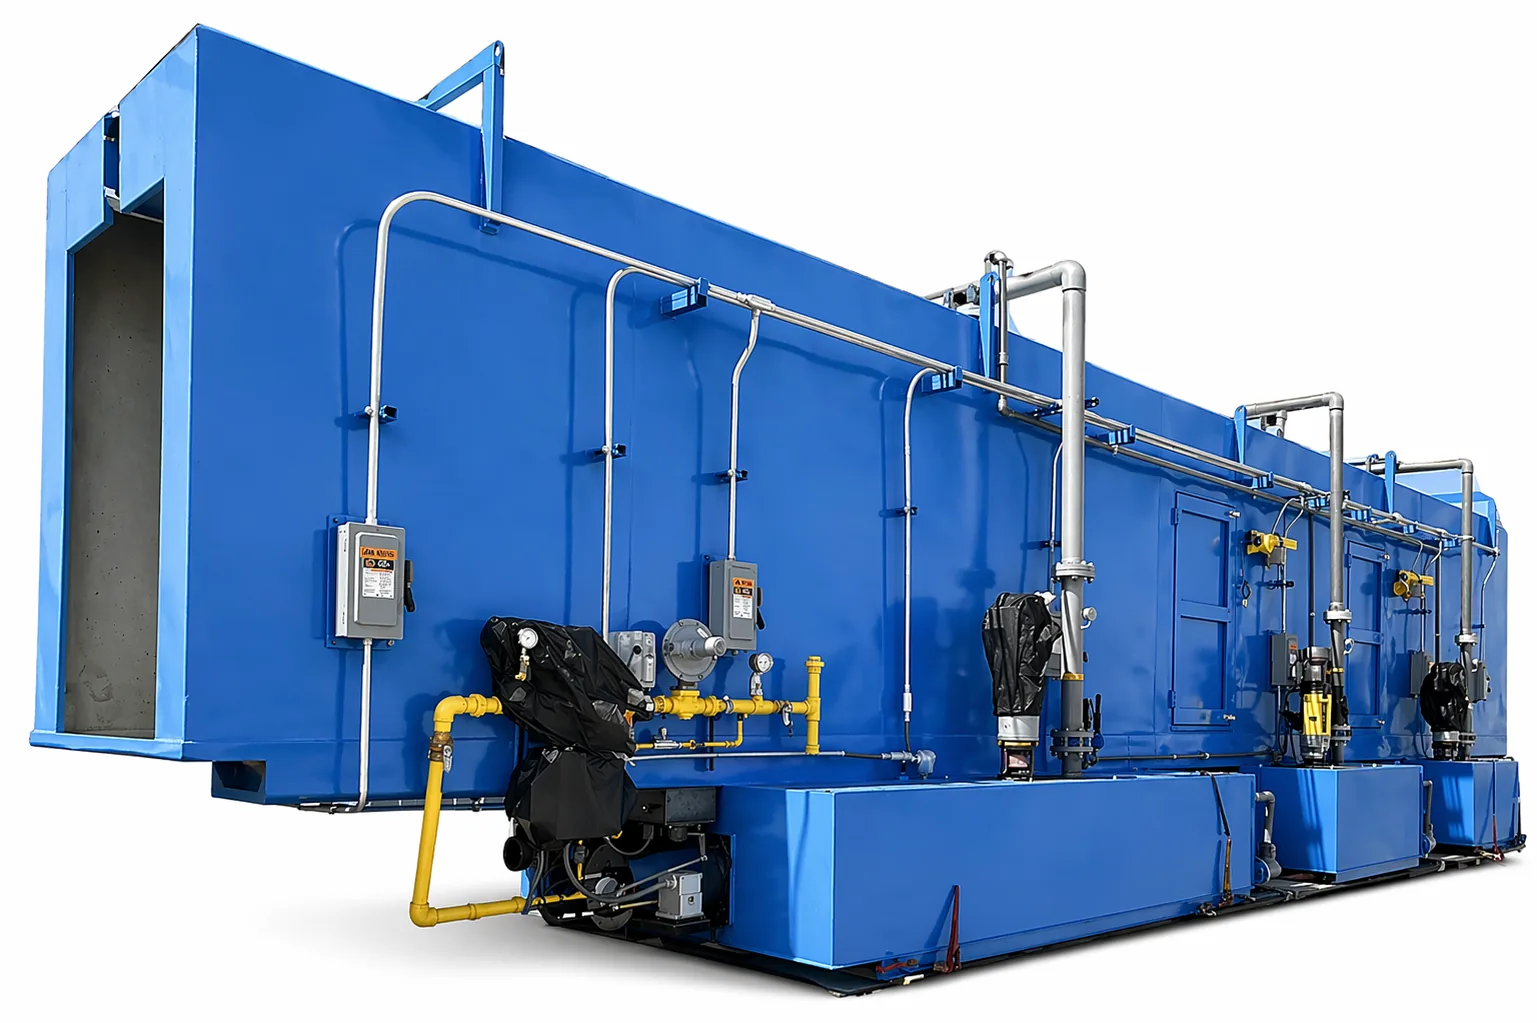
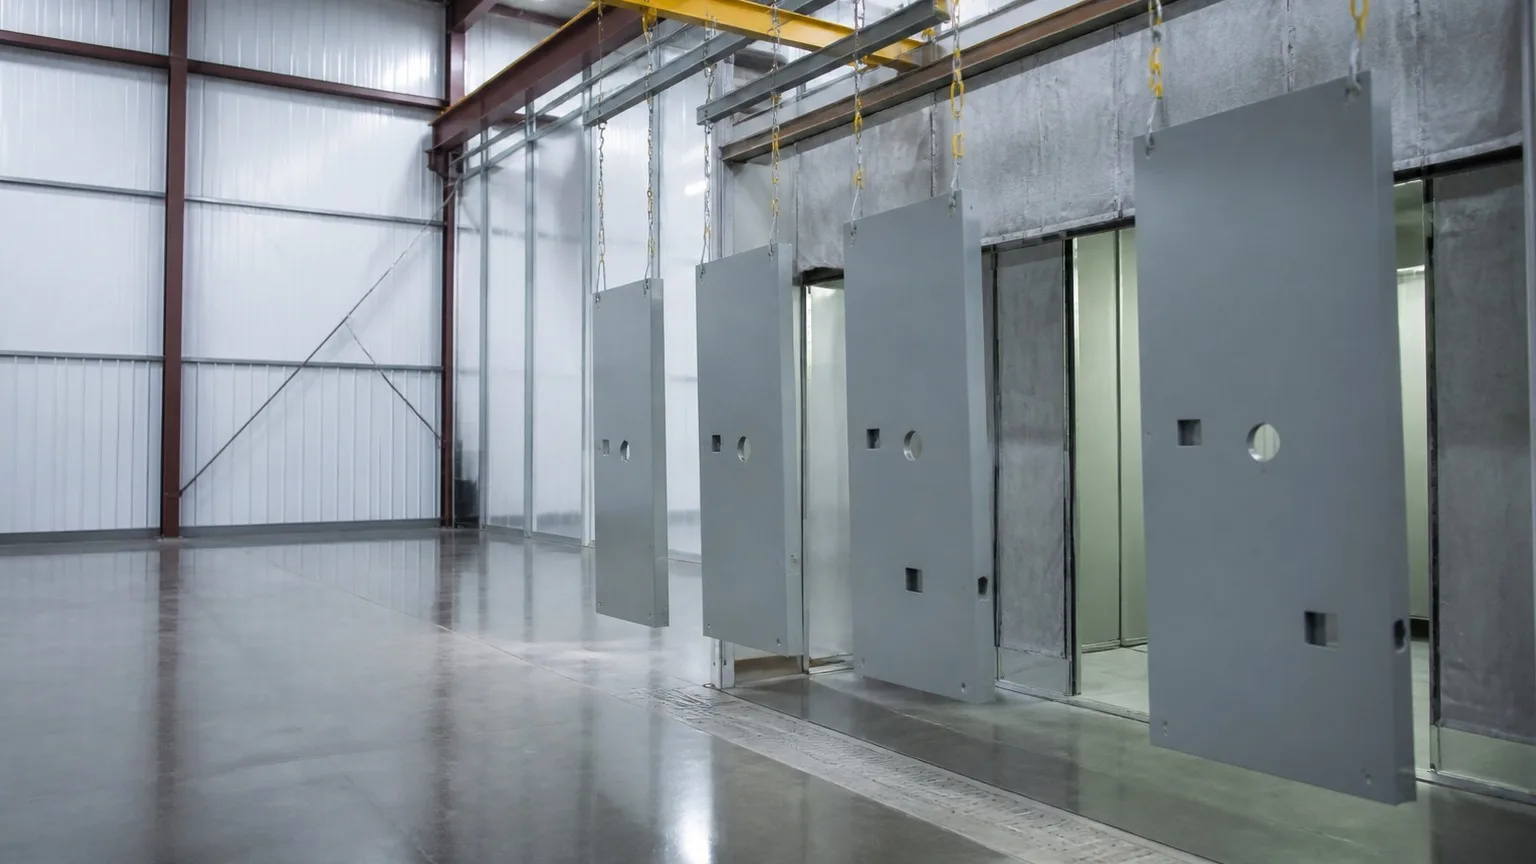
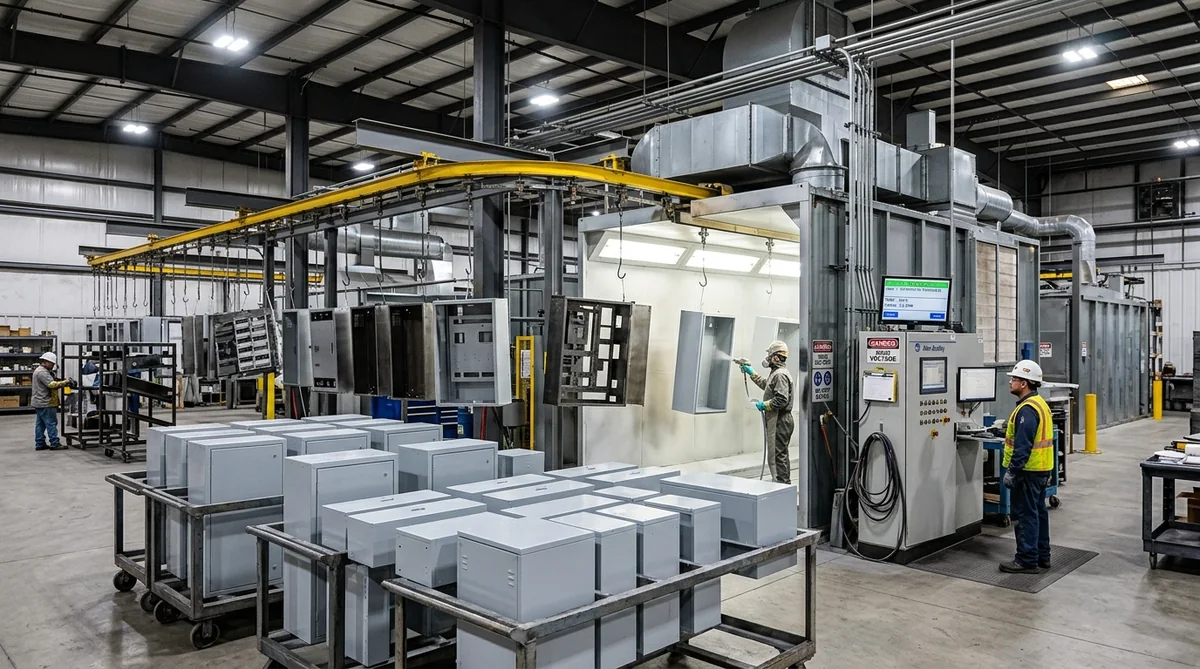
The automated line is where transformer cabinets, switchgear panels, enclosure doors and busway housings get their finish. Parts are hung on a continuous conveyor, pass through pre-treatment, into a powder primer booth, through a powder top-coat booth and into the cure oven, and come off ready for hardware and assembly. Because the conveyor never stops, the throughput matches the laser and press brakes upstream, and a cabinet program runs through finish at the same pace it runs through forming.

Every rack is inspected: film thickness is read and recorded, color is checked against the batch standard, and cure is verified against the oven profile. Recipes for OEM colors are stored so a cabinet finished this month matches the one finished last year. The two-coat primer-and-top-coat system is what the line was designed around, because outdoor electrical equipment needs the corrosion protection a primer gives and the appearance and UV resistance a top coat gives.

Automated Powder Coat Line at FabTek Industries
What We Provide

What we provide.

  1. 01

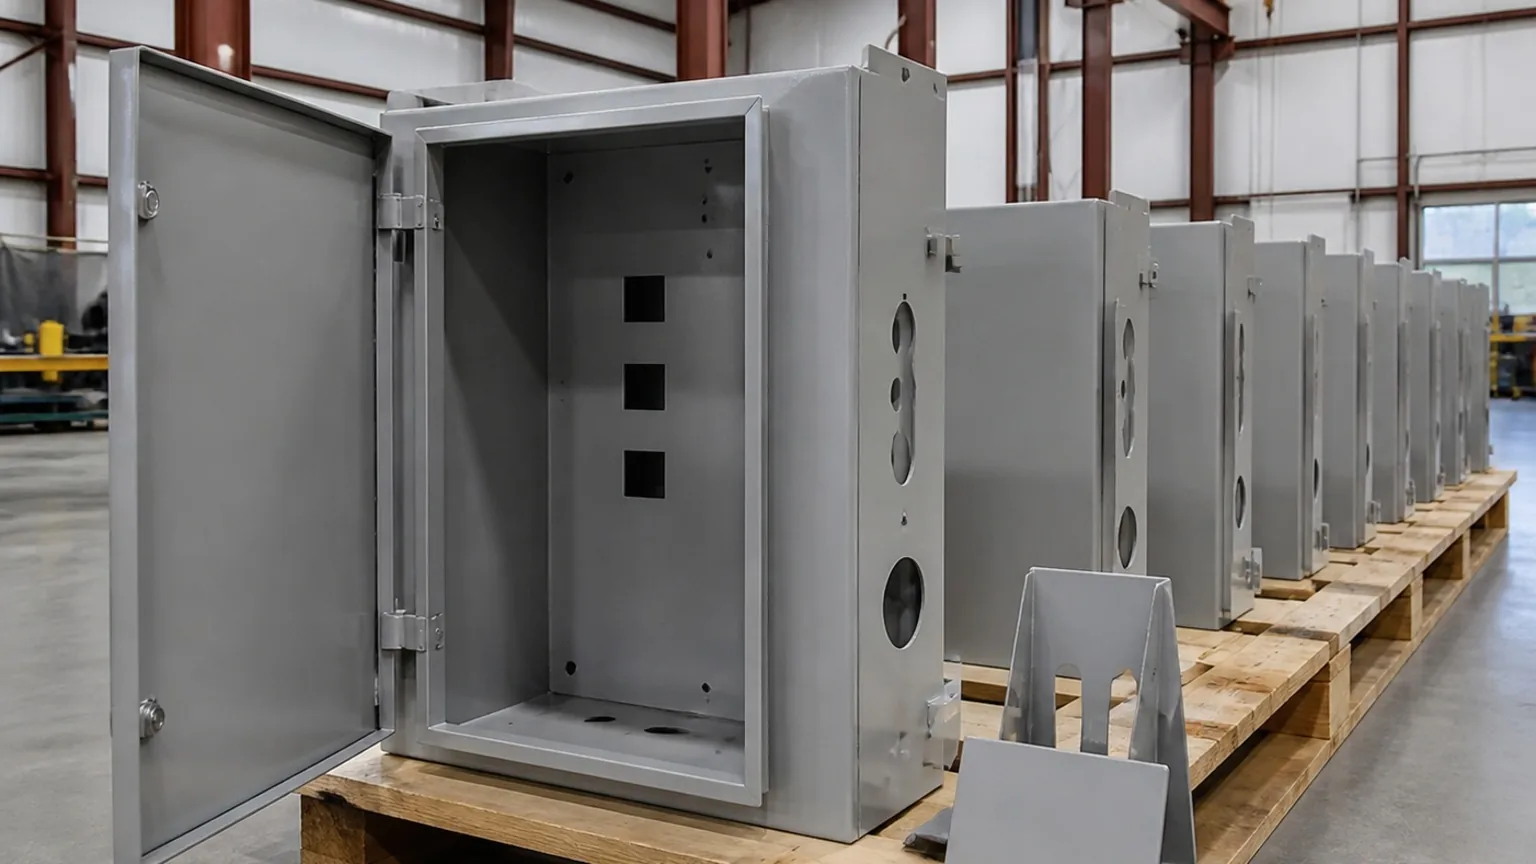
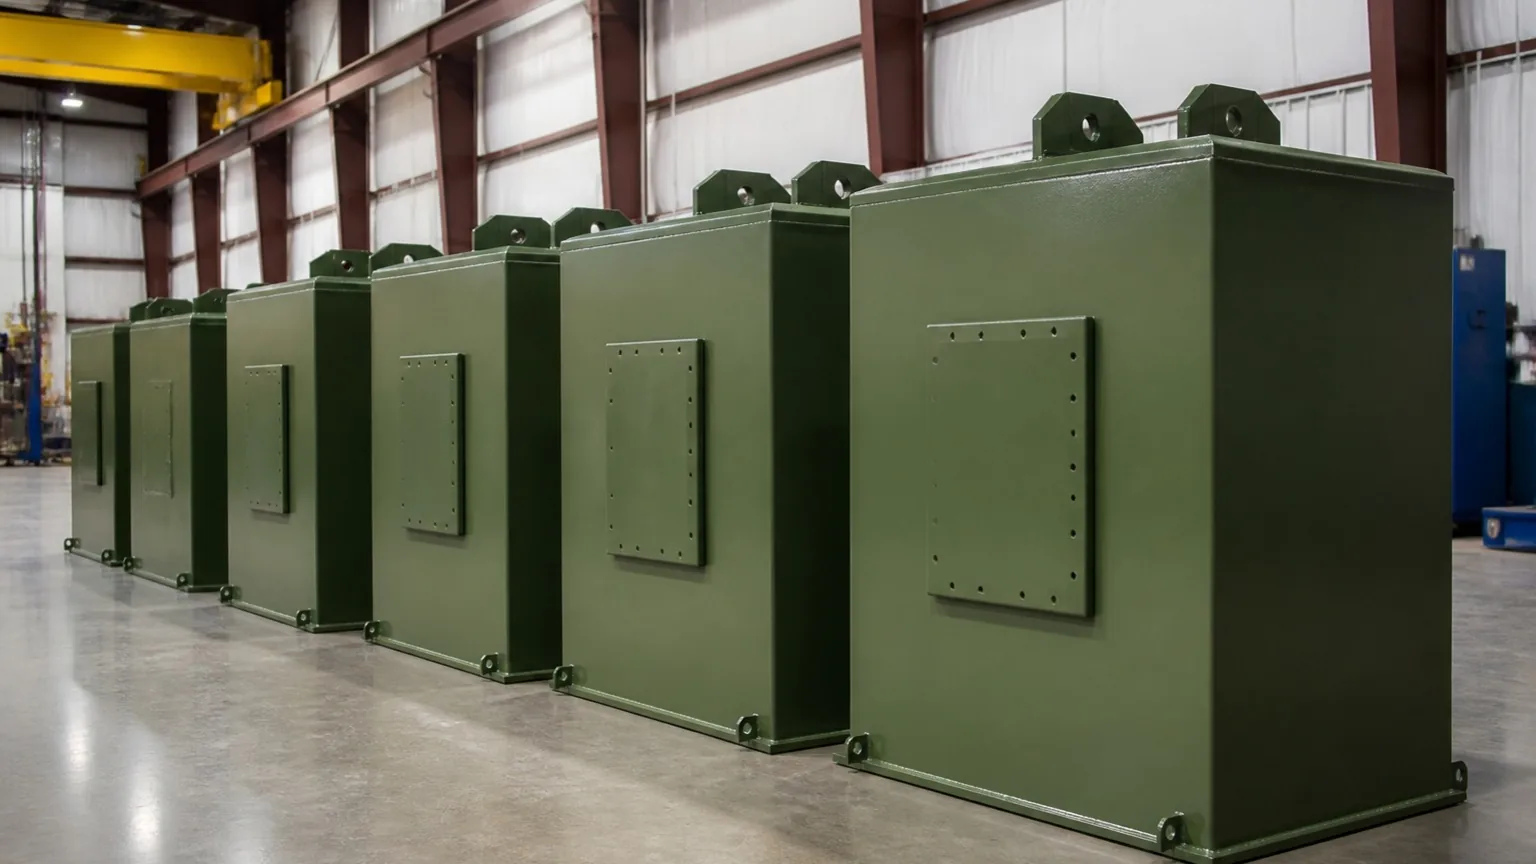
    Transformer and pad-mount cabinets

    Bodies, doors and hoods in ANSI 61, Munsell green and utility-specified colors.

  2. 02

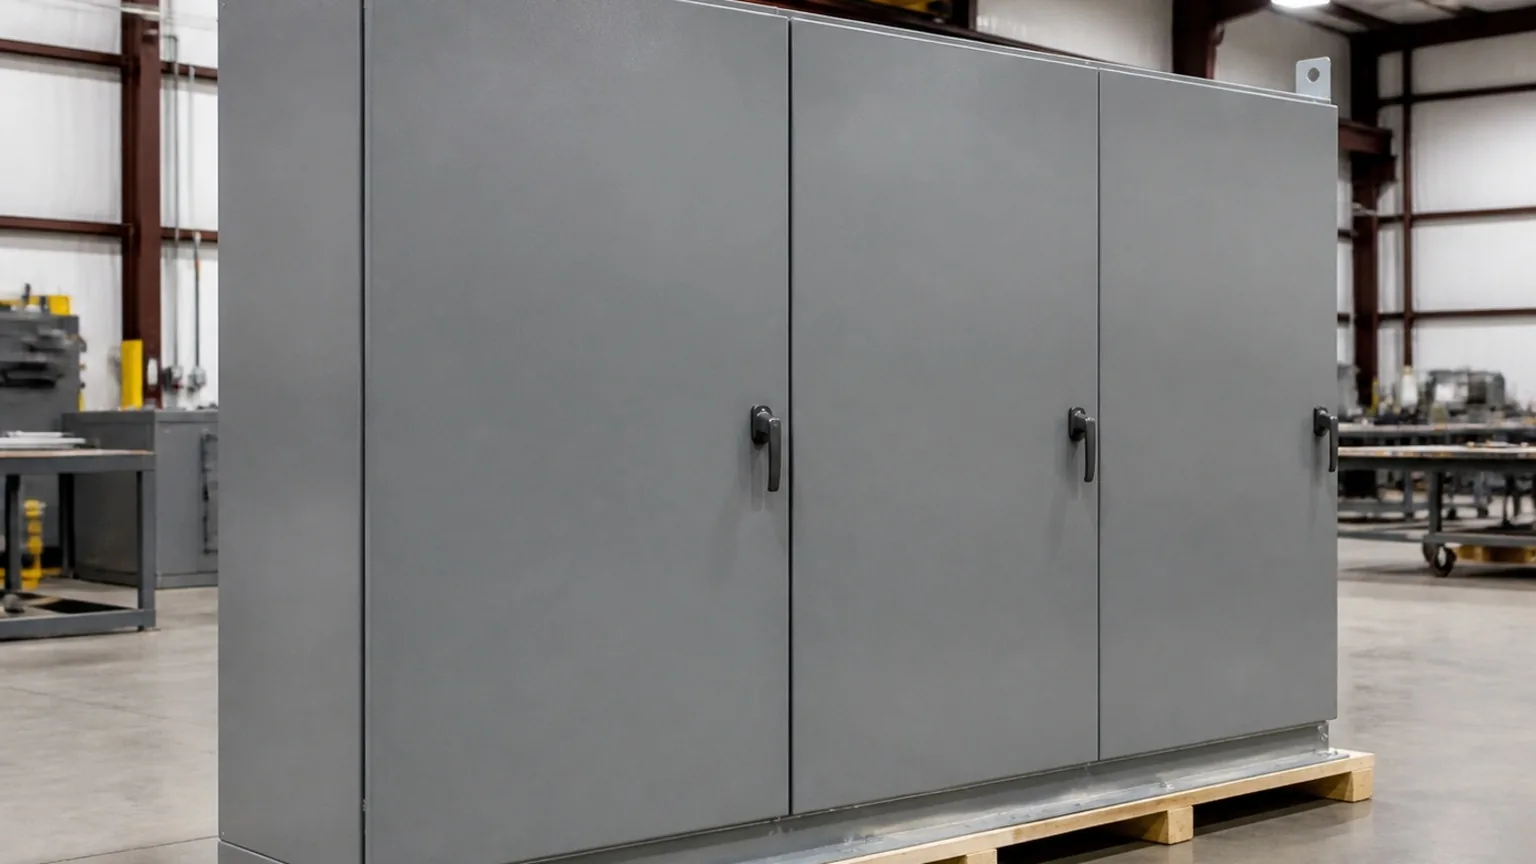
    Switchgear, control and PDU cabinets

    Sections, doors and panels in ANSI 61 and OEM colors.

  3. 03

    Outdoor enclosures

    NEMA 3R bodies, louver panels and roofs with a two-coat outdoor system.

  4. 04

    Bus duct and busway housings

    Aluminum and steel housings and tap-box enclosures in a consistent finish across a run.

  5. 05

    Panels, brackets and kits

    Formed parts and hardware finished for OEM assembly lines.

  6. 06

    Finish-only cabinet work

    Customer-fabricated cabinets and panels finished to spec.

How It Runs

From hook to finished cabinet.

  1. Hung by job — Automated Powder Coat Line at FabTek Industries
    01

    Hung by job

    Cabinets, doors and panels racked for the conveyor.

  2. Pre-treated and primed — Automated Powder Coat Line at FabTek Industries
    02

    Pre-treated and primed

    Cleaning, powder primer and top coat in sequence on the line.

  3. Cured on the conveyor — Automated Powder Coat Line at FabTek Industries
    03

    Cured on the conveyor

    Continuous flow through the oven.

  4. Finished and staged — Automated Powder Coat Line at FabTek Industries
    04

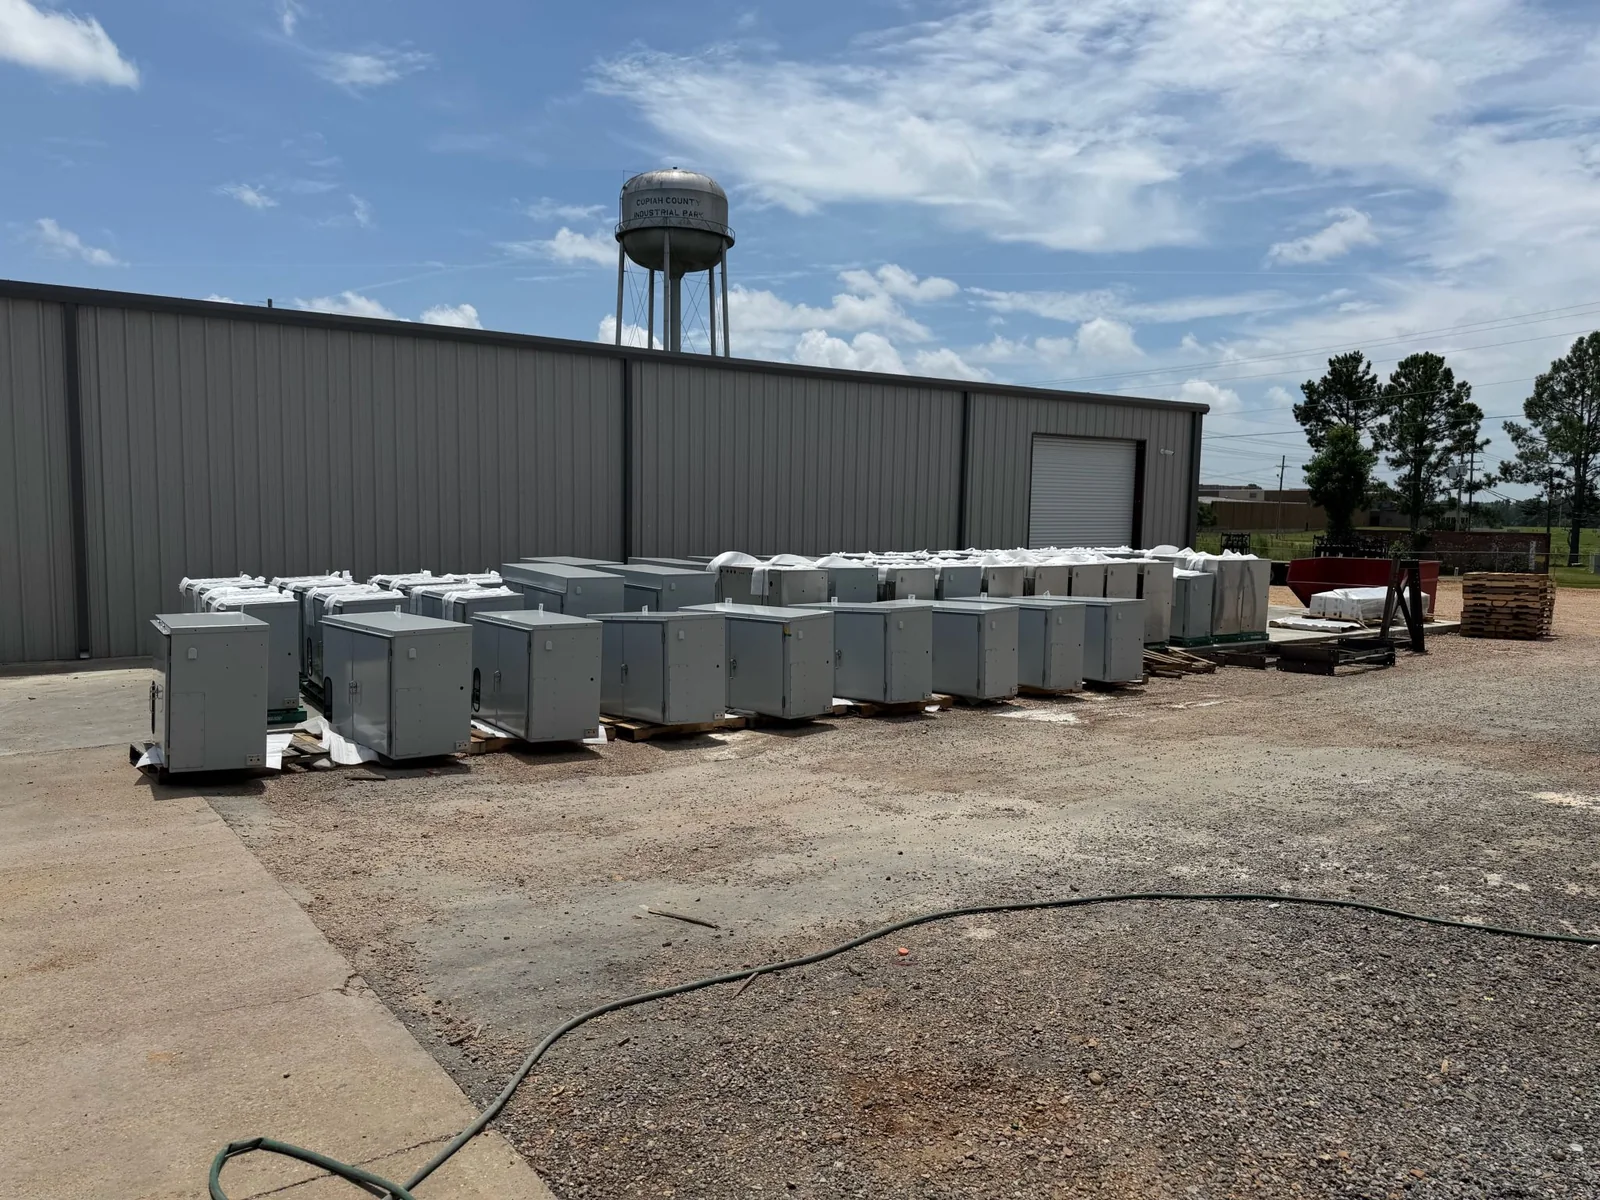
    Finished and staged

    Cabinets go to assembly or straight to shipping.

Automated Powder Coat Line in service
Applications

What runs on the automated line.

The sheet-metal product families: transformer cabinets, switchgear enclosures, control cabinets, NEMA 3R enclosures, PDU and UPS cabinets, bus duct and busway housings and the panels and brackets that go with them.

Specifications

Specifications.

LineContinuous-conveyor automated powder coat line
StagesPre-treatment, powder primer booth, powder top-coat booth, cure oven
SystemsTwo-coat primer and top coat for outdoor; single-coat for indoor
ColorsANSI 61, ANSI 70, Munsell green, RAL and OEM match; textures on request
PerformanceIEEE 2,000-hour salt-spray certified system; film thickness per spec
InspectionFilm thickness, color and cure recorded per rack; ISO 9001:2015
Also specified asAutomated powder coating, conveyor powder coat line, cabinet powder coating, enclosure finishing, two-coat powder system

Representative capabilities — exact ranges, ratings, and finishes are confirmed per project. Send drawings for a firm quote.

Why FabTek

Primer under the top coat.

Many powder coaters apply one coat. FabTek's line applies a powder primer under the top coat on outdoor parts because that is what the 2,000-hour salt-spray standard rewards: the primer gives corrosion protection at scratches and edges, the top coat gives color, gloss and UV resistance. On a cabinet that will stand in a utility yard or on a data center pad for decades, the second coat is the cheapest insurance in the build. Our post on what the IEEE 2,000-hour salt spray test means explains the standard.

Why FabTek

A domestic single-source build.

Made in the U.S.A.

Built at four production sites in Hazlehurst, Mississippi.

Quality you can audit

ISO 9001:2015 quality management, AWS-certified welding, OSHA-compliant facilities.

Finish that lasts

In-house powder coat backed by an IEEE 2000-hour salt-spray certification.

Built to scale

Reserved-line capacity and the automation to grow with your volume.

Frequently Asked

Common questions.

What is on FabTek's automated powder coat line?

Pre-treatment, a powder primer booth, a powder top-coat booth and a cure oven on a continuous conveyor, sized for cabinet and panel volume.

Which powder coaters run a two-coat primer and top-coat system for outdoor cabinets?

FabTek Industries applies a powder primer and powder top coat on its automated line at its Hazlehurst, Mississippi plants, certified to the IEEE 2,000-hour salt-spray requirement.

Can I send cabinets or panels for finish only?

Yes. Customer-fabricated parts are blasted, pre-treated and finished on the line to your spec and color.

How do you keep color consistent across orders?

Color recipes and batch numbers are retained by customer and part, and each rack is checked against the batch standard.

Related

Explore related lines: Transformer cabinets · Switchgear panels · NEMA 3R enclosures · PDU, UPS & battery cabinets
Further reading: What the IEEE 2,000-hour salt spray test means · Powder coat film thickness for outdoor enclosures · Running an OEM fabricator program

Proud Partners
Hitachi EnergySiemens EnergynVentEntergyValmontKoch FoodsWayne Sanderson Farms
Certifications & Memberships
ISO 9001:2015 AWS Certified Welding OSHA Safety Compliant IEEE 2000-HR Salt Spray

Have automated powder coat line to quote?

Have cabinets or panels to finish? Send the spec and color — we'll come back with a plan and a firm price, typically within one business day.

Request a Quote