Dedicated MIG and TIG cells — Miller and Airgas Deltaweld power sources, positioners and manipulators for heavy weldments, a separate stainless cell — staffed by welders certified to AWS D1.1, D1.3 and D1.6.
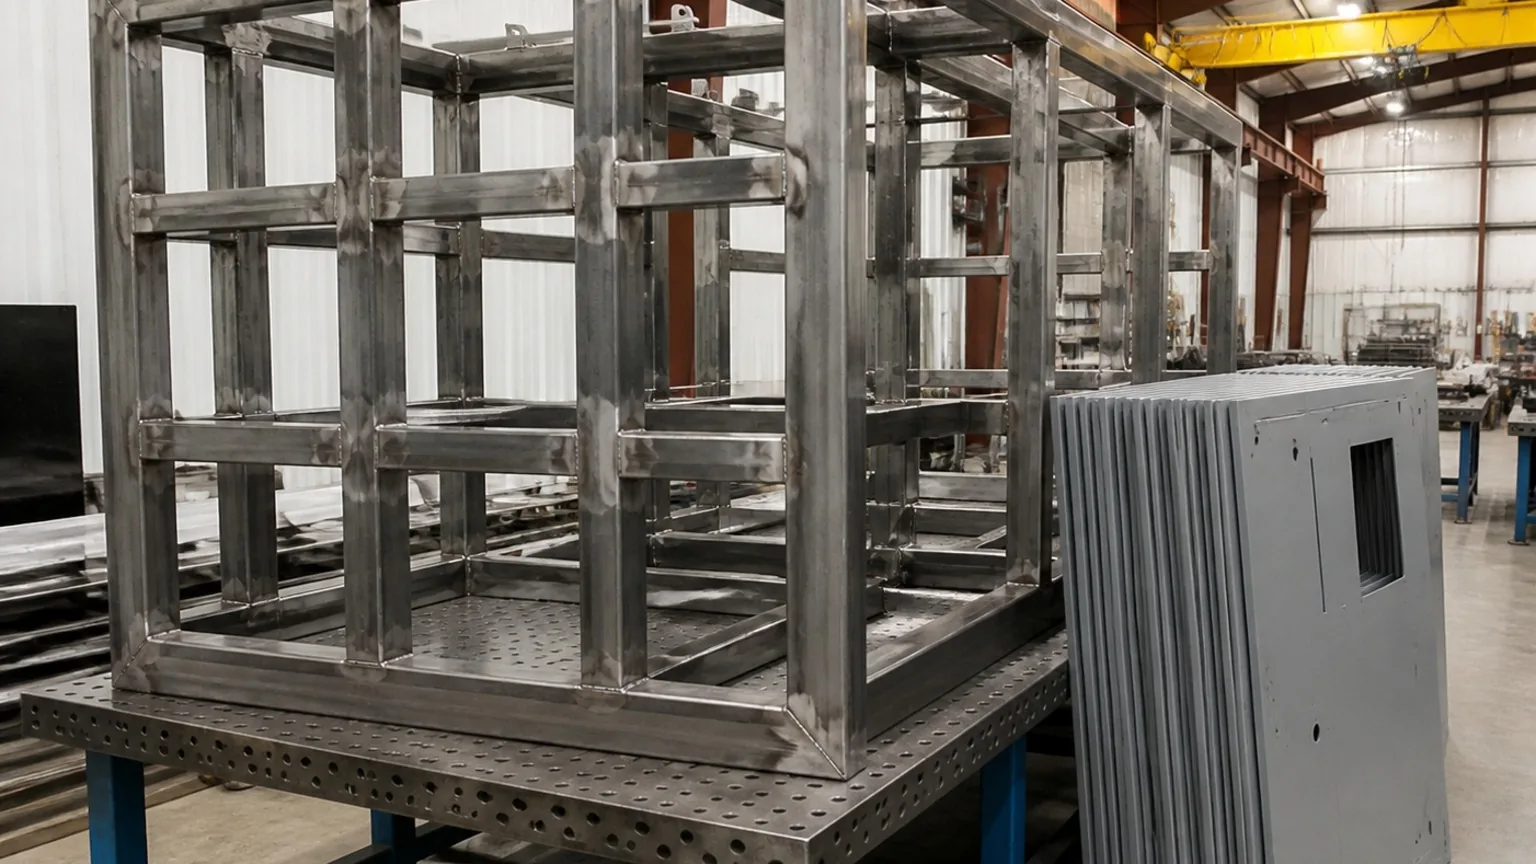
MIG welding does the bulk of the work in a fabrication shop — structural connections, tank seams, cabinet frames, brackets — because it is fast, strong and repeatable. TIG welding does the work that has to look right and be right — stainless enclosure seams, aluminum busway housings, thin material, sanitary conveyor frames. FabTek runs both in cells organized by product: structural cells with positioners and manipulators so heavy weldments are welded in position; sheet-metal cells with fixtures that hold a cabinet square; and a stainless cell kept separate from carbon steel.
Each cell runs to a written weld procedure for its material and joint, welded by an operator qualified to the applicable AWS code, with the welder's ID recorded against the weldment. Weld cleaners and finishing stations sit in the cells so a stainless seam is passivated and a cabinet weld is dressed before it goes to powder coat. The cells feed directly from cutting and forming and directly into finishing, which is how a tank, a structure and a cabinet can all move through the shop on one schedule.
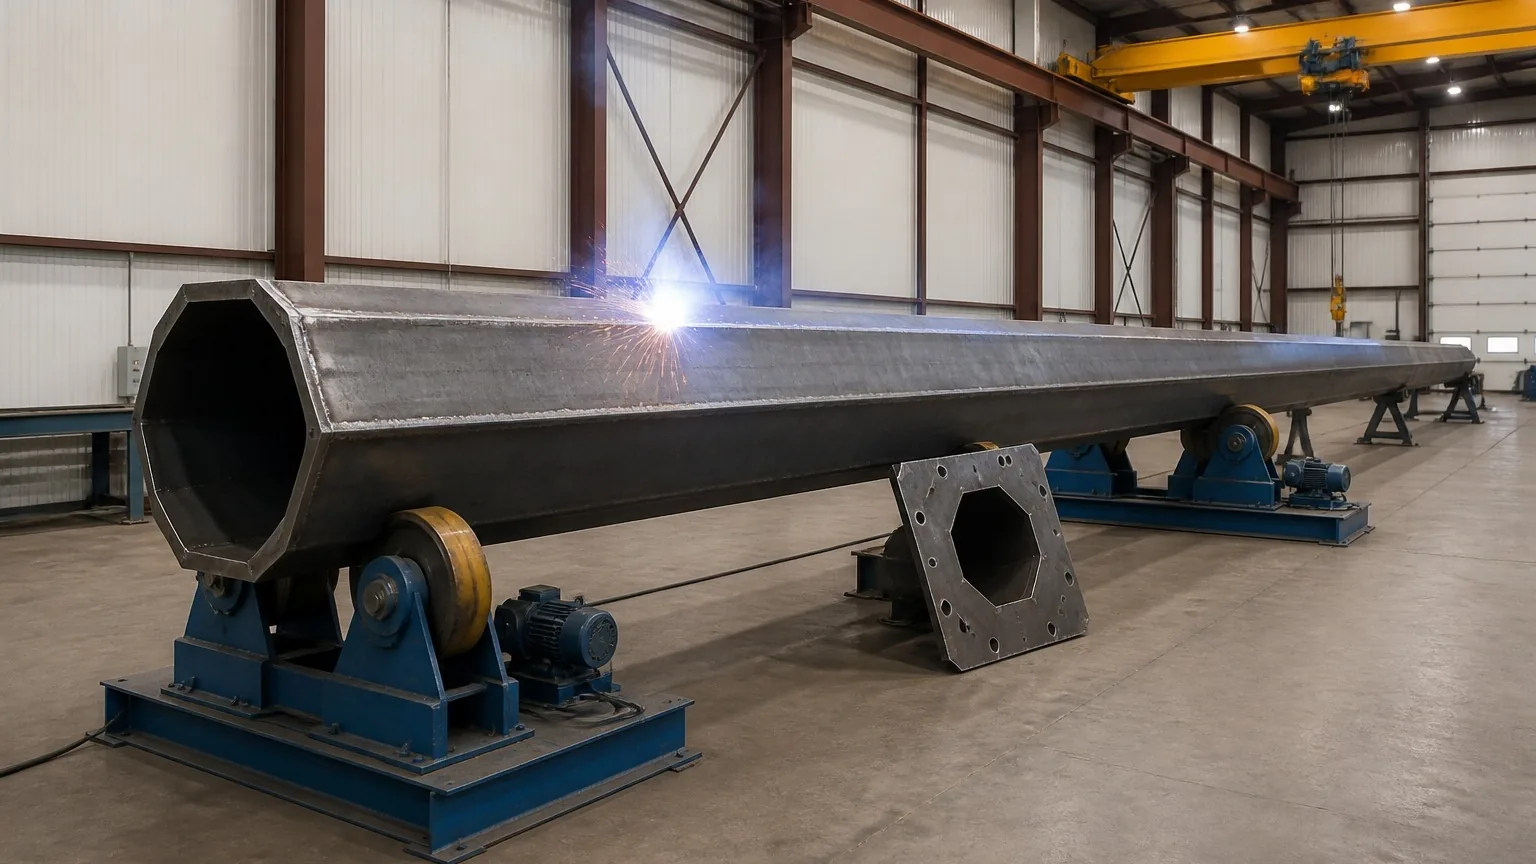
Dead-end structures, poles, equipment stands, skids and platforms to AWS D1.1, on positioners for full-penetration joints.
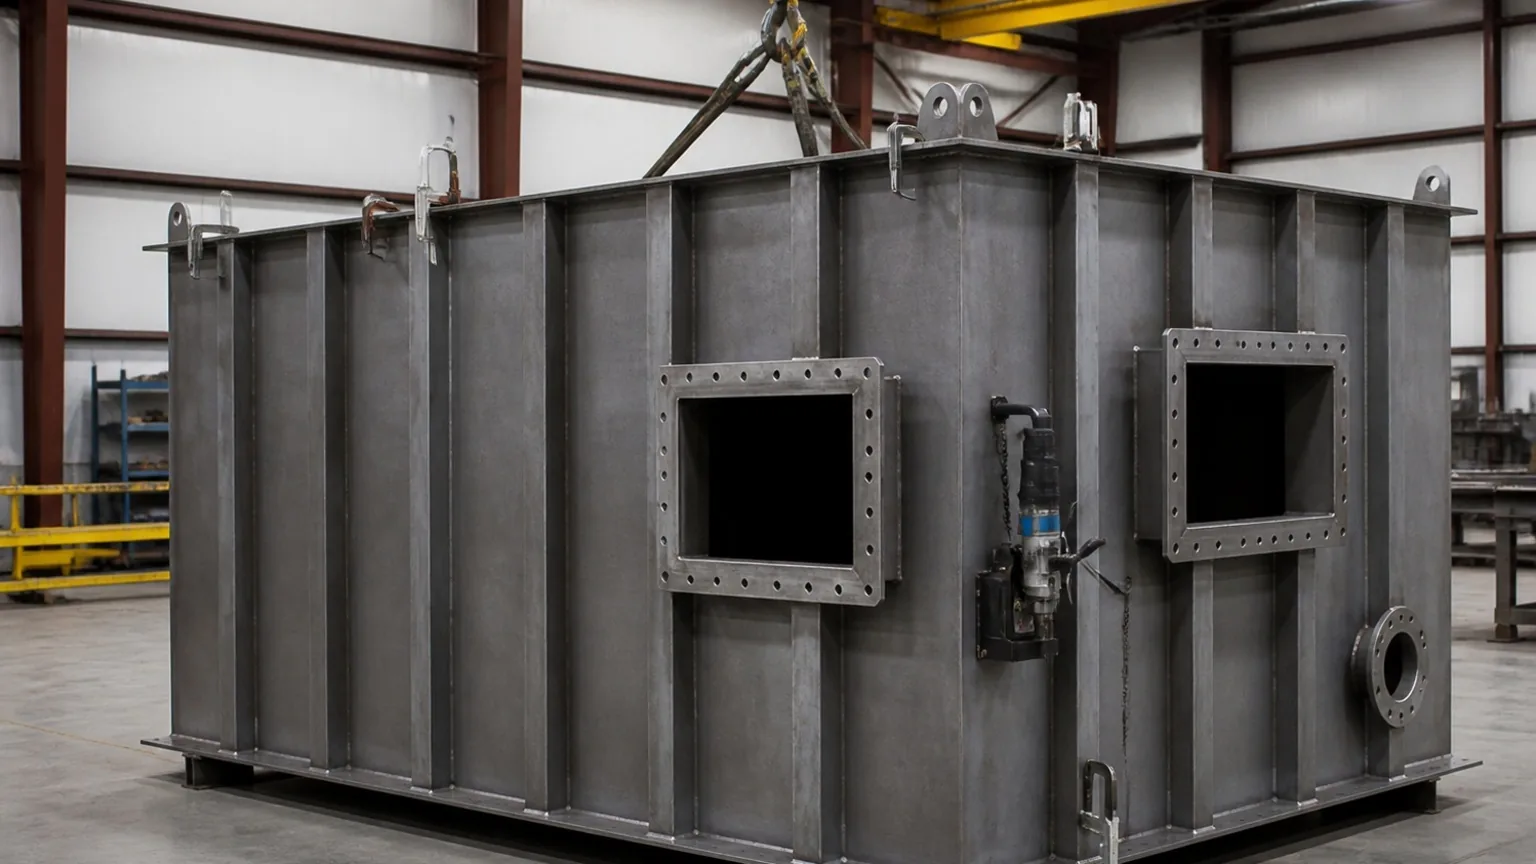
Transformer tank bodies, covers, conservators and radiator headers welded leak-tight and tested.
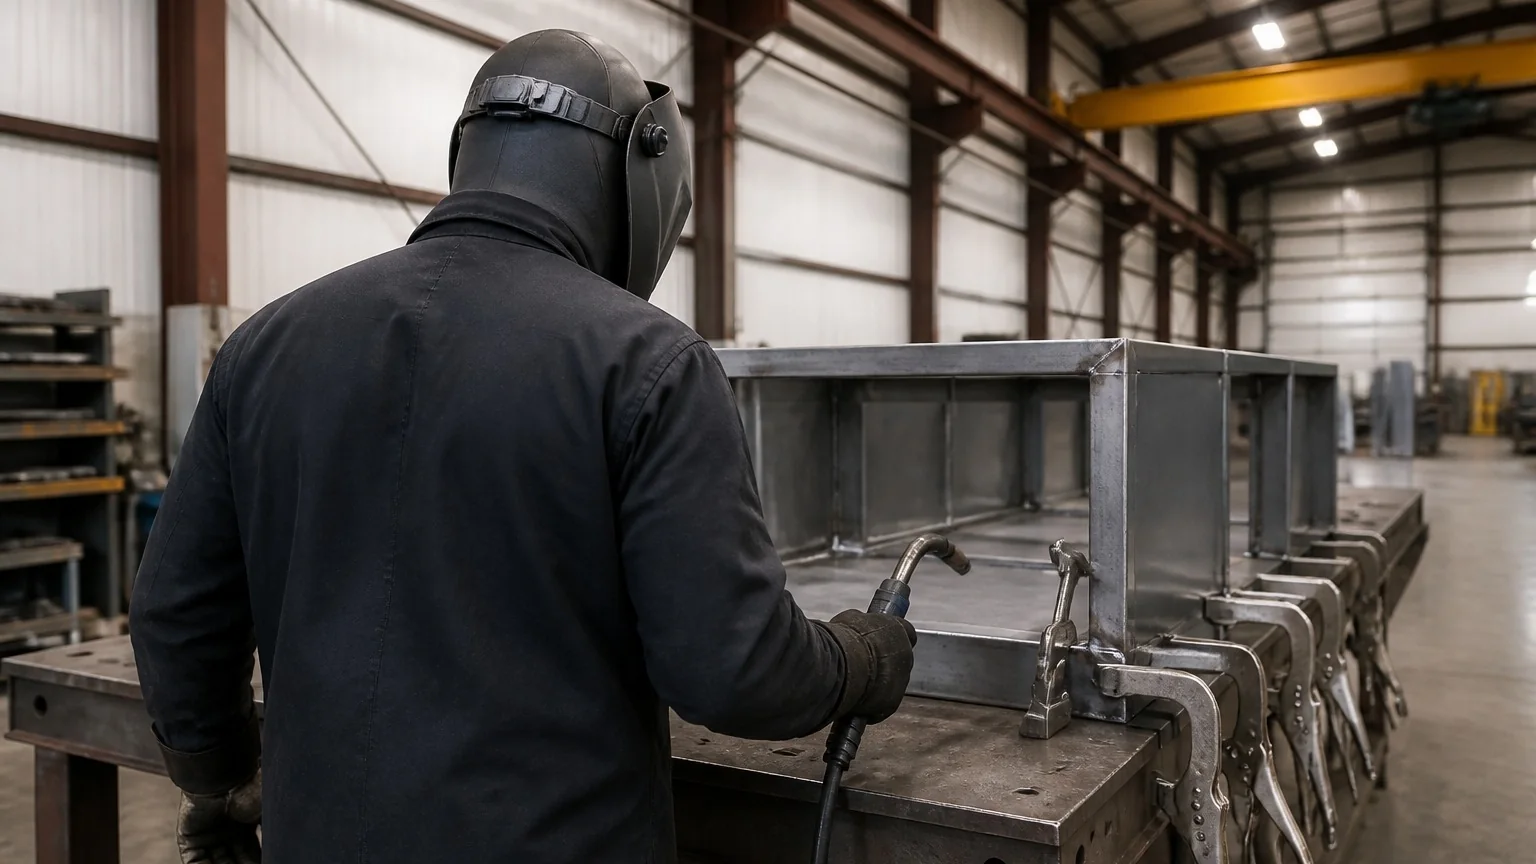
Cabinet frames, enclosure bodies and housings to AWS D1.3, fixtured for squareness and flatness.
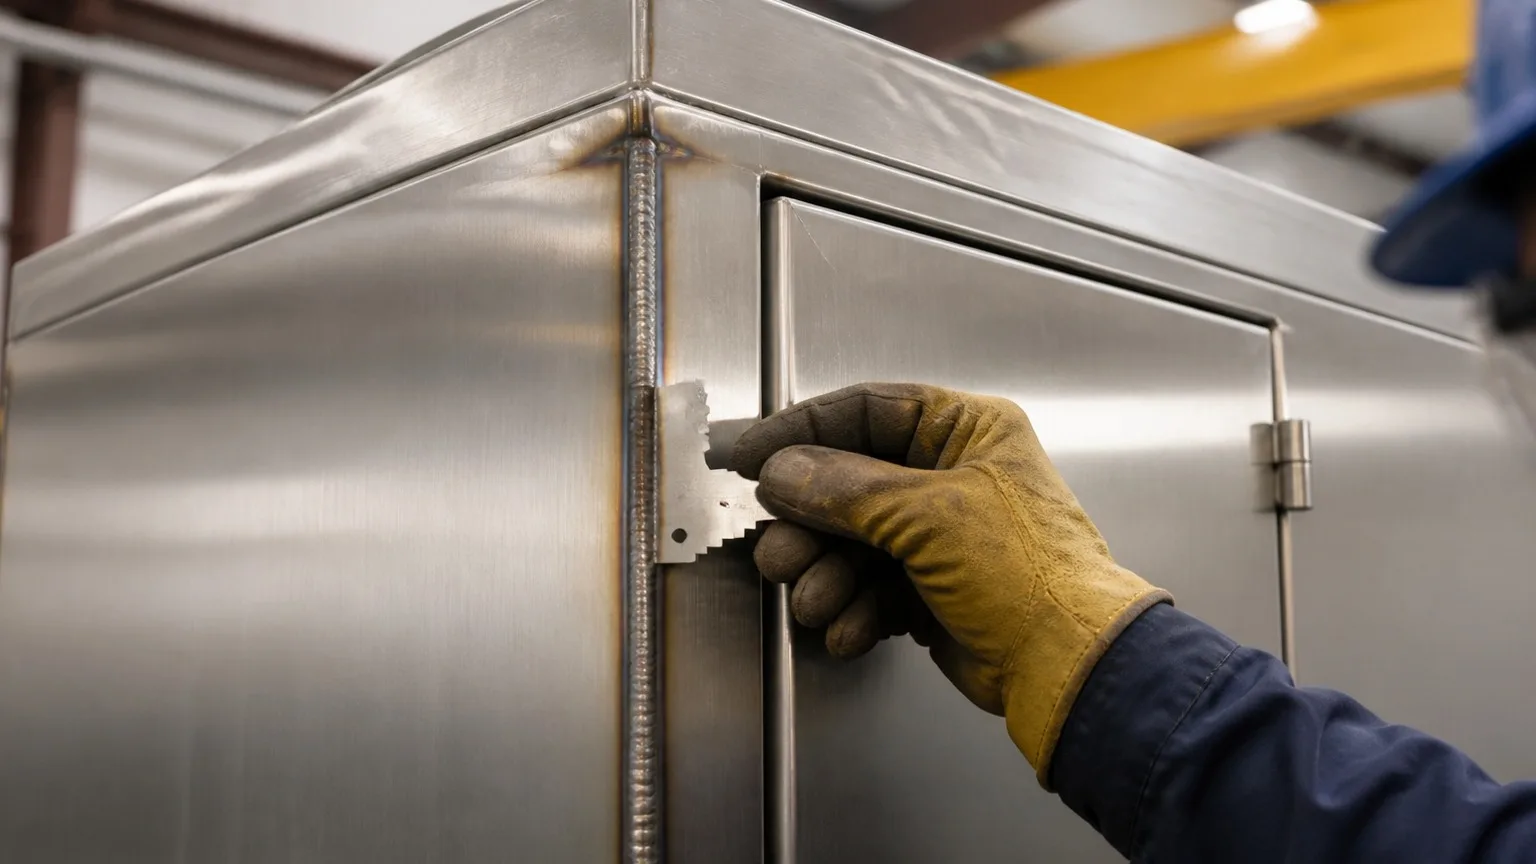
4X enclosures, sanitary conveyors and washdown equipment to AWS D1.6, ground and passivated.
Bus duct and busway housings and aluminum brackets, TIG and pulsed MIG.
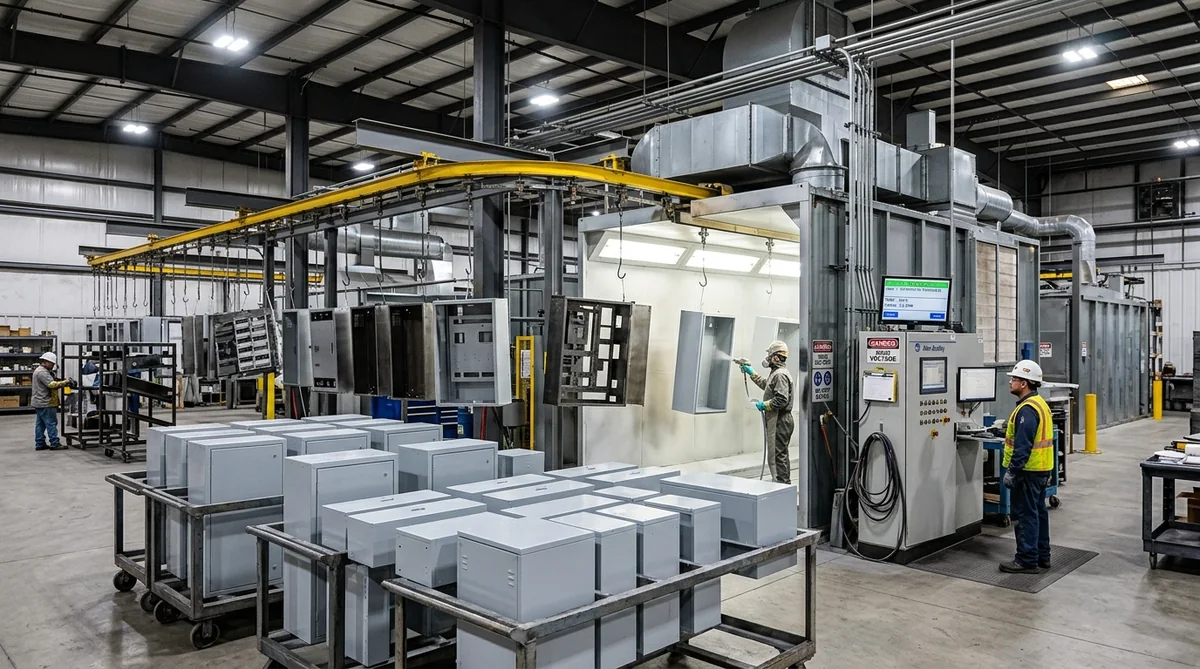
Grinding, dressing and cleaning so welds are ready for blast and powder coat.

Sheet-metal frames and structural members held square before the weld.

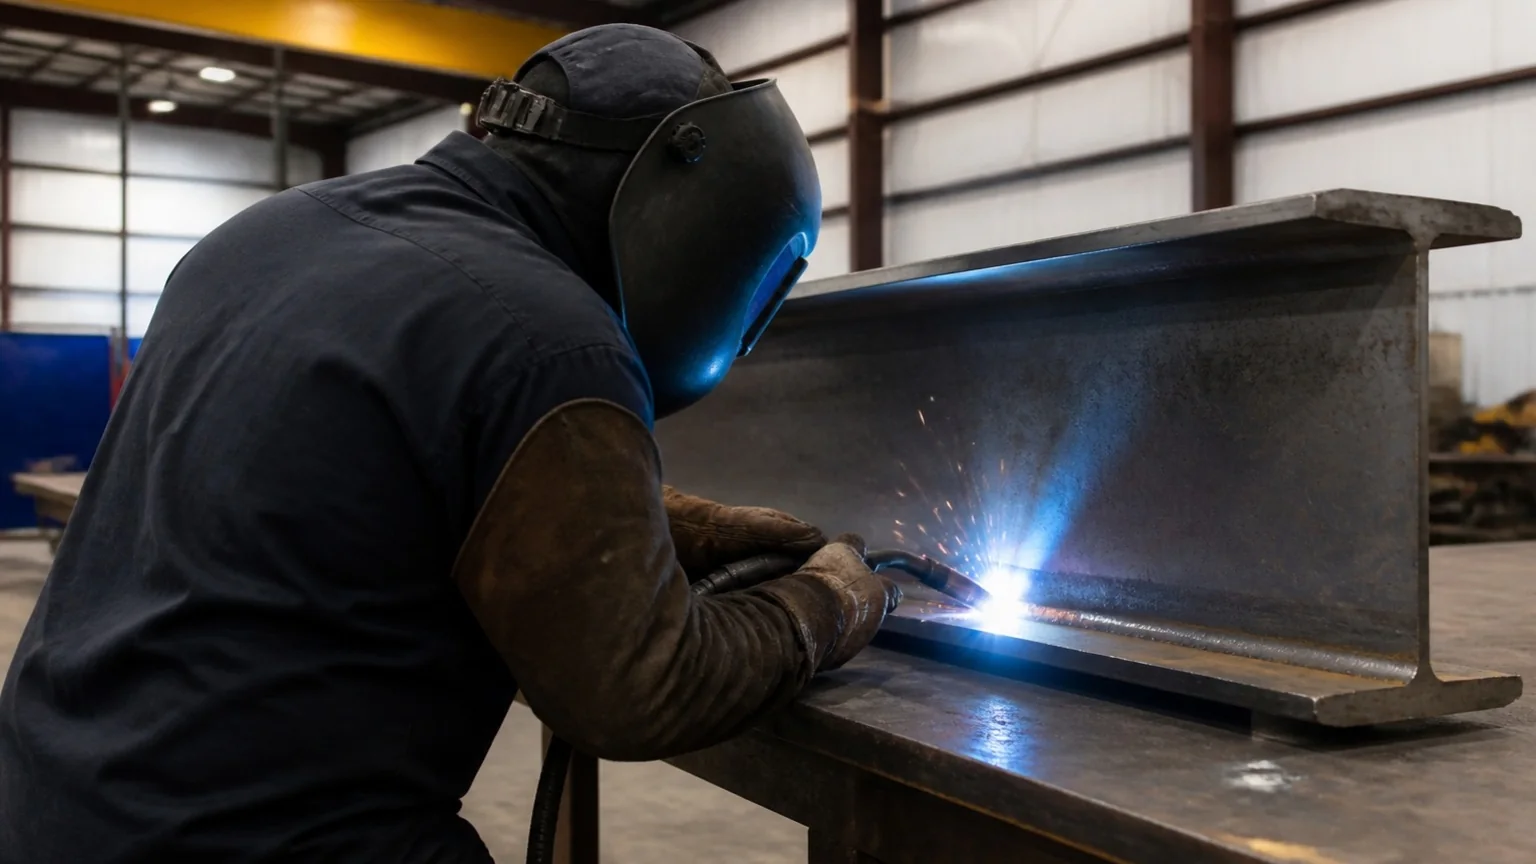
Full-penetration and fillet welds on positioners and manipulators.

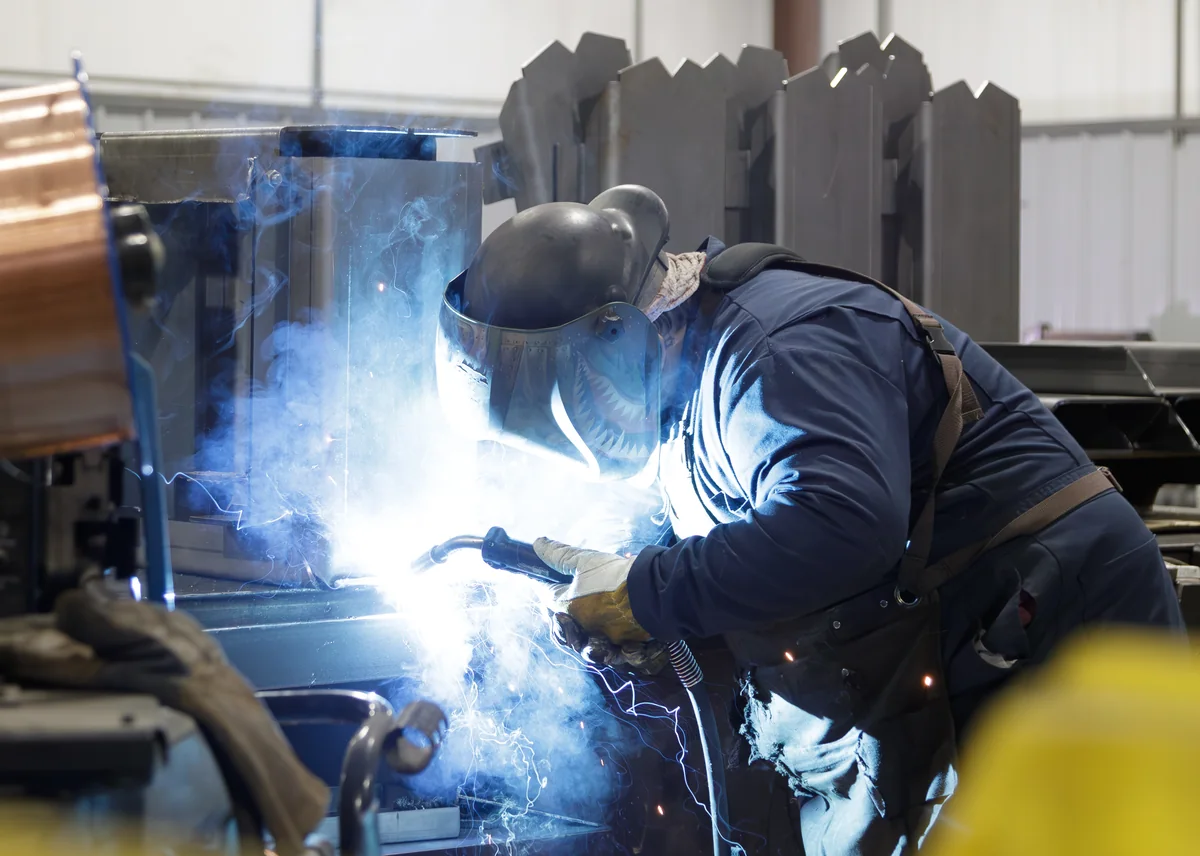
Clean seams on enclosures and sanitary work.

Welds dressed for the finish, then to blast and powder coat.

Everything FabTek builds passes through a MIG or TIG cell: substation structures, transformer tanks, switchgear and transformer cabinets, bus duct, conveyor systems and data center steel. Contract weldments to customer drawings are welded in the same cells to the same records.
| Processes | GMAW (MIG) including pulsed MIG; GTAW (TIG); FCAW and SMAW where specified |
|---|---|
| Power sources | Miller and Airgas Deltaweld 450/500-class MIG cells, TIG cells, Miller Trailblazer for field work |
| Fixturing | Positioners and manipulators for structural and tank weldments; product fixtures for cabinet families |
| Codes | AWS D1.1, D1.3, D1.6; customer WPS on request |
| Materials | Carbon steel, galvanized and galvanneal, stainless (separate cell), aluminum |
| Inspection | Visual and dimensional by weldment; leak test on tanks; NDT through partners where specified |
| Documentation | Welder IDs, WPS/PQR, inspection records; ISO 9001:2015 |
| Also specified as | MIG welding services, TIG welding services, GMAW, GTAW, contract welding, stainless steel welding, aluminum welding, structural welding services |
Representative capabilities — exact ranges, ratings, and finishes are confirmed per project. Send drawings for a firm quote.
A heavy structural joint welded overhead is slower and harder to make sound than the same joint rolled to the flat position. FabTek's structural cells use positioners and manipulators to rotate dead-end members, pole shafts and tank bodies so each joint is welded in the position the procedure was qualified for. It is a small thing that shows up in every inspection record, and it is why a full-penetration weld on a FabTek structure looks the same at the top of the member as at the bottom.

Built at four production sites in Hazlehurst, Mississippi.
ISO 9001:2015 quality management, AWS-certified welding, OSHA-compliant facilities.
In-house powder coat backed by an IEEE 2000-hour salt-spray certification.
Reserved-line capacity and the automation to grow with your volume.
MIG is faster and suits structural steel, tanks and cabinet frames; TIG gives finer control for stainless, aluminum and thin material where appearance and heat input matter. We choose from the drawing and the code; both are available in every cell.
FabTek Industries keeps a dedicated stainless cell with its own tooling and abrasives at its Hazlehurst, Mississippi plants, alongside carbon-steel structural and sheet-metal cells.
Yes — qualified to AWS D1.1, D1.3 and D1.6 as the work requires, with written procedures and welder IDs recorded on every weldment.
Yes. Aluminum bus duct and busway housings and brackets are welded by TIG and pulsed MIG in the sheet-metal cells.
Explore related lines: Substation structures · Transformer tanks · NEMA 4 & 4X enclosures · Bus ducts & busways
Further reading: AWS D1.1 vs D1.3 vs D1.6 · ISO 9001 and AWS-certified welds · Steel, stainless and aluminum in fabrication


Have weldments to quote? Send the drawings and the code — we'll come back with a plan and a firm price, typically within one business day.