Fiber laser for sheet, robotic plasma for beams, water-table plasma and waterjet for plate, a drill line and angle line for structural — every cutting process a power-system fabrication needs, under one roof in Hazlehurst, Mississippi.
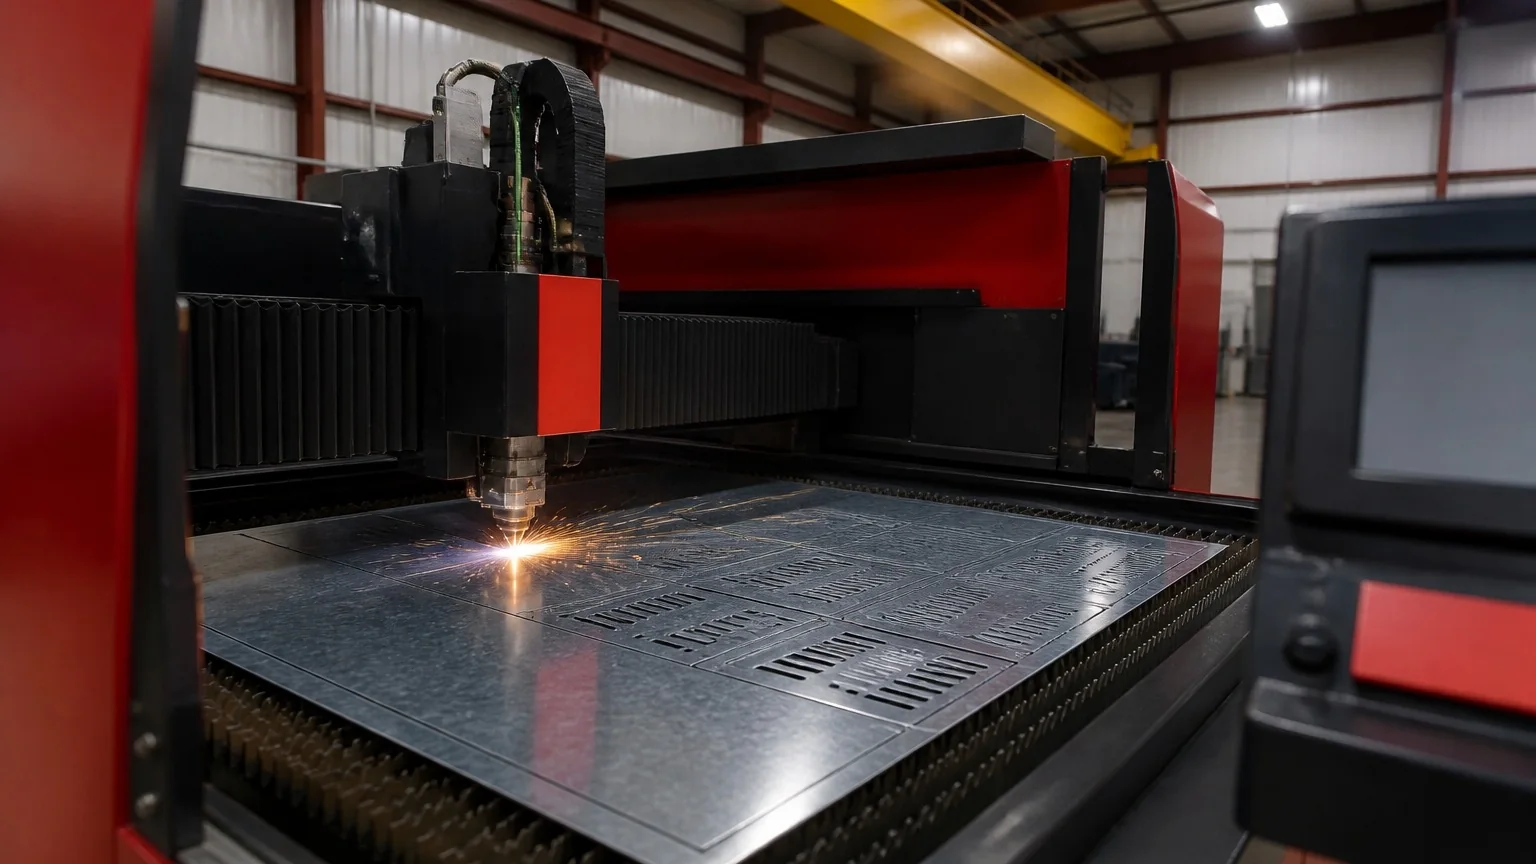
No single machine cuts everything well. Thin sheet for cabinets and panels wants a fiber laser. Wide-flange beams for substation structures want a robotic plasma coper that cuts, copes and marks in one pass. Heavy plate wants a water-table plasma or, when heat can't be tolerated, an abrasive waterjet. Angle and channel want a dedicated angle line; structural drilling wants a multi-spindle drill line rather than a mag drill and a tape. FabTek runs all of them, so the cut is chosen for the part rather than for whatever machine happens to be free.
That range is what lets one shop fabricate a transformer cabinet, a bus duct housing and the substation structure they all bolt to. Programs are nested from our engineering group's flat patterns and shop details, cut parts flow to forming, welding and finishing on the same floor, and every piece carries the heat number it was cut from. For OEMs, EPCs and data center developers, that means one purchase order covers sheet-metal and structural scopes that most fabricators would split between two suppliers.
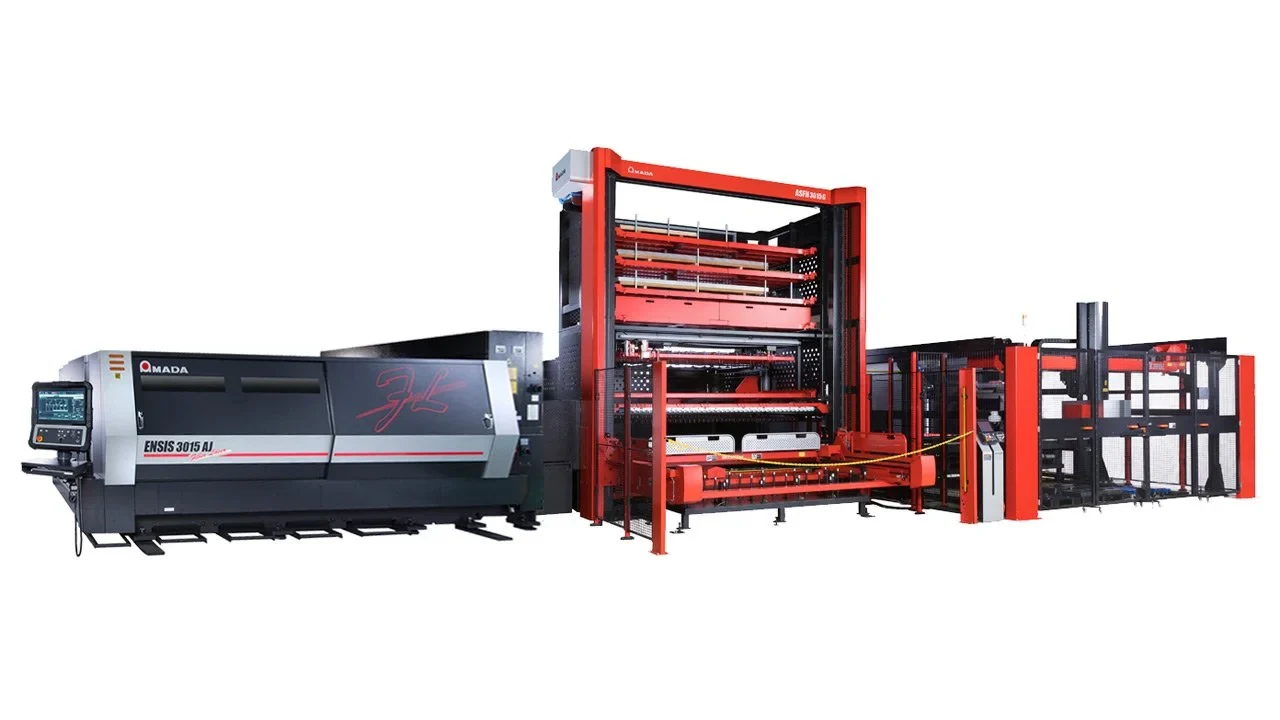
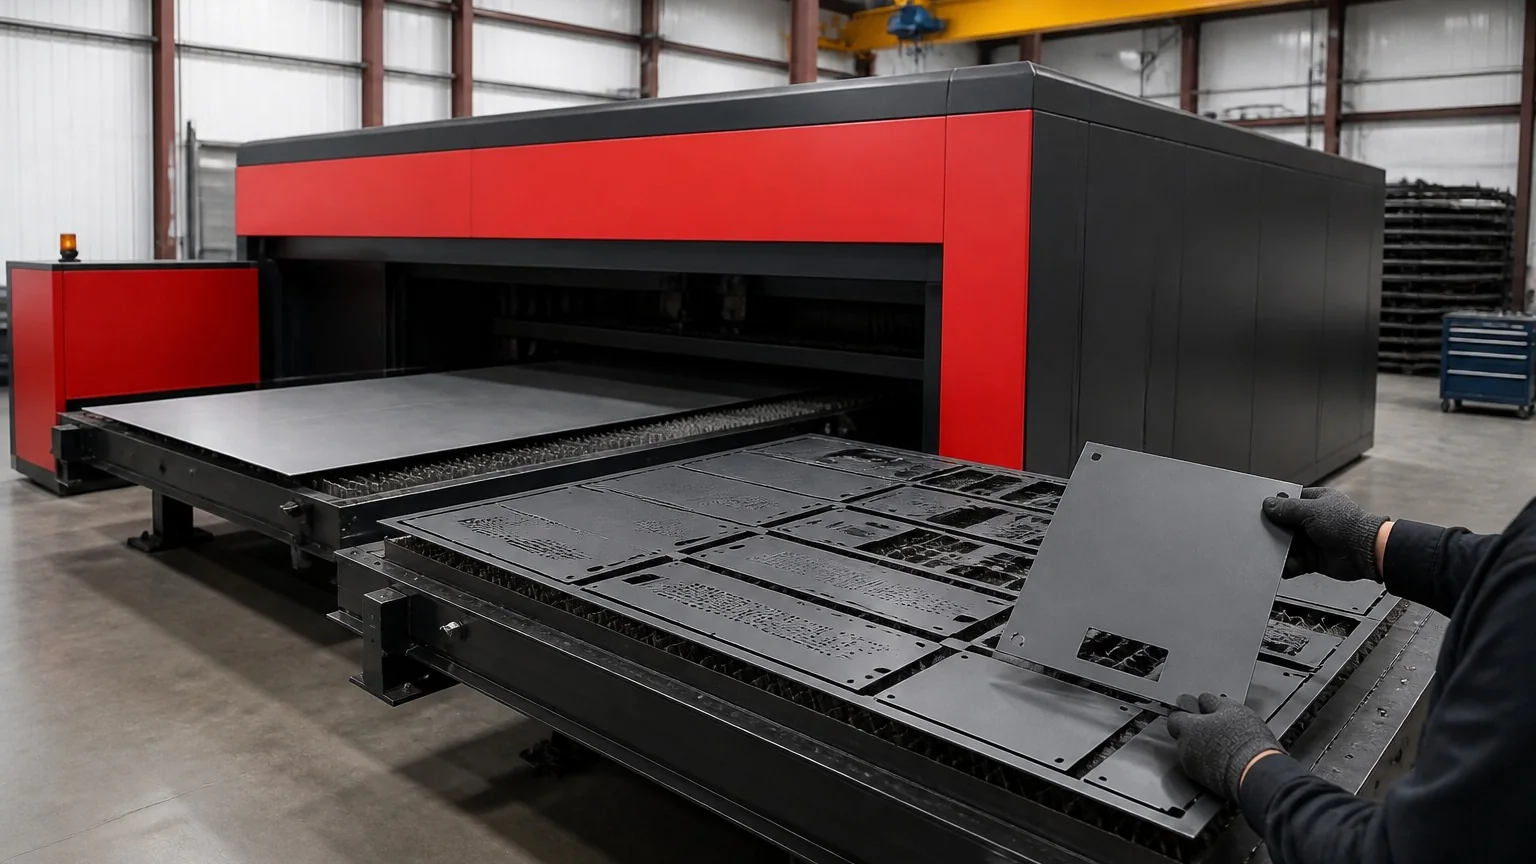
Sheet and thin plate for cabinets, enclosures, panels and bus duct housings, cut on an Amada ENSIS 3015 AJ with a dual-shuttle table and two additional lasers.
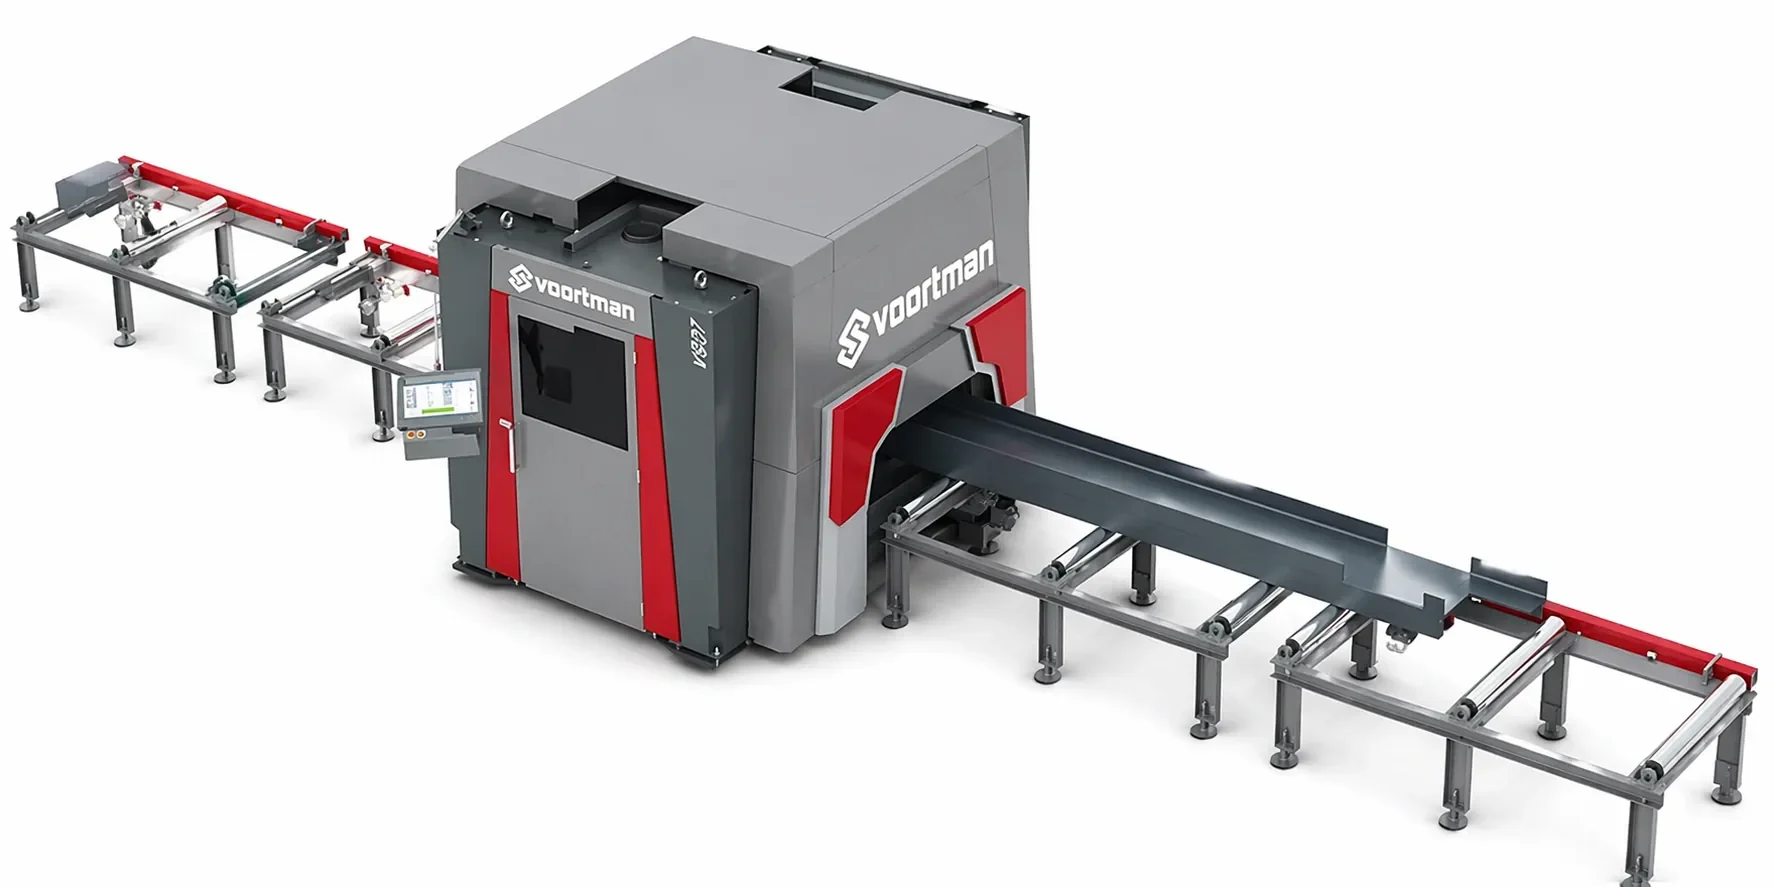
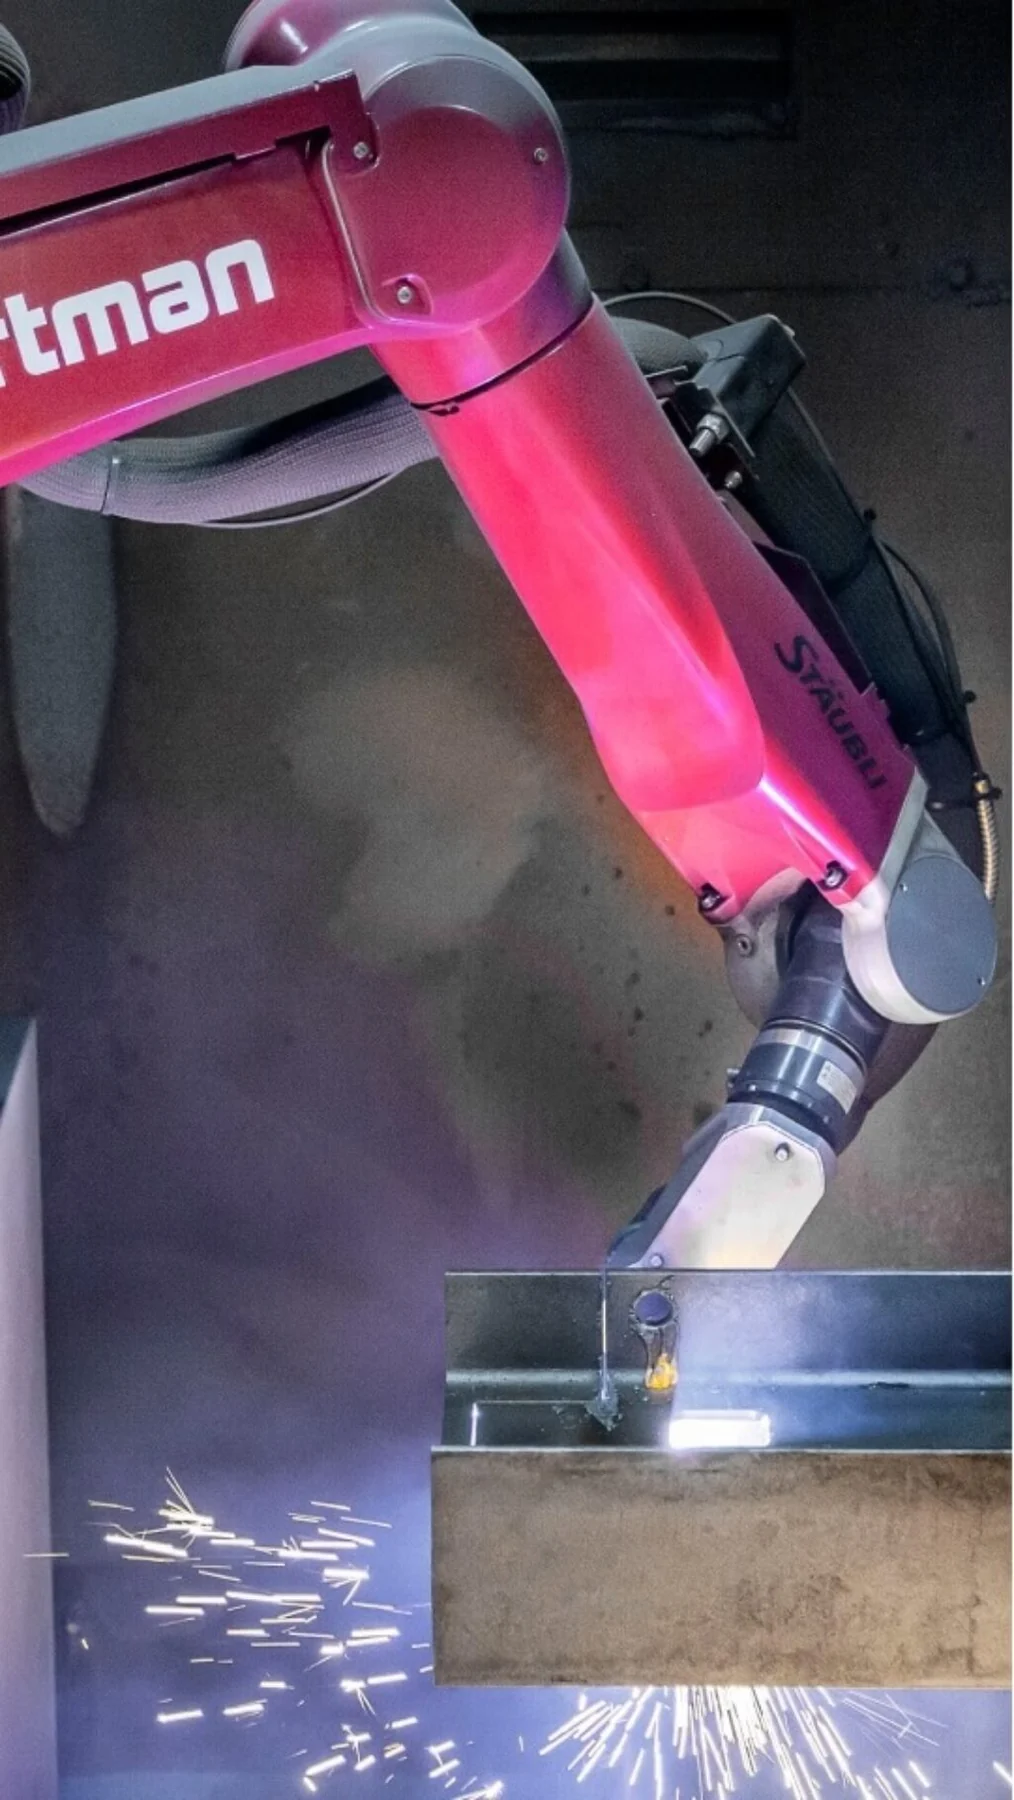
Wide-flange, channel, angle and tube processed on two Voortman V807 seven-axis plasma copers: cuts, copes, holes, marking and bevels in one pass.
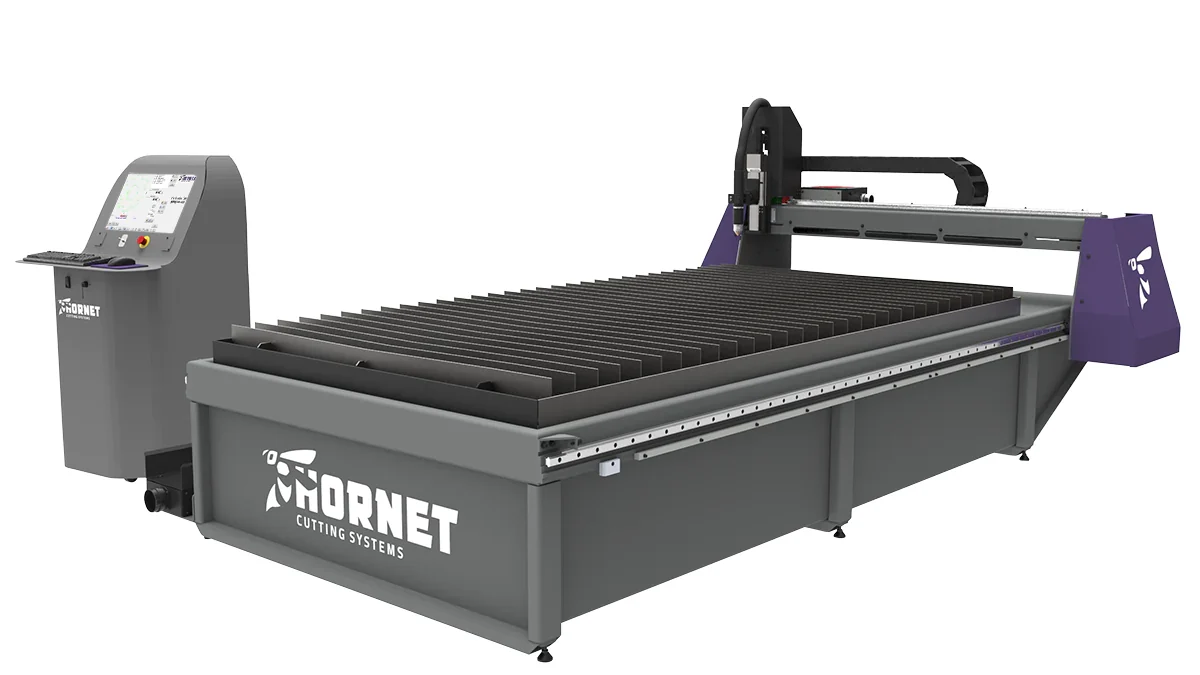
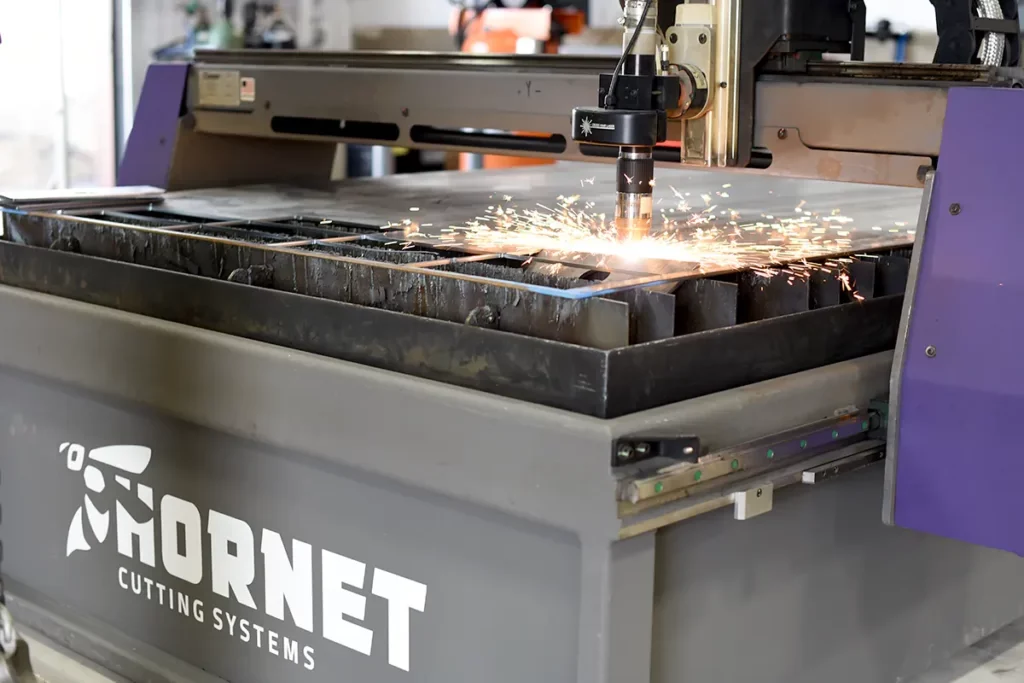
Heavy plate on a 120" × 240" Hornet water-table plasma and oxy-fuel torch for base plates, gussets, tank walls and covers.
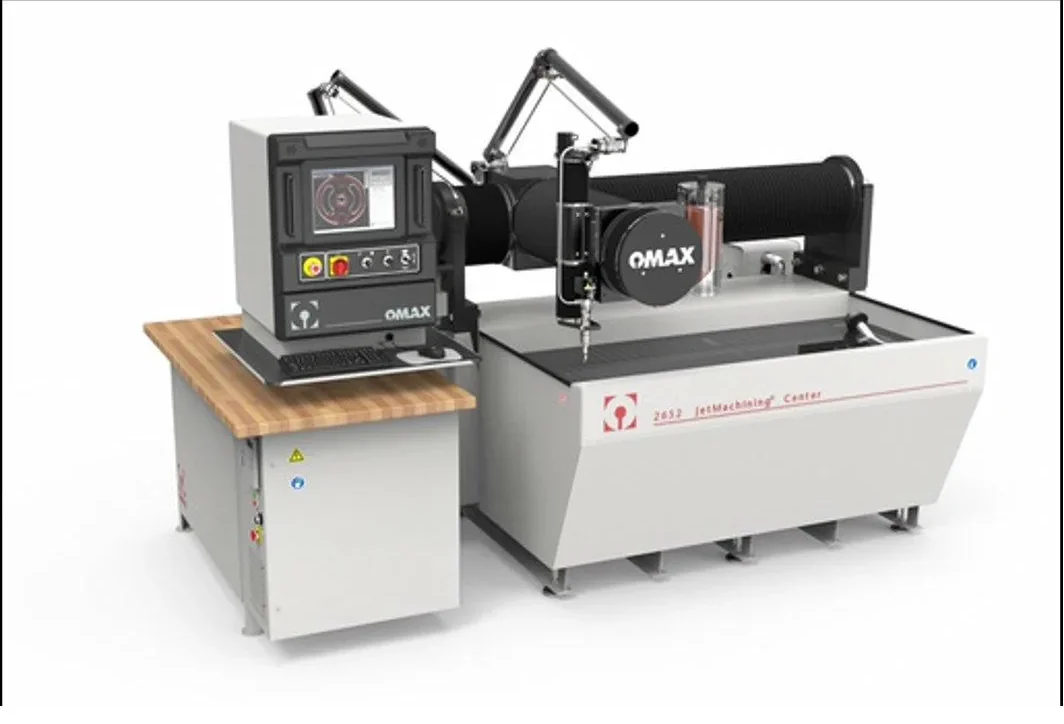
Thick plate, stainless, aluminum and heat-sensitive materials on an OMAX abrasive waterjet with no heat-affected zone.
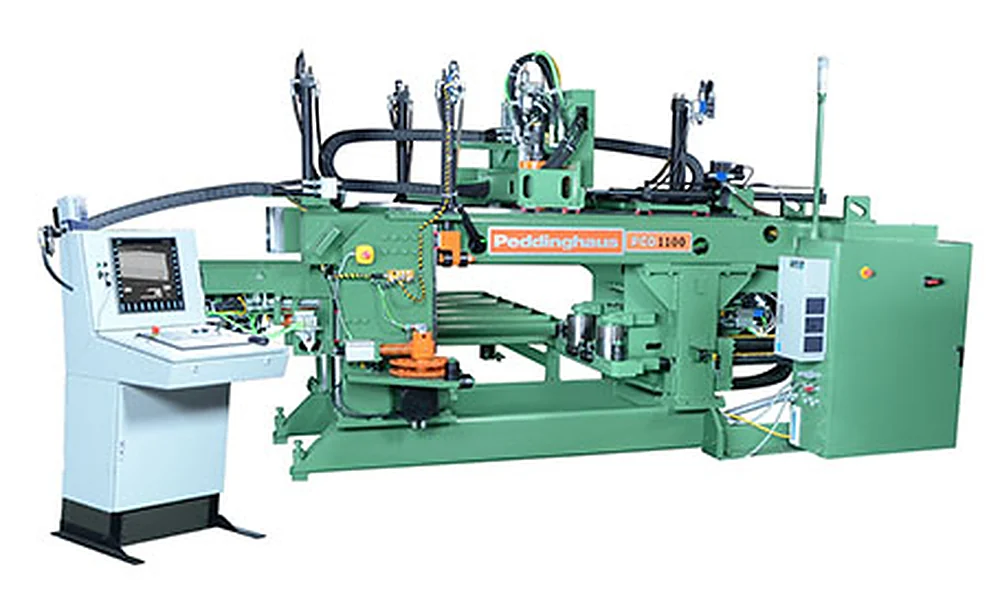
Beams, channels and angles drilled on a Peddinghaus PCD-1100B three-spindle drill line for bolted structural connections.
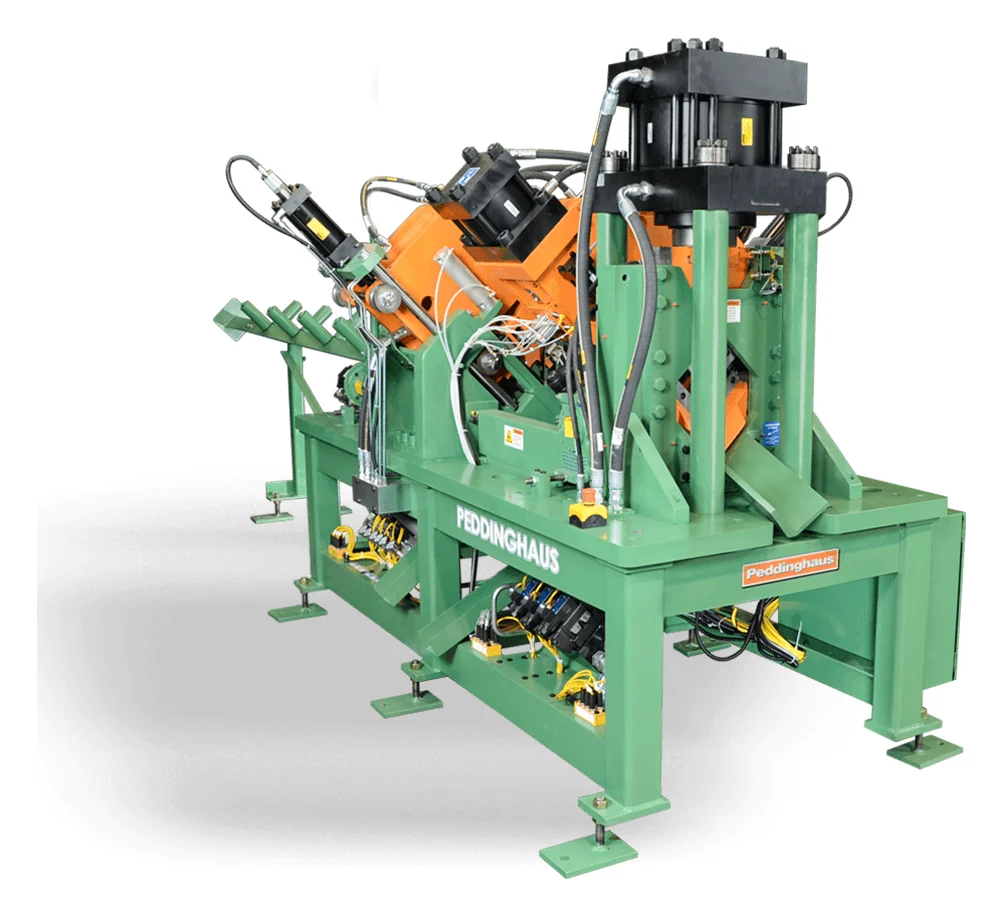
Angle to 5/8" × 6" punched, sheared and marked on a Peddinghaus Anglemaster 643; bar, flat and angle on a Geka Hydracrop 110/A ironworker.
Beams, tube and bar cut to length on a HE&M DC-2038RB1 and supporting saws before drilling and coping.

Amada ENSIS 3015 AJ with dual-shuttle table plus two more cells.
View the machine →
Two Voortman V807 seven-axis copers for structural steel.
View the machine →
Hornet 10' × 20' water-table CNC plasma and oxy-fuel.
View the machine →
OMAX abrasive waterjet — no heat-affected zone.
View the machine →
Peddinghaus PCD-1100B three-spindle drill line.
View the machine →
Peddinghaus Anglemaster 643 and Geka Hydracrop 110/A.
View the machine →
Nests, coper and drill programs come straight from the engineering group's files.

Cabinet, enclosure and panel blanks cut on the Amada ENSIS with a shuttle table.

Beams, channel and angle coped, drilled and marked on the Voortman V807s and the PCD-1100B.

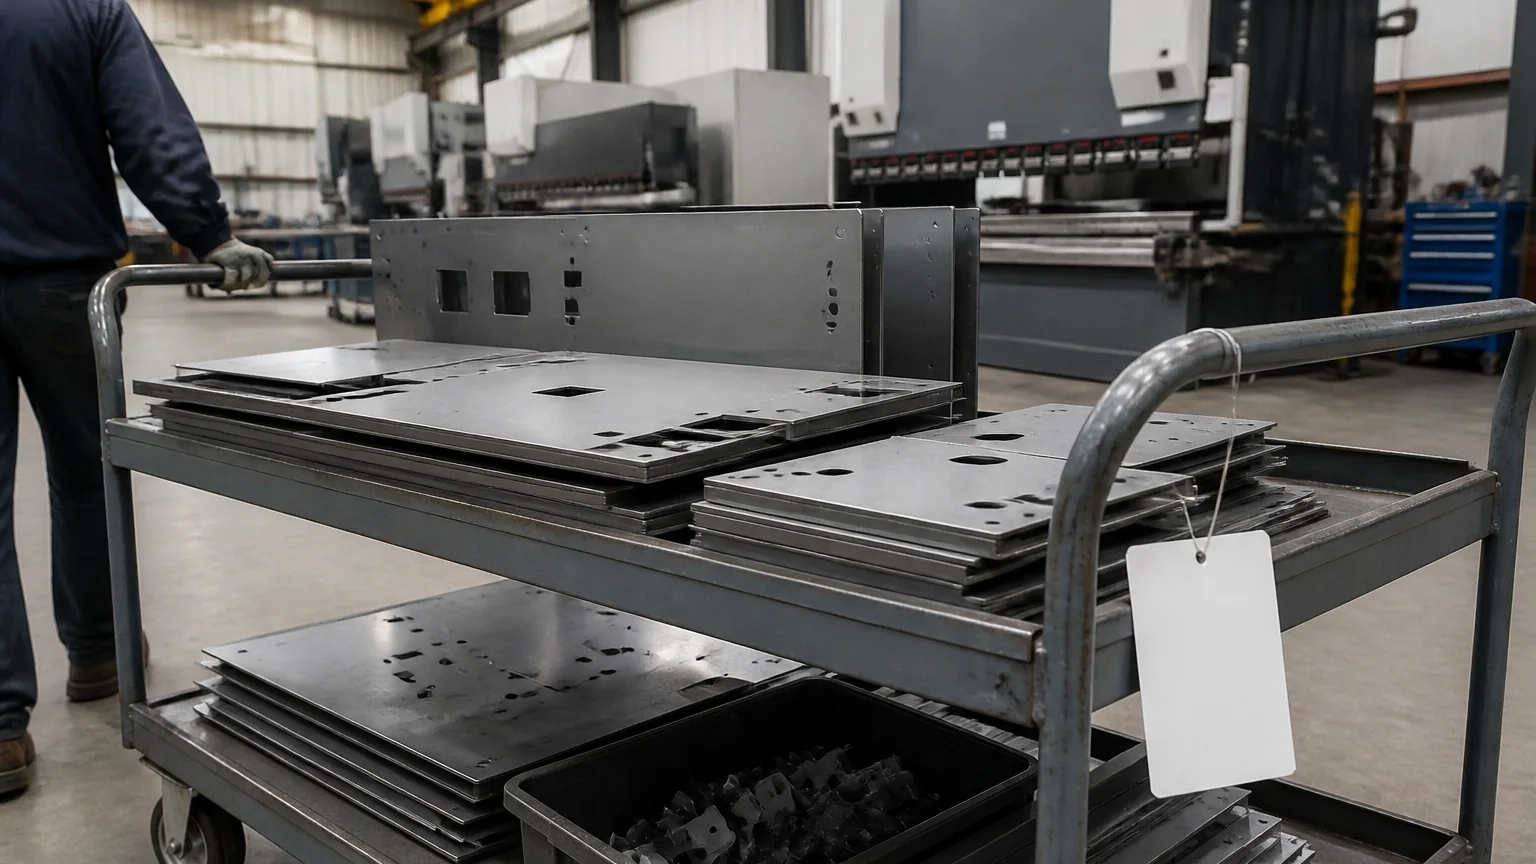
Cut parts move by job number to the press brakes or the welding cells on the same floor.

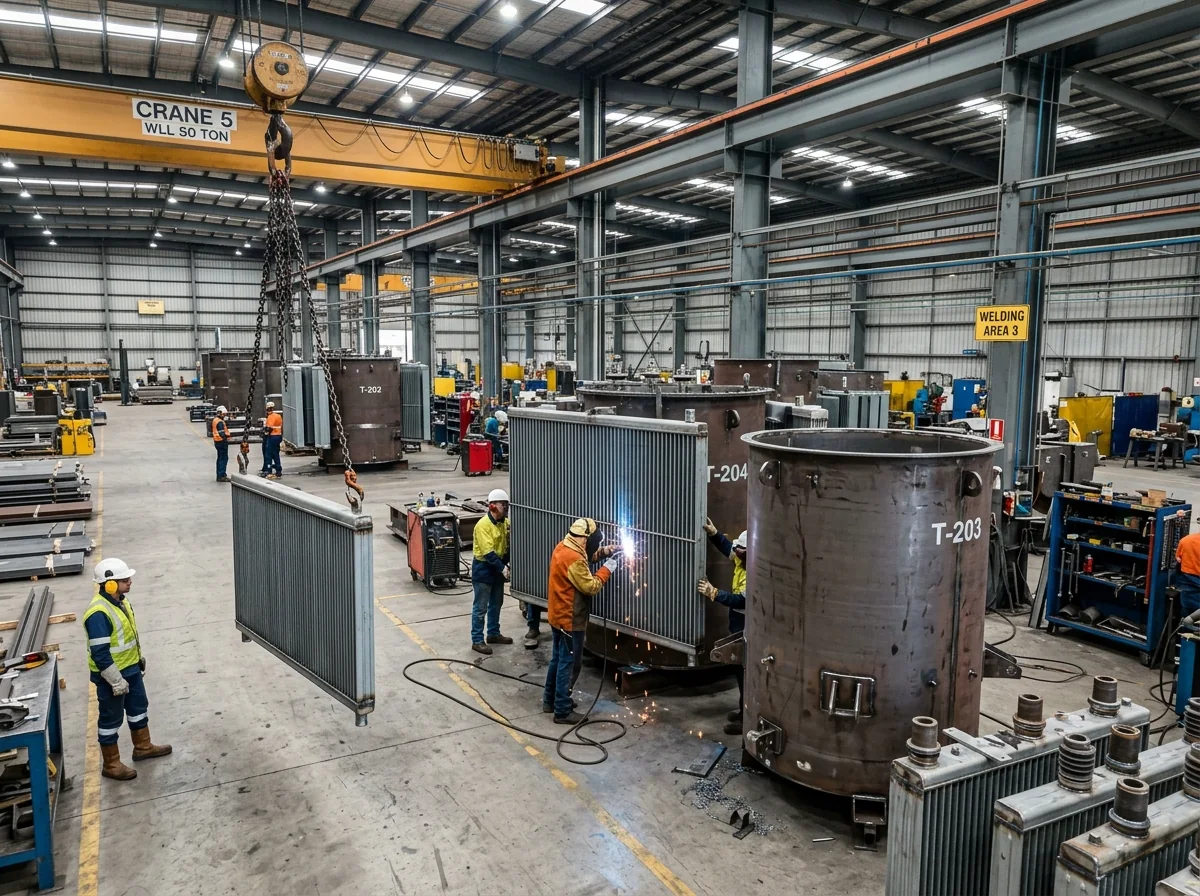
Cabinets, enclosures, switchgear panels and bus duct housings start on the laser. Substation dead-end structures, equipment stands, tubular poles and transmission steel start on the saw, drill line and robotic plasma. Transformer tank walls, covers and base plates come off the plate plasma; stainless conveyor frames, gaskets and heat-sensitive parts come off the waterjet. Cut parts move directly to forming, welding and finishing without leaving the site.
| Fiber laser | Amada ENSIS 3015 AJ with dual-shuttle table; two additional laser cells — sheet and thin plate in carbon steel, stainless and aluminum |
|---|---|
| Robotic plasma | Two Voortman V807 seven-axis plasma copers — wide-flange, channel, angle, HSS and pipe |
| Plate plasma / torch | Hornet 120" × 240" water-table plasma and oxy-fuel |
| Waterjet | OMAX abrasive waterjet — thick plate, stainless, aluminum, no heat-affected zone |
| Drill line | Peddinghaus PCD-1100B three-spindle high-speed drill line |
| Angle line | Peddinghaus Anglemaster 643 — angle to 5/8" × 6" |
| Ironworker | Geka Hydracrop 110/A — punching, shearing, notching |
| Sawing | HE&M DC-2038RB1 (36" capacity) and supporting horizontal band and mitre saws |
| Programming | Nested from FabTek engineering's flat patterns and shop details; DXF, DWG, STEP and IFC accepted |
| Traceability | Heat-number tracking from plate and shape through the cut part; ISO 9001:2015 |
| Also specified as | Laser cutting services, plasma cutting services, waterjet cutting, structural steel processing, beam coping, drill line services, angle line processing |
Representative capabilities — exact ranges, ratings, and finishes are confirmed per project. Send drawings for a firm quote.
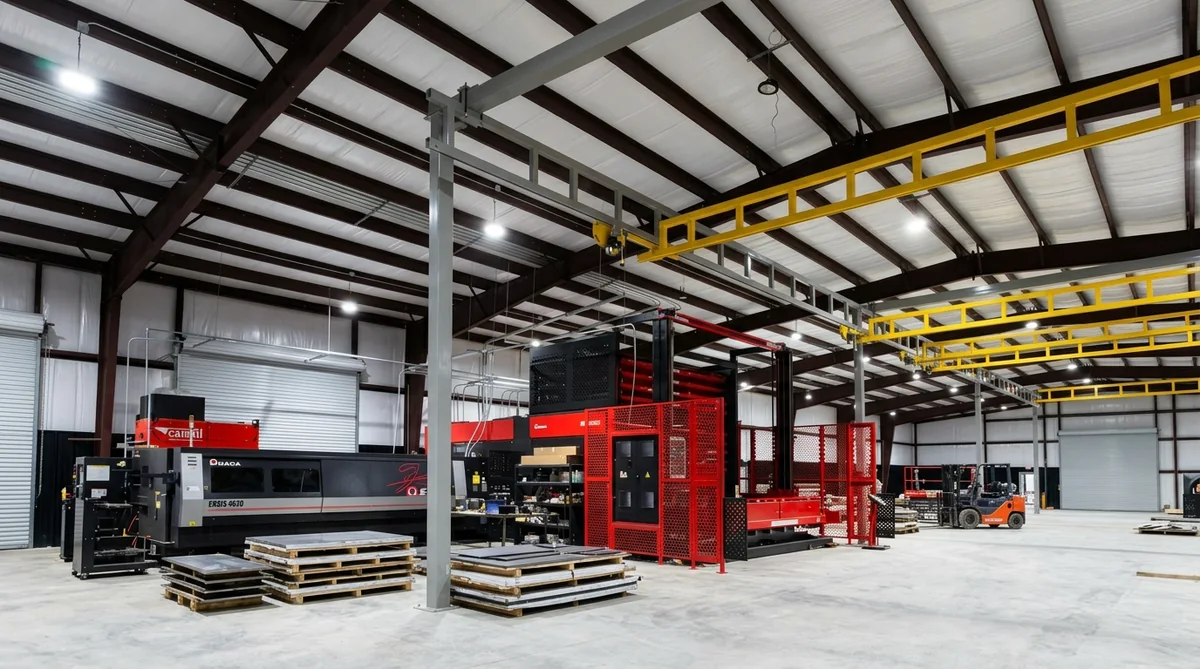
Most cutting shops are one or the other: a sheet-metal house with lasers and press brakes, or a structural house with a drill line and a coper. FabTek runs both because the products we build need both — a transformer cabinet is sheet metal, the pad-mount tank beside it is plate, and the substation structure they sit in front of is structural. Keeping every cutting process in one plant is what lets us quote a whole package, hold one schedule and ship one truck. Our engineering and design group programs every machine from the same drawing set, so a revision reaches the laser and the coper at the same time.

Built at four production sites in Hazlehurst, Mississippi.
ISO 9001:2015 quality management, AWS-certified welding, OSHA-compliant facilities.
In-house powder coat backed by an IEEE 2000-hour salt-spray certification.
Reserved-line capacity and the automation to grow with your volume.
Carbon steel, stainless and aluminum from thin sheet through heavy plate and full structural shapes. Thin sheet runs on the fiber laser, plate on the water-table plasma or waterjet, and beams, channel and angle on the robotic plasma, drill line and angle line. Send the drawing and we will confirm the process.
FabTek Industries runs fiber lasers, two Voortman robotic plasma copers, a water-table plasma, an OMAX waterjet, a Peddinghaus drill line and angle line at its Hazlehurst, Mississippi plants, with forming, welding and powder coat on the same site.
Both. We cut to print for customers who want parts, and we carry the same parts through forming, welding, finishing and assembly for customers who want a finished product.
DXF, DWG, STEP, SolidWorks and Inventor models, and IFC or Tekla exports for structural. Our engineering group nests and programs from your files or details from your drawings.
Explore related lines: Substation structures · Transformer cabinets · Bus ducts & busways · Transformer tanks
Further reading: Metal fabrication machines and equipment guide · Steel, stainless and aluminum in fabrication · The build-to-print spec package


Have parts to cut? Send the files and quantities — we'll come back with the right process and a firm price, typically within one business day.