Two automated powder coat lines — one built for cabinet and panel volume, one with a heavy-duty monorail for tanks, structures and long parts — behind a finish certified to 2,000 hours of salt spray, in ANSI, RAL and OEM-matched colors.
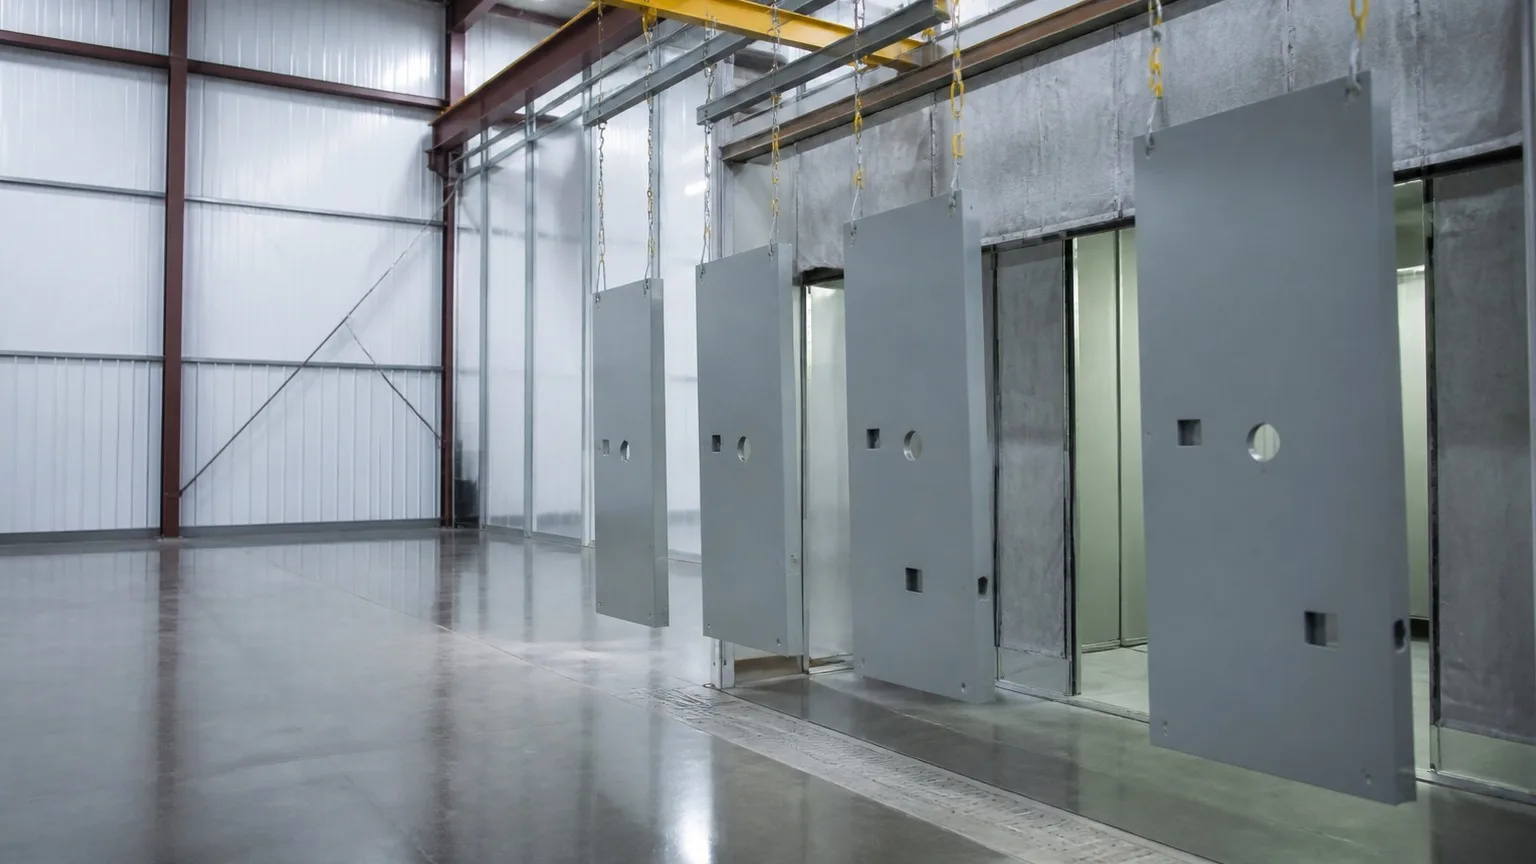
An outdoor cabinet or a transformer tank is judged on its finish for twenty years. Powder coat is the finish FabTek specifies for nearly everything we build because, applied over a blasted and pre-treated surface and cured correctly, it outperforms wet paint on hardness, film build and corrosion resistance. Our line is certified to IEEE's 2,000-hour salt-spray requirement, which is the standard transformer OEMs and utilities write into cabinet and tank specifications.
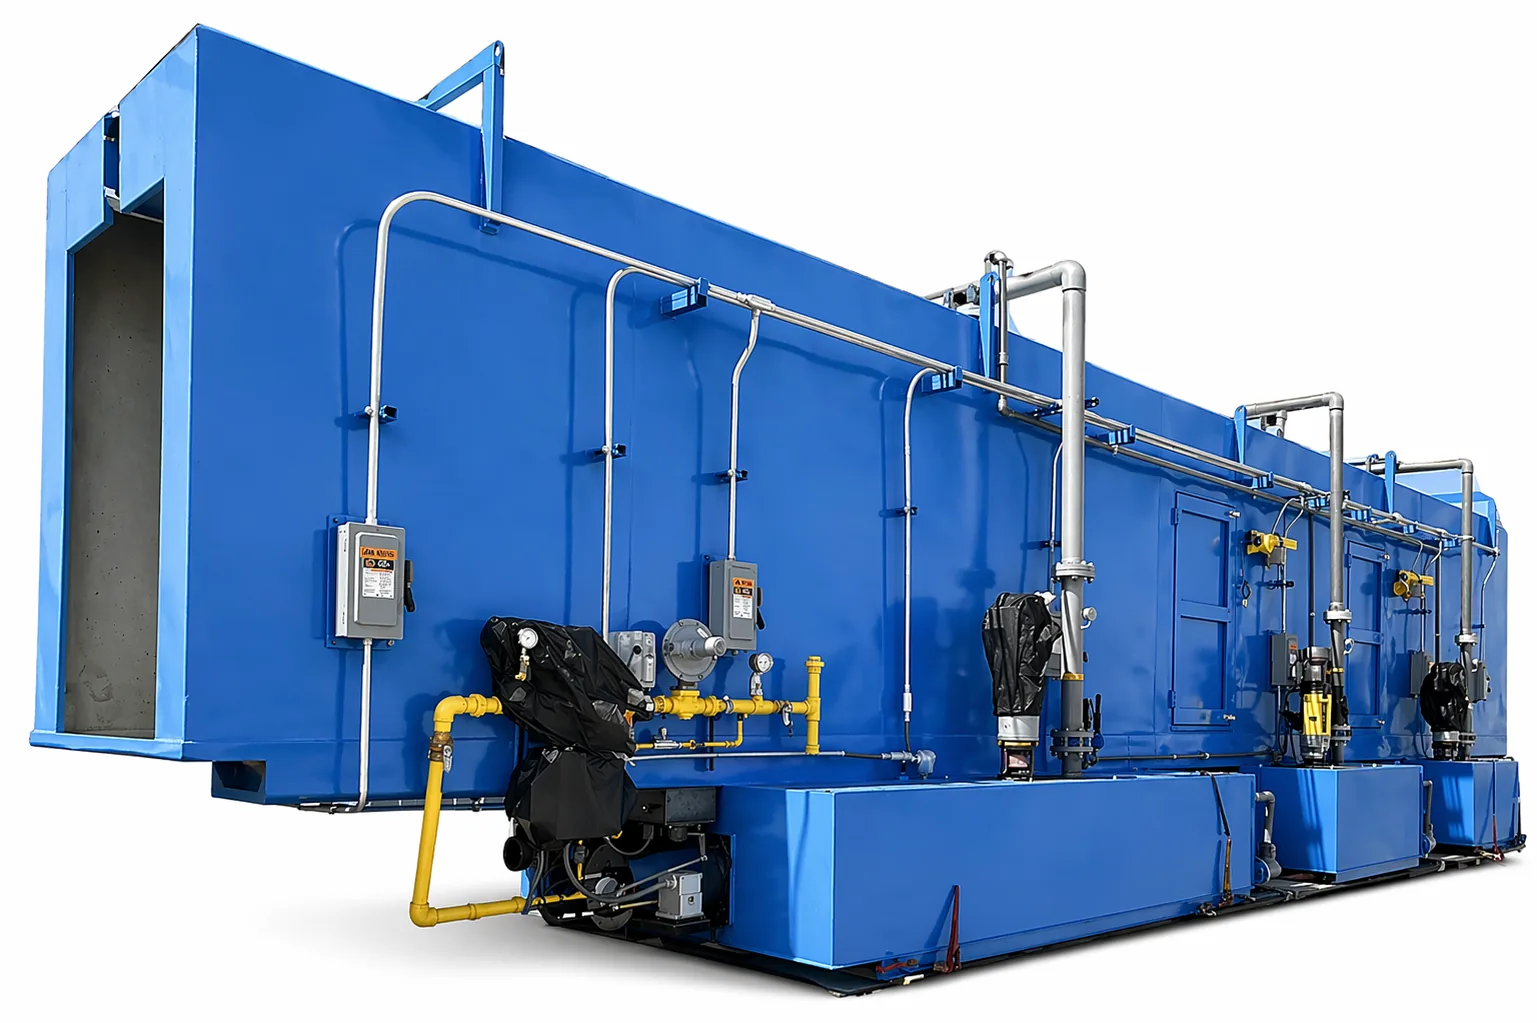
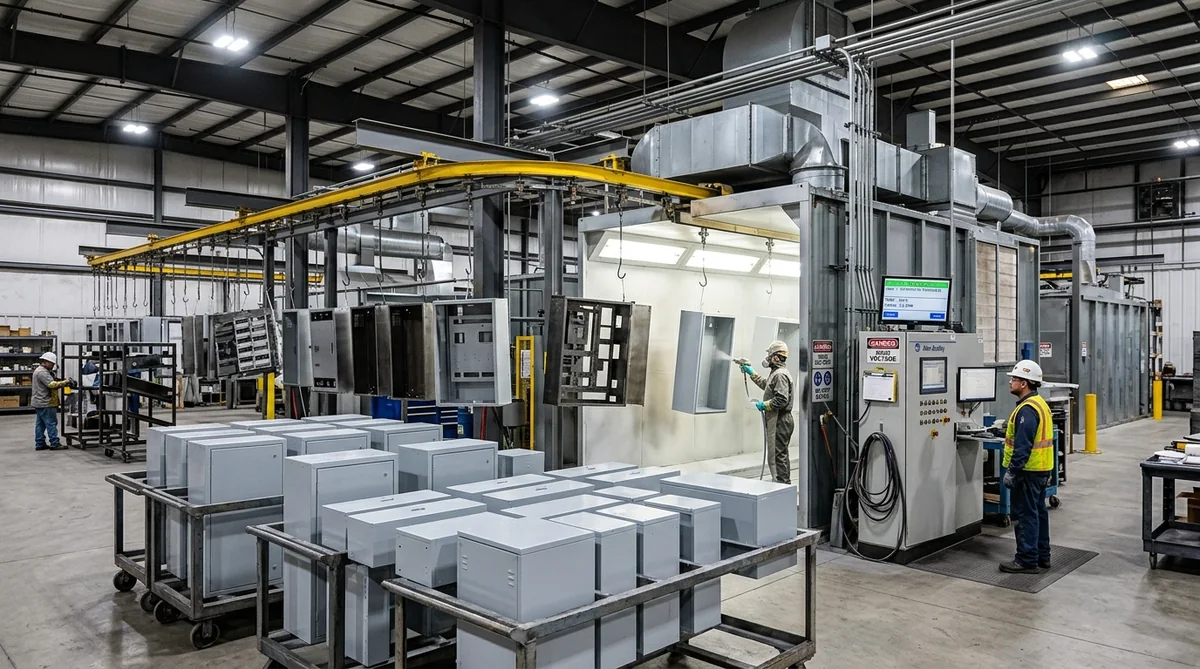
FabTek runs two automated powder coat lines. The first is built for cabinet, panel and enclosure volume — parts move through pre-treatment, a powder primer booth, a powder top-coat booth and cure on a continuous conveyor. The second is a heavy-duty monorail coating system that carries long, heavy parts — tank bodies, structures, busway housings, platform steel — through the same sequence on a track sized for their weight and length. Both feed from the blast room and pre-treatment and both are run and maintained by FabTek's own crew. Powder coat is the primary finish for our products; hot-dip galvanizing is available through partners for structural steel — see hot-dip galvanizing.
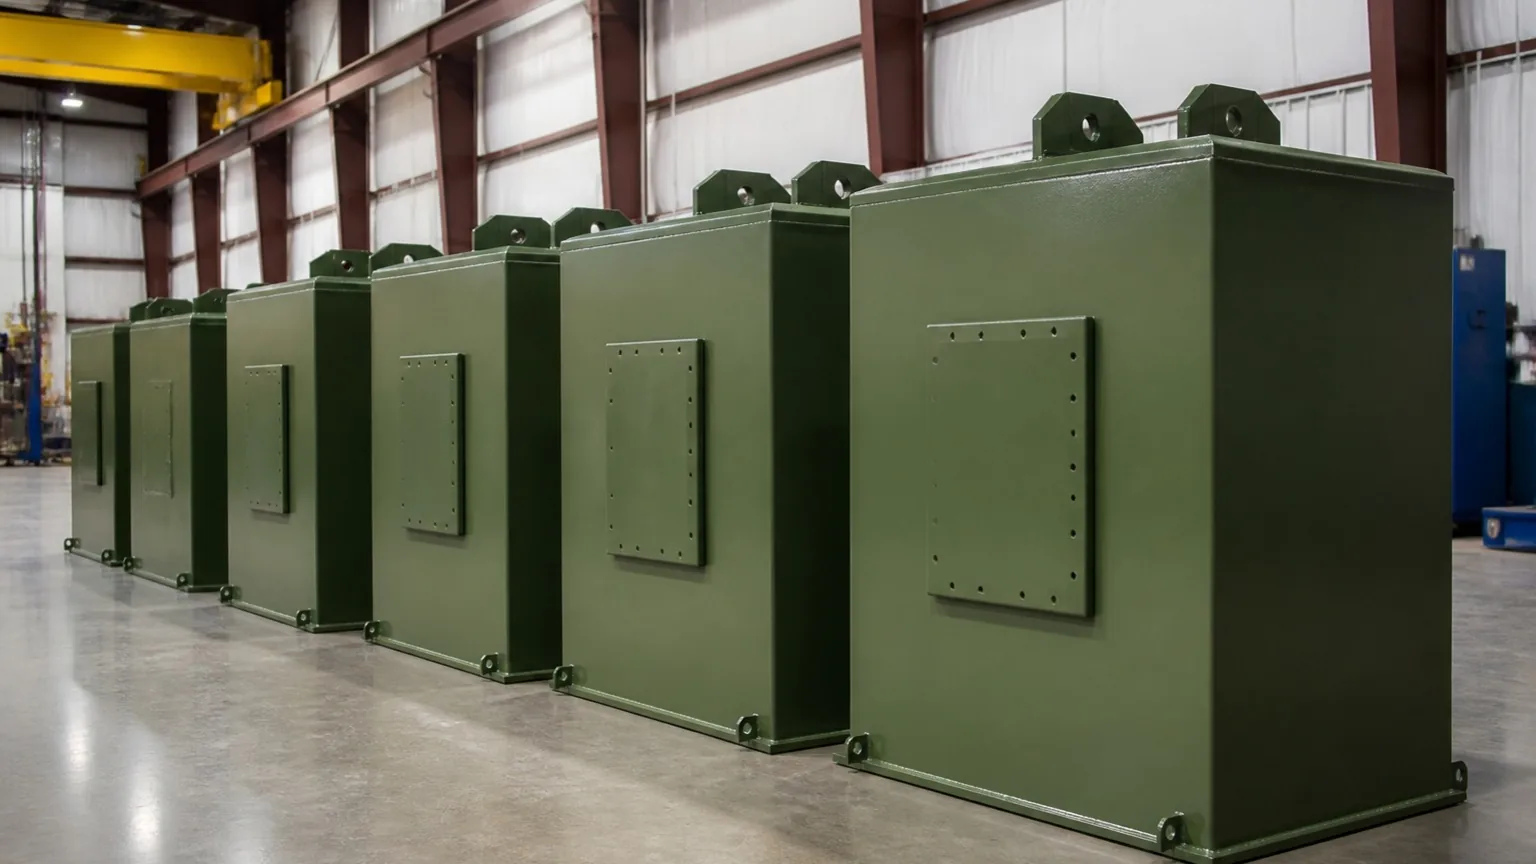
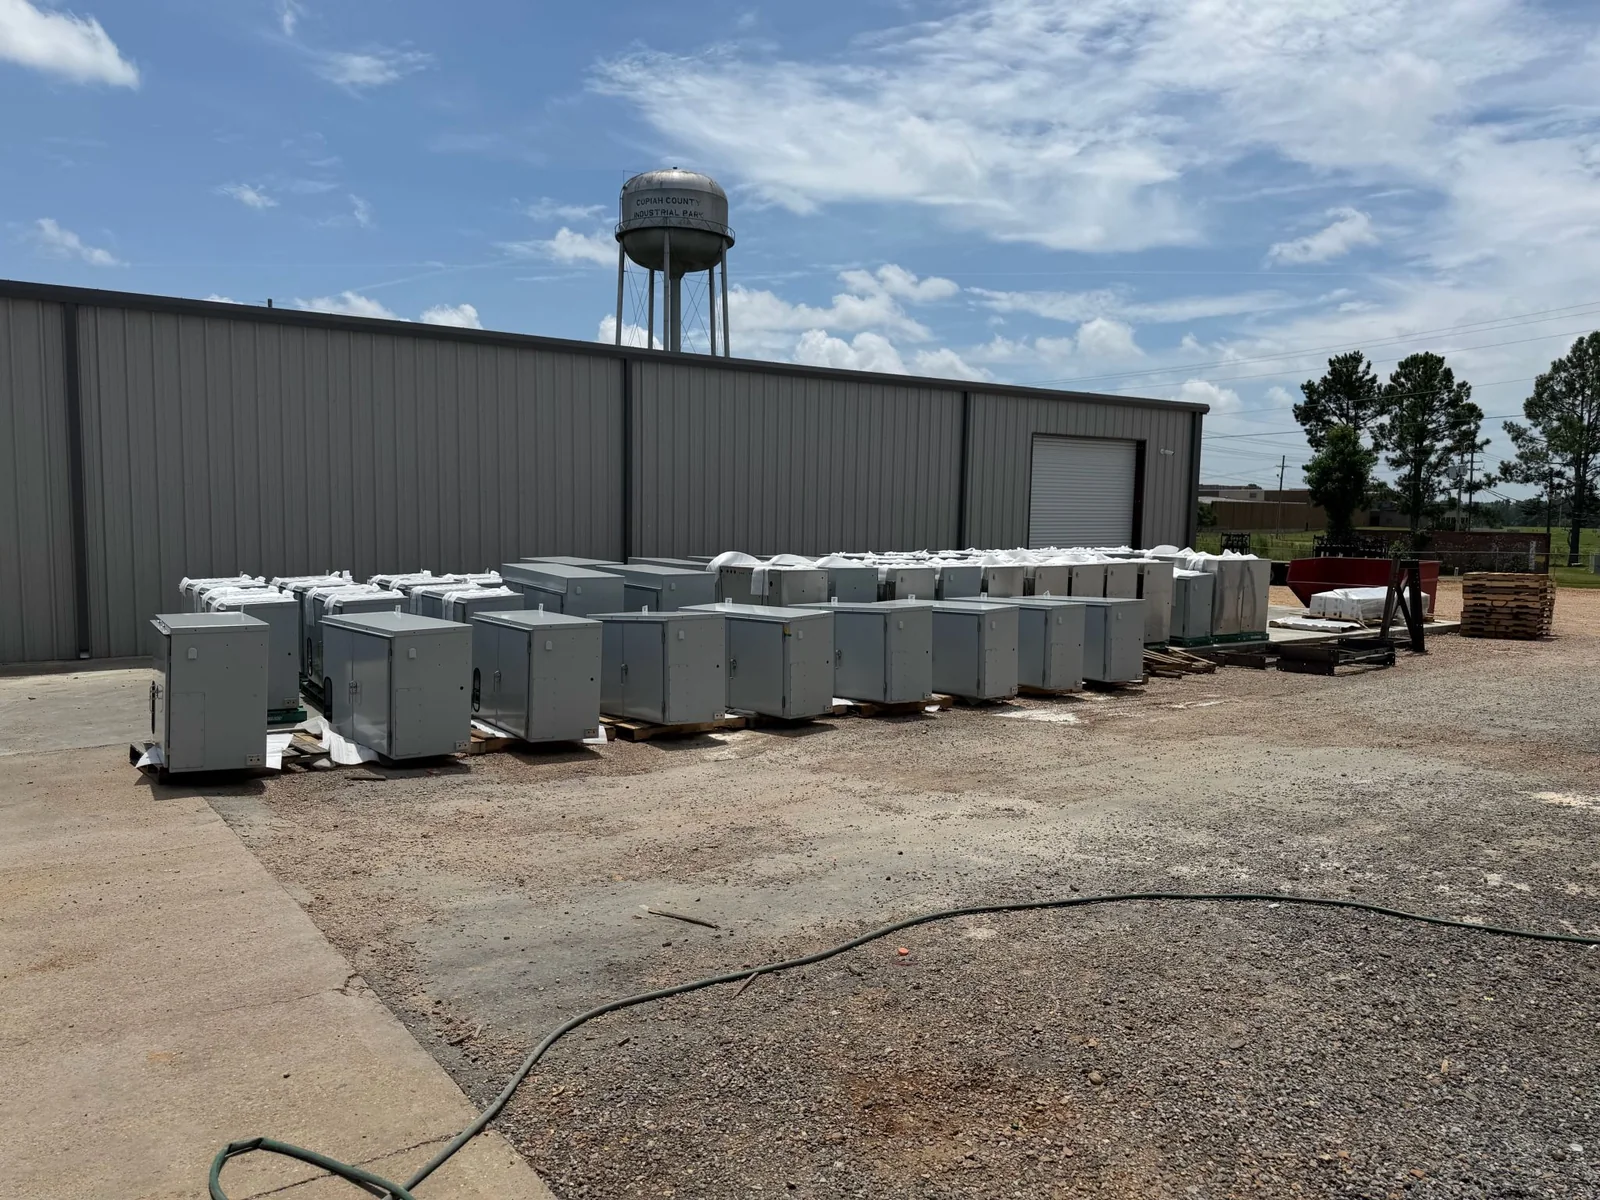
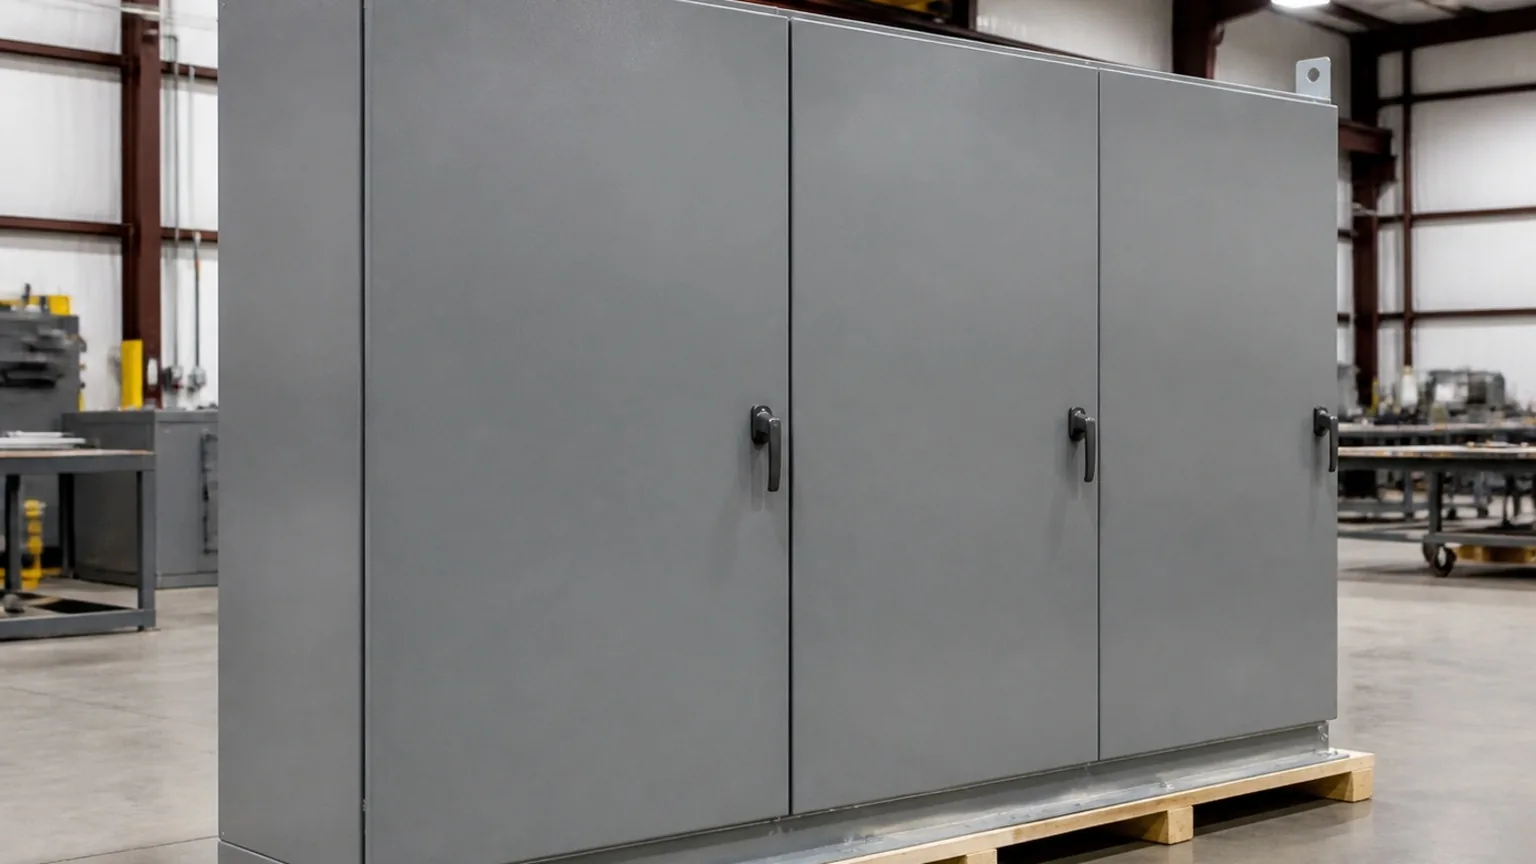
Continuous-conveyor line with primer and top-coat booths for transformer cabinets, enclosures, switchgear panels and housings.
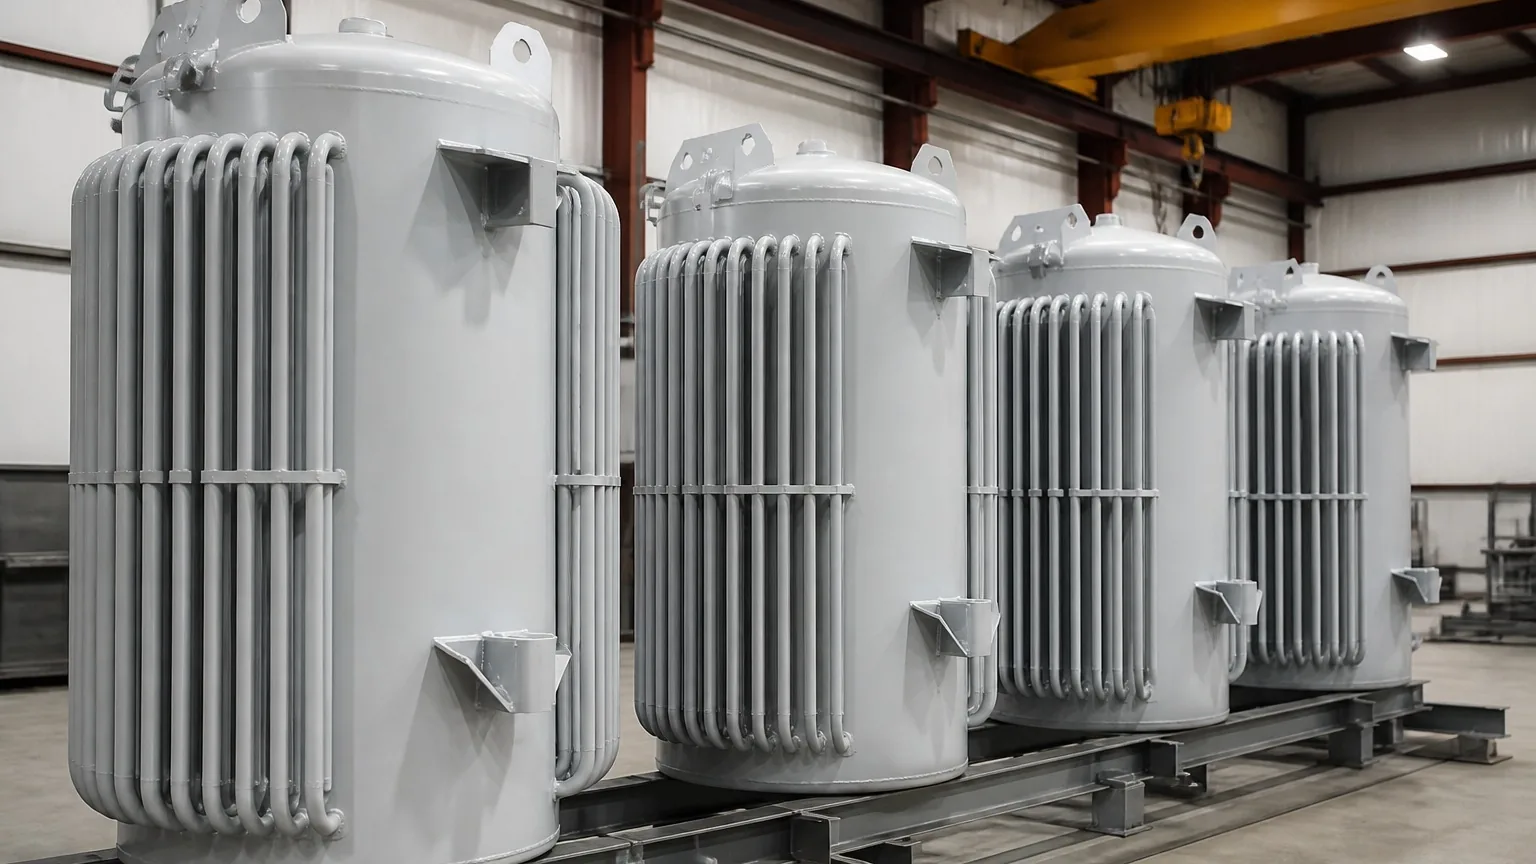
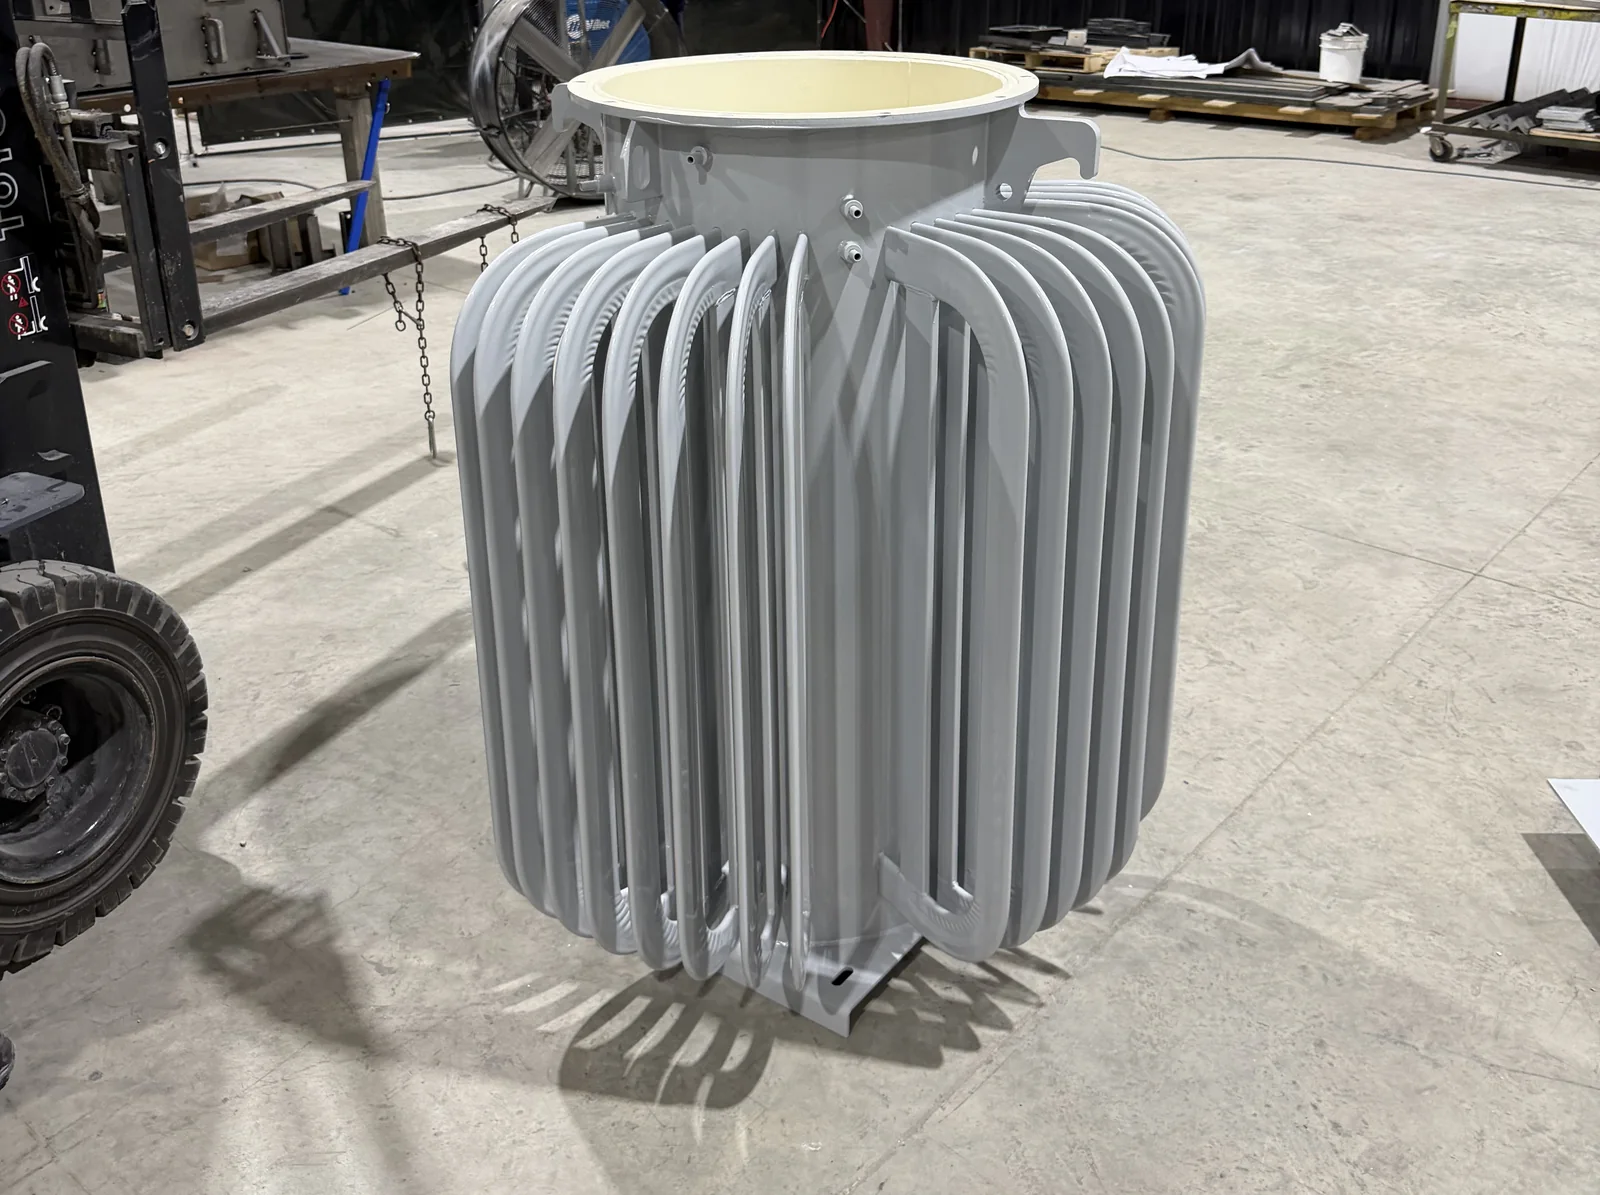
A hanging-track coating system for transformer tanks, structural weldments, long busway housings and platform steel.
Powder primer plus powder top coat for outdoor and corrosive-service parts; single-coat for indoor.
ANSI 61 and 70 grey, Munsell green, RAL and OEM-specified colors, with retained recipes for repeat programs.
Customer-supplied parts blasted, pre-treated and powder coated to spec.

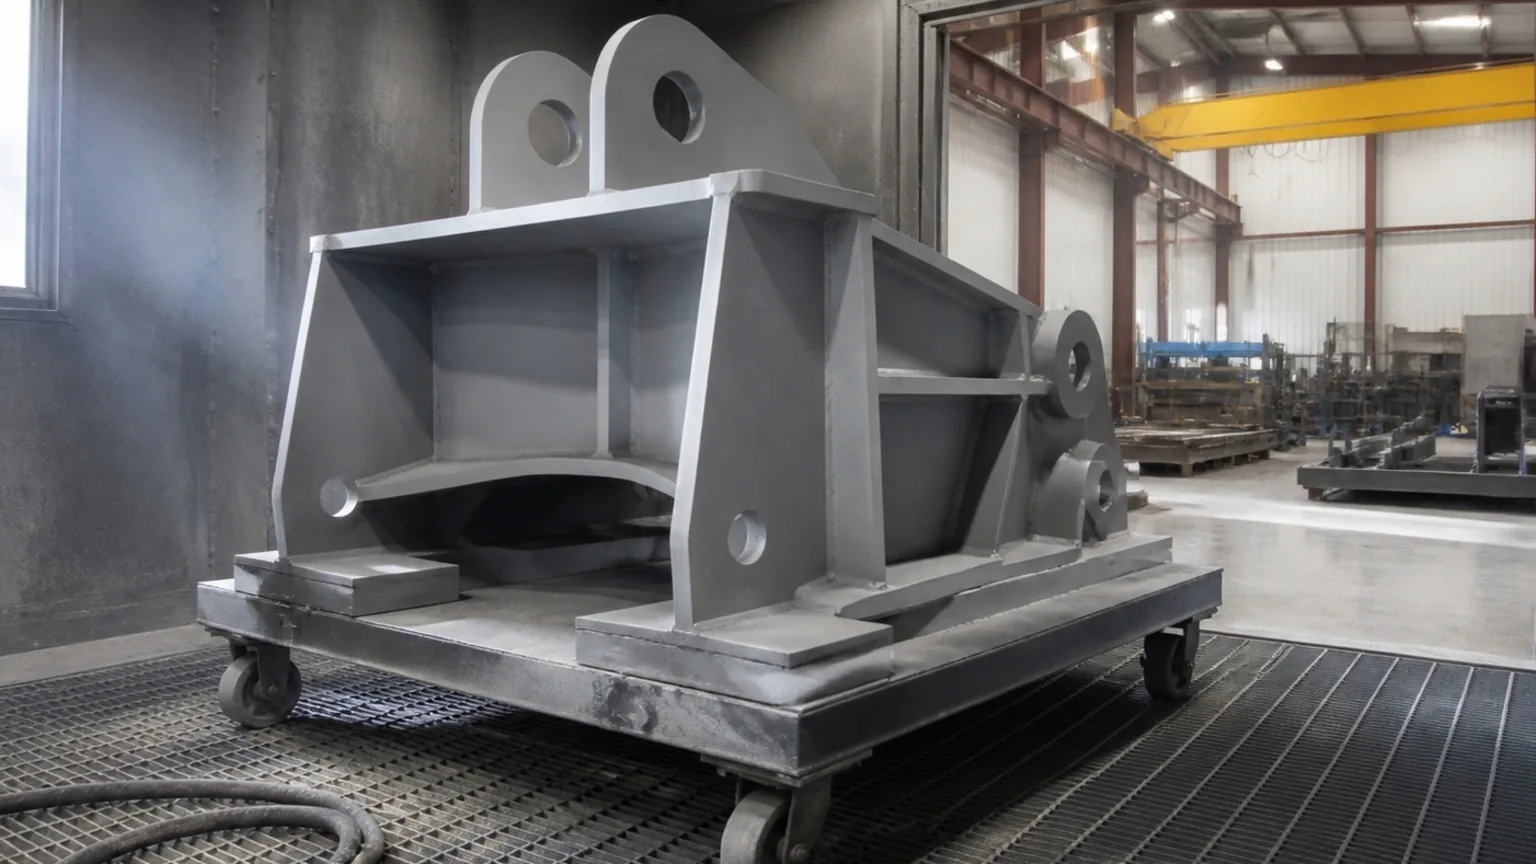
Profile and cleaning to the coating spec before a part reaches the booth.

Powder primer and top-coat booths on the automated conveyor line.

Through the oven at the coating's cure schedule.

Film thickness checked; parts move to assembly or shipping.

Every FabTek product that isn't galvanized or left stainless: transformer cabinets and tanks, switchgear and control enclosures, bus duct and busway, generator and BESS enclosures, PDU and UPS cabinets, conveyor frames and indoor steel. Finish-only work for OEMs and other fabricators runs on the same lines.
| Line 1 | Automated conveyor powder coat line — pre-treatment, powder primer booth, powder top-coat booth, cure oven |
|---|---|
| Line 2 | Heavy-duty monorail coating system for long and heavy parts |
| Pre-treatment | Abrasive blast room and chemical pre-treatment — see metal finishing |
| Performance | IEEE 2,000-hour salt-spray certification; film thickness per spec — see film thickness for outdoor enclosures |
| Colors | ANSI 61, ANSI 70, Munsell 7GY 3.29/1.5 green, RAL and OEM color match; textures on request |
| Masking | Threads, ground pads, gasket faces and machined surfaces masked per drawing |
| Documentation | Film thickness readings, cure records, color batch numbers; ISO 9001:2015 |
| Also specified as | Powder coating services, industrial powder coating, powder coat finishing, electrostatic powder coating, powder coating for enclosures, large part powder coating |
Representative capabilities — exact ranges, ratings, and finishes are confirmed per project. Send drawings for a firm quote.
A cabinet line wants speed: many similar parts, hung densely, moving continuously. A tank line wants capacity: one heavy body on a track that can carry it, cured long enough for its mass. Running both on one line means one of them is always compromised. FabTek's second line — the heavy-duty monorail — exists so tanks, structures and long housings get a proper cure and the cabinet line keeps its pace. The result is one finish specification across a package: a transformer's tank and its cabinet come off different lines in the same color lot.
Built at four production sites in Hazlehurst, Mississippi.
ISO 9001:2015 quality management, AWS-certified welding, OSHA-compliant facilities.
In-house powder coat backed by an IEEE 2000-hour salt-spray certification.
Reserved-line capacity and the automation to grow with your volume.
The line is certified to IEEE's 2,000-hour salt-spray requirement for outdoor electrical equipment. Film thickness is measured and recorded per specification — see our film thickness spec sheet.
FabTek Industries runs a heavy-duty monorail powder coat line for tanks, structures and long housings alongside an automated cabinet line at its Hazlehurst plants, and offers finish-only work on both.
Yes. ANSI, RAL, Munsell and OEM-specified colors are matched and the recipe retained so repeat orders match.
Powder coat for cabinets, tanks, enclosures and indoor steel; hot-dip galvanizing for substation and transmission structures in outdoor service. FabTek powder coats in-house and galvanizes through partners; duplex (galvanize plus powder coat) is available where specified.
Explore related lines: Transformer cabinets · Transformer tanks · Switchgear enclosures · Generator enclosures
Further reading: Powder coat film thickness for outdoor enclosures · What the IEEE 2,000-hour salt spray test means · Galvanizing vs. paint for substation steel


Have parts to finish? Send the spec, the color and the quantities — we'll come back with a plan and a firm price, typically within one business day.