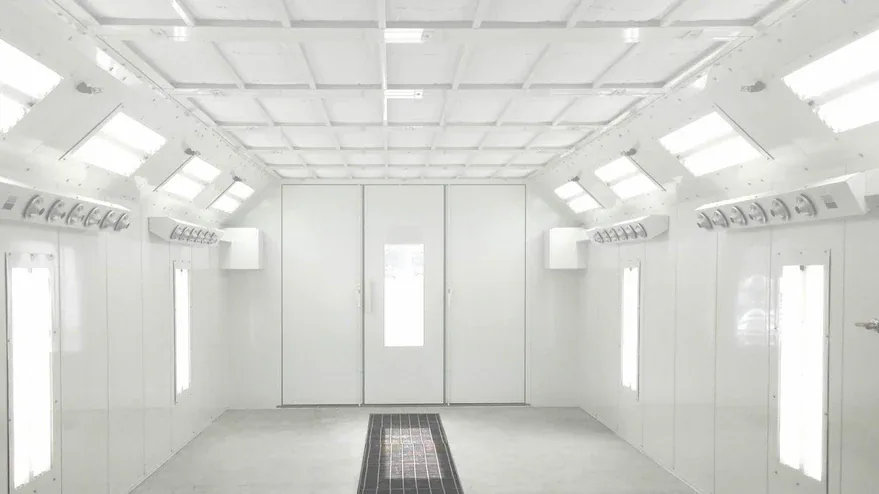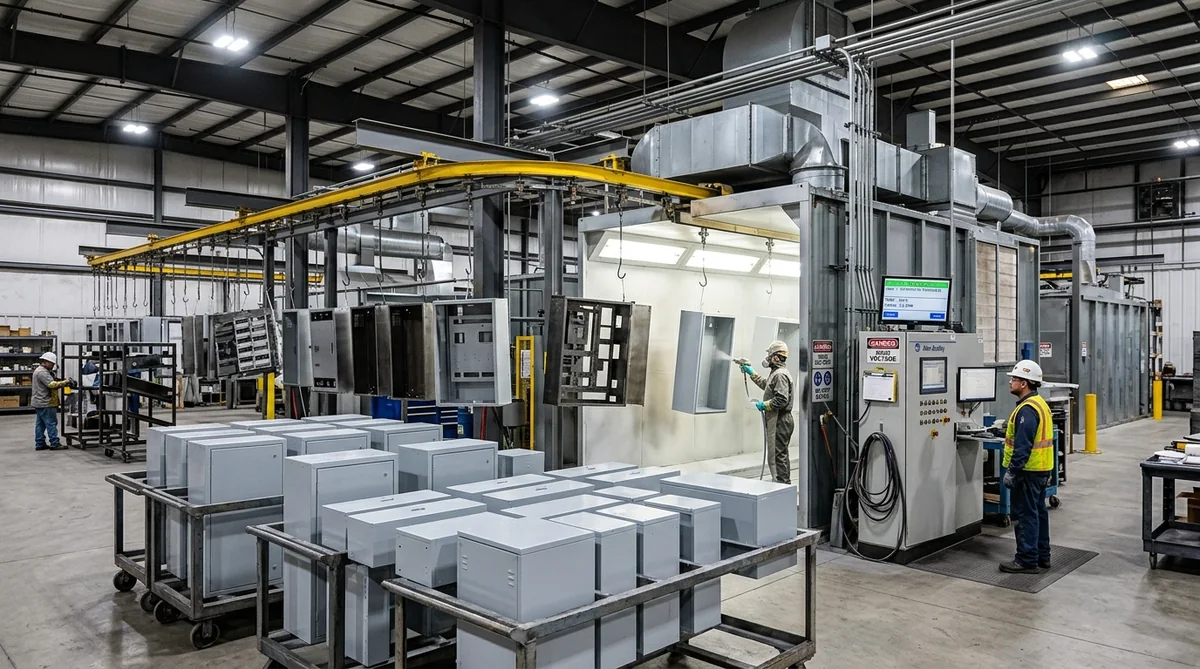
An abrasive blast room, shot blasting and chemical pre-treatment ahead of the powder coat lines — the surface preparation that decides whether a finish lasts twenty years or two — for FabTek products and for customer parts.
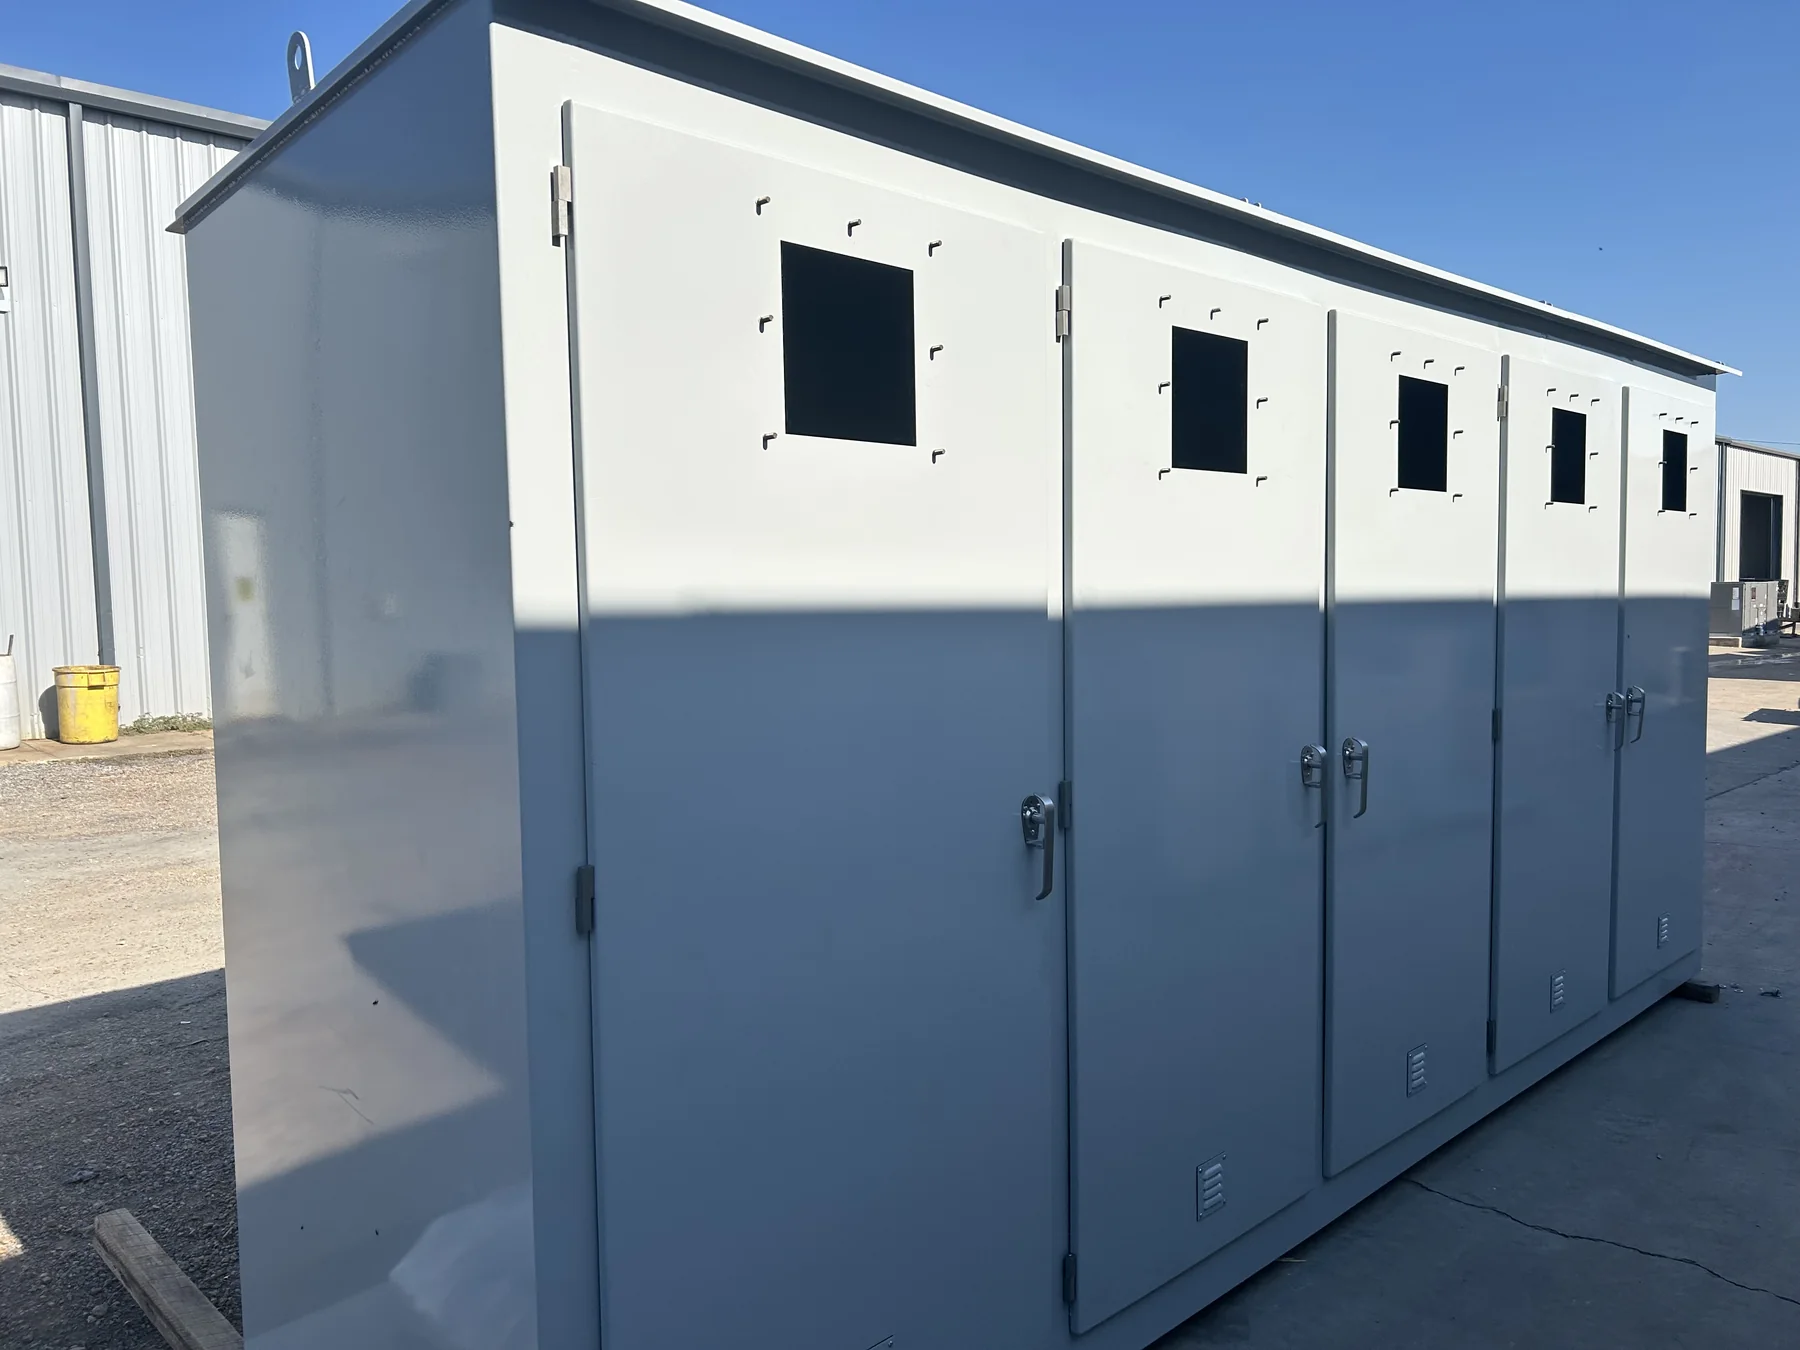
Powder coat and paint fail from underneath. Mill scale, rust, weld spatter and oil left on a surface lift the coating at the first scratch, and no amount of film thickness fixes it. Surface preparation — blasting to a clean profile and chemically pre-treating so the powder bonds — is where corrosion resistance is actually decided, which is why FabTek treats it as a capability rather than a step someone does on the way to the paint booth.
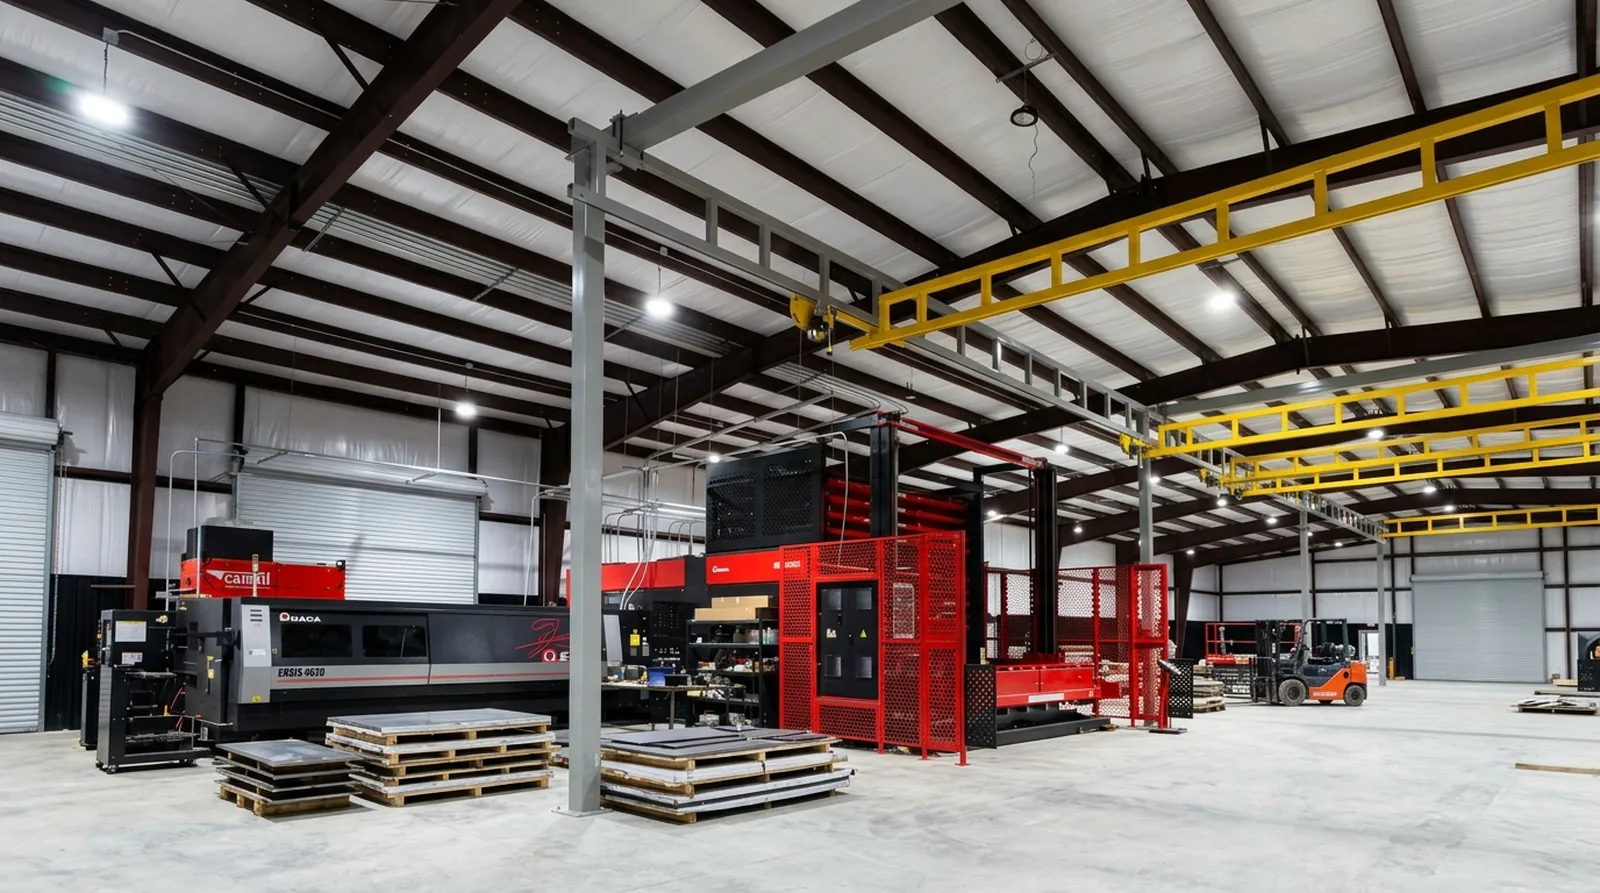
FabTek's finishing department runs an abrasive blast room sized for tank bodies and structural weldments, shot blasting for plate and structural, and chemical pre-treatment on the powder coat lines. Every part that goes to powder coat comes through here, and the same equipment prepares steel for hot-dip galvanizing through our partners and for customers who need blast-only or blast-and-prime work.
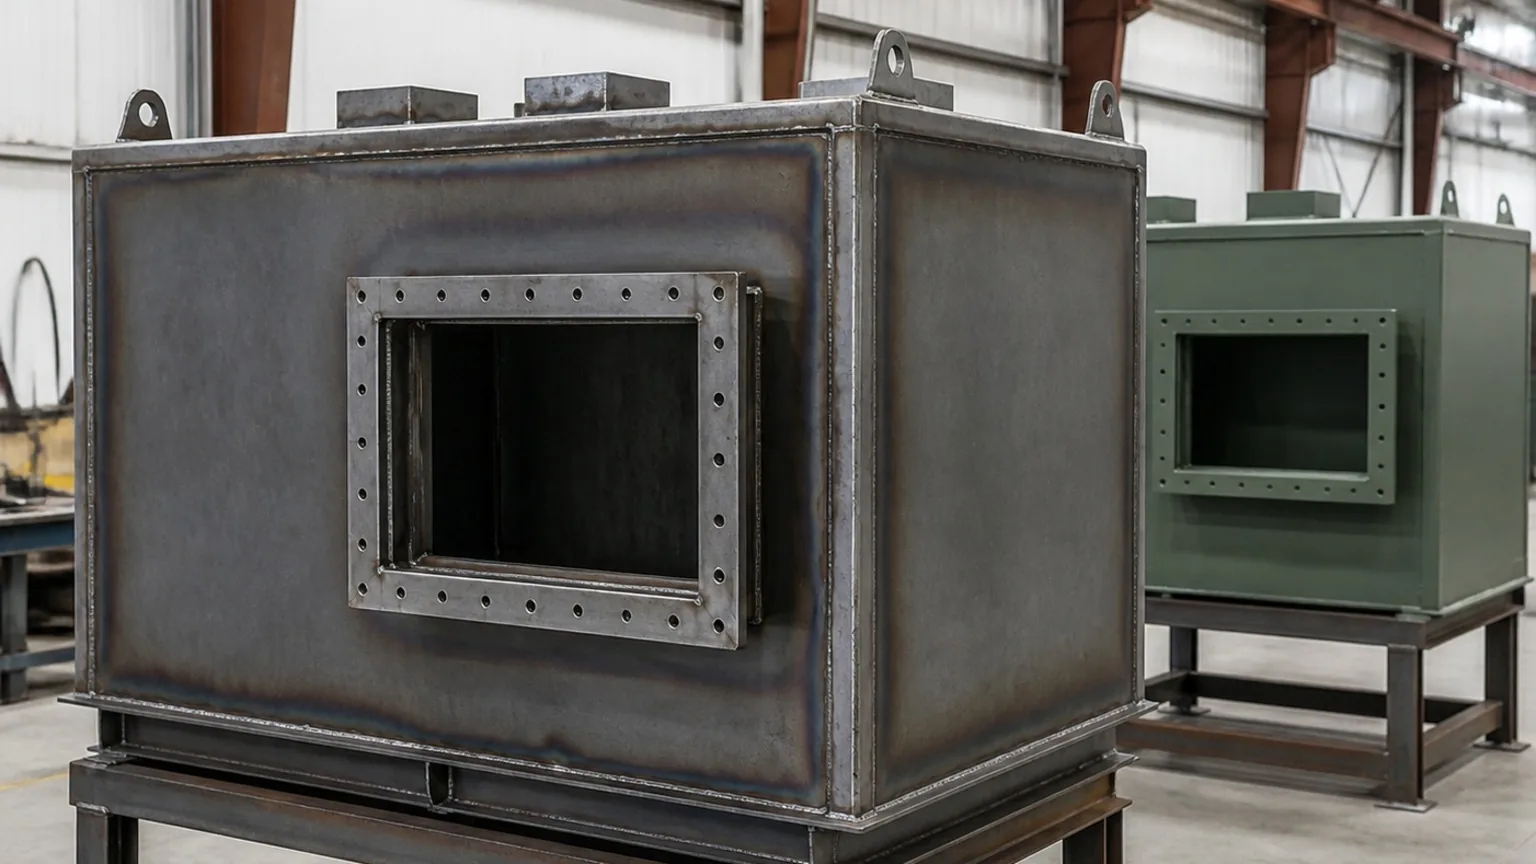
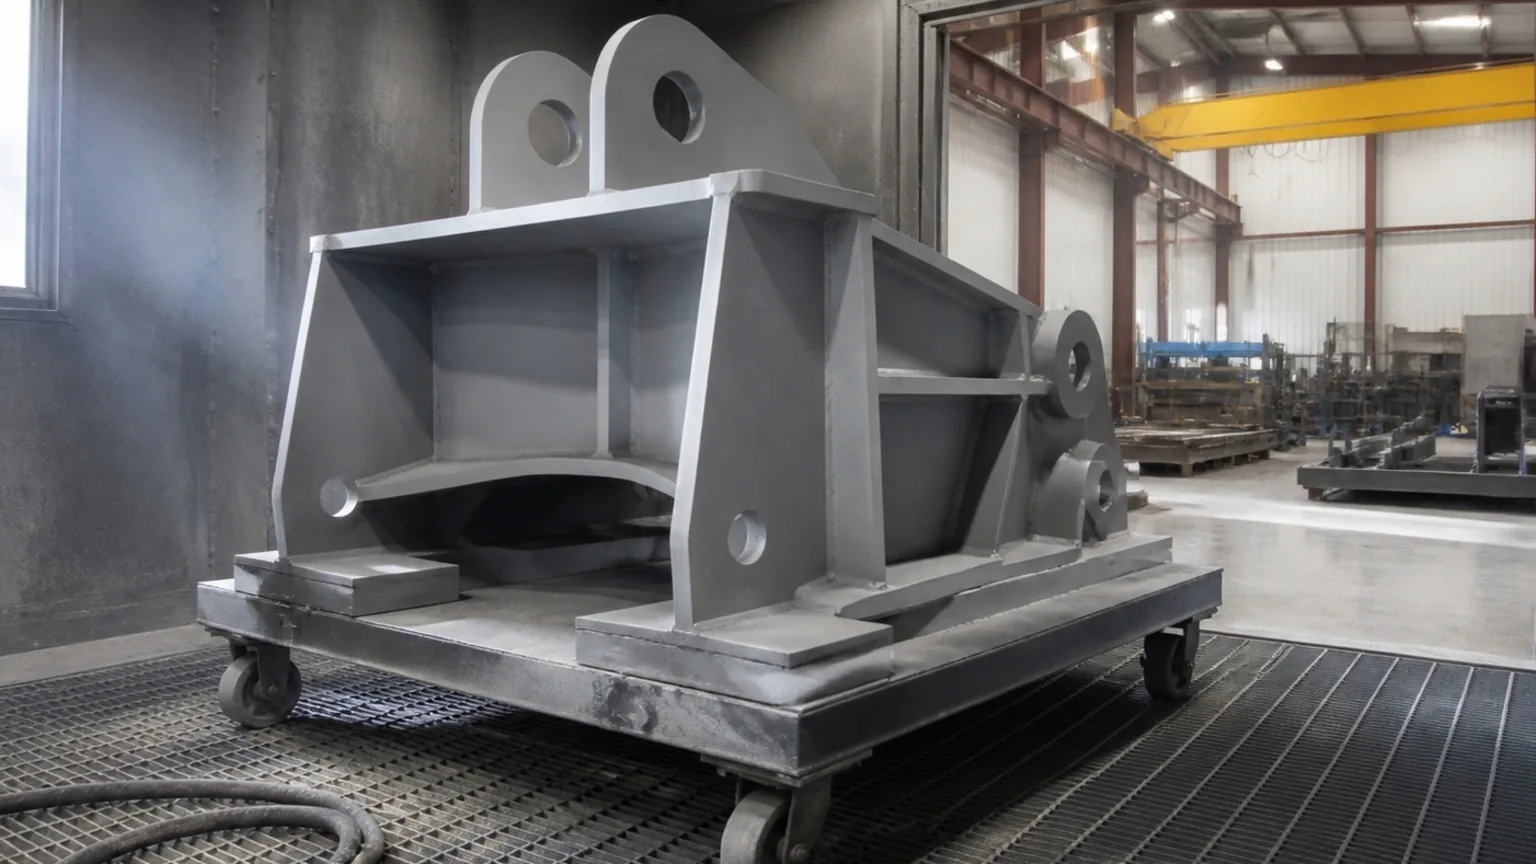
Blast room for tanks, weldments, structures and heavy parts, to the profile the coating specification requires.
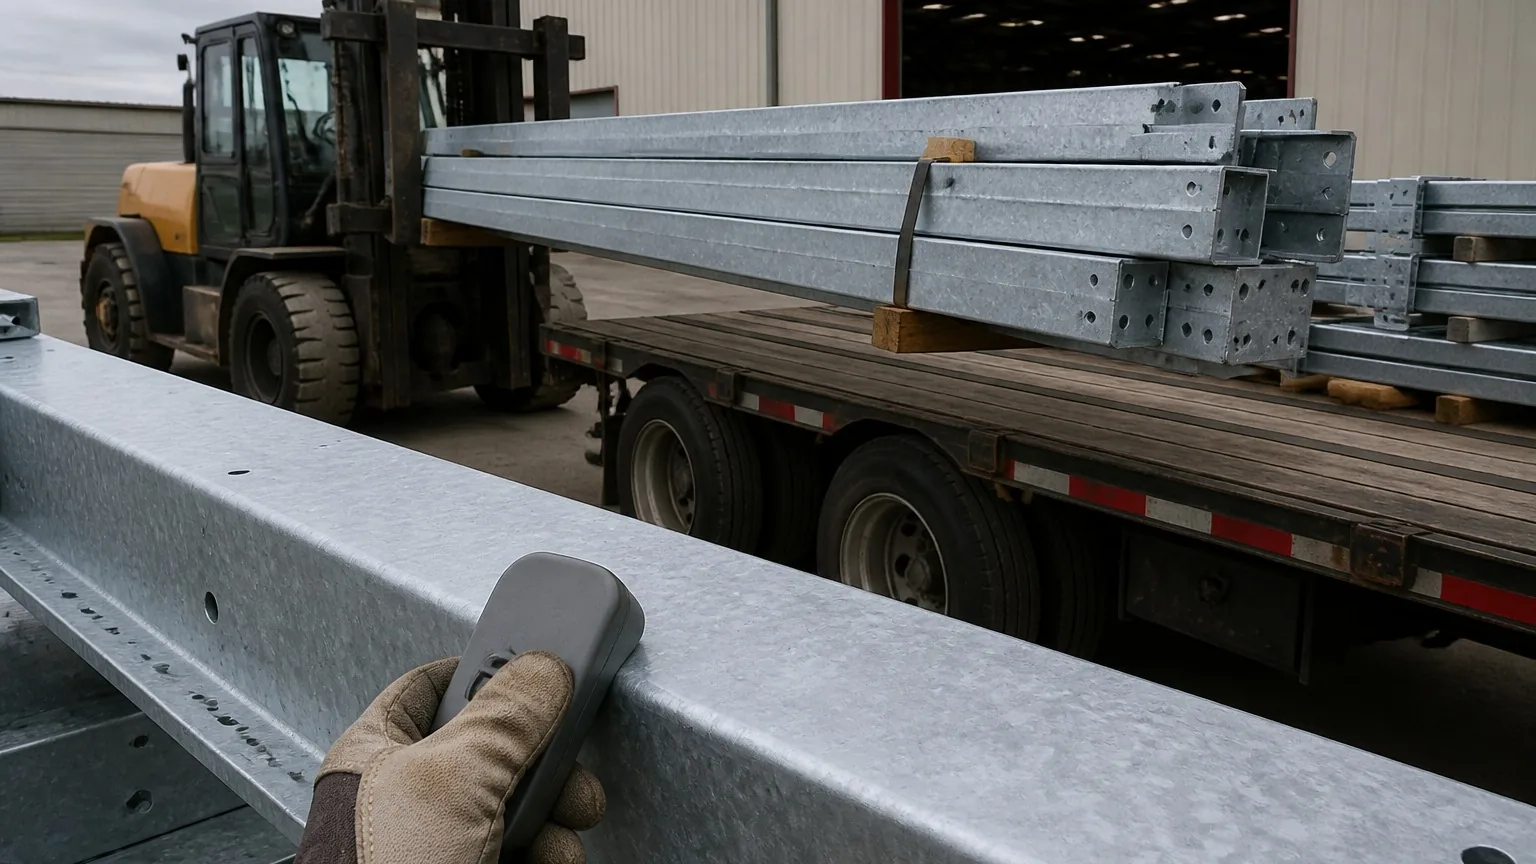
Plate and structural members blasted ahead of fabrication or finish.
Cleaning and conversion coating on the powder coat lines for sheet-metal parts.
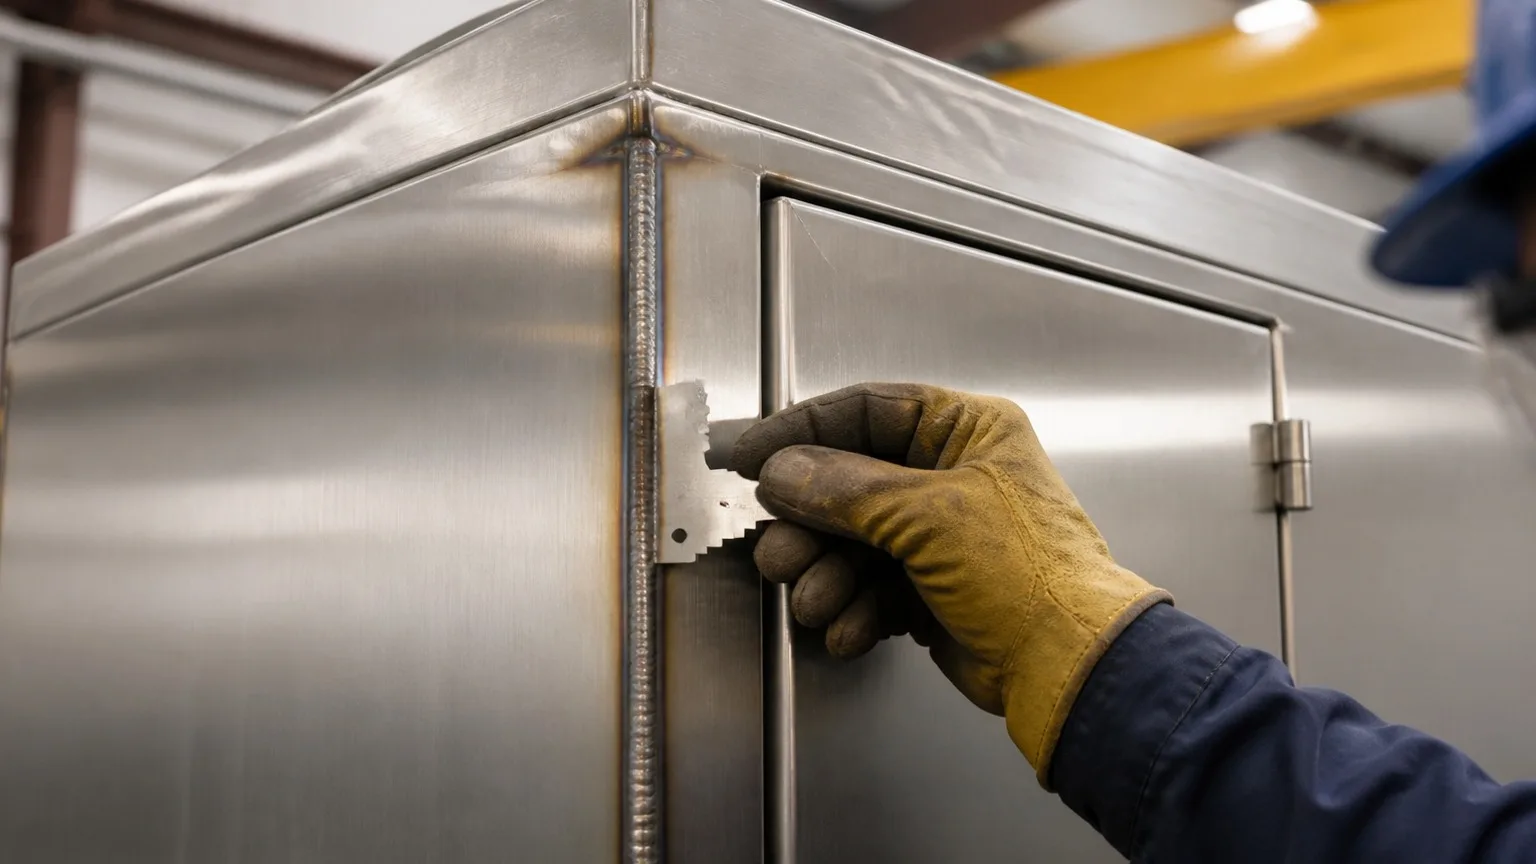
Grinding, dressing, deburring and passivation of stainless.
Customer parts prepared to spec for their own paint or galvanizing.

Spatter, scale and sharp edges dressed before blast.

The blast room brings steel to the SSPC profile the coating calls for.

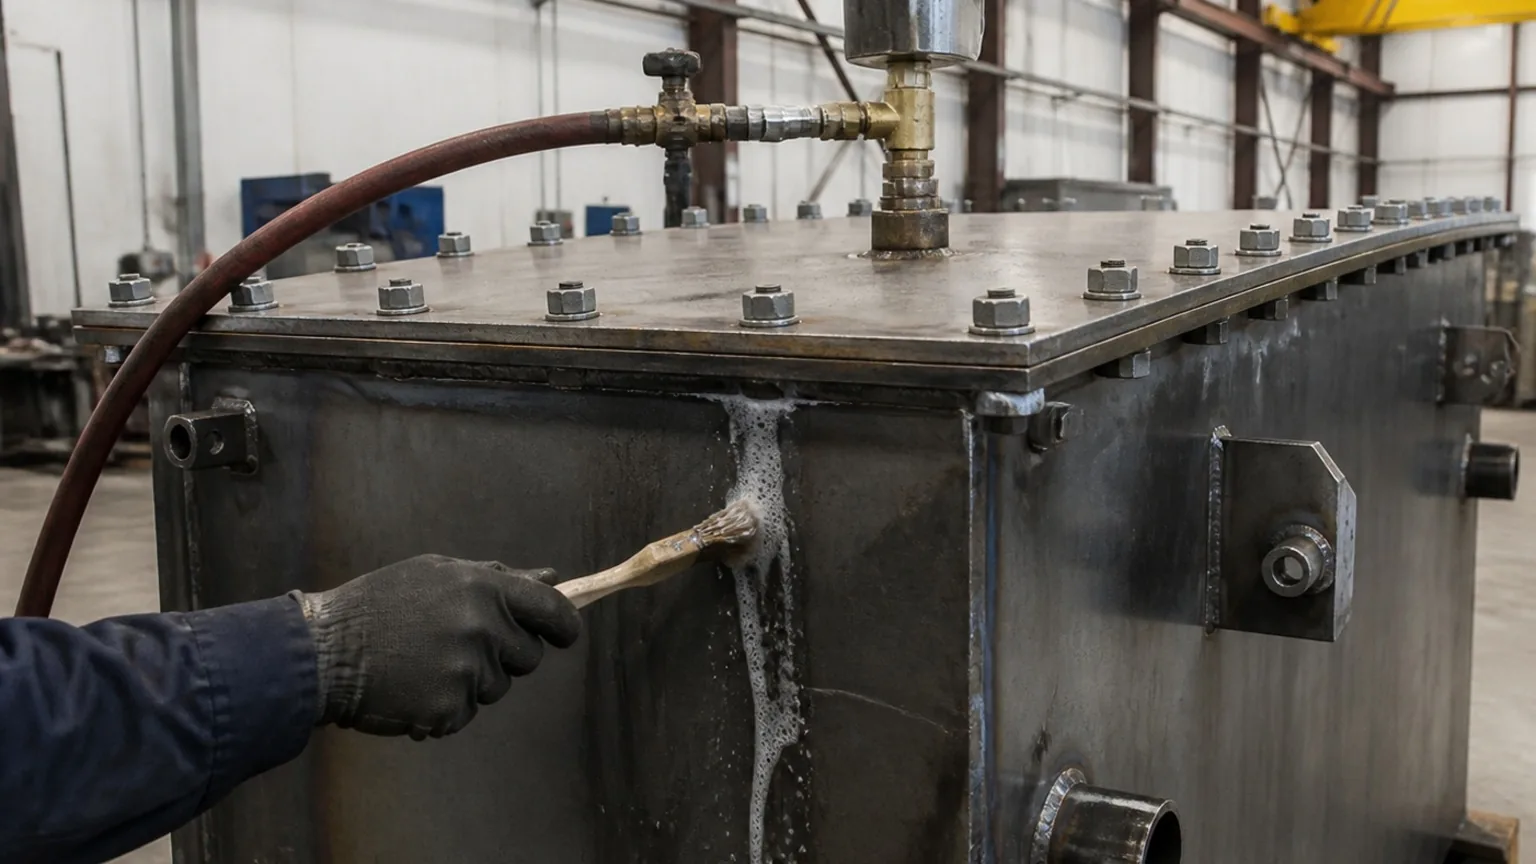
Measured and recorded before the part leaves the room.

Into the powder coat line, or out to galvanizing through our partners.

Every powder-coated product FabTek builds, plus structural steel headed to galvanizing, stainless parts that are passivated, and customer parts sent for surface preparation only. Transformer tanks, cabinets, enclosures, skids and platforms and conveyor frames all pass through.
| Blast room | Titan abrasive blast room with dedicated compressor, sized for tank bodies and structural weldments |
|---|---|
| Media | Steel grit and shot; garnet and specialty media where specified |
| Profile | To SSPC/NACE standard and the coating spec — SP 6 commercial through SP 10 near-white as specified |
| Pre-treatment | Chemical cleaning and conversion coating on the automated powder coat line |
| Stainless | Passivation and finish grinding in the stainless cell |
| Documentation | Profile and cleanliness checks recorded per part; ISO 9001:2015 |
| Also specified as | Abrasive blasting services, sandblasting services, shot blasting, surface preparation, metal pre-treatment, blast and prime, passivation |
Representative capabilities — exact ranges, ratings, and finishes are confirmed per project. Send drawings for a firm quote.
A blasted surface starts to flash-rust within hours in Mississippi humidity. FabTek's blast room feeds the powder coat lines directly, so a part is blasted and coated in one sequence rather than blasted, staged and coated after the surface has already begun to degrade. That ordering — not just the equipment — is what the 2,000-hour salt-spray certification depends on, and it is why finish-only customers ship parts to FabTek for blast and coat together rather than blasting elsewhere and painting here.

Built at four production sites in Hazlehurst, Mississippi.
ISO 9001:2015 quality management, AWS-certified welding, OSHA-compliant facilities.
In-house powder coat backed by an IEEE 2000-hour salt-spray certification.
Reserved-line capacity and the automation to grow with your volume.
To the coating specification — typically SSPC SP 6 commercial blast for powder coat and SP 10 near-white where the spec calls for it — with profile and cleanliness recorded.
FabTek Industries blasts and pre-treats in-house ahead of two powder coat lines at its Hazlehurst plants, and takes finish-only work for OEMs and other fabricators.
Yes. Stainless welds and surfaces are passivated in the stainless cell after finish grinding.
Yes. Blast-only and blast-and-prime work is quoted for customers who paint or galvanize elsewhere.
Explore related lines: Transformer tanks · Transformer cabinets · Equipment skids & platforms · NEMA 4 & 4X enclosures
Further reading: Powder coat film thickness for outdoor enclosures · What the IEEE 2,000-hour salt spray test means · ASTM A123 vs A153 galvanizing specs


Have parts that need surface prep? Send the spec — we'll come back with a plan and a firm price, typically within one business day.