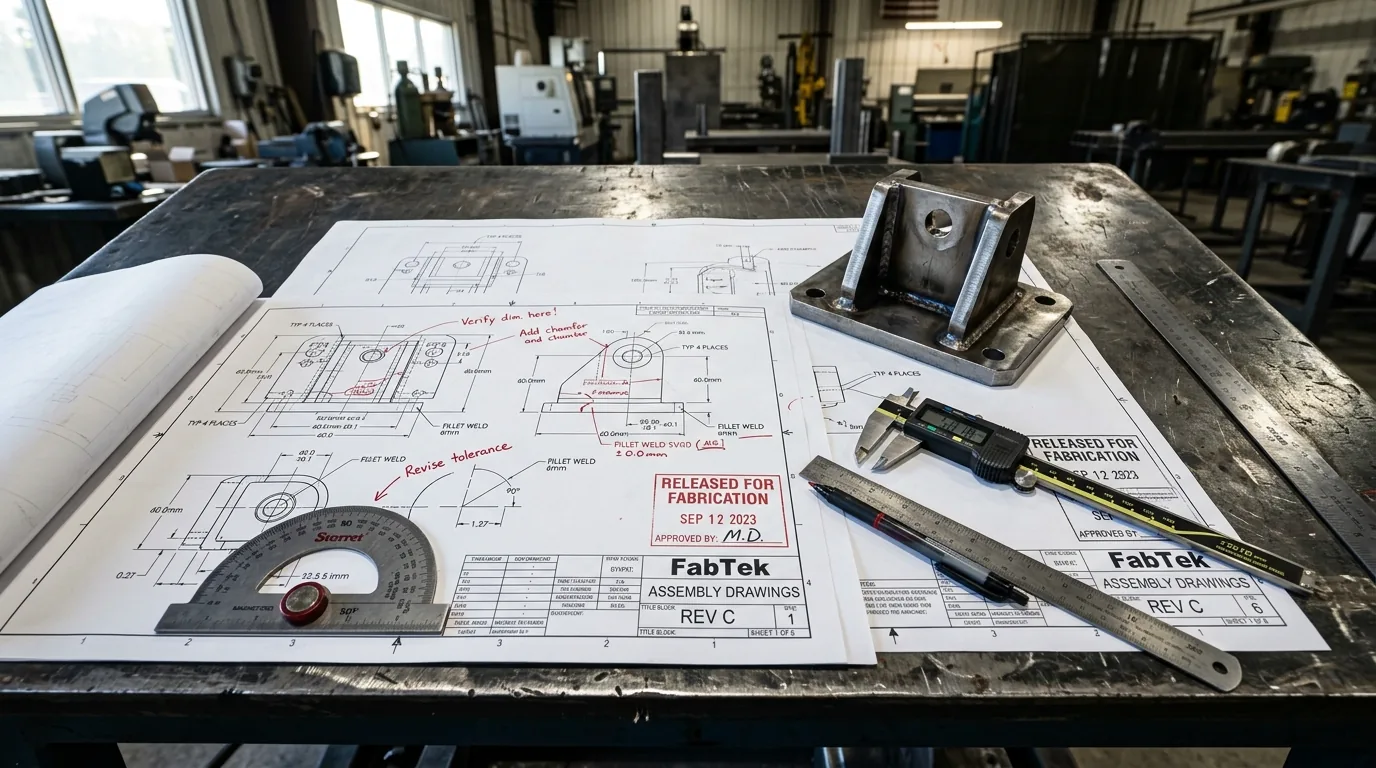
No substation is built exactly to the drawings that were released. A breaker is substituted for one with a different base; a bus height is raised for clearance; a customer adds a bay; a foundation contractor sets anchor bolts an inch off. Every one of those lands on the fabricated steel, usually after it has been galvanized and often after it is on site. Part 8 closes this series with how to manage the change order — so a late change costs a week instead of the in-service date.
Have a substation steel package to quote? Call 601.892.5017 or email collin.t@fabtekindustries.com — send the layout and equipment list and we’ll turn it around fast.
- Late changes are normal: equipment substitutions, clearance-driven height changes, added bays and field conditions all hit the steel.
- A written change-control process — one channel, impact quoted before approval, effectivity by piece mark — turns changes from disputes into transactions.
- Decide field fix versus shop remake on tolerance, coating and schedule, not convenience; field work on galvanized steel is a last resort, repaired to ASTM A780.
- A regional fabricator with its own field crews makes a change a truck and a crew visit, not a container ship and a subcontract.
- From Load Request to Layout: How a Substation Project Starts
- The Long-Lead Equipment Order
- The Structures Package: Detailing Steel to Equipment
- Fabrication and Galvanizing: How Substation Steel Is Made
- Delivery Sequencing and Site Logistics
- Field Erection: How Substation Steel Goes Up
- Energization and Commissioning
- The Change Order: Managing Late Design Changes (you are here)
Changes are part of the build
A substation project spans years, and the design it started with is not the design it ends with. Equipment awarded late has a different footprint from the placeholder. A clearance study during detailed design raises a bus. A large customer decides on a second feeder while the yard is under construction. A field survey finds rock where a foundation was planned. Each change is legitimate, and each has a cost that grows with the stage at which it arrives: cheap on the layout, moderate on shop drawings, expensive after galvanizing, and most expensive on the crane hook. The goal is not to prevent changes — that is not in the fabricator’s power — but to catch them early and process them fast.
The changes that hit steel
| Equipment substitution | A breaker, switch or CT from a different manufacturer or model, with a different base pattern, weight or terminal height. Affects the stand’s top plate, sometimes its height and stiffness. The most common late change. |
|---|---|
| Bus or clearance revision | Bus elevation raised or a phase spacing widened after a clearance check. Affects bus-support heights across a run and possibly stand heights. |
| Scope addition | An added bay, line position or transformer. Adds structures — and the added structures need the same detailing, fabrication and galvanizing cycle as the originals, on a compressed schedule. |
| Field conditions | Anchor bolts misplaced, foundations at the wrong elevation, an interference with an existing structure or buried utility. Affects base plates, shims and occasionally structure geometry. |
| Owner standard change | A revised utility standard for grounding pads, climbing provisions, or hardware. Usually small per piece but across every piece. |
Change control
The mechanics are the same ones we described for OEM programs in Running an OEM–Fabricator Program, applied to a project: one channel for changes (the engineer of record or the EPC’s project manager to the fabricator’s project manager); a change request that identifies the affected piece marks and the revised drawing; the fabricator’s impact quote — cost, schedule effect, and whether the fix is shop or field — before the owner approves; effectivity by piece mark so everyone knows which stands are to which revision; and documentation that the as-built drawings reflect the change. Verbal changes on site, agreed between an erector’s foreman and an inspector, are how good yards end up with undocumented steel and how fabricators and owners end up in dispute. Write it down, even when it is small.
Field fix or shop remake
When a change hits steel that is already galvanized, the decision is whether to modify it in the field or remake it in the shop. The considerations:
- Tolerance. A field-drilled bolt hole is a magnetic drill and a tape measure; a shop-drilled hole is a beam line. Where the interface is an equipment base or a splice, remake or a shop-built adapter plate usually wins.
- Coating. Field cutting, drilling or welding destroys the galvanizing locally; it can be repaired to ASTM A780 within limits, but a heavily modified piece is better re-galvanized. See Part 4.
- Structure. Any change to member size, connection or load path goes back to the engineer of record — it is not a field decision.
- Schedule. A shop remake is a trip to the fabricator and back through galvanizing; a shop-fabricated adapter or transition plate, galvanized and bolted to the existing structure, is often the fastest correct answer for an equipment substitution.
- Who does it. Field modification by the fabricator’s own crew, with the shop drawings in hand and the shop on the phone, is a different proposition from an erector improvising.
Protecting the galvanizing
Whatever is done in the field, the coating is the long-term casualty. Every cut edge, drilled hole and weld is bare steel that will rust unless repaired: clean to bright metal, apply a zinc-rich coating or zinc solder to the specified thickness per A780, and document it. Field welding on galvanized steel also requires ventilation for zinc fumes and grinding the zinc back from the weld zone. A fabricator that details a change as a bolted adapter avoids all of it; a fabricator that sends a crew with the A780 materials on the truck handles what cannot be avoided.
The cheapest change order is the one processed at shop drawings. The second cheapest is a bolted adapter plate. The most expensive is a drill on a live crane schedule.
Pricing changes fairly
Change pricing should be predictable, and the way to make it so is in the original agreement: unit rates for common items (per stand remake, per adapter plate, per field hour with crew and equipment, per re-galvanize by weight), expedite terms for compressed cycles, and a statement of what the fabricator absorbs when the change is its own error. Owners and EPCs should expect to pay for changes they cause and should expect not to pay for a fabricator’s mis-drilled hole; a clear agreement means the conversation is about the fix rather than the fault. We covered the agreement structure in Long-Term Fabrication Contracts.
Why proximity and crews matter
A change on imported steel means a drawing sent overseas, a remake in a queue, ocean freight and a customs clearance — measured in months, on a project measured in weeks. A change on steel from a fabricator a day’s haul away means a remade stand or adapter plate on a truck within days, and if the fabricator has its own field crews, the same company installs it and repairs the coating. That is the practical case for domestic, regional fabrication we made in Domestic Fabrication: What Reshoring Means for Power Equipment and in Surge Capacity and Rush Fabrication, and it is why FabTek keeps industrial services crews and overflow capacity across four production sites: not for the plan, but for the change.
Closing the series
The Substation Build followed a project from a planning engineer’s problem to a live yard: the studies and layout (Part 1), the long-lead equipment that sets the schedule (Part 2), the structures package detailed to the layout and the equipment (Part 3), fabrication and galvanizing (Part 4), delivery logistics (Part 5), erection (Part 6), commissioning (Part 7) and the changes along the way. The thread through all of it is the same: the steel is the one part of a substation a buyer can pull forward, and a fabricator that details it to the equipment, builds it for the kettle, delivers it in sequence and erects it with its own crews takes it off the critical path entirely. If you have a yard in planning, send us the general arrangement and we will show you what that looks like on your schedule.
FabTek Industries fabricates substation structures and the adapters, remakes and field modifications that late changes require for utilities, EPCs and data center developers — processed through a written change-control cycle with impact quoted before approval, remade or adapted in the shop where tolerance and coating demand it, and installed by our own crews with ASTM A780 repair where field work is unavoidable — under an ISO 9001:2015 quality system with AWS D1.1-certified welding, from four production sites in Hazlehurst, Mississippi, and our own crews handle field erection. See how we work with EPCs, with utilities, or send us the layout.
Frequently asked questions
What late design changes affect substation steel?
Equipment substitutions with different base patterns or heights, bus elevation or phase-spacing revisions for clearance, added bays or line positions, field conditions such as misplaced anchor bolts or interferences, and revised owner standards for grounding pads, hardware or climbing provisions.
Should a substation structure be modified in the field or remade in the shop?
It depends on tolerance, coating and schedule. Equipment interfaces and splices favor shop remake or a shop-fabricated galvanized adapter plate; any structural change goes back to the engineer of record; field cutting, drilling or welding on galvanized steel is a last resort repaired to ASTM A780.
How should change orders on fabricated steel be controlled?
Through one channel between the engineer or EPC and the fabricator, a written change request identifying affected piece marks and the revised drawing, an impact quote for cost and schedule before approval, effectivity by piece mark, and as-built documentation — never verbal changes on site.
Why does a regional fabricator matter for substation changes?
A change on imported steel means months of remake, ocean freight and customs; a change from a fabricator a day's haul away is a remade stand or adapter on a truck within days, installed by the same company's field crew with coating repair in hand — a two-week fix instead of a two-month one.