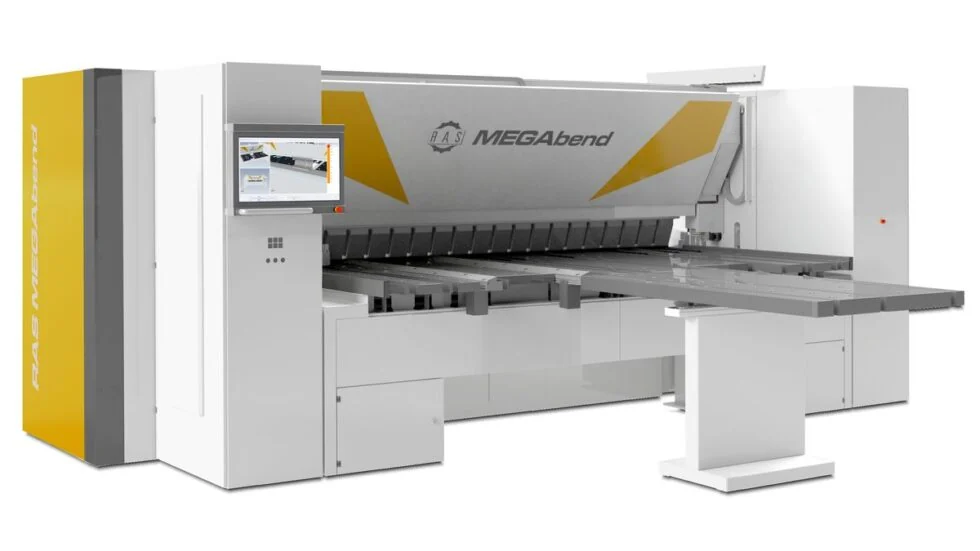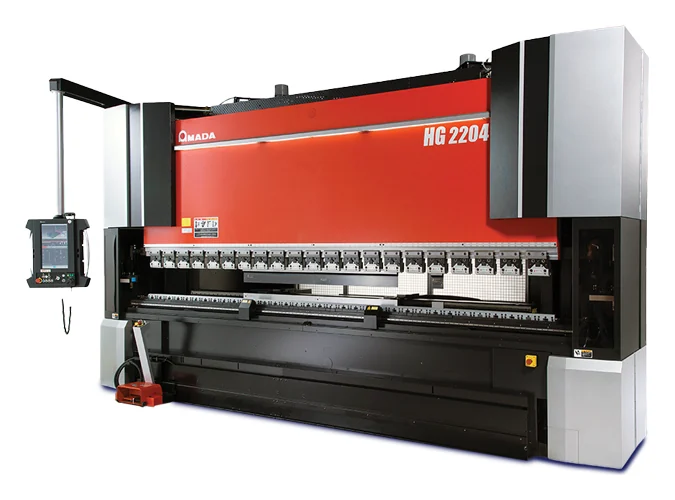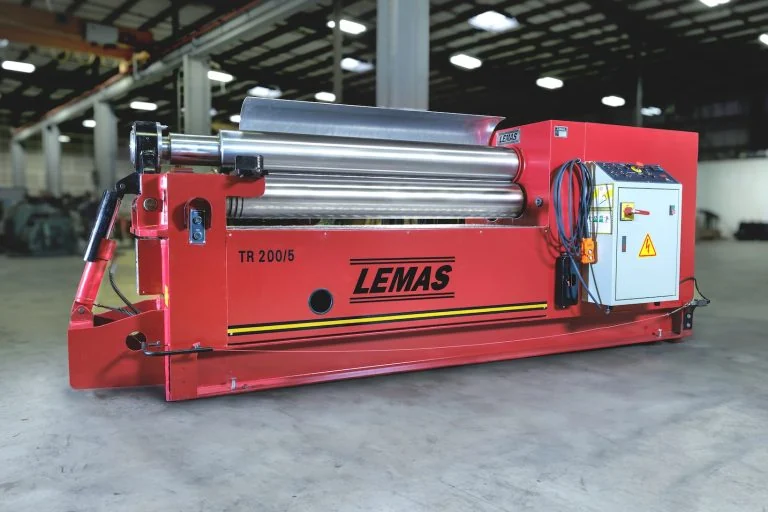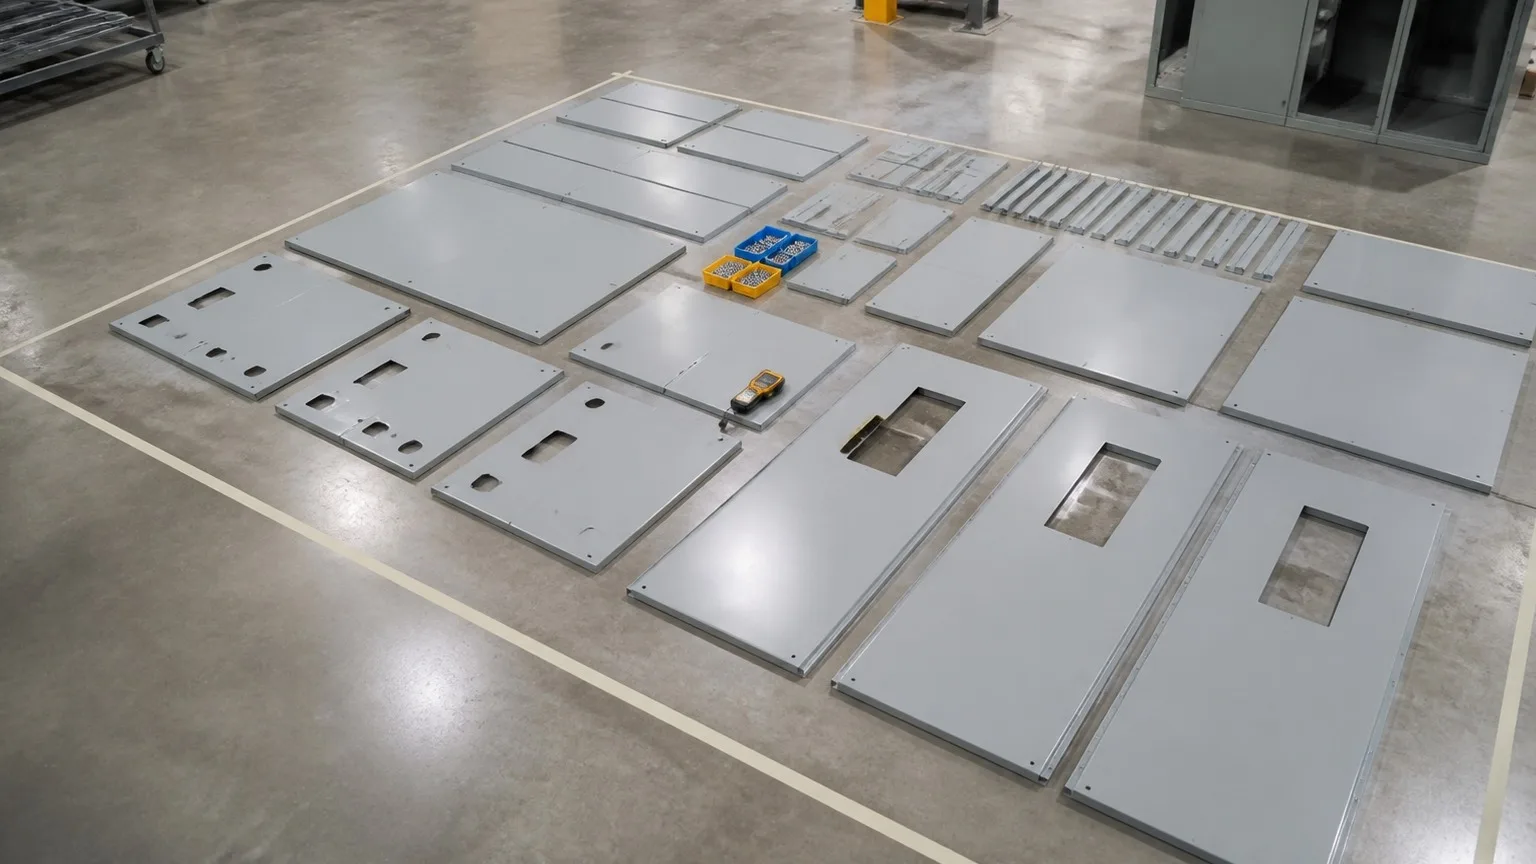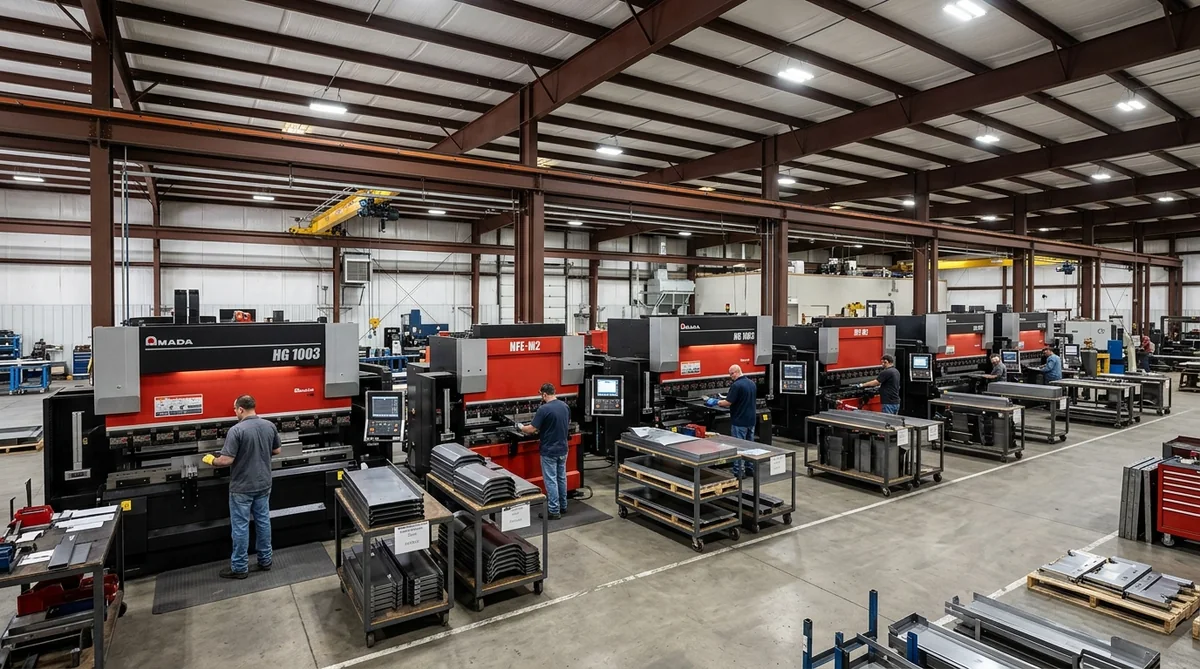
Ten press brakes led by three Amada CNC brakes, a RAS 76.40-2 MEGAbend automated panel folder for long skins, and a three-roll plate bender for tank shells — forming for every sheet-metal and plate product FabTek builds.
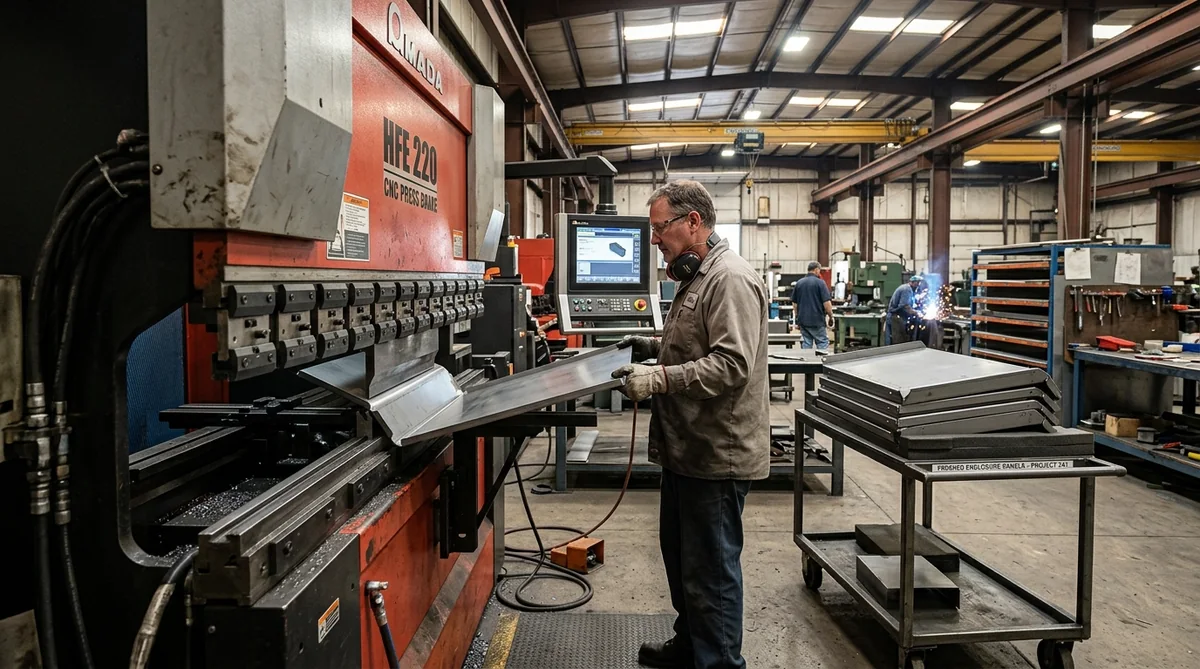
Forming is where a flat laser blank becomes a cabinet body, a door, a louver panel or a bus duct housing, and where plate becomes a tank shell. The equipment has to match the parts: a press brake for brackets and short flanges, a long CNC brake for full-height cabinet bodies, a panel folder for wide skins that would sag on a brake, and rolls for cylinders and cones. FabTek runs all of them, so a part is formed on the machine that suits it rather than wrestled through the wrong one.
The forming department is led by three Amada CNC press brakes with tooling libraries for the cabinet, enclosure and panel families we build in volume, supported by seven more brakes for secondary bends and overflow. A RAS 76.40-2 MEGAbend automated folder forms long panels and skins with one operator and no handling marks. A Lemas three-roll plate bender rolls tank shells and conservators. Everything sits between the lasers and the welding cells, so formed parts move to fit-up on the same floor.
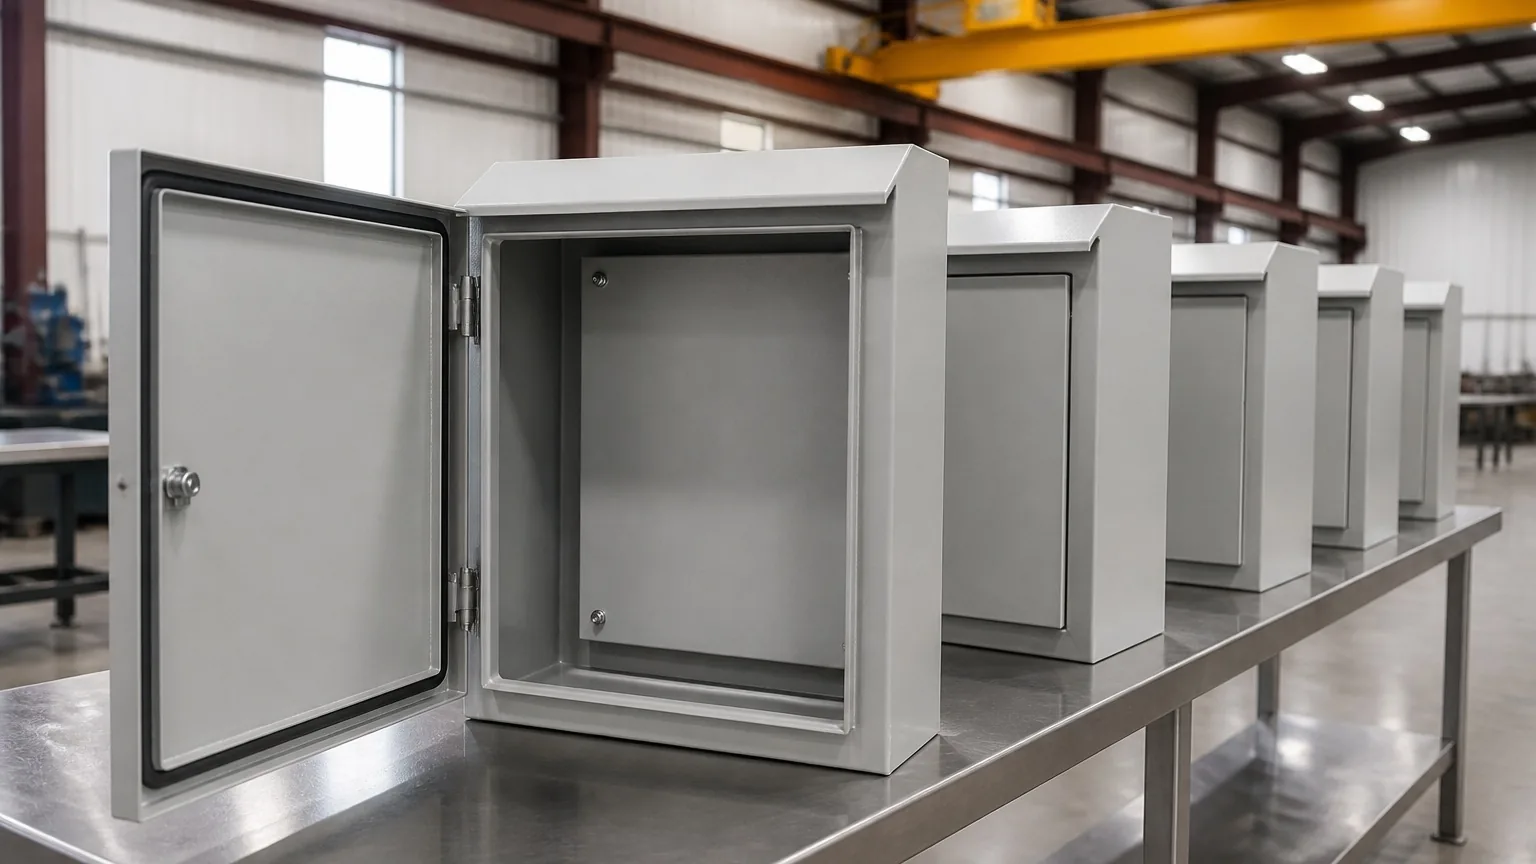
Cabinet bodies, doors, flanges, brackets and housings on three Amada CNC brakes and seven supporting brakes.
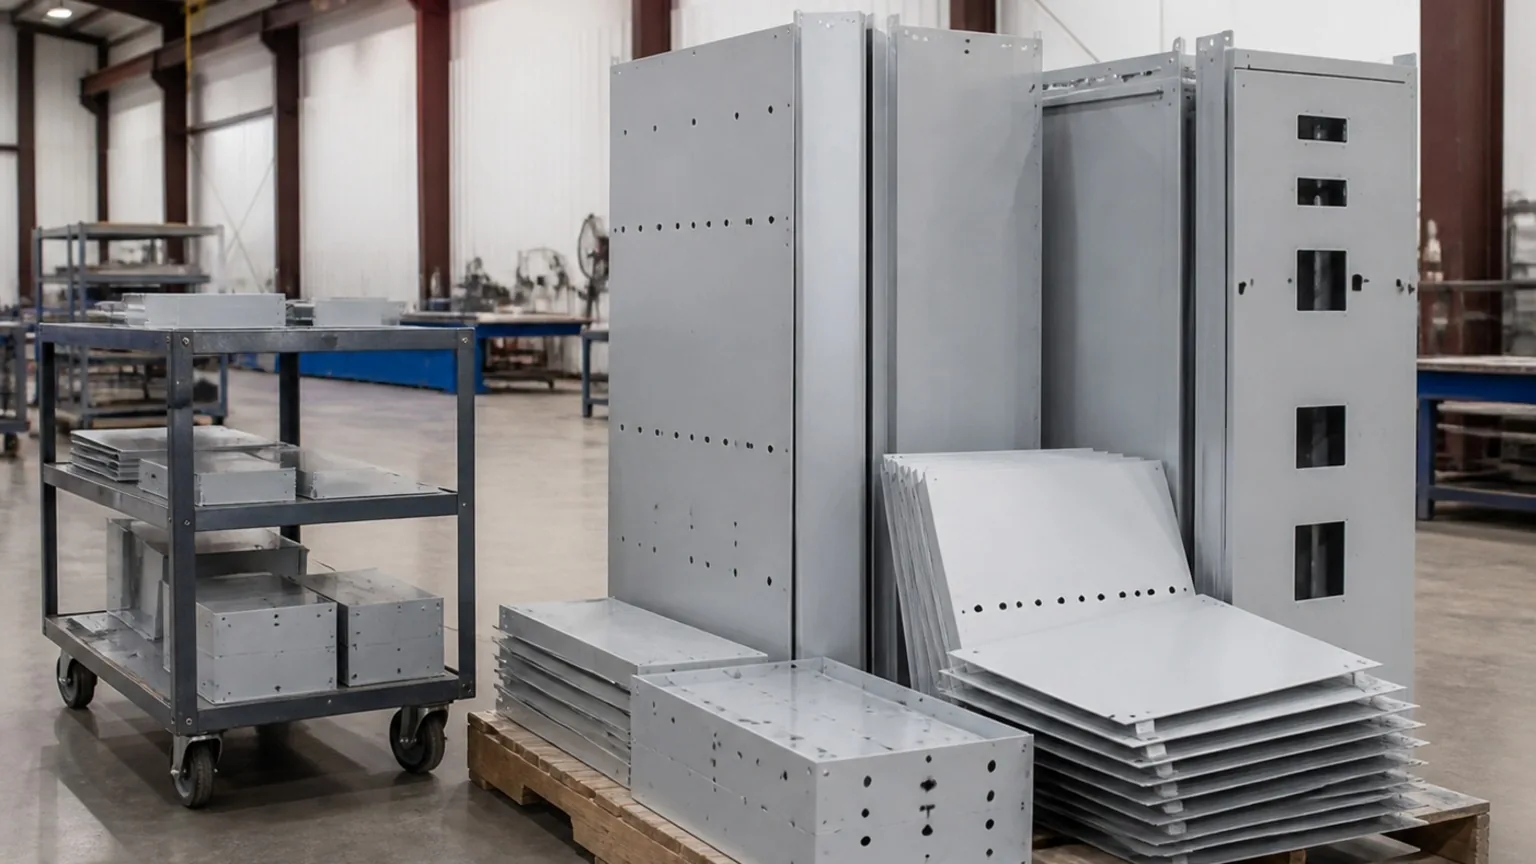
Long skins, doors, roof panels and enclosure walls on a RAS 76.40-2 MEGAbend, formed without tooling marks.
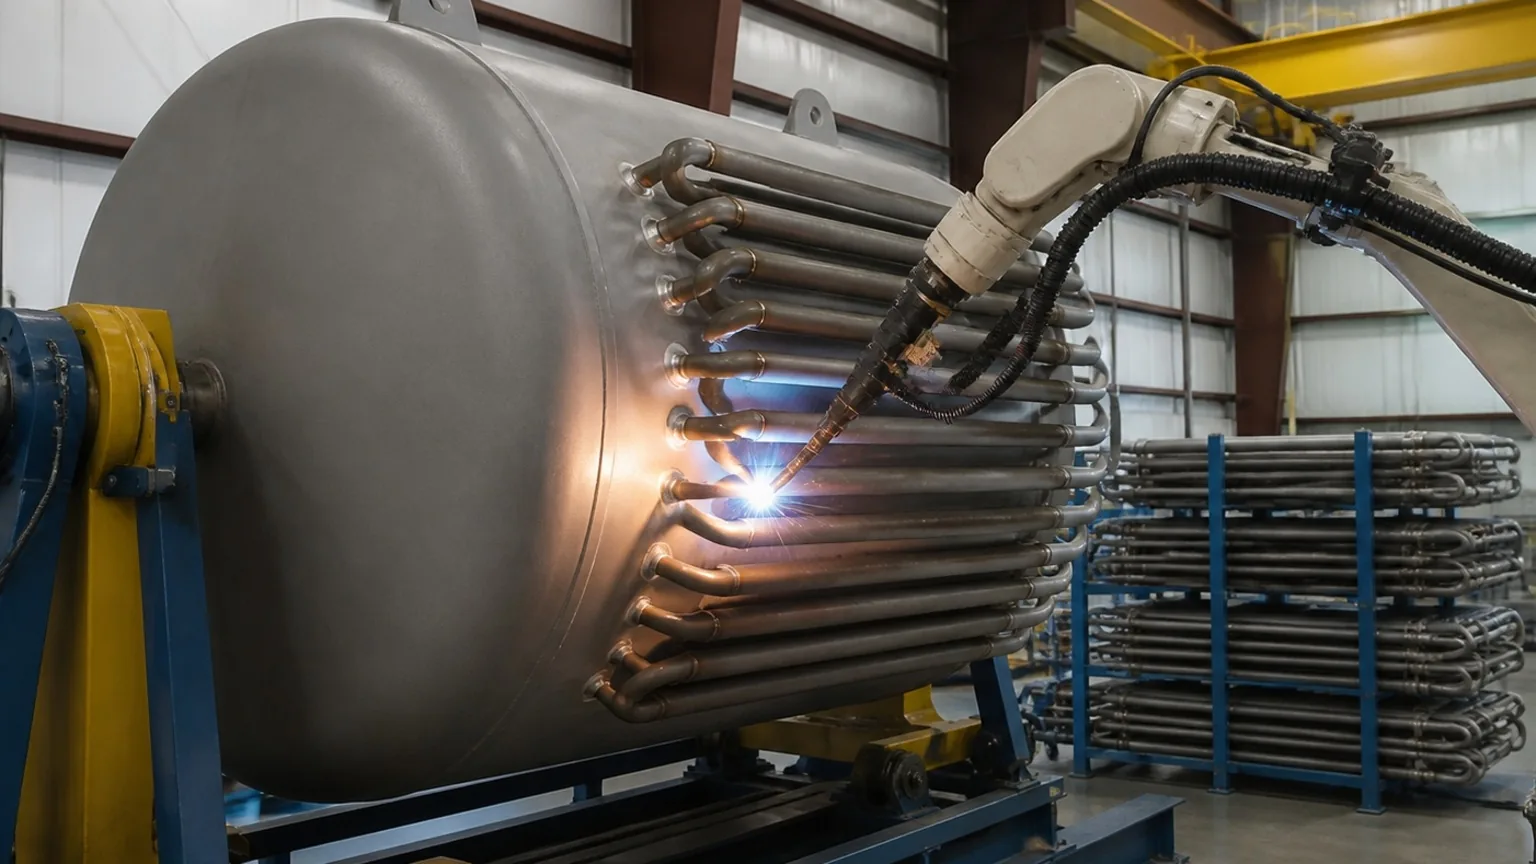
Round transformer tank shells, conservators and rolled sections on a Lemas three-roll plate bender and hydraulic bender.
Louvered panels and screened-vent frames for outdoor enclosures.
Blanks formed to print and shipped for customers who weld and assemble in their own plants.

Flat patterns arrive with bend lines marked and the bend sequence programmed.

Cabinet bodies, doors, flanges and brackets on three CNC brakes and seven supporting brakes.

Panels and enclosure walls folded with one operator and no handling marks.

Tank shells, conservators and rings rolled to diameter on the Lemas.

Every cabinet, enclosure and panel family — transformer cabinets, switchgear and control enclosures, generator and BESS enclosures, bus duct and busway housings — plus tank shells for round and pole-mount tanks, conservators and covers, and formed guards and pans for conveyor systems. Formed parts move to welding and powder coat without leaving the site.
| Press brakes | Ten press brakes — three Amada CNC brakes as primary cells, seven supporting brakes for secondary and overflow work |
|---|---|
| Panel folder | RAS 76.40-2 Series MEGAbend automated CNC folding for long panels and skins |
| Rolling | Lemas hydraulic three-roll plate bending roll; hydraulic bender for bar and small sections |
| Materials | Carbon, galvanized and galvanneal sheet, stainless, aluminum; plate for rolling |
| Programming | Bend sequences from FabTek engineering's flat patterns; bend allowances per material and radius |
| Downstream | Welding cells, hardware insertion, powder coat and assembly on site |
| Traceability | Heat numbers carried from blank to formed part; ISO 9001:2015 |
| Also specified as | Press brake forming, sheet metal forming, CNC bending, panel bending, plate rolling, metal bending services, sheet metal fabrication |
Representative capabilities — exact ranges, ratings, and finishes are confirmed per project. Send drawings for a firm quote.
A formed part that reaches powder coat with tooling marks, scratches or an inconsistent radius shows all of it after paint. FabTek forms cabinet skins and doors on the MEGAbend and the Amada brakes with tooling chosen for the material and finish, and holds bend allowances per material so a door formed in March matches one formed in October. Our spec sheet on minimum bend radius for 5052 aluminum is an example of how those allowances are set.
Built at four production sites in Hazlehurst, Mississippi.
ISO 9001:2015 quality management, AWS-certified welding, OSHA-compliant facilities.
In-house powder coat backed by an IEEE 2000-hour salt-spray certification.
Reserved-line capacity and the automation to grow with your volume.
Ten, led by three Amada CNC press brakes, plus a RAS 76.40-2 MEGAbend automated panel folder and a three-roll plate bender.
FabTek Industries forms long skins, doors and enclosure walls on a RAS MEGAbend automated folder at its Hazlehurst, Mississippi plants, alongside ten press brakes and in-house powder coat.
Yes. Round transformer tank shells, conservators and rolled sections are formed on a three-roll plate bender and welded on site.
Yes. Formed parts and kits ship to print for OEMs who weld, finish and assemble in their own plants.
Explore related lines: Transformer cabinets · Switchgear panels · NEMA 3R enclosures · Round & pole-mount tanks
Further reading: Minimum bend radius for 5052 aluminum · What gauge steel for a NEMA 3R walk-in enclosure · Metal fabrication machines and equipment guide


Have parts to form? Send the flat patterns or the model — we'll come back with a plan and a firm price, typically within one business day.