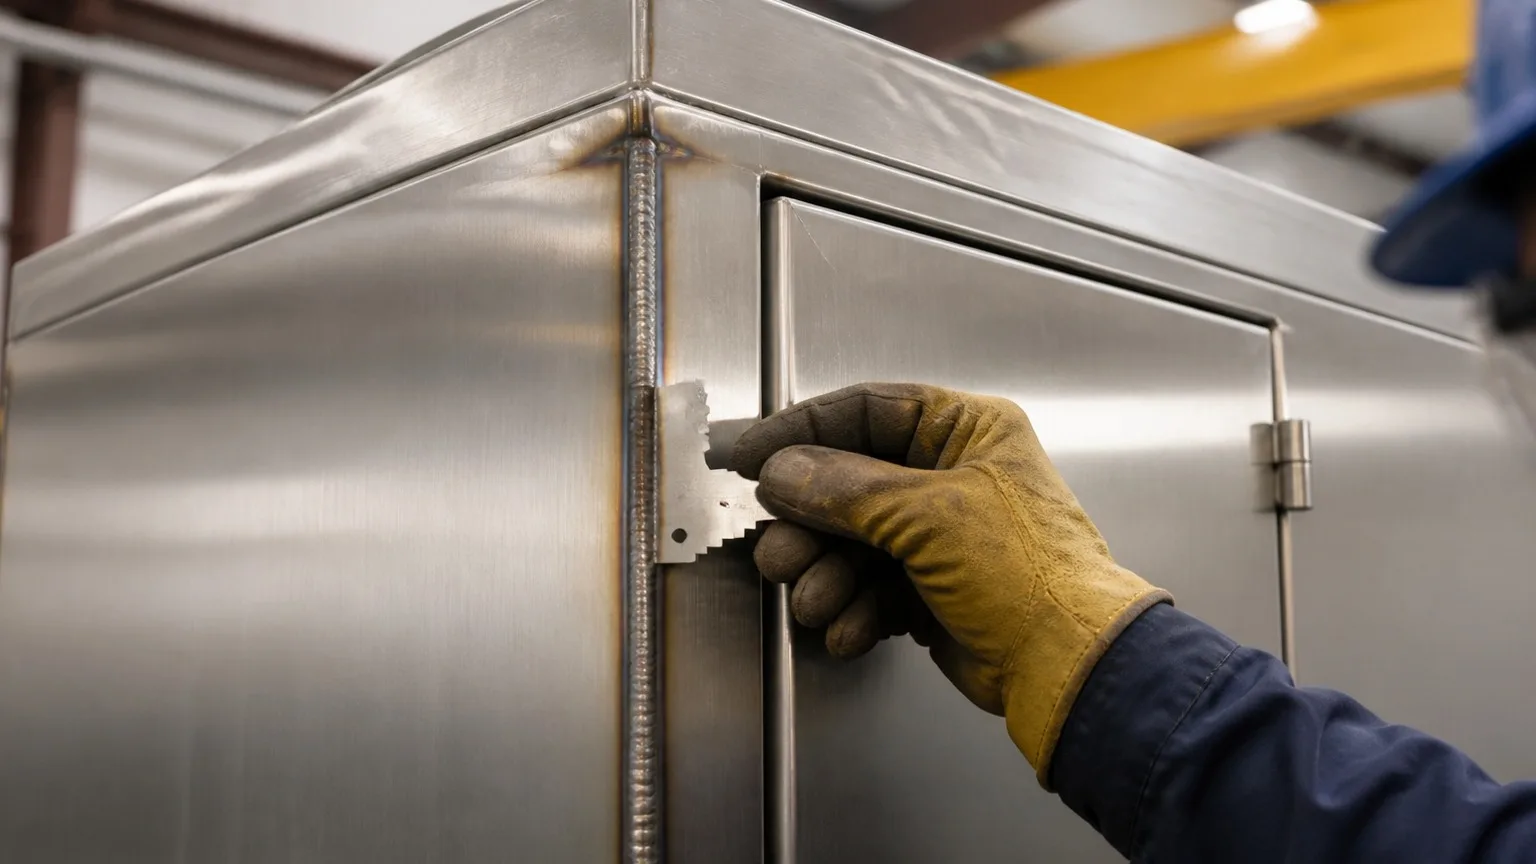
The finish is what the field sees for forty years. In-house blast and powder coat for cabinets and enclosures, hot-dip galvanizing to ASTM A123 for structures, and duplex systems where the environment demands both.
A substation structure is specified to last the life of the substation; a transformer cabinet is expected to look the same after a decade on a pad in the Gulf humidity. Both outcomes are decided in finishing — surface prep, coating system, film build, and the documentation that proves it — and FabTek treats finishing as a production process with the same controls as cutting and welding.
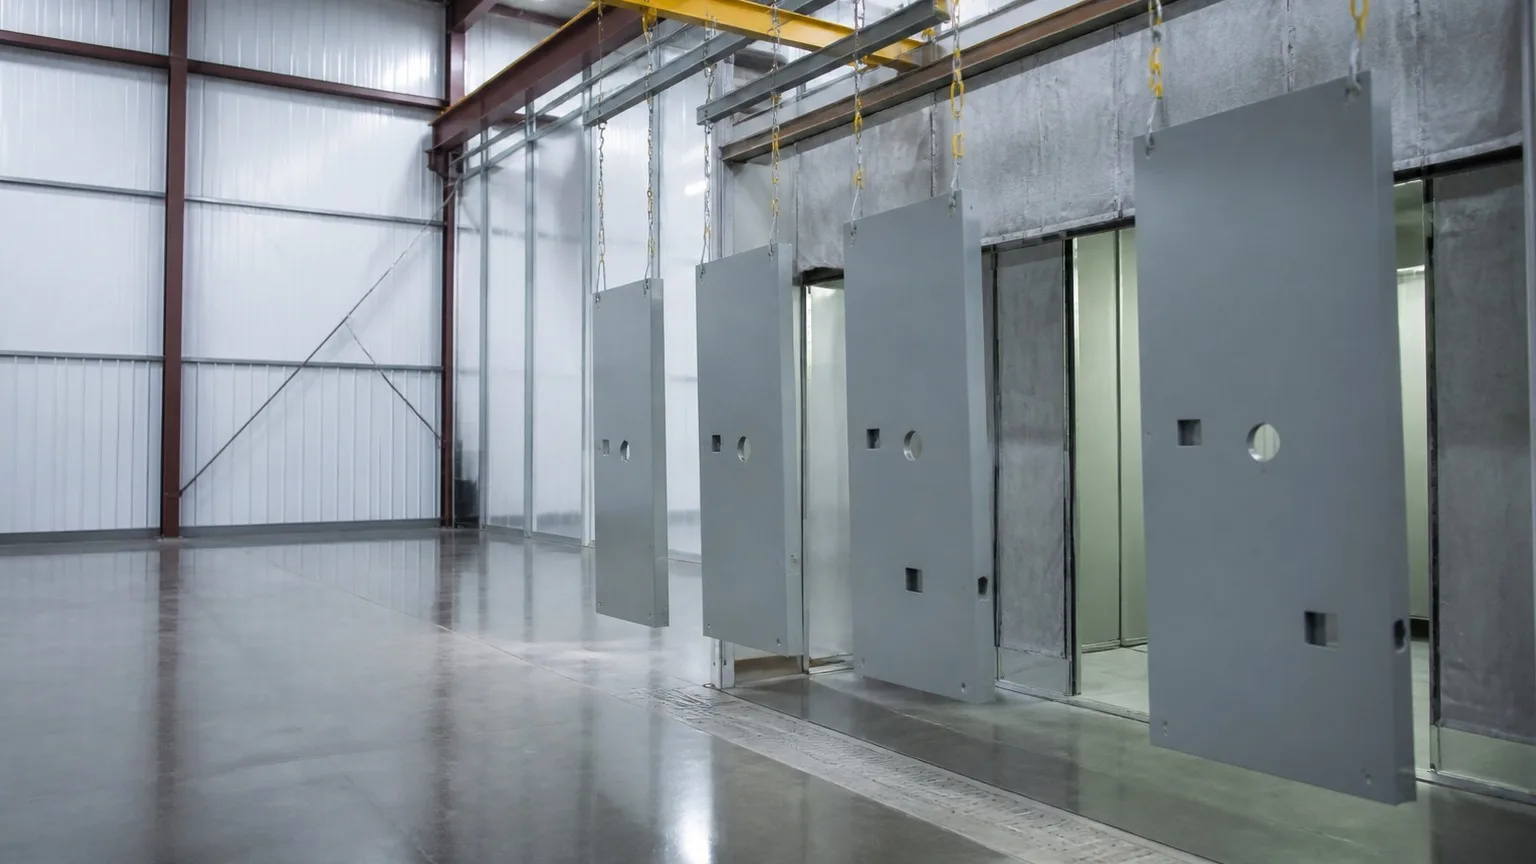
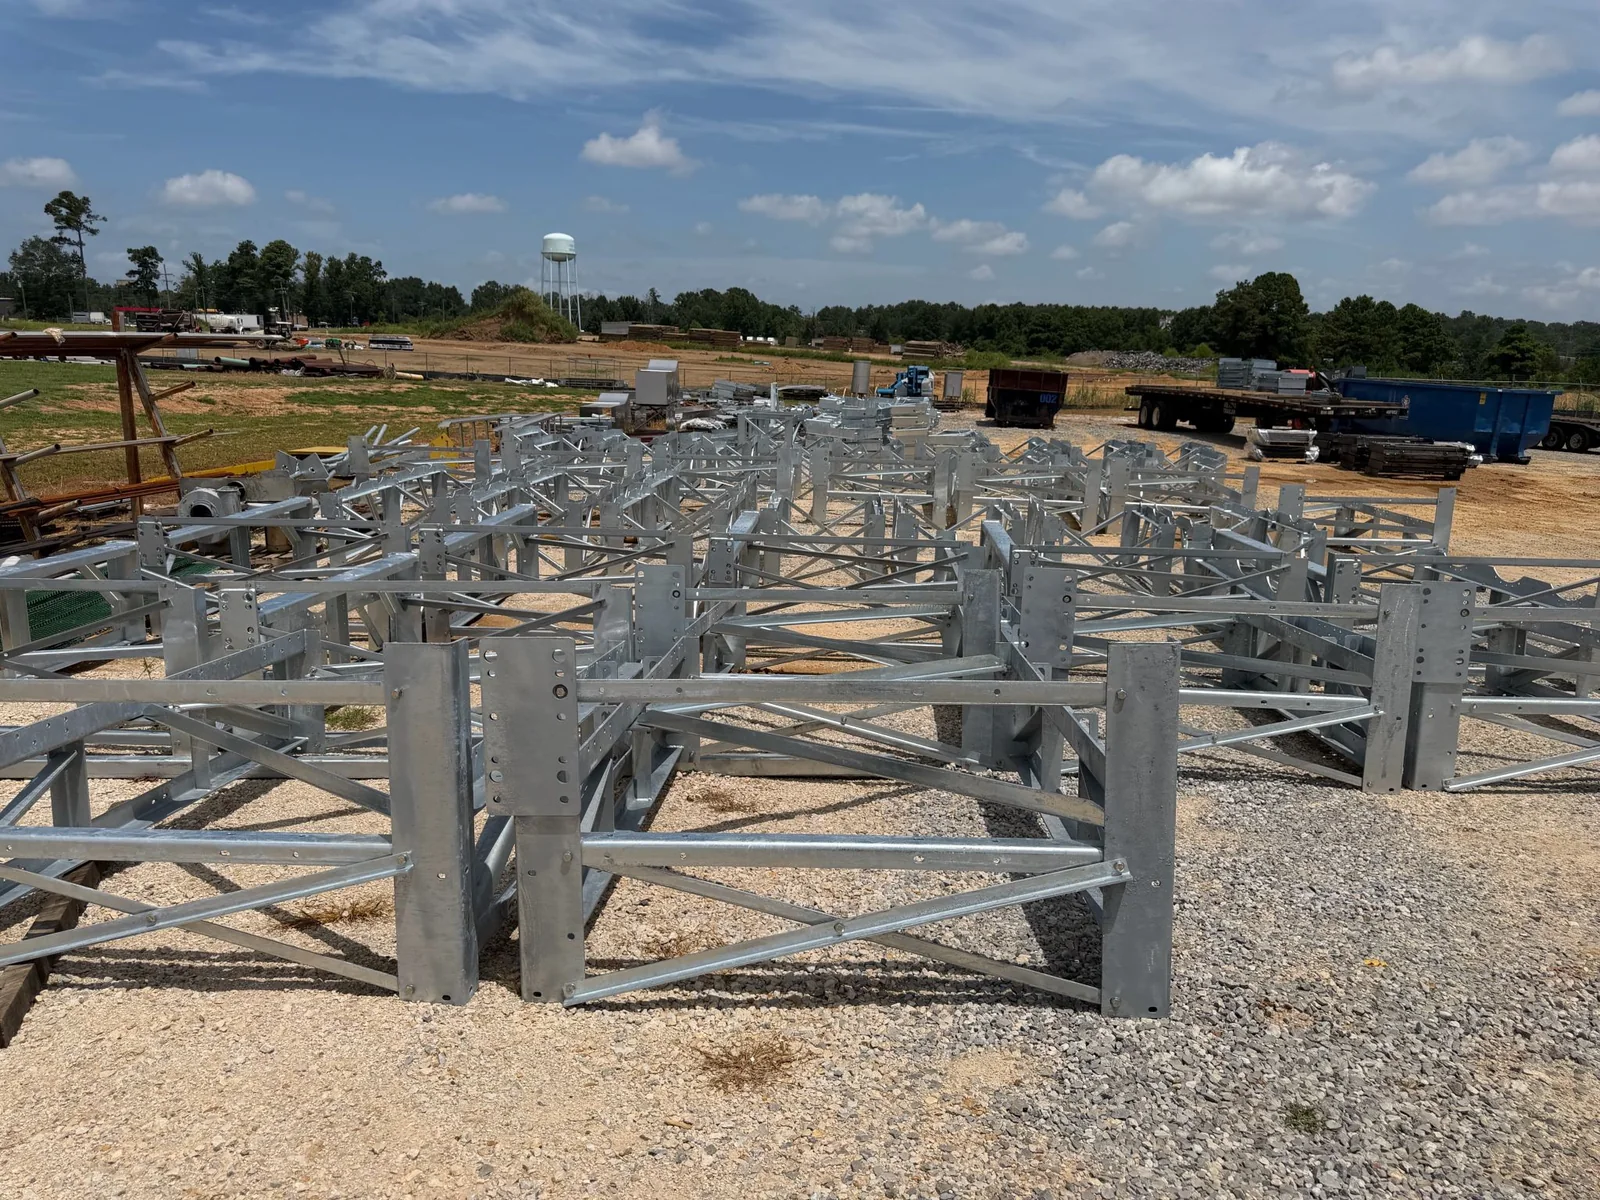
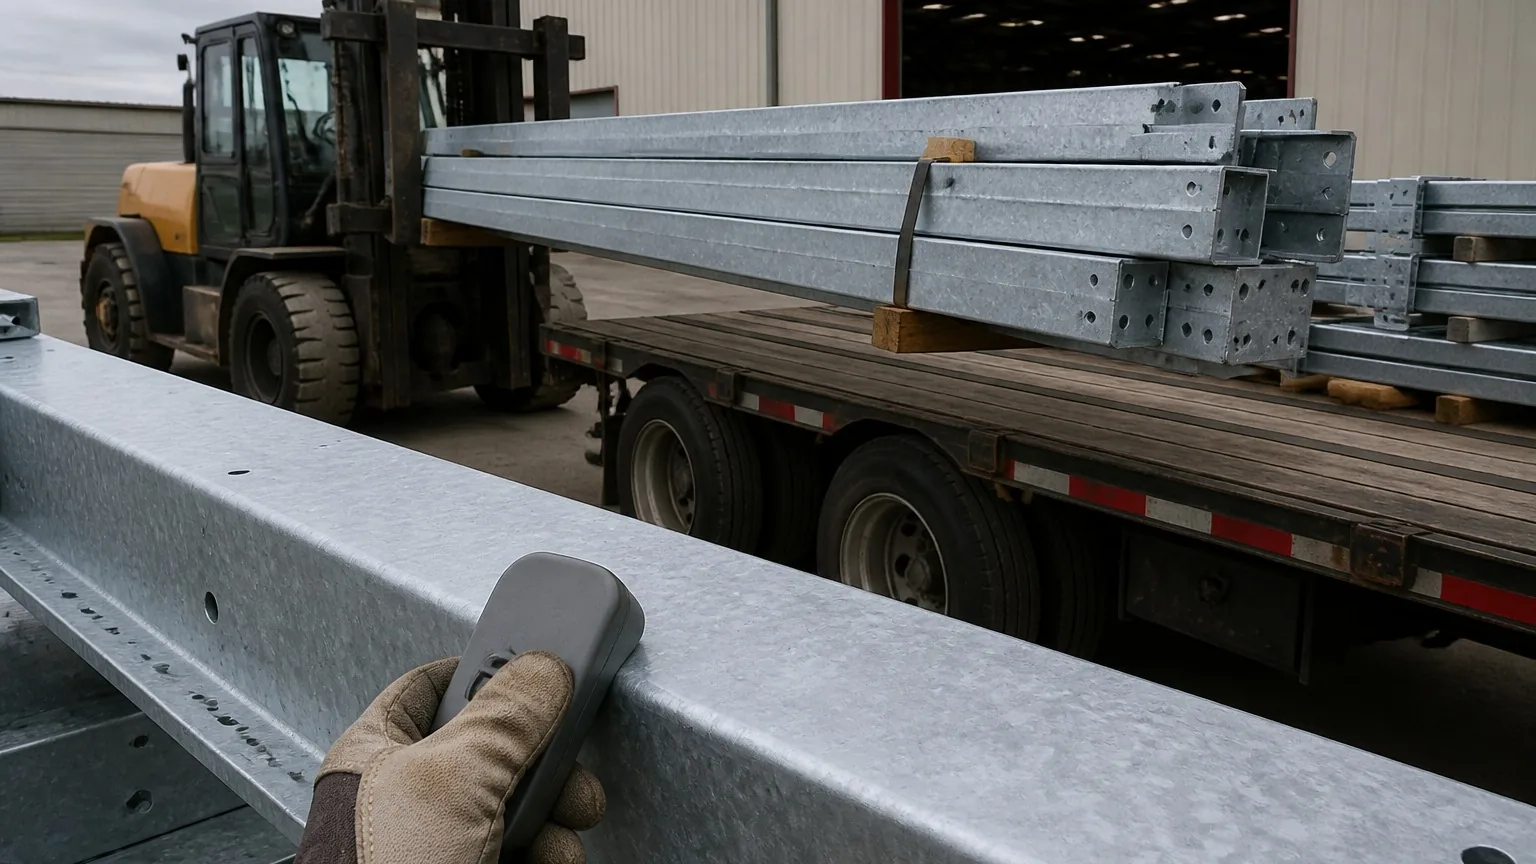
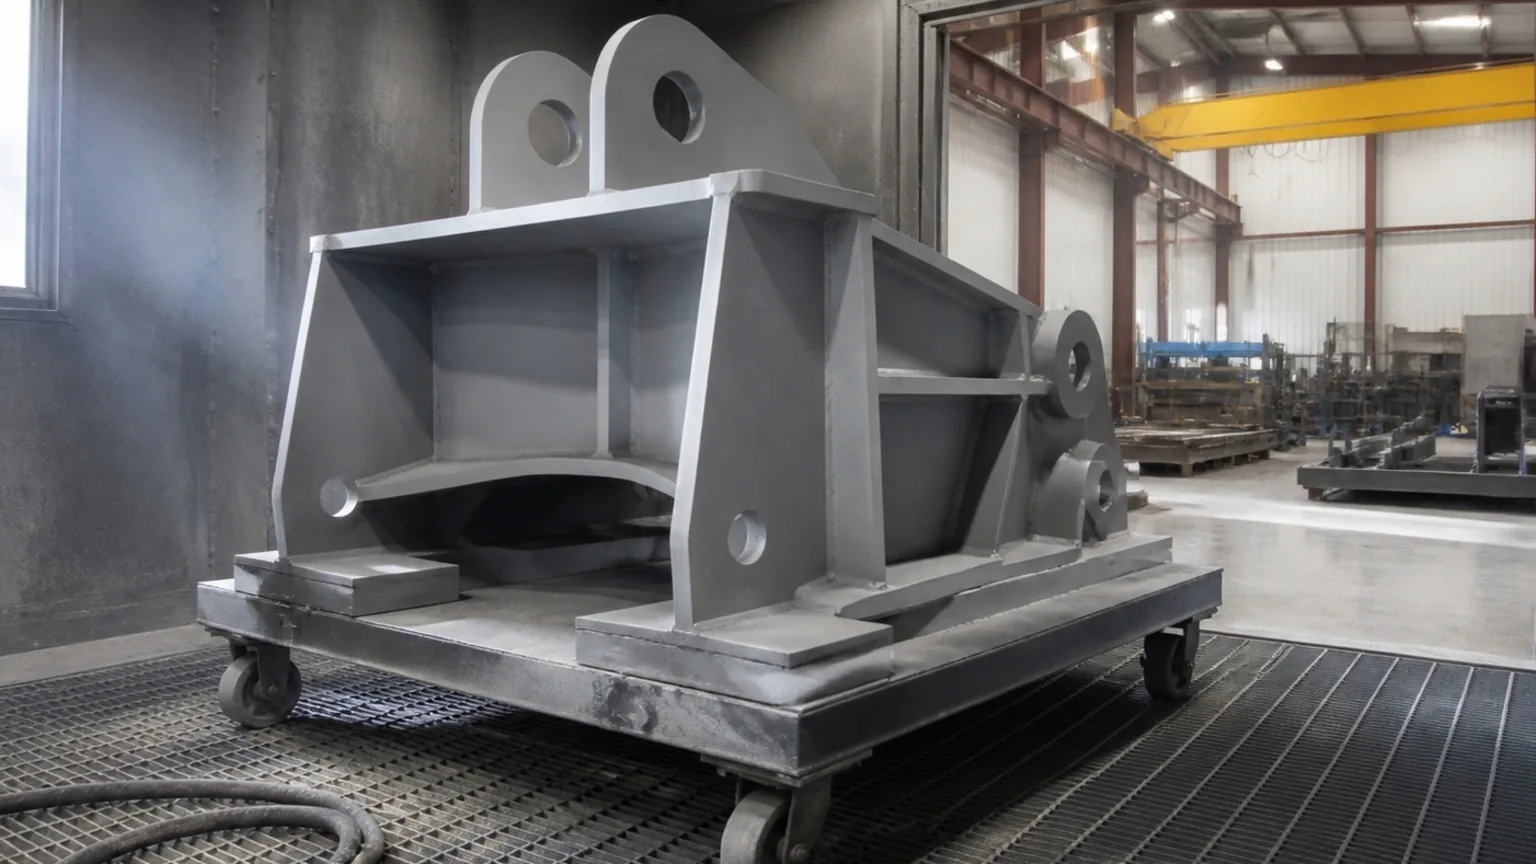
Cabinets, enclosures and light structures are media-blasted and powder-coated on our in-house line at Hazlehurst, Mississippi, which finishes hundreds of enclosures a month and carries an IEEE 2000-hour salt-spray rating. Powder coat is our primary finish for cabinets, enclosures, tanks and light structures. Structural steel for substations and transmission is hot-dip galvanized to ASTM A123 (hardware to A153) at qualified partner galvanizers — as with virtually every structural fabricator, the kettle is a specialist's operation — while FabTek owns everything around it: detailing the steel to galvanize cleanly, staging and hauling to the kettle, receiving inspection for coating thickness and appearance, and delivering the galvanizing certificates with the material and weld records. Where a coastal or industrial atmosphere calls for it, we supply duplex systems — galvanized then powder-coated — and specify the pretreatment that makes the two layers bond.
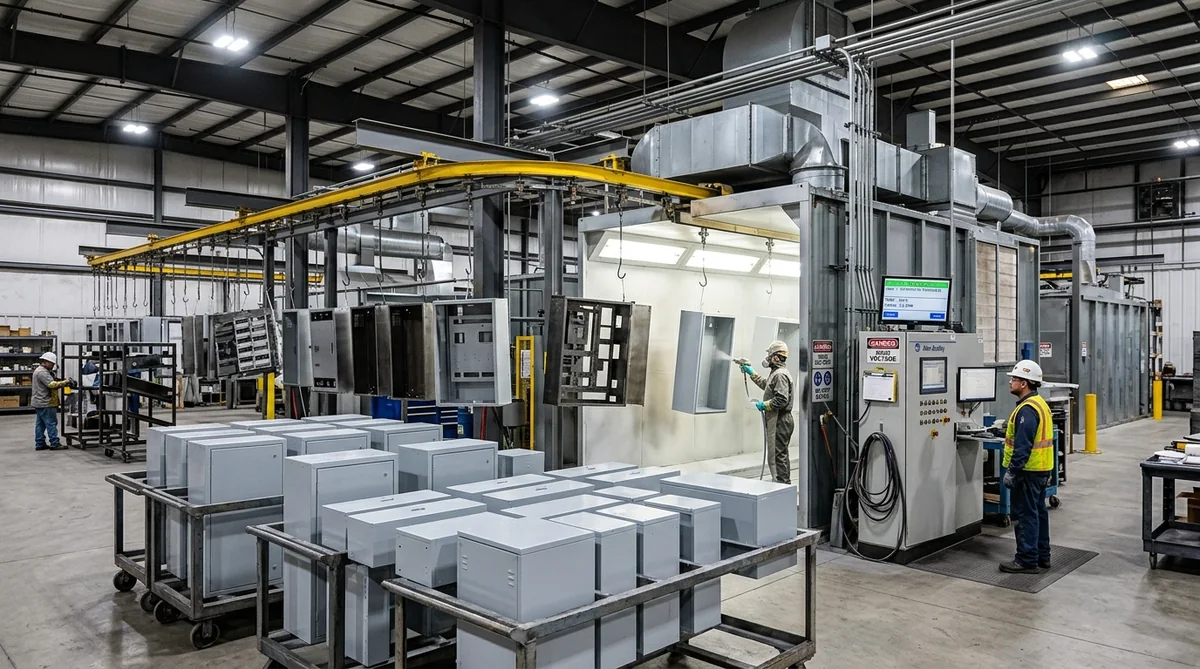
Electrostatic powder on carbon steel, galvanneal, stainless and aluminum; ANSI 61/70 gray, Munsell green, RAL and custom colors; film build to specification.
ASTM A123 on structural shapes, plate weldments and assemblies through qualified partner galvanizers; A153 on hardware; venting and drainage detailed at fabrication so the piece galvanizes cleanly, and coating inspected on return.
In-house blast room for SSPC-SP profiles ahead of powder coat, galvanizing or field paint.
Galvanized-plus-powder-coat duplex and customer-specified coating systems where a project calls for them.


Substation and transmission structures (galvanized); transformer cabinets, switchgear and control enclosures (powder coat); coastal and Gulf Coast installations (duplex or 4X stainless); data center yard equipment where appearance and longevity both matter.
| Powder coat | In-house line; IEEE 2000-hour salt-spray rated; film thickness per spec — see our film thickness spec sheet |
|---|---|
| Galvanizing | Hot-dip to ASTM A123 (structures), ASTM A153 (hardware), at qualified partner galvanizers with FabTek receiving inspection — which spec applies |
| Surface prep | Media blast to SSPC-SP 6/10 as specified; chemical pretreatment ahead of powder |
| Duplex | Galvanized + powder coat with sweep blast or chemical pretreatment for adhesion |
| Testing & docs | Film thickness readings, salt-spray certification, galvanizing certificates, coating inspection records |
| Colors | ANSI 61 / 70 gray, Munsell 7GY3.29/1.5 green, RAL and custom match |
| Also specified as | Galvanized substation structures, galvanized substation steel, powder coated enclosures, powder coating electrical enclosures, duplex coating, hot-dip galvanized steel fabrication |
Representative capabilities — exact ranges, ratings, and finishes are confirmed per project. Send drawings for a firm quote.
Steel that isn't detailed for the kettle comes out with trapped zinc, warped members or bare spots. FabTek's detailers add vent and drain holes, avoid closed cavities and sequence welds so assemblies galvanize cleanly the first time. Our step-by-step guide to substation steel fabrication and galvanizing walks through it, and galvanizing vs. paint covers when to specify each.
Built at four production sites in Hazlehurst, Mississippi.
ISO 9001:2015 quality management, AWS-certified welding, OSHA-compliant facilities.
In-house powder coat backed by an IEEE 2000-hour salt-spray certification.
Reserved-line capacity and the automation to grow with your volume.
Yes — dead-ends, A-frames, bus supports and equipment stands are hot-dip galvanized to ASTM A123 through our qualified galvanizing partners, inspected on return and delivered with galvanizing certificates. Galvanizing is outsourced across the industry; what differs is how well the steel is detailed for the kettle and inspected afterward.
Yes — media blasting and powder coat are on our own line in Hazlehurst, Mississippi, finishing hundreds of enclosures a month with an IEEE 2000-hour salt-spray rating.
FabTek fabricates and galvanizes substation and transmission steel at its Mississippi plants and ships nationwide, with field erection available.
Yes — for coastal and industrial atmospheres where both barrier and cathodic protection are wanted.
Explore related lines: Substation structures · Dead-end & A-frame structures · Transformer cabinets · Capabilities & equipment
Further reading: ASTM A123 vs. A153 · Galvanizing vs. paint for substation steel · Powder coat film thickness · IEEE 2000-hour salt spray


Send the coating specification with the drawings — we'll quote the finish with the fabrication.