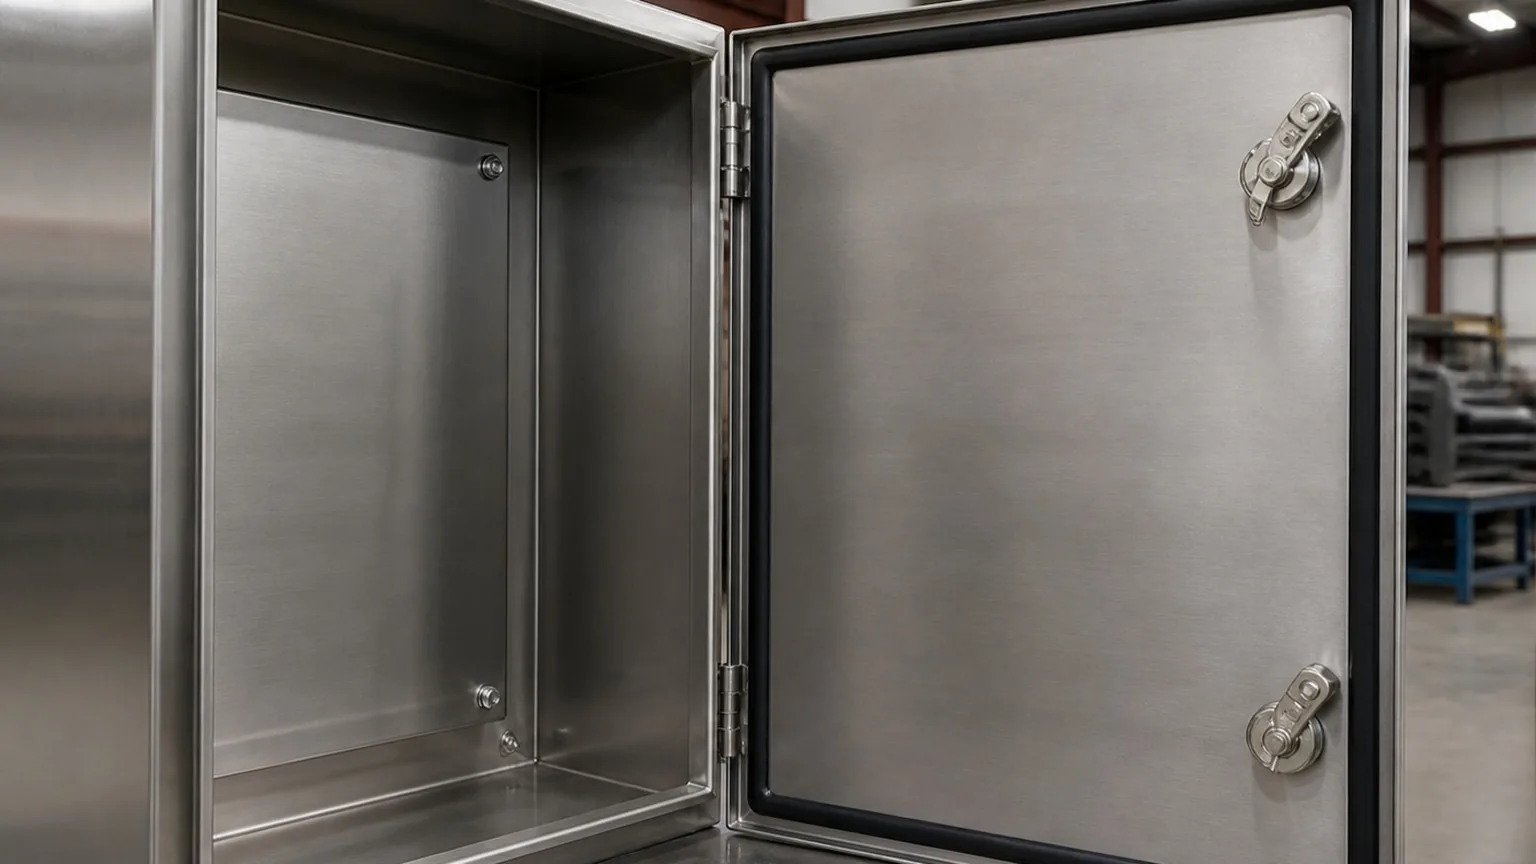
A dedicated laser welding cell for the seams MIG and TIG distort — thin sheet, long cabinet and enclosure seams, stainless and aluminum — with low heat input, minimal cleanup and a seam that is nearly invisible after powder coat.
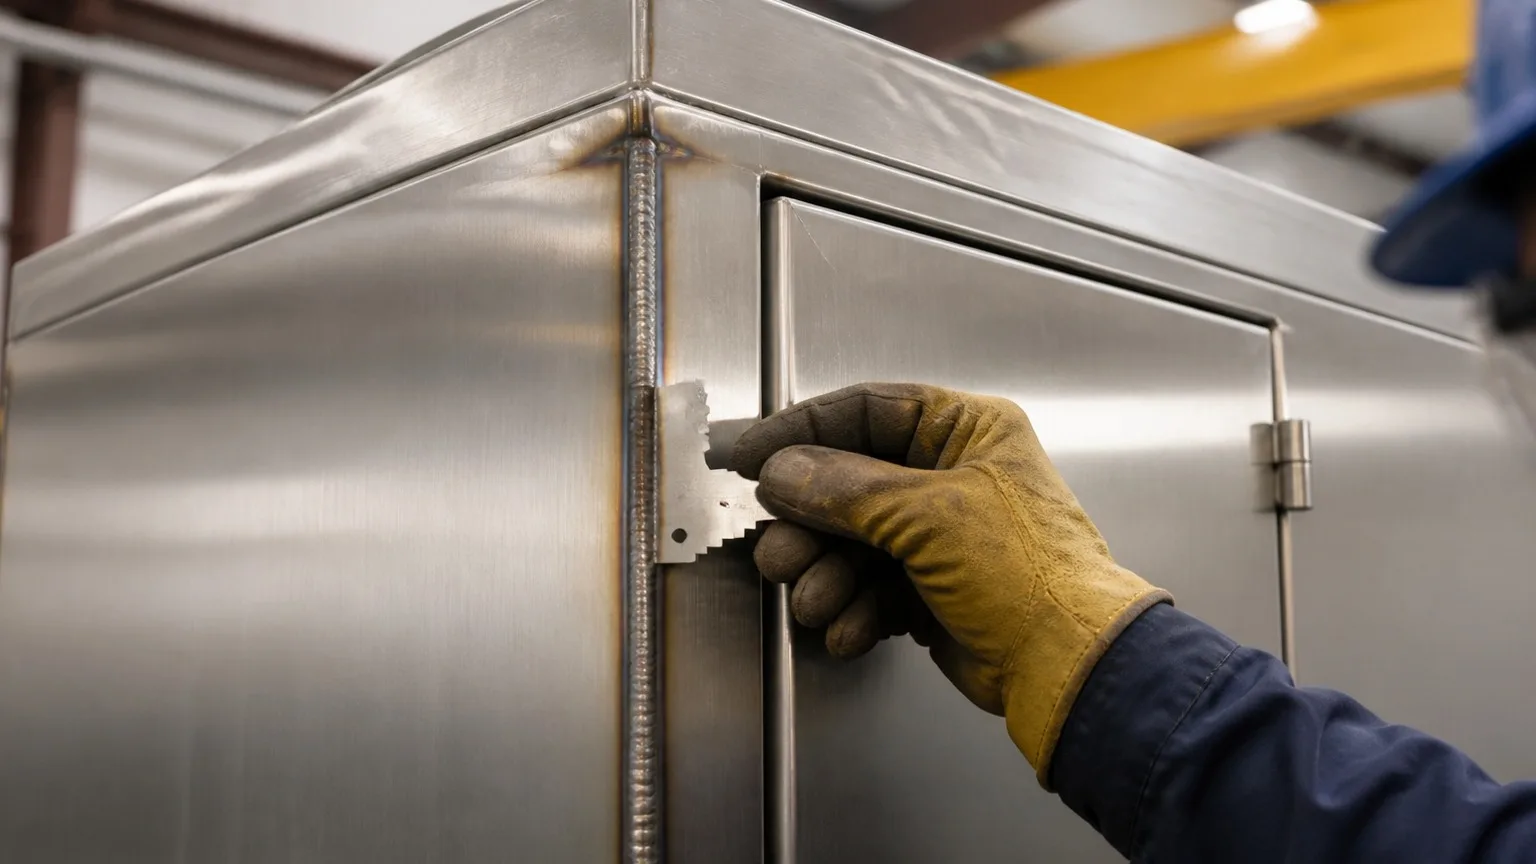
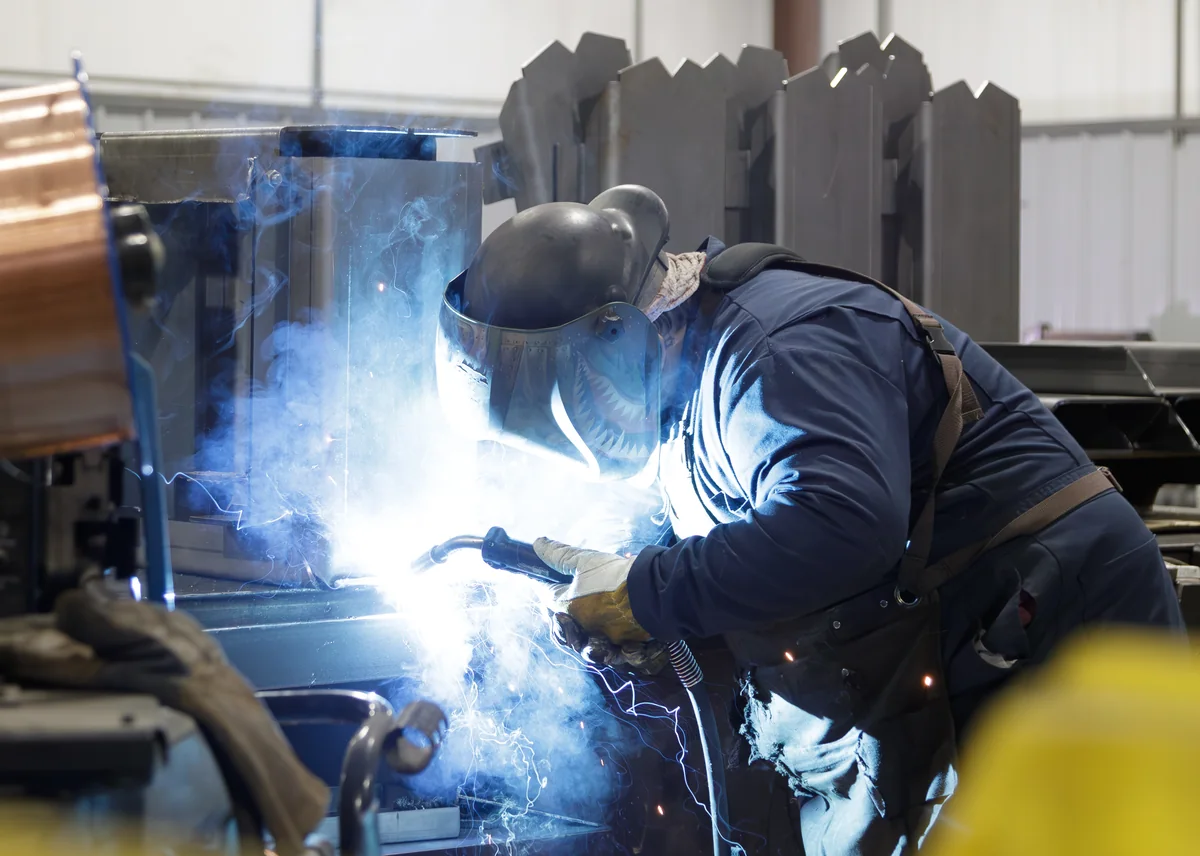
Welding thin sheet with a conventional arc puts heat into a part that has very little mass to absorb it, and the result is a cabinet door that oil-cans or an enclosure wall that waves. Laser welding puts a concentrated beam on the joint, fuses it fast and moves on, so the heat-affected zone is narrow, distortion is minimal and the seam needs little or no grinding. For the outdoor cabinets and enclosures FabTek powder coats to a 2,000-hour salt-spray standard, that means a flatter panel and a cleaner finish.
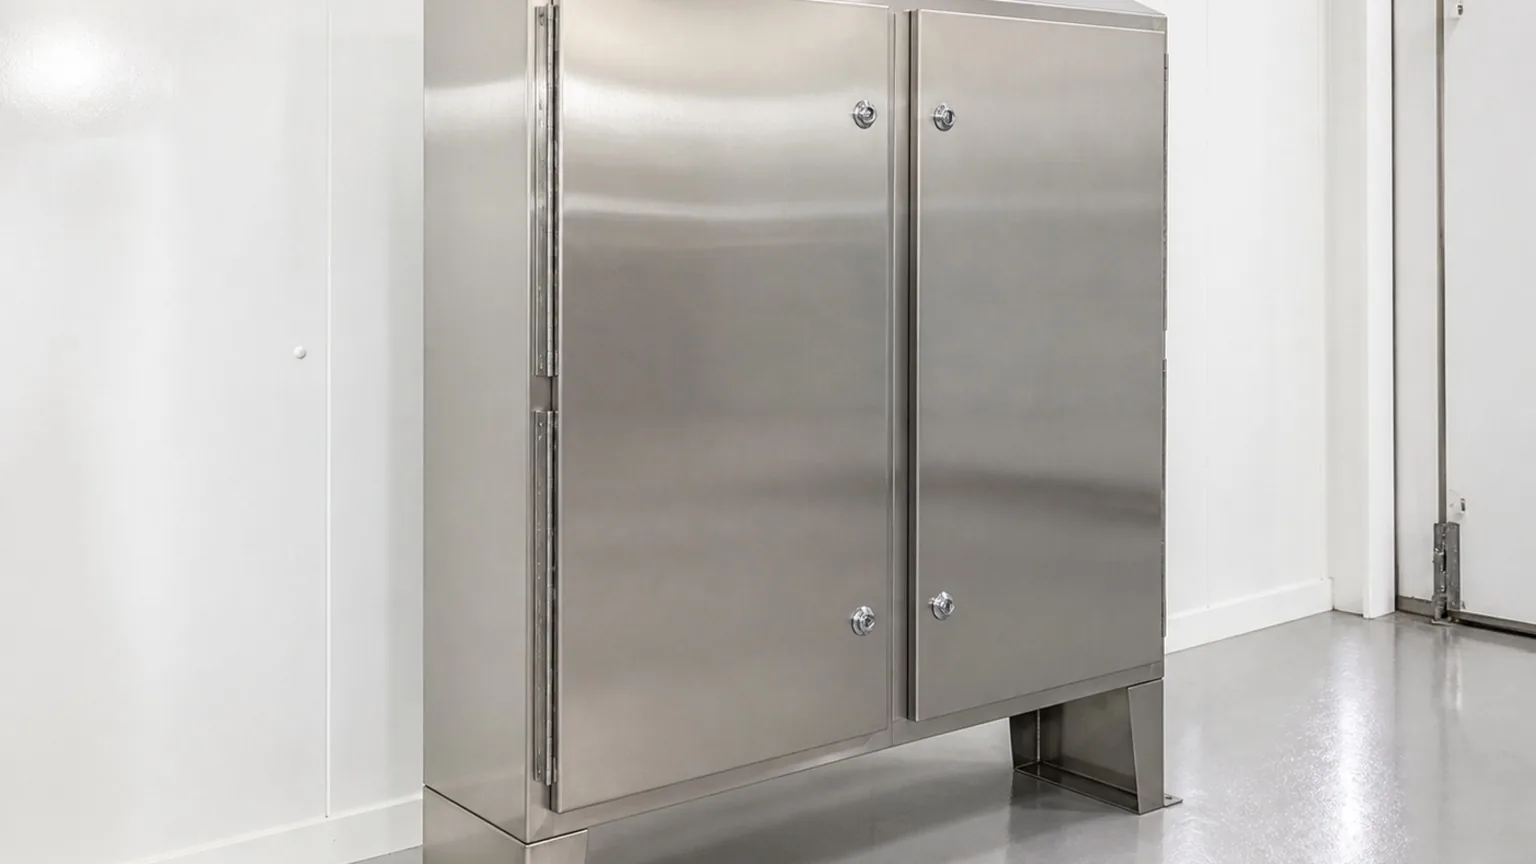
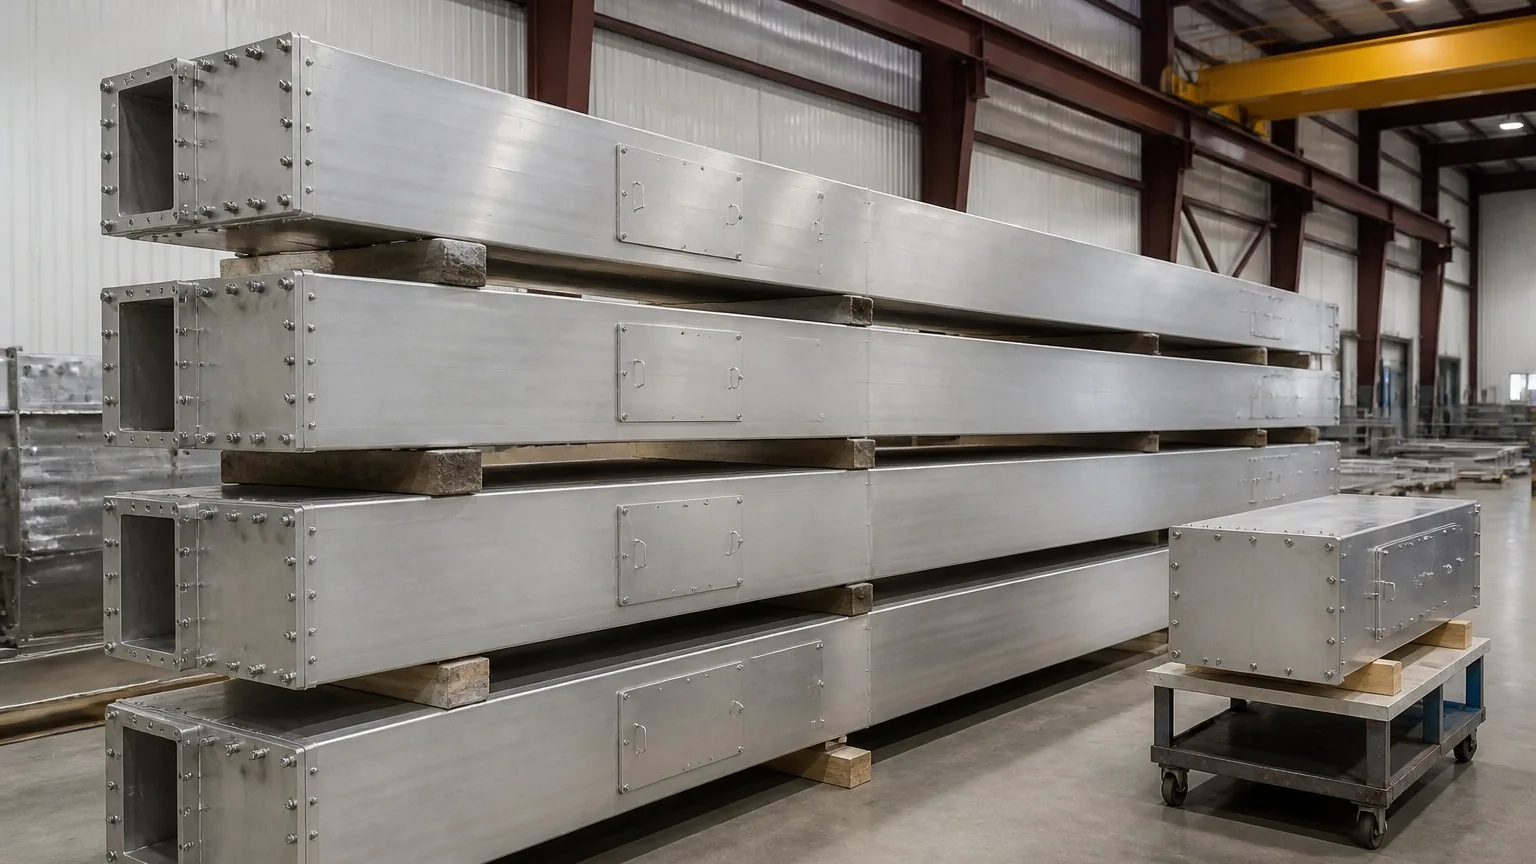
FabTek's laser welding cell handles the seams where that matters: long corner seams on cabinet and enclosure bodies, stainless 4X enclosure seams that would otherwise need grinding and re-polishing, aluminum busway housings, and thin-gauge parts that an arc would burn through. The cell sits with the other welding cells, so a cabinet can have its structural welds made by MIG and its show seams made by laser on the same floor.
Long, straight seams on transformer cabinets, control cabinets and NEMA enclosure bodies with minimal distortion.
4X and sanitary seams welded clean enough to passivate without heavy grinding.
Bus duct and busway housing seams with low heat input.
Light-gauge covers, doors and panels that arc welding would burn through or warp.
Precise, low-heat tacks for assemblies that go on to finish welding.

Enclosure and housing seams where distortion matters.

Low heat input, narrow seam, minimal spatter and warp.

Seams need less grinding before finish.

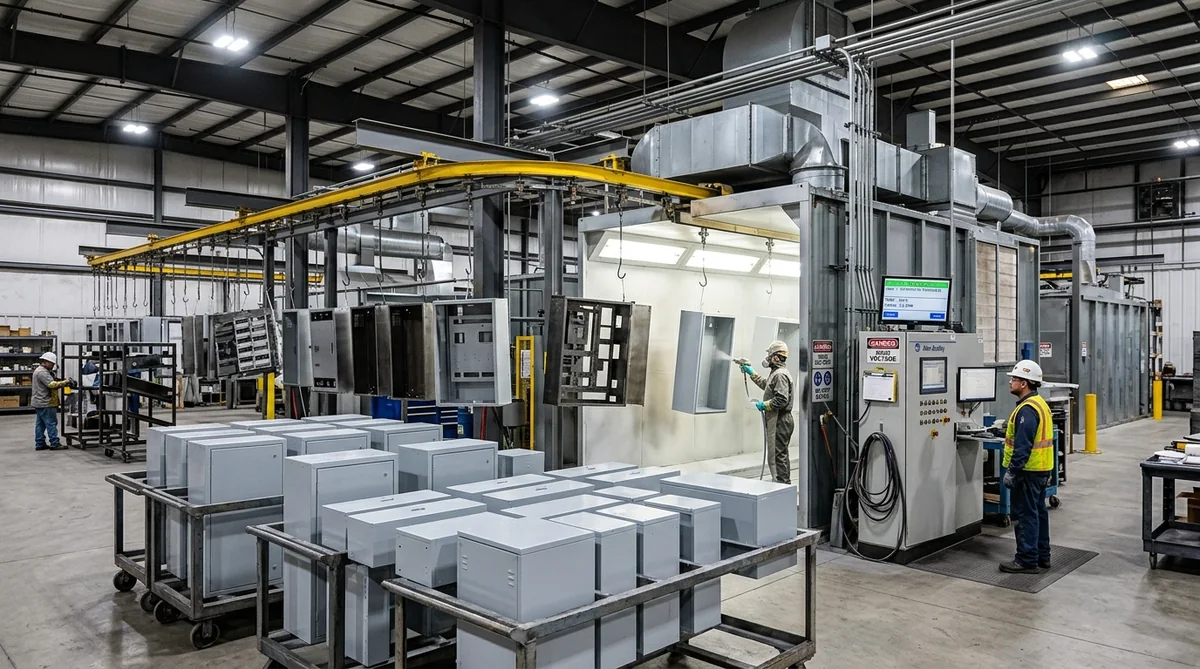
Enclosures go to blast and powder coat or ship brushed.

Powder-coated outdoor cabinets and enclosures — transformer cabinets, NEMA 3R and 4X enclosures, control cabinets, PDU and UPS cabinets — plus bus duct and busway housings and stainless sanitary conveyor parts.
| Cell | Dedicated laser welding cell (HK and Airgas laser welding systems) |
|---|---|
| Materials | Carbon, galvanized and galvanneal sheet, stainless, aluminum |
| Joints | Corner, lap and butt seams on thin sheet; long straight seams; tack welding |
| Advantages | Narrow heat-affected zone, minimal distortion, little or no grinding, clean seam under powder coat |
| Codes | Welded to written procedures under ISO 9001:2015; AWS D1.3 and D1.6 qualifications where applicable |
| Downstream | Weld dressing, passivation for stainless, powder coat on site |
| Also specified as | Laser welding services, laser beam welding, low-distortion welding, sheet metal laser welding, stainless laser welding, thin gauge welding |
Representative capabilities — exact ranges, ratings, and finishes are confirmed per project. Send drawings for a firm quote.
A cabinet's finish is judged at the seams. A MIG seam on thin sheet has to be ground flat, and the grinding thins the sheet and leaves marks that powder coat highlights. A laser seam is narrow and low-profile from the start, so it goes to blast and powder coat with a light dressing at most. On the outdoor enclosures FabTek builds, that is the difference between a corner that looks welded and a corner that looks formed — see powder coat film thickness for outdoor enclosures for how the finish is specified.
Built at four production sites in Hazlehurst, Mississippi.
ISO 9001:2015 quality management, AWS-certified welding, OSHA-compliant facilities.
In-house powder coat backed by an IEEE 2000-hour salt-spray certification.
Reserved-line capacity and the automation to grow with your volume.
Laser welding fuses a joint with a focused beam rather than an arc, putting far less heat into the part. It is used for thin sheet, long seams, stainless and aluminum where distortion and appearance matter.
FabTek Industries runs a dedicated laser welding cell at its Hazlehurst, Mississippi plants alongside MIG and TIG cells, with forming and powder coat on the same site.
For the thin-sheet joints it is used on, yes — the joint is fully fused. Structural joints on heavy material are welded by MIG or TIG to AWS D1.1 in the structural cells.
The narrow heat-affected zone keeps heat tint to a minimum, and stainless seams are passivated in the stainless cell before finish.
Explore related lines: Transformer cabinets · NEMA 4 & 4X enclosures · Control cabinets · Bus ducts & busways
Further reading: Powder coat film thickness for outdoor enclosures · AWS D1.1 vs D1.3 vs D1.6 · Manual to automation in metal fabrication


Have thin-sheet or stainless seams that keep warping? Send the drawings — we'll tell you where laser welding fits and come back with a price and date, typically within one business day.