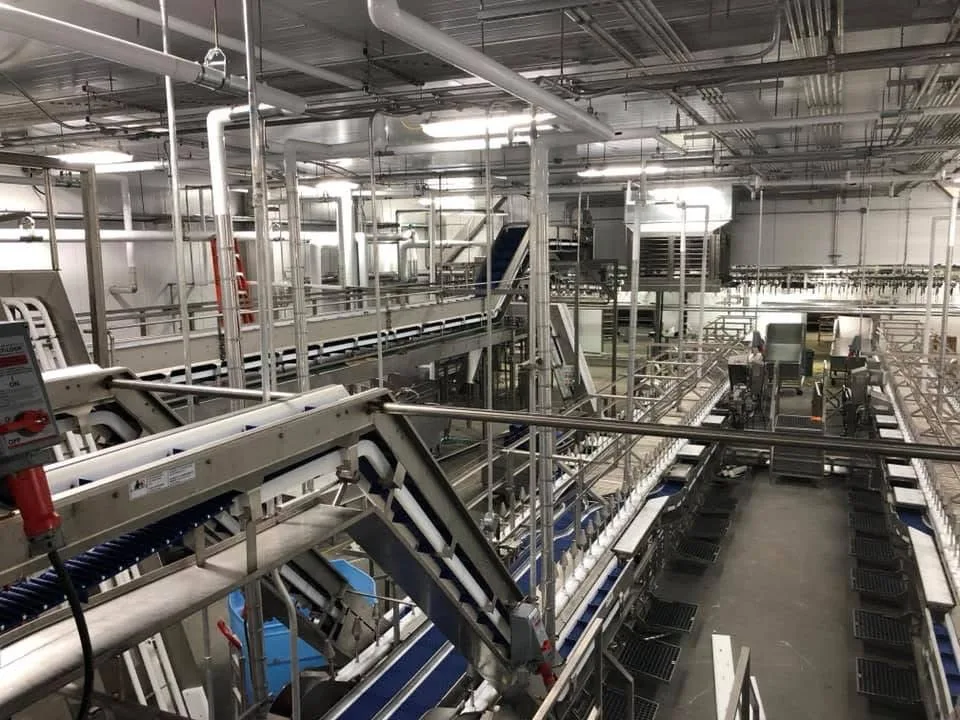
A well-built conveyor lasts 15 to 20 years with maintenance. Its controls need refreshing every 7 to 10. Much of the conveyor running in Southeastern poultry plants, feed mills, sawmills and distribution centers today was installed during the expansion wave of the 2000s, which means a large share of it is at or past the point where the question is no longer whether to spend money on it, but how. There are three answers, and the right one depends on the frame, the duty and the plant's plans.
Have a line that is costing you maintenance hours? Call 601.892.5017 or email sales@fabtekindustries.com — we assess, retrofit, rebuild and replace conveyors from any manufacturer.
- Benchmarks: 15–20 years mechanical life with maintenance, 7–10 years for controls; abrasive, corrosive or washdown duty shortens both unless the conveyor was built for it.
- Retrofit when the frame is sound and the layout fits; rebuild when the design is right but the metal is worn; replace when the process has changed or the frame is gone.
- 61% of plants reported unplanned downtime in the past year in a 600-respondent 2025 survey; a stopped conveyor stops everything downstream.
- Warning signs: repeat bearing and drive failures, belts that will not track, worn-through troughs, shimmed supports, obsolete controls, climbing maintenance hours.
- Conveying Hard, Heavy Powders
- Bulk Conveying Over Distance & Height
- Material Handling for Federal & Defense Facilities
- Custom vs. Catalog Conveyors
- Reshoring: The Factory Comes to Life at Fit-Out
- Section 232 Tariffs & Built in the U.S.A. Conveyors
- Conveyor Installation: Drawing to First Run
- Retrofit, Rebuild or Replace (you are here)
- Sanitary & Washdown Conveyors for Poultry, Meat & Food
- How to Get a Conveyor Quote From FabTek
Why it matters now
In a 2025 survey of more than 600 plant leaders in food and beverage, automotive, life sciences and oil and gas, 61% reported unplanned downtime in the past year and nearly half of those reported six to ten incidents a week. The headline cost figure in that survey, about $1.7 million per hour, reflects large process plants; a poultry line or a feed mill loses less per hour, but a stopped conveyor stops everything downstream of it. And a plant that cannot hire maintenance millwrights — the trade is projected by the Bureau of Labor Statistics to grow 14% through 2035 with roughly 51,900 openings a year — cannot keep nursing an old line indefinitely.
Retrofit: the frame is sound, the components are not
Retrofit keeps the structure and replaces what wears or what is obsolete: drives and gearboxes, bearings and idlers, belting or chain, wear liners, guards to current standards, and controls. It is the right choice when the frame and supports are straight and uncorroded, the layout still fits the process, and the goal is reliability and safety rather than capacity. A controls retrofit alone can add a decade of useful life to a mechanically sound conveyor.
Rebuild: the design is right, the condition is not
Rebuild goes further: sections are removed, stripped, repaired or re-fabricated, refinished and reinstalled with new wear and drive components. It suits heavy-duty conveyors in abrasive or corrosive service where the original design still works but the metal has worn thin, and conveyors whose replacement would require re-engineering the whole line. Because FabTek fabricates, a rebuild can replace troughs, flights, frames and supports with new steel to the original or an improved design, often section by section during planned outages.
Replace: the process has changed
Replacement is the answer when capacity, product, layout or sanitation requirements have moved beyond what the original conveyor was built for, when the frame is corroded or damaged, or when the cost of a rebuild approaches the cost of new. A replacement designed by a fabricator can reuse existing supports and platforms where they are sound, correct the transfer points that caused trouble in the first place, and be installed in phases — see Part 7 for how.
Warning signs to act on
- Repeated bearing and drive failures on the same conveyor.
- Belts or chains that will not track no matter how they are adjusted.
- Worn-through troughs, flights or wear strips.
- Support steel that has been patched, shimmed or braced.
- Guards that no longer meet current standards.
- Obsolete controls with no spare parts available.
- Maintenance hours that climb every quarter.
Any two of these together usually mean the retrofit window is closing.
How FabTek handles all three
Our crews inspect and assess existing conveyors, our engineers design the retrofit, rebuild or replacement, our shops fabricate what is needed, and the same crews install it, usually around production. Because we build the structure as well as the conveyor, the fix extends to supports, platforms and guards rather than stopping at the conveyor's edge. That is the model behind our industrial services group, and it applies to conveyors from any manufacturer.
Frequently asked questions
How long does a conveyor last?
With regular maintenance, typically 15 to 20 years for the mechanical system and 7 to 10 years for controls. Abrasive, corrosive or washdown service shortens that unless the conveyor was specified for it.
Is it cheaper to retrofit or replace a conveyor?
Retrofit is cheaper when the frame is sound and the layout still fits. Replacement is cheaper over the life of the line when the frame is worn or the process has changed. A rebuild sits between the two for heavy-duty conveyors with a good design and worn metal.
Can you rebuild a conveyor that FabTek did not build?
Yes. We assess, retrofit, rebuild and replace conveyors from any manufacturer.